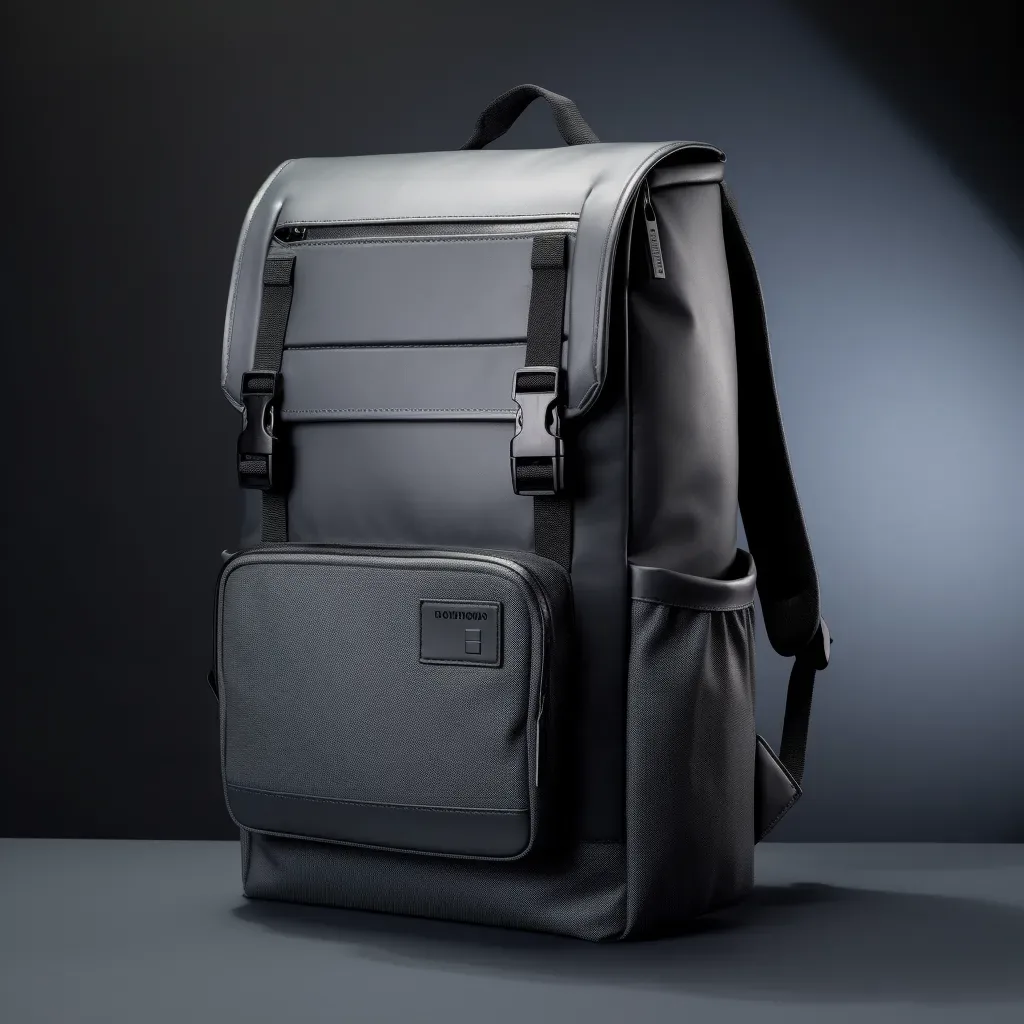
A great business bag is an engineering achievement. Behind the clean exterior of a premium briefcase or backpack lies a complex system of weight distribution calculations, impact absorption engineering, modular organization architecture, and material science tradeoffs — all balanced against cost targets and brand aesthetics. This technical guide explores the functional design principles that separate exceptional business bags from mediocre ones, and how OEM manufacturers translate these principles into production reality.
With over 20 years of OEM and ODM experience, Bespoke Bags has engineered and manufactured business bags for brands across 40+ countries. Our SGS-verified 4,950 m² production floor in Quanzhou, Fujian Province houses dedicated prototyping labs, material testing equipment, and ergonomic assessment tools that inform every design decision. This guide shares the technical knowledge we apply to business bag development — whether you are launching a new brand, expanding an existing line, or refining your current product's functionality.
Ergonomic Principles in Business Bag Design
Ergonomics in bag design is not optional — it is a fundamental determinant of product success. A business bag that causes shoulder strain, back pain, or hand fatigue will be abandoned regardless of how beautifully it is designed. The three core ergonomic principles guide every business bag we engineer.
Weight Distribution
The human body handles carried weight most efficiently when it is distributed across the largest possible contact area and positioned closest to the body's center of gravity. In practical bag design terms, this means:
- Backpack configurations: Weight should be distributed so that 60–70% rests on the hips (via a padded hip belt) and 30–40% on the shoulders. For business backpacks without hip belts, the target shifts to distributing load evenly across both shoulder straps with the heaviest compartment (typically the laptop sleeve) positioned closest to the back panel — within 5 cm of the spine. This positioning minimizes the lever arm effect that causes forward lean and shoulder strain.
- Messenger/sling configurations: The cross-body strap should position the bag's center of mass at the lower back, not the hip. The stabilizing strap (if present) should angle at 30–45° from shoulder to opposite hip. We design strap attachment points using triangulation geometry to prevent the bag from swinging during movement.
- Briefcase/handle carry: The handle should be positioned so that when the bag is lifted, its center of gravity falls directly below the grip point. An offset handle creates rotational torque that forces the wrist into ulnar deviation — a primary cause of repetitive strain. We test handle positioning using a simple plumb line test during prototyping: hang the bag from the loaded handle; if the bag's bottom tilts more than 10° from vertical, the handle position needs adjustment.
Center of Gravity Management
Beyond static weight distribution, the center of gravity must remain stable during dynamic movement — walking, running for transit, navigating stairs, or bending to retrieve items. Design strategies include:
- Low-profile base: Keeping the bag's depth (front-to-back dimension) narrow relative to its height reduces the pendulum effect during walking. For business backpacks, we target a depth-to-height ratio of 0.5–0.6. A 45 cm tall backpack should have a maximum depth of 22–27 cm when at typical load.
- Internal load stabilizers: Compression straps inside the main compartment secure contents and prevent weight shift. We use cam-lock buckles or speed-hook systems for one-handed adjustment.
- Weighted base construction: Some premium business bags incorporate a denser material or reinforced panel at the base to lower the overall center of gravity. This provides a self-standing property that also improves stability when set down.
Strap Pressure Point Engineering
The contact points between straps and the body are the most common sources of discomfort. Our strap engineering follows these specifications:
- Shoulder strap width: Minimum 38 mm (1.5") for bags under 5 kg, 50 mm (2") for 5–10 kg, and 65 mm (2.5") for 10+ kg loads. Width must increase proportionally with load to distribute pressure below the 3.5 kPa pain threshold on the trapezius muscle.
- Padding thickness: Closed-cell foam padding of 8–12 mm on shoulder straps. The foam density must be 40–60 kg/m³ to prevent bottoming out under load. We prefer contoured (S-curve or anatomical) strap shapes that follow the shoulder's natural curvature.
- Edge finishing: Strap edges must be bound or folded to eliminate hard edges that create pressure concentrations. We use bias tape binding on woven straps and folded-and-stitched edges on padded straps.
- Sternum strap: For backpack-style business bags, a removable sternum strap positioned at mid-chest height (sternal angle level) reduces shoulder strap spread by 25–30% and distributes load across the chest.
Laptop Protection Engineering
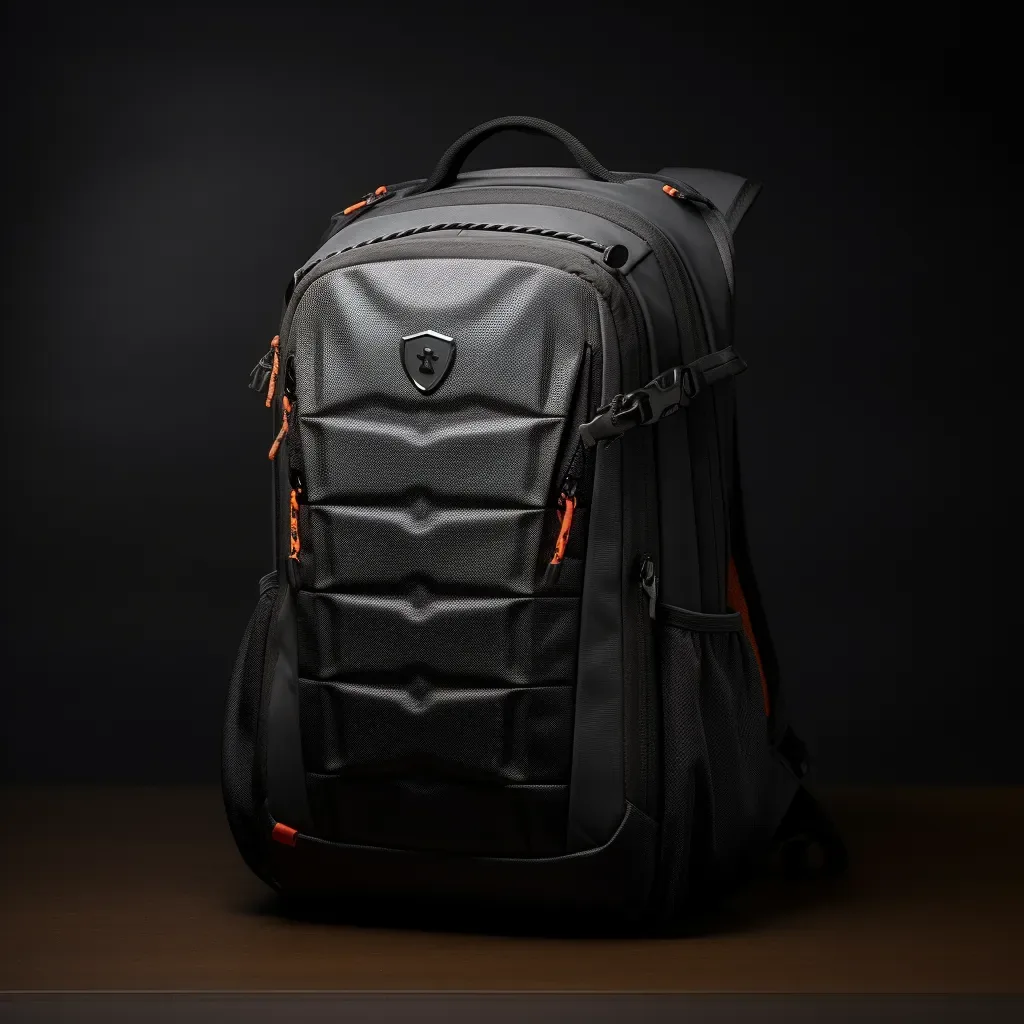
With business users carrying laptops valued at $1,000–$4,000+, the laptop compartment is the single most engineered zone in any business bag. Our protection system addresses impact, compression, moisture, and abrasion through multiple defense layers.

Padding Thickness and Material Selection
Laptop compartment padding is engineered based on the drop height scenarios a business bag will realistically encounter:
Key engineering decisions in padding specification:
- Density vs. thickness tradeoff: Higher-density foam provides equivalent protection at reduced thickness. A 10 mm layer of 60 kg/m³ EVA outperforms a 15 mm layer of 30 kg/m³ EVA in impact absorption — while adding less bulk and weight.
- Corner protection: Laptop corners are the most vulnerable point during drops because they concentrate impact force. We integrate TPU or silicone bumpers at all four corners of the laptop sleeve, with 3–5 mm thickness and a durometer of 60–80A (Shore scale) for optimal energy absorption.
- False bottom construction: The laptop sleeve should never sit flush with the bag's base. We engineer a 15–25 mm "false bottom" — a padded shelf that suspends the laptop above the bag's floor. This protects against drops when the bag is set down and prevents contact with moisture that may pool at the bag's base.
Suspended Laptop Sleeve Architecture
The gold standard in laptop protection is the suspended sleeve — a laptop compartment where the device is held in a "floating" position, surrounded by padding on all six faces and elevated above the bag's base. This design isolates the laptop from direct impact transmitted through the bag's exterior.
Construction approach:
- The sleeve is formed from two pieces of closed-cell foam-lined fabric, stitched together on three sides to create a pocket.
- The open top of the sleeve is attached to the bag's internal structure at the top edge only — typically via a binding tape that connects to an internal panel.
- This "top-hung" attachment means the sleeve is suspended from above, with no hard contact points on the sides or bottom. Impact forces applied to the bag's exterior are absorbed by the foam layers before reaching the sleeve.
- A hook-and-loop (Velcro®) closure strap at the top of the sleeve secures the laptop and prevents it from sliding out when the bag is opened.
Organization System Design
The organization system — the internal arrangement of pockets, dividers, and accessory holders — is where business bags earn their daily utility. A well-designed organization system reduces the time to locate items from 15–30 seconds (rummaging) to 1–3 seconds (targeted retrieval). Over a year of daily use, this translates to hours of cumulative time savings.
Modular vs. Fixed Organization
Two fundamental approaches to internal organization serve different user profiles:
Fixed organization: Permanent sewn-in pockets and dividers. Advantages: lower production cost, lighter weight, cleaner aesthetic, and more predictable user experience. Disadvantages: cannot adapt to changing needs, pockets may go unused while needed space is unavailable. Best for: minimalist users, brands targeting a single use case (e.g., "the lawyer's briefcase").
Modular organization: Removable and repositionable dividers, pockets, and accessory pods typically attached via Velcro, magnetic snaps, or clip rails. Advantages: user-customizable, adaptable across use cases, future-proof. Disadvantages: higher cost (+15–30%), additional weight from attachment hardware, potential for components to be lost. Best for: versatile professionals, tech users with evolving device ecosystems, brands targeting the "one bag for everything" market.
Essential Organization Components
Pen Loops with Elastic: A Design Detail That Matters
Pen loops seem simple but are among the most poorly executed features in mass-market business bags. Common failures include elastic that loses tension after 3 months, loops too narrow for thick markers, or loops placed too close together causing pen caps to interfere.
Our specification for pen loops:
- Elastic type: Woven elastic (not knitted) with 40–50% stretch recovery rate. Woven elastic maintains tension through 10,000+ stretch cycles compared to 2,000–3,000 for knitted elastic.
- Loop diameter: 8 mm relaxed, expanding to 12–14 mm under load. This accommodates pens from slim styluses (7 mm) to thick highlighters (12 mm).
- Loop spacing: Minimum 20 mm center-to-center to prevent pen caps from interfering with adjacent pens.
- Loop depth: 70–80 mm deep to secure pens through the cap end, which is typically the widest point and provides the most friction grip.
Accessibility Features
The best organization system is useless if accessing it is cumbersome. Accessibility engineering focuses on reducing the number of actions required to retrieve or store an item.
Quick-Access Pockets
A quick-access pocket provides external access to frequently needed items (phone, transit pass, keys, pen) without opening the main compartment. Design principles:
- One-hand operation: The closure must be operable with a single hand while the bag is being worn. Magnetic closures, oversized zipper pulls with glove-friendly tabs, and flip-top closures with magnetic catches all qualify.
- Positioning: Quick-access pockets should be located on the front panel or top lid, within natural hand reach when the bag is worn on the back or hip. For briefcases, the front face pocket with a horizontal zipper provides the most natural access angle.
- Depth management: Quick-access pockets should be shallow (80–120 mm depth) to prevent items from sinking to the bottom. A "false bottom" pad or angled floor keeps contents near the opening.
Magnetic Closures
Magnetic closures provide silent, effortless opening and closing — ideal for professional environments. Specifications:
- Magnet type: Neodymium (NdFeB) magnets rated at N35–N42 for strong hold without excessive force.
- Pull force: 2–5 kg of pull force to open — strong enough to keep the pocket securely closed during movement, light enough for one-handed operation.
- Alignment: We use magnetic guide channels to ensure magnets self-align within 15 mm of the closure point, creating the satisfying "snap" that signals secure closure.
- Durability: Magnets must withstand 50,000+ open-close cycles without significant field degradation. We test all magnetic closures on automated cycle testers during development.
TSA-Friendly Lay-Flat Design
For business travelers, TSA-friendly design is a significant value proposition. A lay-flat bag opens like a book, allowing the laptop to remain in its compartment while passing through X-ray screening.
- Clamshell opening: The main compartment opens 180° using a U-shaped or three-sided zipper, allowing the bag to lay completely flat.
- Dedicated laptop-only zone: The laptop compartment is isolated from the main packing area. When the bag is opened flat for screening, only the laptop and its immediate accessories are visible — not clothing or personal items.
- Compliant dimensions: The laptop compartment must not exceed TSA's recommended tray dimensions (35 × 30 cm) to ensure smooth screening.
Structural Design
Structural engineering in business bags ensures the bag maintains its shape under load, protects its contents from compression, and presents a clean silhouette whether full or empty.
Base Reinforcements and Self-Standing Construction
A business bag that collapses when set down is functionally deficient. Self-standing construction requires:
- Semi-rigid base panel: A 2–3 mm HDPE (high-density polyethylene) sheet or EVA-molded base panel that provides a rigid floor. This panel also serves as a "false bottom" that elevates contents above the ground.
- Bottom feet: Four molded rubber or metal feet (8–12 mm diameter) positioned at the bag's base corners. Feet provide a 5–8 mm clearance between the bag's bottom panel and the surface, protecting against moisture, dirt, and abrasion. Metal feet add a premium visual element; rubber feet provide better grip on smooth surfaces.
- Reinforced side panels: Internal foam board or corrugated PP inserts in the side panels prevent the bag from bulging or collapsing when partially loaded. These are especially critical for briefcase-style bags where the silhouette must remain rectangular.
Rain Flaps and Water Management
Business bags must protect contents from rain exposure during commutes. Water management design includes:
- Rain flaps: Overlapping fabric flaps that cover zipper lines on the bag's exterior. A rain flap adds 20–30 mm of fabric coverage above and beside any zipper. Water running down the bag's exterior is diverted away from zipper tracks.
- Water-resistant zippers: YKK Aquaguard or equivalent water-resistant zippers with polyurethane-coated tape. These reduce water ingress by 90% compared to standard zippers while maintaining smooth operation.
- Drainage grommets: For bags used in outdoor or wet environments, small drainage grommets (3–4 mm) at the base corners allow trapped water to escape.
Ventilation and Breathability
Back panel ventilation is critical for backpack-style business bags, particularly in warm climates. A poorly ventilated back panel causes sweat buildup, discomfort, and fabric degradation over time.
Back Panel Airflow Channels
The most effective ventilation strategy is channeled airflow — creating defined air pathways between the back panel and the wearer's back:
- 3D mesh padding: A spacer mesh fabric (typically 8–15 mm thick) with a three-dimensional structure that creates air channels between the raised contact points. This reduces skin contact area by 40–60% while maintaining load-bearing support.
- Vertical channel design: Vertical grooves in the back panel foam create chimney-effect airflow — warm air rises and exits through the top of the back panel while cooler air enters from the bottom. We design channels 10–15 mm wide and 3–5 mm deep for optimal airflow without compromising padding effectiveness.
- Suspended back panel: Advanced designs use a tensioned mesh panel stretched across a frame, creating a 15–25 mm air gap between the bag and the wearer's back. This "trampoline back" design reduces back contact heat buildup by up to 25% compared to foam-on-back construction.
Moisture-Wicking Materials
For back panels that contact skin directly, we specify moisture-wicking materials:
- CoolMax® or equivalent: Polyester fiber with a cross-sectional shape that pulls moisture away from skin through capillary action. Dries 50% faster than standard polyester.
- Bamboo charcoal fabric: Natural antimicrobial properties reduce odor buildup. Moisture absorption rate 3× higher than cotton. Common in Asian market-preferred designs.
- Perforated EVA: For back panels with foam padding, laser-perforated EVA allows moisture vapor transmission while maintaining cushioning properties.
Security Features
As business bags carry increasingly valuable electronics and sensitive information, security features transition from "nice to have" to essential differentiators.
RFID Blocking Pockets
RFID (Radio-Frequency Identification) blocking pockets prevent unauthorized scanning of contactless credit cards, passports, and transit passes.
- Construction: A layer of metallic mesh or foil (typically nickel-copper ripstop fabric) laminated between the pocket's outer and inner fabric layers. This creates a Faraday cage that attenuates RF signals at 13.56 MHz (the frequency used by contactless payment systems).
- Effectiveness: Properly constructed RFID-blocking pockets achieve 99%+ signal attenuation (>30 dB reduction). We test every RFID pocket design with a calibrated reader to verify blocking performance before approving for production.
- Design integration: RFID pockets add minimal thickness (0.3–0.5 mm) and weight. We typically integrate them into the front admin panel or a dedicated security pocket adjacent to the body.
Hidden Compartments
Discreet storage compartments provide security through obscurity for high-value items:
- Back panel hidden pocket: A zippered pocket between the back panel padding and the bag's main body. Invisible from the exterior and inaccessible without removing the bag. Ideal for passports, emergency cash, or backup keys.
- False-bottom compartment: A pocket beneath the bag's base panel, accessed via a hidden zipper under the bottom feet. Used for emergency storage of small flat items.
- Disguised entry zippers: Zippers concealed within seam lines or under fabric flaps that appear to be decorative seams. Prevents casual "dip" theft in crowded environments.
Lockable Zippers and Anti-Theft Hardware
- Lockable zipper pulls: Dual zipper pulls that align to accept a small padlock or integrated combination lock. Common on travel-focused business bags.
- Slash-resistant panels: Some premium business bags incorporate wire mesh or UHMWPE (ultra-high-molecular-weight polyethylene) fabric layers that resist cutting from knives or razors. This adds 80–150 g/m² of weight but provides significant anti-theft protection for urban commuters.
- Cable lock loops: Reinforced webbing loops that allow the bag to be secured to a fixed object (desk leg, chair frame, luggage rack) using a small cable lock. Essential for laptop bags used in co-working spaces, libraries, and airports.
Modular and Convertible Design
The modern professional's needs shift throughout the day — from office commute to client meeting to gym to travel. Modular business bags adapt to these transitions without requiring multiple bags.
Detachable Straps and Carry Mode Conversion
The most impactful convertible feature is the ability to switch between carry modes:
- Briefcase to backpack: Handles are supplemented with stowable backpack straps that tuck into a zippered rear panel. When not needed, straps disappear behind a clean panel — no dangling straps. The transition takes 5–10 seconds.
- Shoulder to crossbody: A detachable shoulder strap with adjustable length converts a briefcase from hand-carry to hands-free crossbody carry. Attachment points use low-profile D-rings recessed into the bag's side gussets to avoid protrusion.
- Tote to messenger: Some designs incorporate folding side panels that transform an open-top tote into a flap-closure messenger bag for secure transit.
Expandable Gussets
Expandable gussets add 30–50% more packing capacity when needed, then compress back to a sleek profile:
- Zipper-activated expansion: A circumferential zipper around the bag's perimeter, when opened, expands the gusset depth by 3–5 cm. This is the most common and user-friendly expansion mechanism.
- Bellows gusset: A folded fabric gusset that expands accordion-style. Common in leather and premium bags where a visible zipper would compromise aesthetics.
- Compression straps: External compression straps secure the expanded gusset at the desired depth and compress it back when the bag is less full.
Removable Organizers
Removable internal organizers — often called "tech organizers" or "admin pods" — are Velcro-attached panels or pouches that can be detached for use standalone or repositioned within the bag:
- Standalone use: The organizer can be removed and placed on a desk, providing instant access to pens, cables, chargers, and drives during a meeting — without digging through the bag.
- Interchangeable organizers: Some systems support multiple organizer inserts (e.g., a tech organizer for electronics and a grooming organizer for personal care) that can be swapped based on daily needs.
- Attachment systems: We use hook-and-loop (Velcro) for the most cost-effective removable system, or magnetic attachment for premium products where silent, effortless attachment is desired.
Material Selection: Durability vs. Weight Tradeoffs
Every material choice in a business bag involves balancing durability against weight. The ideal material maximizes the durability-to-weight ratio for the target use case and price point.
The optimal material strategy for most business bag lines is a multi-material approach: high-abrasion zones (base, bottom corners, strap attachment points) use heavier denier fabrics, while low-wear zones (side panels, top lid) use lighter materials. This targeted approach reduces overall bag weight by 10–20% while maintaining durability where it matters most.
Testing Protocols: Validating Design Through Data
Every business bag design must pass rigorous testing before entering production. Our testing protocols simulate real-world use accelerated to compress years of wear into days of testing.
Load Testing
- Static load: The bag is loaded with 15 kg (or 1.5× the rated capacity, whichever is greater) and hung from its carry handles or shoulder straps for 24 hours. After removal, all attachment points, seams, and straps are inspected for deformation, stitch pull-out, or material stretch.
- Dynamic load: The loaded bag is dropped from 60 cm height onto a concrete surface at each face (6 drops total). Post-test inspection checks for broken hardware, seam failure, padding displacement, and structural deformation.
- Cycle load: Shoulder straps are subjected to 5,000 cycles of 10 kg load application and release on a strap fatigue tester. This simulates approximately 3 years of daily strap loading/unloading.
Zipper Cycle Testing
- Standard: All zippers are tested through 5,000+ open-close cycles on automated zipper testers. This exceeds the ISO standard of 1,000 cycles and simulates 3–5 years of daily use.
- Load-bearing zippers: Zippers on main compartments and laptop openings are tested with 5 kg of internal pressure during cycling to simulate the stress of a fully loaded bag.
- Pass criteria: Zero zipper tooth separation, zero slider derailment, and smooth operation throughout all cycles. Any failure requires zipper specification upgrade or reinforcement.
Strap Pull Testing
- Static pull: Straps and handles are subjected to 30 kg of static pull force for 60 seconds. No separation, stitch breakage, or material tearing is acceptable.
- Dynamic pull: 20 kg of force applied in quick-release cycles for 500 repetitions. This tests the attachment points' resistance to fatigue failure.
- Torque test: Handles are twisted 180° under 5 kg load to simulate wringing motions during heavy carry. Attachment points must withstand without deformation.
Drop Testing
- Methodology: The loaded bag (at rated capacity) is dropped from heights of 0.8 m, 1.0 m, and 1.2 m onto a concrete surface. Each height is tested across all six faces (top, bottom, front, back, left, right) for a total of 18 drops per test protocol.
- Assessment criteria: No structural failure (frame breakage, seam separation, hardware detachment). No functional failure (zipper jamming, laptop sleeve damage). Minor cosmetic marks are acceptable.
- Laptop survival test: A laptop simulator (equivalent weight and form factor with accelerometers) is placed inside the laptop compartment. Post-drop accelerometer data is analyzed to verify that peak G-force transmitted to the laptop remains below 50G — the threshold for hard drive damage in mechanical drives and well within safe limits for SSDs.
Brand Engineering Examples: Learning from Industry Leaders
Some brands have elevated business bag functionality into core brand identity. Studying their approaches provides valuable benchmarks for OEM development.
Tumi's Organization System Philosophy
Tumi pioneered the "everything has a place" approach to business bag organization. Their design philosophy centers on:
- Dedicated device pockets: Every device size has a specific, labeled pocket — not generic "pocket" but purpose-built slots for phone, tablet, power bank, and cables. This reduces the cognitive load of "where does this go?" to zero.
- Color-coded interior: A signature lining color (Tumi uses a distinctive orange) makes items visually easy to locate against the interior background. This contrasts with black-on-black interiors that make retrieval difficult in low light.
- Exterior tracking: Tumi integrates a unique product identification number (Tumi Tracer®) that aids recovery if the bag is lost. This concept of built-in traceability is increasingly expected in premium business bags.
Briggs & Riley's Lifetime Warranty Engineering
Briggs & Riley backs their bags with a "forever warranty" — they will repair any defect for the life of the product, regardless of who caused the damage. This warranty is only economically viable because their engineering exceeds expected use conditions by significant margins:
- Over-specified materials: They use 1680D ballistic nylon as standard — 3× the denier of typical business bag fabrics. This creates a material margin that absorbs decades of use without failure.
- Reinforced stress points: Every strap attachment, handle base, and zipper endpoint is backed with bartack reinforcement (42+ stitches in a dense zigzag pattern) and an internal fabric patch. These "hidden reinforcements" are invisible from the exterior but multiply the stress capacity of each attachment point.
- Replaceable components: Wheels, handles, and zipper pulls are designed as replaceable parts. When a component wears, it can be replaced without discarding the entire bag — extending product life and reducing warranty costs.
For brands developing their own business bag lines through our OEM program, we recommend studying these engineering philosophies and adapting the relevant principles to your target price point and positioning. Our engineering team can benchmark your design against industry leaders during the development process.
OEM Design Development Process
Translating a business bag concept into a production-ready product requires a systematic development process. Here is the 8-stage workflow we follow at our custom design facility.
Stage 1: Design Brief & Market Analysis
Every project begins with a detailed design brief covering target market segment, price positioning (retail MSRP), feature priorities, competitive benchmarks, and volume forecasts. We review comparable products on the market to identify feature gaps and differentiation opportunities.
Stage 2: Concept Sketching & Design Direction
Our design team produces 2–4 concept directions as technical illustrations — showing exterior styling, organization layout, and material concepts. These are presented to the client for feedback and direction selection.
Stage 3: Material Sourcing & Selection
Based on the approved design direction, we source fabrics, hardware, padding, and accessories that meet the design intent and cost targets. Material options are presented as physical swatches alongside cost and performance data. Our quality control team tests all candidate materials for colorfastness, tensile strength, and abrasion resistance.
Stage 4: Technical Drawing & CAD Specification
Every component is specified in detailed CAD drawings including dimensions to 1 mm tolerance, seam allowances, stitch types and densities, hardware placement coordinates, and assembly sequence. This technical package serves as the production blueprint.
Stage 5: First Prototype & Fit Testing
The first physical prototype is built to validate proportions, ergonomics, and feature functionality. Fit testing uses actual devices (laptops, tablets, phones) to verify compartment dimensions. Ergonomic assessment includes weighted wear testing by multiple testers across different body types.
Stage 6: Design Refinement
Client feedback and test results drive 1–3 revision rounds. Each revision produces a new prototype with incremental improvements. Common refinements at this stage include adjusting strap length ranges, repositioning pockets based on user testing, upgrading hardware, and optimizing weight distribution.
Stage 7: Pre-Production Sample
The final sample is produced using production-intent materials, processes, and tooling. This sample serves as the quality benchmark for bulk production and is signed by both parties as the production standard.
Stage 8: Bulk Production & Quality Inspection
Bulk production follows with in-line inspections (checking first 10% of production) and final random inspection (AQL 2.5 standard). Our quality control team documents every inspection with photographs and measurements, providing clients with complete quality records before shipment.
For brands requiring rapid market entry, our small batch production program supports initial orders of 200 units per style — enabling market testing before scaling to full production volumes through our wholesale program.
Carry Modes: Designing for How People Actually Move
Most business bags are designed for a single carry mode and then used in three. A briefcase gets carried by its handle at a client meeting, slung over the shoulder through a station, and hooked onto a trolley handle in an airport — often within the same day. Each mode loads the shell differently, and the attachment points that work for one are frequently the first to fail under another.
| Carry mode | Load path | Design requirement |
|---|---|---|
| Top handle | Weight hangs directly from the handle attachment | Reinforcement must run into the shell panel, not just the lining |
| Shoulder strap | Load crosses the shell diagonally | Anchor at the structural edges, not mid-panel |
| Backpack | Weight sits against the back and pulls downward | Strap anchors need vertical reinforcement and even spacing |
| Crossbody | Single-point diagonal load with rotation | A swivel at the anchor prevents strap twisting |
| Trolley sleeve | Bag is supported by a separate frame | The sleeve seam carries shear, so it needs a bar-tack at each end |
Where two modes are both essential, the honest answer is usually two sets of attachment points rather than one compromise. A detachable backpack harness that clips into reinforced D-rings, paired with a conventional top handle, covers almost every situation without asking a single anchor to do two contradictory jobs.
Handle drop is the measurement most often left to chance. If the handle is too short the bag catches the thigh when walking; too long and it drags. Specifying drop from the top of the handle to the shoulder line, and testing with the wearer in a jacket, removes a complaint that is very hard to fix once tooling is cut.
Finish, Colour and the Professional Context
A business bag is carried into rooms where it is read as part of the wearer's presentation, which makes finish decisions commercial rather than cosmetic. Hardware colour has to agree across zip, feet, buckles and logo plate, because a mismatch is visible at arm's length. Equally, the leather finish determines how the bag looks after a year — and a bag that looks tired at twelve months reflects on the brand that sold it.
- Fix one hardware finish across every metal component, including the zip tape and pull
- Choose edge paint in a matching or deliberately contrasting tone, and specify the number of coats
- Test corner abrasion, since corners and handle roots show wear before any other area
- Decide deliberately between a leather that patinates and one that stays uniform
- Confirm the lining colour does not read through lighter leather shades
- Check the bag under the lighting it will be used in, not only under studio light
Dark colours are forgiving on wear and demanding on consistency; light colours are the reverse. Where a range includes both, the shade tolerance that works for black will not be adequate for a stone or taupe, and the specification should say so. Stating a single tolerance for an entire range is a common source of rejected shipments.
Serviceability: Designing for a Five-Year Working Life
A business bag is used far harder than almost any other leather product — carried daily, set down on floors, overloaded on the last day of a trip. The brands that earn repeat business are usually the ones whose bags can be repaired rather than replaced. Serviceability is decided at the design stage, and it costs very little to specify.
- Use standard, replaceable hardware sizes rather than bespoke fittings with no second source
- Fit shoulder straps with buckles or clips rather than stitching them permanently into the shell
- Keep the lining accessible so a pocket or zip can be replaced without dismantling the bag
- Reinforce handle roots, corners and base edges, since these are the predictable failure points
- Record the component list with the technical pack so replacements can be ordered years later
- Specify finish standards that can be matched again if a panel is replaced
| Component | Common failure | Design response |
|---|---|---|
| Handle roots | Stitch pull-out under repeated load | Extend reinforcement into the panel and bar-tack the ends |
| Shoulder strap | Permanently stitched, cannot be replaced | Fit a clip or buckle at both ends |
| Base corners | Abrasion through the finish | Add a reinforced panel or metal feet |
| Zip | Slider wear and tape separation | Specify a branded zip and cycle-test at sampling |
| Lining pockets | Tear at the seam under load | Bind the seam and reinforce the stress points |
The final piece is documentation. A bag whose components are recorded — hardware finish code, thread specification, leather reference — can be repaired in year five. One whose specification exists only in a sample-room folder cannot, and the customer experiences that as a brand that does not stand behind its product.
We specify to that standard on our Quanzhou production floor, where inspection runs to AQL 2.5 under ISO 2859-1 single sampling at general level II. It is a modest discipline that shows up in the warranty claims rather than in the specification sheet.
Partner with Bespoke Bags for Your Next Business Bag
Designing a great business bag requires the convergence of ergonomic science, material engineering, organizational psychology, and manufacturing expertise. At Bespoke Bags, we bring over 20 years of experience across all four disciplines to every project.
Whether you are an established brand developing your next generation of business bags, an entrepreneur launching your first product line, or a corporate buyer seeking customized employee bags, our team provides end-to-end support — from initial concept to delivered product.
- SGS-verified 4,950 m² production floor with dedicated prototyping and testing facilities
- MOQ of 500 pieces per style — accessible for emerging brands
- In-house design engineering team with expertise in ergonomics and organizational systems
- Comprehensive testing protocols ensuring every design exceeds real-world demands
- Full supply chain management from material sourcing through global logistics
Frequently Asked Questions
What laptop screen sizes can be accommodated in custom business bags?
Our custom business bags can accommodate laptops from 10 inches to 17.3 inches, with dedicated sleeve compartments engineered for specific device dimensions. Each laptop sleeve is designed with 10–15 mm padding on all sides using closed-cell EVA foam or memory foam, plus corner protection bumpers made from TPU or silicone. We design suspended laptop sleeves that keep the device elevated above the bag's base, providing drop protection equivalent to a 1-meter free-fall onto concrete. For brands targeting specific laptop models (e.g., MacBook Pro 14" or ThinkPad T16), we engineer sleeves to those exact dimensions ±2 mm tolerance.
What testing protocols do your business bags undergo?
All business bags produced in our facility undergo a comprehensive testing regimen before bulk production approval. Load testing: bags are loaded with 15 kg of weight and carried, shaken, and dropped from 60 cm height to test seam integrity and strap attachment points. Zipper cycle testing: all zippers are tested through 5,000+ open-close cycles on automated testing machines to simulate 3+ years of daily use. Strap pull testing: shoulder straps and handles are subjected to 30 kg+ static pull force and 20 kg dynamic pull for 500 cycles. Drop testing: loaded bags are dropped from heights of 0.8–1.2 meters onto concrete surfaces at multiple angles to assess corner protection and structural integrity. These tests are documented and available for client review.
What is the OEM design development process for a new business bag?
Our OEM development process follows a structured 8-stage workflow: (1) Design Brief — understanding target market, price point, feature priorities, and brand positioning; (2) Concept Sketching — 2–4 design directions rendered as technical illustrations; (3) Material Selection — sourcing fabrics, hardware, and components aligned to design intent and cost targets; (4) Technical Drawing — full CAD specification with all dimensions, seam allowances, and construction details; (5) First Prototype — physical sample built to test proportions, ergonomics, and feature functionality; (6) Design Refinement — client feedback incorporation with revised prototypes as needed (typically 1–3 revision rounds); (7) Pre-Production Sample — final sample made with production-intent materials and processes; (8) Bulk Production — manufacturing with in-line and final quality inspections. Total timeline from brief to production-ready: 6–10 weeks.
What is the minimum order quantity for custom business bags?
Our MOQ is 500 pieces per style per color. This applies to our full range of bag types including briefcases, messenger bags, backpacks, and tote-style business bags. For orders of 200–500 units, we recommend simpler constructions with fewer unique components to maintain efficient production. Orders of 500+ units allow for more complex organization systems and custom hardware. Our SGS-verified 4,950 m² production floor in Quanzhou supports production scaling up to 10,000+ units per style per month for established programs.
Can business bags be designed with modular or convertible features?
Yes. Modular and convertible design is one of our core engineering capabilities. We design business bags with features such as detachable shoulder straps (via D-ring and clip attachments), expandable gussets (zipper-activated expansion adding 3–5 cm of depth), removable internal organizers (Velcro-attached divider systems), convertible carry modes (briefcase handles with hideaway backpack straps), and modular accessory attachment (MOLLE-compatible panels, magnetic accessory pods). Each modular component is engineered for durability through thousands of attachment/detachment cycles. We work with brands to balance modularity complexity against cost and weight targets.
How much clearance should a laptop compartment allow?
Allow roughly three to five millimetres beyond the device on each dimension, plus padding compression. A sleeve cut exactly to the device will be difficult to insert and will not accommodate a protective case. Test with the largest device the bag is specified for, not the average one.
How wide should a shoulder strap pad be on a business bag?
Fifty to seventy-five millimetres spreads load comfortably for a typical daily carry. Narrower pads concentrate pressure on the trapezius and become uncomfortable once the bag is loaded. Width matters more than padding thickness for perceived comfort under sustained load.
Which parts of a business bag wear out first?
Handle roots, base corners and the zip are the consistent first failures. All three are predictable and all three are addressed at the pattern stage by extending reinforcement into the shell panel, protecting the corners, and specifying a cycle-tested zip.
Can one bag be designed for both shoulder and backpack carry?
Yes, provided you do not ask a single anchor to serve both. Use a conventional top handle plus reinforced D-rings that accept a detachable harness. The load paths differ enough that sharing one attachment point is where convertible designs usually fail.
How is charger and cable organisation best handled?
Dedicated elastic loops with a fixed grid work better than open pockets, because cables stay separated and visible. Keep the charger loops away from the laptop sleeve seam so a rigid plug does not press against the device.
Which hardware finish lasts longest under daily use?
Brushed or antiqued finishes conceal the contact marks that a high-polish surface shows within weeks. Plating thickness at the rub points matters more than the base metal. Whatever the finish, specify the same one across every component so wear appears uniform.
Can a shoulder strap be replaced rather than the whole bag?
Only if it was designed that way. Straps stitched permanently into the shell cannot be swapped without dismantling the bag. Specifying a clip or buckle at each end costs almost nothing at build time and makes the difference between a repair and a replacement.
How do you keep a structured business bag from slumping when empty?
A base board and a structured back panel carry most of the work; the leather alone will relax. Reinforce the base, add a light internal frame at the back, and test the empty bag standing on a hard surface for an hour before approving the pattern.