
Leather bag production capacity of 200,000 units a month describes the maximum number of finished bags a facility can complete in thirty days when every line runs at its planned rate, materials are available and the order mix is stable. It is a ceiling on throughput, not a schedule and not a promise. For a brand, the useful question is never simply whether a partner can reach that number, but how quickly and predictably it can absorb a specific order volume without pushing lead times out.
What a Monthly Capacity Figure Actually Measures
Capacity is the product of several things running at once: the number of lines, the number of machines, the number of trained operators, the hours available and, critically, the complexity of the bags being made. A facility that can complete 200,000 simple pouches in a month will not complete 200,000 structured handbags in the same window, because each style consumes a different amount of labour and machine time. Capacity is therefore always stated against a reference mix.
- Line count: more lines allow parallel styles, but only if each has trained operators and the pattern and cutting capacity to feed it.
- Machine hours: stitching machines, cutting presses, skiving and edge-finishing equipment all set upper limits on how much work can pass in a day.
- Labour: capacity is capped by the number of skilled hands, not by the number of machines parked on the floor.
- Style complexity: a multi-panel tote with internal organisation consumes far more minutes than a single-seam pouch.
- Material availability: no line can run faster than the leather, lining and hardware delivered to it.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Why Capacity Is a Ceiling, Not a Delivery Date
A common mistake is to divide a monthly capacity figure into a desired order quantity and assume the result is the time required. That arithmetic ignores sampling, material lead time, line loading and finishing. A facility may hold a nominal ceiling of 200,000 units a month while already running at a large fraction of it for other clients; your order enters a schedule rather than an empty room.
| Factor | What it controls | Effect on your order |
|---|---|---|
| Nominal capacity | Maximum monthly output at a reference mix | Sets the theoretical ceiling, not the start date |
| Current loading | Capacity already committed to other programmes | Determines how much headroom remains for a new order |
| Sampling time | 6–10 working days, or 12–15 for complex construction | Must complete and be approved before bulk begins |
| Material lead time | Time to receive leather, lining and hardware | Can exceed stitching time if the hide is not in stock |
| Bulk window | 35–50 days after sample approval | The realistic production span for a committed order |

How Lines, Machines and Staff Combine
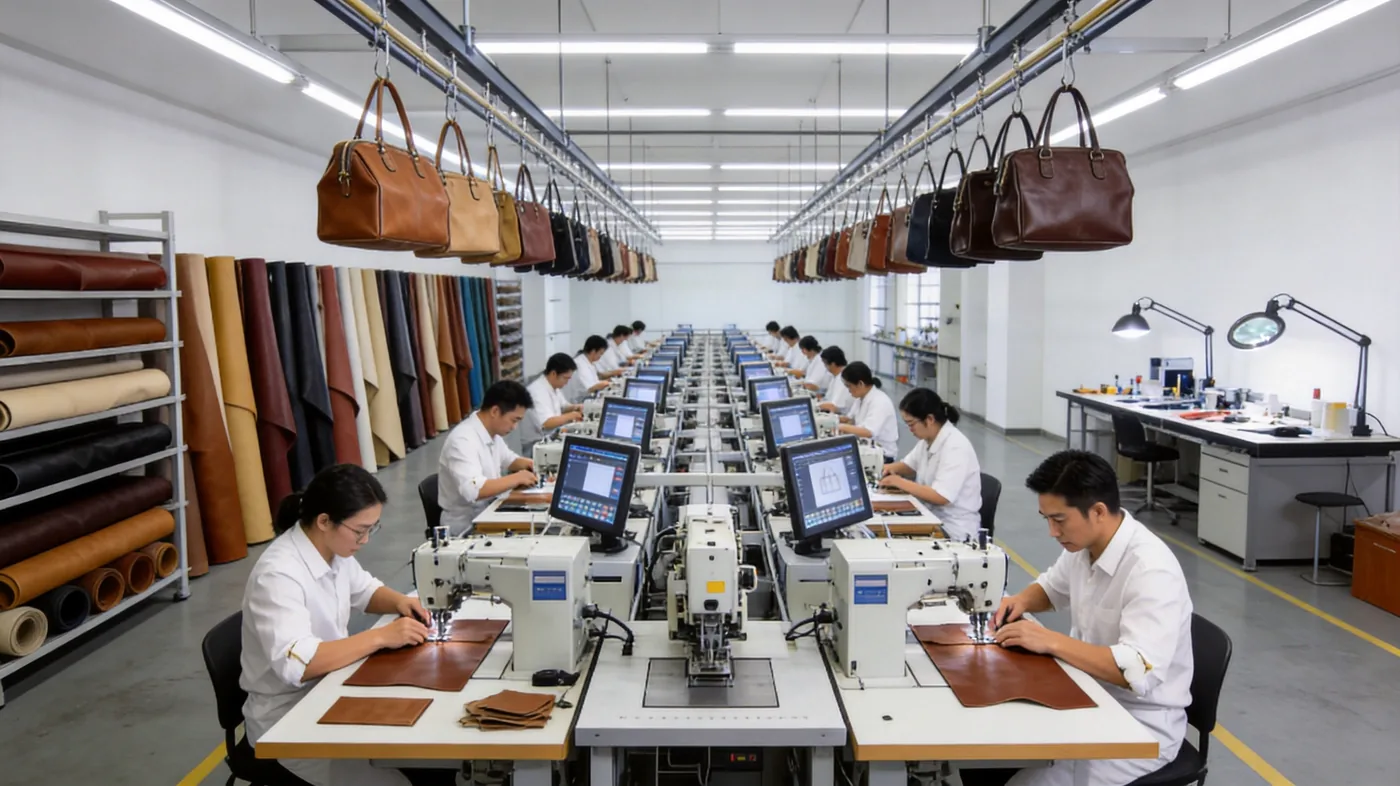
Capacity only becomes real when the inputs balance. Our SGS-verified production floor in Quanzhou runs to 4,950 m² with 137 staff, seven lines and 149 machines, and the monthly figure of 200,000 pieces describes what that combination can achieve when it is fully loaded on a representative mix. Understanding how those numbers relate is more useful than memorising the headline.
| Asset | Figure | What it enables |
|---|---|---|
| Production floor | 4,950 m² (SGS-verified) | Space for parallel lines, cutting, finishing and packing without congestion |
| Staff | 137 | Trained operators across cutting, stitching, finishing and inspection |
| Lines | 7 | Ability to run several styles concurrently rather than one at a time |
| Machines | 149 | Stitching, skiving, cutting and finishing capacity to feed each line |
| Monthly output | 200,000 pieces | Theoretical ceiling on completed units at a reference mix |
The important point is that none of these assets works in isolation. A seventh line with no pattern cutter to feed it adds no output, and a cutting press with no operator is a stationary object. Real capacity is the slowest link in the chain, evaluated across all of them. When a programme team schedules a new order, it is not asking whether the floor can physically make the bags, because it almost always can; it is asking which line, which operators and which machines can absorb the work alongside whatever else is running. That is why a capacity conversation is really a scheduling conversation, and why a facility that manages its calendar well will quote a more dependable date than one with a larger nominal figure and a crowded book.
Reading Capacity Against Your Own Order
For a buyer, the practical exercise is to compare a proposed order against the facility's loading and the style's labour content, then decide how much of the ceiling the order will occupy. The math matters less than the discipline of asking the question before committing to a launch date.
A worked example makes the logic concrete. Suppose a brand needs 10,000 units in a single style and a partner states 200,000 units a month at a reference mix of a relatively simple construction. The same floor might reasonably complete a more complex structured handbag at a substantially lower daily rate, so the same 10,000 units occupy a larger slice of the month than the headline figure implies. The brand that plans against the simple-mix number builds an optimistic calendar; the brand that plans against its own style builds a calendar it can keep. The discipline is to convert the headline figure into style-specific throughput before any date is fixed, then to add a margin for the sampling, material and inspection stages that sit outside the line itself.
The Real Constraints Sit Before the Line
At scale, stitching is rarely the bottleneck. The constraints that set genuine capacity are usually upstream and downstream of the line itself: the availability of the right leather, the number of skilled operators, and the finishing and inspection stages that every unit must pass. A facility can only complete as many bags as it can cut, finish and inspect, whatever the stitching lines are capable of.
- Leather supply: hides must be sourced, checked and colour-matched before cutting, and premium leathers carry their own lead times.
- Cutting and skiving: each style consumes a set amount of press and knife time that must be scheduled alongside others.
- Skilled labour: edge finishing, hardware setting and fitting require trained hands that cannot be added overnight.
- Inspection: AQL 2.5 single sampling under ISO 2859-1 consumes time at the end of the run and cannot be skipped to save days.
- Packing: cartoning and labelling are the final gate, and a narrow packing area will throttle output regardless of line speed.
What a Capacity Claim Can Hide
A large number on a slide is easy to state and harder to verify. Capacity claims become meaningful when they are tied to a reference mix, to a floorspace that has been independently verified, and to a transparent account of current loading. Without those, a headline figure tells you very little about reliability.
| Claim | What to verify | Why it matters |
|---|---|---|
| Monthly output | The reference mix the figure assumes | A simple mix inflates the number against a complex one |
| Floorspace | Independent verification such as an SGS audit | Confirms the physical space exists as described |
| Line count | Whether lines are dedicated or shared across clients | Shared lines reduce headroom for a new order |
| Staffing | Trained operators versus headcount on paper | An untrained operator adds no usable capacity |
| Lead time | The stated bulk window after sample approval | The figure that actually governs your launch date |
Verification does not require a formal audit for every order, but it does require asking the right questions and listening for specific answers. A partner who can describe the reference mix, name the floorspace and explain current loading is doing something a bare number cannot: demonstrating that the capacity figure is drawn from a real schedule rather than a marketing document. For larger programmes, an independent audit such as the SGS verification behind our own 4,950 m² floor removes most of the remaining doubt, because it confirms the physical assets exist as described rather than as intended.
Planning a Programme Against Stated Capacity
The most reliable way to use a capacity figure is to plan backwards from the launch date and confirm each stage fits. Sampling, material sourcing, bulk production, inspection and freight each take time, and only by laying them end to end does it become clear whether a given order volume is comfortable, tight or unrealistic.
- Fix the launch date and work backwards to the shipment date you need.
- Allow the 35–50 day bulk window, measured from approved sample rather than from the deposit.
- Add sampling at 6–10 working days, or 12–15 where the construction is complex.
- Confirm leather and hardware are available for the order quantity, not just for a sample.
- Reserve line capacity in advance, so the order enters a schedule rather than a queue.
Read alongside the wider leather bag manufacturing process, this planning discipline turns a headline capacity number into a workable production calendar rather than a hopeful estimate.

How Capacity Interacts With the Sample-to-Bulk Timeline
Capacity only begins to matter once a sample has been approved. Before that point, an order is a specification rather than a scheduled run, and no amount of monthly ceiling shortens the sampling stage. This is why an experienced buyer treats the two phases separately and does not let a large capacity figure create a false sense of speed.
| Phase | Typical duration | What capacity means here |
|---|---|---|
| Sampling | 6–10 working days (12–15 for complex builds) | Low relevance; sampling uses a sample room, not the main lines |
| Material sourcing | Varies by leather and hardware | Determines when bulk can actually begin |
| Bulk production | 35–50 days after approval | The phase where line capacity governs how fast units complete |
| Inspection | Scheduled within the bulk window | AQL 2.5 sampling confirms the lot before it ships |
| Packing and freight | After inspection | Packing throughput can throttle output if the area is narrow |
A capacity figure is therefore best read as the size of the pipe, while lead time describes how long the water takes to travel through it. Both matter, and neither substitutes for the other. Buyers who understand this distinction plan launches that hold, and they rarely find themselves explaining a missed date to a retail partner.
Plan capacity against your launch, not against a headline
Share your target quantity, style complexity and launch date. The programme team will map the order against real loading and return a phased timeline covering sampling, bulk and shipment, so the capacity figure becomes a plan you can hold.
Frequently Asked Questions
What does 200,000 units a month actually mean for a leather bag order?
It describes the maximum number of finished bags a facility can complete in thirty days when fully loaded on a representative style mix, with materials available and every line running at its planned rate. It is a ceiling on throughput rather than a schedule for your order. Your order enters that schedule alongside existing commitments, so the figure tells you the size of the pipe rather than how quickly your particular bags will move through it.
Why is a capacity figure not the same as a delivery date?
Because production has to pass through sampling, material sourcing, bulk manufacture, inspection and packing before anything ships. A monthly ceiling describes the maximum rate at which finished goods can leave, but it says nothing about how much capacity is already committed to other clients or how long the hides take to arrive. Lead time for a real order is governed by those stages, which is why the bulk window of 35–50 days after sample approval matters more than the headline number.
How long does bulk production take once capacity is reserved?
For a committed leather bag order the bulk window is typically 35–50 days after the sample has been approved. That span covers cutting, assembly, finishing, inspection and packing, and it starts from approval rather than from the deposit. Reserving line capacity in advance means the order is scheduled rather than queued, but it does not compress the working time the bags themselves require.
Can a factory with high capacity produce my order faster?
Not necessarily. Capacity sets an upper limit on how many units can be completed per month, but speed for a specific order depends on sampling time, material availability and current loading. A facility running close to its ceiling may have little headroom for a new programme, while one with spare capacity can slot an order in sooner. The relevant question is always how much of the ceiling is free and when.
What is a reference mix in capacity calculations?
A reference mix is the representative blend of bag styles that a facility uses when calculating its monthly figure. Because a structured handbag consumes far more labour and machine time than a simple pouch, capacity stated against an easy mix will be higher than capacity against a complex one. Asking a partner to name the mix behind its figure is one of the quickest ways to test how much weight that number can carry.
How many lines does a modern leather bag facility run?
Our SGS-verified production floor in Quanzhou runs seven lines across 4,950 m², supported by 137 staff and 149 machines, with a monthly output of 200,000 pieces at a representative mix. Line count matters because several styles can run in parallel rather than one at a time, but a line only produces as much as its operators, patterns and cutting capacity allow it to produce.
Does a large MOQ always follow from high capacity?
No. High capacity describes what a facility can do when fully loaded, not the minimum order it will accept. Our standard MOQ is 500 pieces per style and colourway, and small-batch pilots are available for brands testing a new line. Capacity and minimum order are separate settings: one describes throughput, the other describes the smallest run a programme will schedule economically.
What limits production capacity besides machines?
The most common constraints sit before and after stitching. Leather must be sourced and matched, cutting and skiving consume scheduled time, edge finishing and hardware setting need skilled hands, and every lot must pass inspection. A facility can only complete as many bags as it can cut, finish and inspect, so machines alone never tell the whole story of how much output a floor can achieve.
How should a brand use a capacity figure when planning a launch?
Work backwards from the launch date and confirm each stage fits. Allow sampling at 6–10 working days, the 35–50 day bulk window measured from approval, plus freight. Then check that the leather and hardware are available for the full order quantity and that line capacity has been reserved. Used this way, a capacity figure becomes a planning input rather than a marketing claim.
What should I verify when a supplier claims a monthly capacity figure?
Ask for the reference mix the figure assumes, independent verification of the floorspace such as an SGS audit, the current loading of the lines, and the realistic bulk window after sample approval. A facility that publishes these details gives you something to plan against, while a bare headline number tells you very little about how much of that capacity is actually available to your order.
Does capacity change with the complexity of the bag?
Substantially. A multi-panel tote with internal organisation, a lining and detailed edge finishing consumes far more labour and machine minutes than a simple pouch, so the number of units a floor can complete in a month falls as complexity rises. This is why any credible capacity figure is stated against a named reference mix rather than presented as a single unconditional number.
How does inspection fit inside the bulk window?
Inspection is scheduled within the 35–50 day bulk window rather than added on afterwards. Under our standard plan, AQL 2.5 single sampling under ISO 2859-1 is applied at the end of the run, positioned so that any rework can be completed without delaying shipment. Because the plan is fixed in advance, neither side can move the goalposts after the lot is finished.
Can capacity be reserved before sampling is approved?
It can be pencilled in, but bulk work only begins once the sample is approved. Reserving provisional capacity protects your preferred production slot, yet no line starts cutting until the approved sample and the gold-sealed reference are confirmed. Treating sampling and bulk as separate phases, with their own timelines, is the most reliable way to plan a launch that holds.
What is the difference between capacity and capability?
Capacity is how much a facility can produce in a given period, usually stated monthly. Capability is what it can produce at all: the materials, constructions and finishes within its experience. A floor may have ample capacity for simple totes but limited capability for a framed structured handbag. Buyers should assess both, because a large capacity figure is useless if the style sits outside what the floor can actually make well.
How does order splitting affect the use of production capacity?
Splitting an order into a small pilot batch followed by a larger run uses capacity more gently and reduces risk. The pilot confirms construction and market fit before the brand commits to a full run, and because capacity is released and rebooked between the two, the schedule can absorb the second phase without competing with the first. Brands testing a new style often find that this staged approach is safer than loading the entire quantity into a single production slot.
Can a facility run my order alongside other clients' work?
Yes, and most do. With seven lines, a floor can run several styles concurrently, which is how a programme schedules new business without displacing existing clients. The practical consequence for a buyer is that capacity is shared, so availability depends on how the lines are already loaded at the moment the order is confirmed. Asking about current loading, rather than only about the monthly ceiling, gives a far more accurate picture of when production will actually begin.
What happens to capacity during peak seasons?
Peak demand tightens every facility's schedule, because more clients want the same lines at the same time. Capacity itself does not shrink, but the free headroom does, and lead times can drift towards the upper end of the 35–50 day bulk window if materials also become slower to source. Brands with fixed launch dates are wise to reserve capacity early and confirm orders well ahead of the season rather than relying on spare lines being available at short notice.