
Sustainable bag manufacturing rests on measuring and reducing three inputs and outputs: water, solid waste and energy, with the biggest single lever being material yield rather than machine efficiency. Industry estimates put leather cutting utilisation at roughly 75 to 85 per cent on well-engineered patterns, which means that for every four square metres of hide purchased, close to one square metre never reaches a finished bag. Water consumption is concentrated upstream at the tannery rather than on the cutting and stitching floor, while electricity is spread across lighting, motors, ventilation and air conditioning. The honest position is that a production partner controls only part of the footprint: finish quality, pattern efficiency, waste separation and energy discipline are within reach, while tannery chemistry and raw-material agriculture sit upstream and require supplier pressure rather than internal fixes. This guide sets out where the burdens actually occur, what a programme can verify, and which interventions pay back.
Where the burden actually sits in a bag's life cycle
Buyers often assume the stitching floor dominates a leather bag's environmental footprint. It does not. Tanning is water-and chemistry-intensive, hide production carries agricultural burdens, and long-haul freight adds a further leg. The cutting-and-assembly stage is comparatively light, but it is the stage a brand can most directly influence, which is why improvement programmes should start there and extend upstream through material specifications.
| Life-cycle stage | Dominant burden | Rough order of significance | Who controls it |
|---|---|---|---|
| Raw hide production | Agricultural emissions, land and water use | Usually the largest single block | Upstream supply chain; influenced by hide selection and origin |
| Tanning and finishing | Water volume, effluent load, chemistry, energy for drying | The largest process-stage burden | Tannery; verifiable through LWG audit scope and effluent reporting |
| Cutting and components | Solid waste from offcuts, hardware manufacture | Moderate; the most addressable in-house burden | Production partner; pattern efficiency and yield management |
| Assembly and finishing | Electricity for machines, lighting, ventilation, edge-paint chemistry | Moderate and highly variable by facility | Production partner; equipment and scheduling choices |
| Packaging | Corrugate, film, textiles, void fill | Small in weight, large in perceived waste | Production partner and brand jointly |
| Distribution | Freight emissions, mode-dependent | Significant, and governed by shipping mode not craft | Brand and logistics route |
The practical conclusion is that a brand wanting to reduce the footprint of a bag programme should work on three fronts at once: choose leather from a tannery with current LWG scope, engineer patterns and nesting for maximum yield, and manage energy and waste on the finishing floor. Software-driven nesting has improved cutting efficiency considerably in recent years, but it cannot rescue a pattern that was drawn without yield in mind.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Water: mostly upstream, but not entirely out of reach
Water use in leather is a tannery story. Beamhouse operations, soaking, liming, deliming, tanning, dyeing and finishing all draw water, and the effluent carries dissolved organics, salts and, in chrome tanning, chromium species. That is precisely why independent tannery assessment bodies exist, and why a brand's most effective water intervention is specifying leather from a tannery with a current audit and asking for the water-related scope items rather than assuming them.
- Ask for the tannery's current audit status and the specific scope items covering effluent treatment and water management; an expired certificate supports nothing.
- Request effluent parameters and treatment description for the article you actually buy, not for the tannery's best-performing line.
- Prefer tanneries operating closed-loop or recycling systems where the claim is documented rather than asserted.
- Reduce the number of tanneries in a programme: fewer suppliers mean deeper oversight and more influence over process.
- Avoid over-specifying finish: every additional coating operation in dyeing and finishing adds process water and chemistry for a marginal aesthetic gain.
- Frame leather as a by-product of food production in consumer copy; the hide's agricultural footprint is shared with the meat industry and must not be double-counted.
On the cutting and sewing floor itself, water consumption is domestic and modest, but two process points matter: edge painting and any wet finishing step. Both consume small volumes, and both can be managed through controlled dispensing, covered containers and worker training. These are hygiene and cost items before they are environmental ones, which is why they are usually already under control at a well-run facility and easy to verify on a walkthrough.
Waste: yield is the biggest lever a programme controls
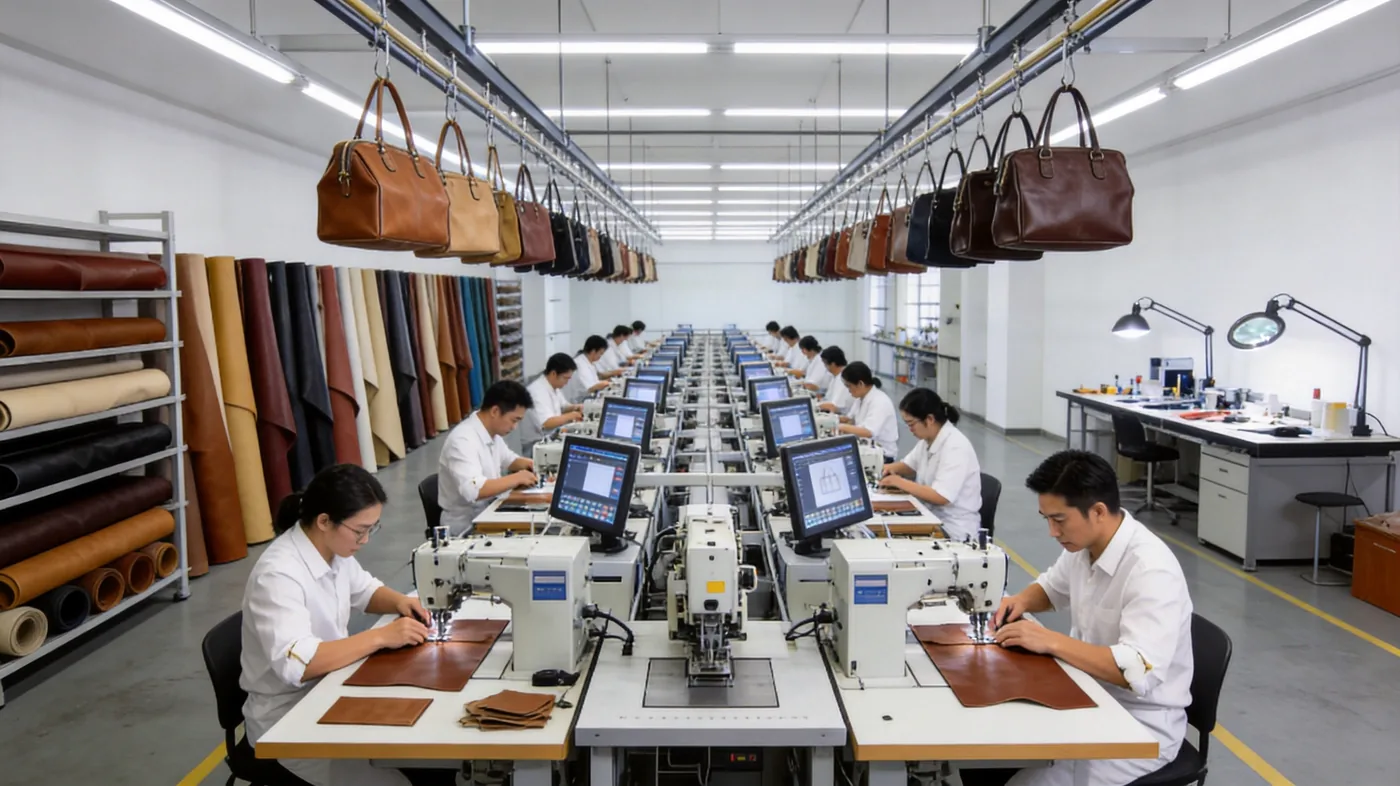
Solid waste is where a production partner's influence is largest. Leather arrives in irregular hide shapes with natural defects, so pattern placement determines how much material is consumed and how much leaves the table as offcuts. Good nesting, defect-aware marking and disciplined panel sizing routinely improve utilisation by several percentage points, which reduces material purchase, cost and waste simultaneously.
| Waste stream | Typical source | Reduction lever | Recovery route |
|---|---|---|---|
| Leather offcuts | Pattern nesting and irregular hide geometry | Defect-aware marking, revised nesting, panel consolidation | Fibre recovery for bonded applications; small-goods production |
| Fabric and lining scrap | Panel cutting from roll goods | Nesting efficiency, standardising lining panels across styles | Textile recycling where mono-material |
| Cardboard and paper | Packaging inbound, cartons, tags | Right-sized cartons, reusable inbound totes | Standard paper recycling; well-established and simple |
| Metal and hardware waste | Rejected components, scrap fixings | Supplier quality management to reduce rejects | Scrap metal recovery, particularly brass and steel |
| Chemical and solvent waste | Edge paint, adhesives, cleaning agents | Controlled dispensing, batch sizing, sealed storage | Licensed chemical waste handling, never general refuse |
| Process water and sludge | Edge painting, cleaning, domestic use | Dispensing discipline, spill prevention | Wastewater treatment or licensed disposal |
| Rejected finished goods | Quality failures, transit damage | Tighter in-line QC to reduce rework | Dismantle for recoverable components where feasible |
The most under-used lever is panel consolidation: redesigning a pattern so the same lining panel serves three styles removes an entire cutting operation, its scrap and its quality risk. Brands briefing a range rather than a single style can ask for this analysis at the development stage, when it is free, rather than at a cost-review meeting, when it is not.
Energy: small machines, large aggregate
A bag facility is not an energy-intensive installation in the way a tannery or a foundry is, but aggregated over 149 machines, seven lines and a large air-conditioned floor, electricity becomes the dominant controllable cost and emissions source on site. The consumption profile is unglamorous: lighting, ventilation and cooling, stitching motors, cutting presses, compressors and drying or heat-setting where applied.
| Energy consumer | Typical pattern | Improvement action | Verification method |
|---|---|---|---|
| Lighting | Continuous across shifts, often older fixtures | LED conversion with zoned switching | Fixture count and metered load before and after |
| Air conditioning and ventilation | Largest single load in warm humid months | Insulation, zoning, filtered recirculation, set-point discipline | Metered consumption against degree days |
| Stitching and skiving motors | Many small motors, moderate duty cycle | Servo motors, maintenance to reduce drag | Machine-level metering or rated-load estimation |
| Cutting presses | High peak load, intermittent use | Efficient press scheduling, idle shutdown | Shift-level consumption records |
| Compressed air | Leakage is a common hidden waste | Leak survey and repair, pressure optimisation | Leak-down test; compressor load hours |
| Heat setting and drying | Concentrated, controllable | Insulated cabinets, batch scheduling, temperature control | Chamber temperature and cycle logs |
The pattern that matters is measurement. A facility that reads its meters, records consumption per production day and reviews anomalies will outperform one that buys efficient equipment and never checks it. When we review a programme partner's environmental management with a brand, the questions we encourage are about records rather than equipment: what is metered, how often it is read, and who acts on a spike.

Systems, audits and what verification really covers
Certification is a means, not an outcome, and buyers who understand the distinction negotiate better. An environmental management system such as ISO 14001 evidences that a facility identifies its impacts, sets objectives, tracks them and reviews performance; it does not state that any particular bag was made with less energy. Independent social and environmental audit programmes cover labour and management practice. Tannery audits address the leather supply chain specifically. Each covers a defined scope and different time period.
None of these replaces measurement. A brand serious about manufacturing impact should ask a partner for three things: a facility-level energy and waste baseline, the improvement actions taken in the last year with their results, and the internal owner of that data. Answers that name a person and a date are worth more than a framed certificate on a wall.
How a programme sets and holds improvement targets
Targets work when they are attached to a number a partner already collects. Below are the metrics we see brands adopt successfully, because each maps to an existing production record rather than requiring a new measurement discipline.
- Material yield per style, tracked as square metres of leather per finished bag, reviewed at pattern sign-off and after the first bulk run.
- Cutting waste percentage, with an accessory or small-goods plan for the recovered offcut.
- Rejected-component rate by supplier, which reduces both waste and rework on the floor.
- Electricity per production day where sub-metering exists, or per shift where it does not.
- Waste separation compliance: the proportion of floor waste sorted into leather, textile, paper, metal and chemical streams.
- Packaging weight per unit shipped, which links the manufacturing question to the unboxing experience.
Reporting cadence matters more than target ambition. A quarterly review of six simple metrics, discussed with the brand and actioned by the programme team, will outperform an annual sustainability report whose numbers nobody remembers. It also creates the evidence base a brand needs if it later wants to make a public claim: without records, there is nothing to substantiate.
Packaging Weight and Freight: The Line Nobody Owns
Cutting yield gets the attention in most sustainability conversations, because it is the number a production team sees every day. Packaging rarely does, and yet it travels with every unit, is discarded within minutes of arrival, and adds chargeable volume to the freight that carries it there.
| Packaging element | What it costs | Reduction that usually survives a drop test |
|---|---|---|
| Individual polybag | Plastic per unit, discarded on arrival | Right-size the gauge; a thinner bag often performs the same job |
| Shaped insert or filler | Paper or foam volume inside the bag | Replace void fill with a folded paper shape sized to the cavity |
| Master carton | Board weight and chargeable volume | Size the carton to the units rather than to a standard case |
| Hangtag and care card | Printed material per unit | Combine into one card, or print the care information on the insert |
| Protective corner or sleeve | Extra material on structured shapes | Keep only where a drop test shows the corner actually fails |
- Weigh a packed unit and record it, so a change can be measured rather than estimated.
- Size the carton to the product rather than buying a standard case and filling it.
- Test the reduction before adopting it — a damaged arrival costs more than the material saved.
- Ask for the packaging weight to appear with the quotation, alongside yield and cutting waste.
- Separate protective material from presentation material, because only one of them has to survive the journey.
None of this is glamorous and none of it requires new equipment. It requires the weight to be recorded, which is the step most programmes skip, and a willingness to test a thinner specification rather than assume the current one is the minimum that works.
Repairability and Second Life: Extending the Useful Life
The largest reduction available to most bag programmes is not in how the bag is made but in how long it stays in use. A bag that is repaired twice carries its manufacturing impact across years rather than seasons, and whether it can be repaired at all is decided on the drawing board.
| Construction decision | Effect on repair | Practical specification |
|---|---|---|
| Riveted versus stitched handles | Stitched handles can be re-sewn; riveted ones need drilling out | Stitch load-bearing joints where the design allows |
| Lining fixed to the shell | A glued-in lining makes interior repair expensive | Fix the lining at accessible seams rather than fully bonding it |
| Standard versus proprietary hardware | Proprietary parts cannot be replaced later | Use standard zip gauges and common component sizes where possible |
| Turned and stitched versus bonded seams | Bonded seams rarely survive a repair attempt | Specify sewn construction at stress points |
| Availability of spare parts | Without spares, a small fault retires the bag | Order spare components with the bulk run |
- Ask which components can be replaced and which are permanently fixed, before the design is signed off.
- Order spare components with the production run — they cost little and extend the life of every unit.
- Written repair guidance in the box keeps a repairable design repairable in practice.
- Specify standard component sizes, because a proprietary part ends a bag's life early.
A programme can report useful life honestly only if it knows what fails first, which is why returns and repair data belong in the same review as yield and energy. The cheapest environmental improvement in most ranges is the one that keeps a well-made bag in service for another few years.
Ask for the numbers behind the process
Give us a style and we will report yield, cutting waste and packaging weight alongside the quote, and share the improvement actions already running on our production floor in Quanzhou, Fujian. Request a sample report at service@junyuanbags.com, or talk to us on WhatsApp at +86 177 5002 0688.
Frequently Asked Questions
What are the main environmental impacts of bag manufacturing?
The largest burdens sit upstream in hide production and tanning, where water use, effluent load and chemistry concentrate. On a cutting and assembly floor the dominant controllable impacts are solid waste from cutting offcuts and electricity for lighting, ventilation, motors and climate control. Packaging adds a small weight but a large perceived waste share, and freight emissions depend on shipping mode. A credible reduction plan addresses material specifications upstream and yield, waste separation and energy discipline on site.
How much leather is wasted in bag production?
Industry estimates for cutting utilisation on leather bag programmes commonly fall between 75 and 85 per cent, depending on hide quality, defect levels and how well patterns nest. That means 15 to 25 per cent of purchased hide leaves the table as offcuts. Defect-aware marking, revised nesting and panel consolidation improve the figure, and planning a small-goods or accessory line from the same hides raises effective yield again without changing the bag construction.
Does cutting and stitching use a lot of water?
No, comparatively little. Water use in leather sits overwhelmingly in the tannery's beamhouse, tanning, dyeing and finishing operations rather than on the bag floor. On-site water is domestic plus small quantities for edge painting and cleaning, where controlled dispensing and spill prevention keep volumes negligible. This is why a brand's meaningful water intervention is tannery selection and specification, not pressuring the cutting room.
What is a realistic energy reduction for a bag facility?
Most facilities can reduce electricity consumption through unglamorous measures: LED conversion with zoned switching, insulation and set-point discipline on cooling, servo motors on stitching machines, scheduled shutdown of presses and, often overlooked, compressed-air leak repair. Because consumption is spread across many small loads rather than one large process, the reliable route is sub-metering plus a routine that reviews consumption per production day. Improvement is usually incremental rather than dramatic.
How should a brand verify a tannery's environmental performance?
Start with current audit status and, crucially, the scope items actually covered, since an expired certificate supports nothing. Ask for effluent parameters and the treatment description for the article you buy rather than the tannery's best line, and prefer documented closed-loop or recycling systems over asserted ones. Consolidating your leather across fewer tanneries deepens oversight and increases your influence over process decisions, which matters more than the certificate count.
What does ISO 14001 actually prove?
It evidences that a facility operates a functioning environmental management system: identified impacts, set objectives, tracked performance, internal review and corrective action. It does not state that a particular order was produced with less energy or water, and it is not a product claim. ISO 14001 is useful as evidence of management discipline and of a partner's capacity to improve, but it should be paired with actual consumption and waste data before it supports any public statement.
How can waste be reduced without changing the design?
Through nesting and marking discipline. Defect-aware placement of patterns, revised nesting layouts and the same lining panel shared across multiple styles reduce consumption with no visual change to the product. Consolidating the material range also helps: fewer leathers and linings mean larger effective cutting areas and less remnant stock. These are production-engineering changes, so they are best briefed at pattern stage, before tooling and dies are cut.
Are leather offcuts waste or a resource?
They are a resource if a programme plans for them. Offcuts from bag production feed small leather goods, key fobs, card cases and internal reinforcement panels, raising effective yield from the same hides. Fibre recovery services also accept cutting waste for bonded applications. The caution is performance: bonded leather from recovered fibre is not equivalent to full-grain leather, so it belongs in stiff components or small goods, never load-bearing panels or straps.
Does sustainable manufacturing cost more?
Often it costs less. Yield improvements reduce material purchase, which is the largest unit cost in a leather bag. Waste separation lowers disposal charges and recovers scrap-metal value. Energy measures such as leak repair and LED conversion pay back within a predictable period. The costs concentrate in capital items and in the staff time needed to record and review data. Programmes that treat measurement as an overhead rather than a control tend to see the benefits only partially.
How do we set improvement targets with a production partner?
Attach them to records the partner already keeps: leather area per finished bag, cutting waste percentage, rejected-component rate, waste separated by stream, electricity per production day and packaging weight per unit. Six simple metrics reviewed quarterly outperform an annual report nobody reads, and they create the evidence base for any future public claim. Without records there is nothing to substantiate, so measurement discipline comes before target ambition.
What role does REACH play in manufacturing sustainability?
REACH governs restricted substances in articles placed on the EU market, including leather goods and their components. It is a chemistry and consumer-safety framework rather than a process performance standard, so it controls which substances may remain in the finished bag rather than how much energy was used to make it. A programme should treat REACH compliance as a baseline obligation, evidenced by testing and supplier declarations, separate from water, waste and energy performance.
Is sea freight better than air freight for bag shipping?
Generally yes for emissions per unit of product moved, which is why most bag programmes ship by sea on FOB Xiamen terms with a 35 to 50 day production window allowing the longer transit. Air freight is reserved for urgent replenishment or high-value small runs. The trade-off is time and cash flow rather than craft quality, and brands should factor the additional lead time into launch planning rather than defaulting to air when a schedule slips.
What waste streams should a bag facility separate?
At minimum: leather offcuts, textile and lining scrap, paper and corrugate, metal hardware and fixings, chemical and solvent waste including edge paint and adhesives, and rejected finished goods. Paper, metal and leather streams are straightforward and often have recovery routes. Chemical waste requires licensed handling and proper storage, while rejected goods should be dismantled for recoverable components rather than discarded. Separation without labels and ownership decays quickly, so nominate a floor owner.
Can a small brand influence manufacturing impact?
Yes, through specification rather than volume. Choosing leathers from a tannery with current audit scope, keeping the material palette narrow, asking for yield reporting, and specifying repairable construction all shift outcomes regardless of order size. Small brands often have more leverage than they assume because they can move quickly and because their orders can be consolidated onto production partners whose processes are already disciplined. The limit is upstream agriculture, which no single buyer controls.