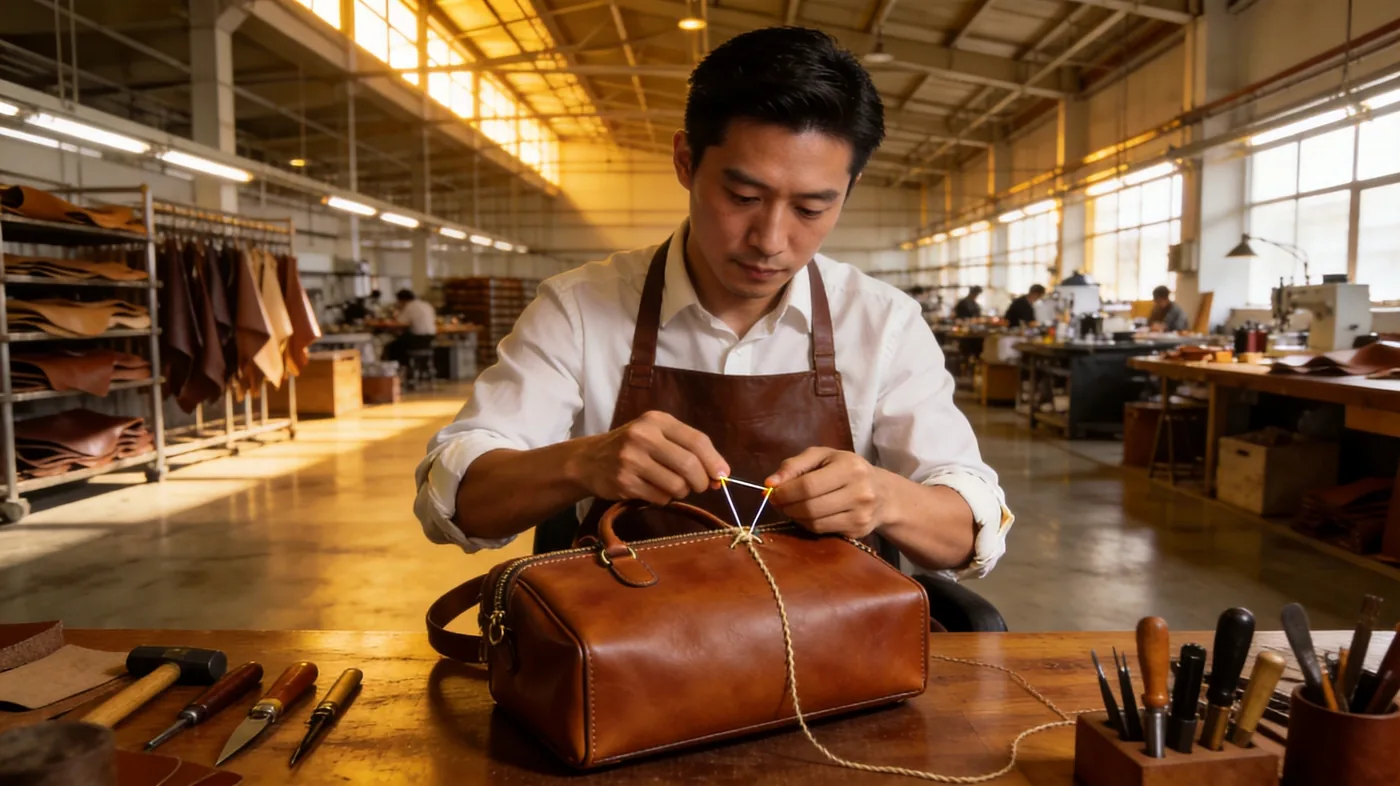
Bespoke bags are bags developed from your own brief: the pattern is drafted for you, the materials and hardware are selected for that pattern, and the finished specification is engineered so piece one and piece five hundred are the same object. A stock style printed with a logo is not bespoke; it is decoration, and it behaves differently on cost, tooling ownership and lead time. This guide defines the term as the trade uses it, walks the bespoke process end to end, breaks down what bespoke bags cost and why, compares bespoke with custom and made-to-measure, and sets out the brief structure and quality markers that separate a clean first run from an expensive rework.
What Bespoke Means for Bags
Bespoke means the bag did not exist before you commissioned it. In a genuine bespoke programme the silhouette is drawn from a brief, the panel geometry is patterned from scratch, the leather or textile is chosen for that geometry rather than fitted around a stock cutting file, and hardware is either selected from a vetted catalogue or tooled specifically for the design. The buyer owns the resulting specification and, in most commercial arrangements, the tooling paid for to produce it. The practical test is simple: if you remove your branding, does the bag still look like anything else on the market? If it does, you bought customisation, not bespoke.
The distinction is not pedantry. It determines three commercial outcomes. First, unit cost: a bespoke run carries new tooling, new pattern grading and a learning curve on the line, all of which sit inside the first order. Second, lead time: a new pattern must be sampled, corrected and re-sampled before bulk is authorised. Third, exclusivity: only a bespoke specification can be contractually ring-fenced from other buyers, whereas a shared base pattern cannot. Buyers searching for bespoke bag brands or comparing bespoke bags UK and bespoke bags USA programmes are usually, in effect, asking which of these three outcomes they are paying for.
Most programmes sit on a spectrum rather than at a pole. A first collection is often a made-to-measure core with one bespoke hero style, because the hero carries the press story while the core carries the margin. A mature label will invert that ratio once it knows which silhouettes sell through. Nothing about the spectrum is dishonest provided the brief says which tier each style occupies, and the price is built accordingly.
- A written technical pack: dimensional drawings, panel schedule, material call-outs and hardware references.
- A new pattern drafted and graded for the intended size range, with a cutter's marker and yield calculation.
- A prototype built in the intended material, not a substitute, followed by a corrected second sample where needed.
- Tooling or dies for any bespoke hardware, embossing plate, logo badge or moulded component.
- A confirmed bill of materials by line item, with consumption per unit and an agreed substitution policy.
- A pre-production sample retained as the golden reference for bulk and for inspection.
- An inspection protocol agreed before bulk begins, with the acceptable quality limit stated in writing.
- A written position on exclusivity: which elements are ring-fenced, for which territories, and for how long.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The Bespoke Process End to End
A bespoke bag programme is a sequence of gates, not a single transaction. Each gate produces an artefact you can approve or reject, and skipping a gate is the most common cause of a bulk run that does not match the sample that sold it. The stages below describe the path we run with brands, retailers and corporate buyers; the artefacts and gating factors are the same whether you work with us or audit another production partner.
- Stage 1 — Brief and feasibility. You supply drawings, references, target retail price, target volume and deadline. The programme team tests the brief against material availability, construction capability and cost, and returns a written feasibility note with the risks flagged before any money moves.
- Stage 2 — Specification and costing. The brief becomes a technical pack: dimensions, panel schedule, material call-outs by tannery or mill reference, hardware finishes, stitch specification and packing method. Costing is built from a line-item bill of materials plus a labour-minute estimate.
- Stage 3 — Pattern and material sourcing. The pattern is drafted and graded; the marker is calculated for yield. Leather, linings, hardware and trims are sourced or ordered. Where a tannery lot must be reserved, this is the gate that protects your colour standard across repeats.
- Stage 4 — Prototype. The first bag is built in the intended materials. Expect fit, balance and construction comments rather than perfection; the prototype exists to expose problems while they are still cheap.
- Stage 5 — Correction and second sample. Comments are applied to the pattern and the specification, and a corrected sample is produced. Complex constructions and multi-component travel pieces routinely need this second pass before they are right.
- Stage 6 — Compliance and testing. Where the destination market requires it, materials are submitted for restricted-substance and safety testing against the relevant framework — REACH in the European Union, CPSIA in the United States — and lining or textile components may be certified to OEKO-TEX standards.
- Stage 7 — Pre-production sample and golden seal. A sample from the bulk-intent material lot is signed off and retained. This is the physical reference against which inspection is later judged; without it, any dispute about bulk quality becomes a matter of opinion.
- Stage 8 — Bulk production. Cutting, skiving, assembly, edge finishing, hardware setting and final assembly run to the sealed reference, with in-line checks at the operations where defects are cheapest to catch.
- Stage 9 — Inspection and release. Finished goods are inspected to the agreed sampling plan, packing is verified against the carton specification, and the balance payment releases the shipment.
- Stage 10 — Logistics and repeat. Goods ship on the agreed Incoterm with documentation for customs. The retained specification and tooling make the repeat run faster and cheaper than the first.
| Stage | What happens | Artefact you receive | Gating factor |
|---|---|---|---|
| Brief and feasibility | Commercial and technical test of the concept | Feasibility note with risks and target cost band | Clarity of drawings and target price |
| Specification | Brief converted into a buildable technical pack | Technical pack and line-item bill of materials | Material and hardware confirmation |
| Pattern and sourcing | Pattern drafted, graded and marked for yield | Pattern, marker, yield calculation | Leather lot reservation and trim lead times |
| Prototype | First build in the intended materials | Physical prototype with construction comments | Availability of the specified material |
| Correction | Comments applied to pattern and specification | Corrected second sample | Number and severity of changes |
| Compliance | Restricted-substance and safety testing | Test reports against the required framework | Laboratory turnaround and material submission |
| Pre-production | Bulk-intent sample sealed as the reference | Golden sample and signed specification | Buyer sign-off |
| Bulk | Cutting, assembly, finishing and packing | Production units with in-line records | Deposit, material arrival and line capacity |
| Inspection | Sampling to the agreed acceptable quality limit | Inspection report and release note | Agreed inspection standard |
| Logistics | Shipment, documentation and customs clearance | Shipping documents and tracking | Incoterm, booking and balance payment |
Two numbers govern the calendar. Sampling runs 6–10 working days for standard constructions and 12–15 working days where the build is complex, hardware is bespoke or multiple components must be married. Bulk production runs 35–50 days after sample approval. Everything else in the schedule — material reservation, testing, shipping — sits around those two windows, and any brief that compresses them is buying risk rather than time.
What Bespoke Bags Cost
There is no list price for bespoke bags, and any supplier quoting one without a technical pack is quoting a guess. Unit price is the sum of material consumption, purchased components, labour minutes, tooling amortised across the order, overhead, compliance cost and the commercial terms attached to the Incoterm. Understanding which lever moves which line is the difference between a negotiation and a misunderstanding, and it is the single most useful thing a buyer can learn before asking for a bespoke bags price.
| Cost factor | How it moves the unit price | How to keep it under control |
|---|---|---|
| Leather selection and yield | The largest single line in most leather programmes. Grade, cut selection and panel size drive consumption per unit more than headline hide price. | Design panels to the hide. Ask for the yield calculation before you approve the pattern, and accept grain-direction rules. |
| Hardware | Stock hardware is predictable; bespoke dies, moulds and plating add both unit cost and a one-off tooling charge. | Use stock hardware in the first run and reserve bespoke tooling for the style you know will repeat. |
| Construction labour minutes | Hand-burnished edges, hand-set rivets, piped seams and lined gussets add minutes, and minutes are money at scale. | Specify hand work where the customer sees it, machine work where they do not. |
| Pattern complexity | Every extra panel is another cutting, skiving and sewing operation, plus more waste. | Reduce panel count in the first collection; add complexity to proven silhouettes later. |
| Tooling and moulds | One-off charges for embossing plates, logo dies and moulded components, amortised over the order. | Amortise across a larger first order or a committed repeat schedule. |
| Order quantity against MOQ | Below the 500-piece threshold per style and colourway, fixed costs spread over fewer units and the unit price rises. | Consolidate colourways, or run a small-batch pilot to prove demand before committing to the full run. |
| Testing and compliance | Restricted-substance testing, safety testing and certification are per-material costs. | Use materials with existing certification and limit the number of distinct materials per style. |
| Finishing and packaging | Dust bags, boxes, tissue, barcode and labelling work add both material and labour. | Specify retail packaging only where retail packaging is needed; ship bulk-packed for e-commerce. |
| Logistics and Incoterms | Freight, insurance, duty and port charges move the landed cost independently of the unit price. | Compare quotes on the same Incoterm — FOB Xiamen is our default, with EXW, CIF and DDP available on request. |
The most common costing mistake is to compare two quotes that were never built on the same specification. A price built on a bonded lining will always beat one built on a woven lining; a price that excludes testing will always beat one that includes it. Before you compare bespoke bag price quotations, normalise them: same bill of materials, same packing, same Incoterm, same inspection standard, same assumed defect allowance. Only then is the delta real.
- Spend on the material the customer touches first — the outer leather or shell — because perception is built at the point of contact.
- Spend on hardware cycles and plating thickness, since failure here generates returns rather than complaints.
- Spend on the edge finish, which is the fastest visual read of quality in a luxury bag.
- Save on interior panelling that is never seen once the bag is in use.
- Save on packaging in the first run and upgrade it when the sell-through data justifies it.
- Save on colourway breadth: one colourway at 500 pieces costs less per unit than three at 167 each.
- Never save on compliance testing in a regulated market; the exposure is not linear and it is not recoverable.
Bespoke vs Custom vs Made-to-Measure
The three terms are used interchangeably in marketing and precisely in production, and the gap between those two usages is where disputes begin. The comparison below is the trade reading: what changes is who owns the pattern, how much of the cost is fixed, and how defensible your exclusivity claim is.
| Dimension | Bespoke | Custom / customised | Made to measure |
|---|---|---|---|
| Pattern | Drafted from scratch for the buyer | Existing pattern, modified | Existing pattern, dimensionally adjusted |
| Tooling | New dies, plates or moulds where needed | Usually none, or a logo plate only | Usually none |
| Design freedom | Full, within construction physics | Colour, hardware, lining, branding | Dimensions only |
| Exclusivity | Defensible and contractually ring-fenced | Limited; the base style is shared | Limited; the base style is shared |
| Fixed cost in the first order | Highest — tooling, grading, learning curve | Low | Low to moderate |
| Sampling | Prototype plus correction pass as standard | One confirmation sample | One dimensional sample |
| Minimum quantity | 500 pieces per style and colourway | Often lower, set by the base style | Often lower, set by the base style |
| Best for | Hero styles, signature silhouettes, brand-defining product | Fast entry, colour stories, gift programmes | Fit-driven categories: laptop, garment, cabin, trolley |
Choose by what the product has to do commercially. If the bag is the reason a customer chooses your brand, it should be bespoke. If it extends a range that already has a hero, customisation is faster and cheaper. If the problem you are solving is dimensional — a 16-inch laptop, a specific cabin allowance, a garment bag that must fold a jacket without creasing — made-to-measure is the correct instrument and bespoke would be over-engineering.
- Bespoke suits a signature silhouette you intend to repeat for several seasons.
- Customisation suits seasonal colourways, capsule drops and corporate gift programmes with fixed branding requirements.
- Made-to-measure suits technical categories where the fit is the selling point and the silhouette is conventional.
- A blended programme — one bespoke hero, two customised support styles — is the most common structure in a first collection.
- Whichever route you take, state the tier in the brief so the quote is built on the same assumption you are.

Best Bespoke Bag Choices by Buyer Type
The right first bespoke bag depends on who is buying it. Margin structure, sell-through risk and the reason the bag exists all point to different starting silhouettes. The matrix below is the short form of the advice the programme team gives in a first conversation: pick the row that describes you, then read the specification priority as the thing to resolve before anything else in the brief.
| Buyer type | Start with | Specify first | Volume approach | Watch-out |
|---|---|---|---|---|
| Luxury fashion label | A structured top-handle or shoulder bag with a signature closure | Leather grade, edge finish, bespoke hardware | 500 pieces in one colourway; repeat before adding colours | Hand-work minutes inflating the labour estimate late in sampling |
| Contemporary direct-to-consumer brand | A convertible crossbody that works day to evening | Strap comfort, weight, hardware durability | Pilot small-batch, then scale the proven colourway | Over-colouring the first drop and splitting the MOQ three ways |
| Corporate gifting programme | A business bag or document folio with restrained branding | Branding method, packaging, delivery window | Consolidate into one style across recipients | Branding applied too prominently for the recipient to carry it |
| Hotel and hospitality group | An amenity or weekend piece sized to the guest profile | Lining durability, laundering, restocking cadence | Standing annual order against a retained specification | Specifying retail-grade finishes for a non-retail use case |
| Travel and luggage brand | A cabin-sized carry-on or duffel with a trolley sleeve | Wheel and handle cycles, weight, shell construction | Tool the shell once, then extend the family | Under-specifying hardware cycles for a checked-bag duty cycle |
| Private-label retailer | A tote or shopper with a clear price architecture | Unit cost against retail price, packing efficiency | Larger runs across fewer styles | Confusing private label with bespoke and paying for tooling you do not own |
| First-collection start-up | One hero bag plus one made-to-measure support style | The story: what makes the hero recognisable | Minimum viable run in the hero, customised support | Designing five styles before learning which one sells |
A buyer checklist worth running before you commit to a silhouette: it costs nothing to answer these questions in week one and considerably more to answer them in week nine, when the pattern is already graded and the leather lot is reserved.
- What does the bag have to carry, and what are the internal dimensions at the widest point rather than the nominal size?
- What is the retail price, and what multiple of the landed unit cost does that imply for your channel?
- Who is the wearer, and what is the duty cycle — daily commute, occasional travel, single-use gifting?
- Which element is the signature: the closure, the handle, the leather, the proportion?
- How many colourways can you realistically sell through at the minimum quantity each?
- What is the repeat plan, and does the tooling make sense against it?
- Which market is it shipping to, and which compliance framework applies there?
- What is the fallback if the first material lot fails testing — is a substitute approved?
- How will the bag be packed, and does that packing survive the chosen freight mode?
- Who signs off the golden sample, and is that person named in the brief?
How to Brief a Bespoke Programme
A brief is not a mood board. It is the document a pattern cutter, a material sourcer and a line supervisor will each read for different information, and its quality sets the ceiling on everything downstream. The steps below produce a brief that can be costed accurately on the first pass instead of the fourth.
- State the commercial frame first: target retail price, target landed cost, intended volume and the date the goods must be on the water or in the warehouse.
- Supply dimensional drawings with tolerances, not just a silhouette. Note the internal clearances that matter — laptop bay, bottle pocket, garment fold — because those drive the pattern.
- Attach reference images and say what you like about each. A reference without a reason is noise; 'the handle attachment on image three' is instruction.
- Call out materials by reference where you have one, and by performance where you do not: substance, temper, finish, colour standard and any certification requirement.
- Specify hardware by finish and function, and state the test expectation — cycle count for zips, pull strength for straps, plating thickness for metal.
- Define the branding method: emboss, deboss, foil, metal plate, woven label or print, with artwork supplied in vector and a placement dimension.
- Set the construction standard: stitch density, seam type, edge finish, lining style, interlining and any reinforcement at stress points.
- Name the compliance framework for the destination market and any customer-mandated standard — REACH, CPSIA, OEKO-TEX for linings, LWG-sourced leather where the brand has a tannery policy.
- State the packing and labelling requirement, including carton specification, barcode format and any retail packaging.
- Fix the approval protocol: who signs the technical pack, who signs the golden sample, and what happens if the two disagree.
- Declare the repeat intention. Tooling and material reservation decisions are made on that answer, and it changes the unit price.
- Ask for the bill of materials back, line by line, before you ask for a final price.
Quality Markers to Check Before You Commit
Quality in bag production is measurable, and the measurements are knowable before you place an order. The checklist below is what we would want a buyer to ask of any production partner, including ourselves; a partner who cannot answer these questions in writing is telling you something about how the bulk run will go.
- Stitch density: count stitches per inch on the prototype and require the same figure in bulk, with a stated tolerance.
- Seam allowance and reinforcement at every stress point: handle roots, strap anchors, zip ends and base corners.
- Edge finishing: smoothness, adhesion, colour consistency and resistance to cracking after flexing.
- Grain direction and panel matching: consistent direction across the front panel and symmetry across a pair of panels.
- Hardware setting: no rotation, no scratching, correct alignment, and a stated cycle-test result for zips and clips.
- Plating thickness and colour-fastness of metal components, verified by a rub test on the sample.
- Lining fit: no pooling at the base, no tension at the top seam, clean turning at the mouth.
- Colour consistency between the outer material, the lining, the thread and the edge paint, assessed under retail lighting.
- Dimensional tolerance against the technical pack, measured on three units rather than one.
- Odour and finish cure: a bag packed too soon after finishing will arrive smelling of solvent.
- Carton specification and packing density: crushing in transit is a packing failure, not a product failure.
- Inspection protocol: AQL 2.5 under ISO 2859-1, single sampling, general level II, applied and reported in writing.
- Traceability: material lot references recorded against the production batch so a repeat can be matched.
| Marker | How to verify | Evidence to ask for |
|---|---|---|
| Stitch density and seam type | Count and measure on the golden sample | Written stitch specification in the technical pack |
| Edge finish durability | Flex and rub test on a sample edge | Sample with the production finishing method |
| Hardware performance | Cycle and pull testing | Test report or supplier datasheet with cycle counts |
| Material compliance | Restricted-substance testing for the destination market | Test report against REACH, CPSIA or the applicable framework |
| Lining and textile safety | Certification of the lining and thread | OEKO-TEX certificate where the brand requires it |
| Leather sourcing | Tannery traceability and environmental audit status | LWG tannery reference and lot documentation |
| Bulk conformance | Statistical sampling against a stated standard | Inspection report citing ISO 2859-1 at AQL 2.5, general level II |
| Management systems | Certification of the production floor's quality and environmental systems | ISO 9001 and ISO 14001 certificates, plus SGS verification of the site |
Where a brand has the volume and the exposure, an independent third-party audit of the production site is worth the fee, and is standard practice among the established houses. Our own floor is SGS-verified at 4,950 m² in Quanzhou, Fujian, with 137 staff, seven lines, 149 machines and a monthly capacity of 200,000 pieces; those figures are published so a buyer can size us against their programme before the first call. The entity was founded in 2014 and the principal has been in the trade since 2004.

Working With a Programme Partner Remotely
Almost every bespoke bags programme is run across time zones, and distance is a manageable risk provided it is managed. The failure mode is not geography; it is ambiguity left in place because a call felt easier than a document. The table below maps the risks that actually materialise in remote programmes and the control that answers each.
| Risk | Control | Cadence |
|---|---|---|
| Specification drift between calls | One written technical pack, versioned, with changes logged | Every change, in writing |
| Sample comments lost in translation | Annotated photographs with numbered comments against a sample reference | Each sampling round |
| Material substitution without approval | Written substitution policy stating what may be substituted and who approves it | At specification sign-off |
| Colour standard drifting across lots | Retained reference swatch and a sealed golden sample for every colourway | Each repeat |
| Schedule slippage discovered late | A shared critical path with named owners at each gate | Weekly during development |
| Quality expectations set only verbally | Inspection standard agreed before bulk, with the accepted defect list written down | Before bulk authorisation |
| Shipment documentation errors | Document checklist verified before balance payment is released | Per shipment |
A remote programme runs well when the artefacts travel instead of the opinions. Ask for photographs at defined moments: first cuts off the marker, first assembled shell, hardware set but unfinished, and the finished pre-production sample. Each photograph is a decision point, and each decision point is cheaper before the next operation begins. Video walk-throughs of the line are now routine and are a reasonable request at any stage of the programme.
- Agree a single written channel for specification changes and a single named approver on each side.
- Hold a fixed weekly development call during sampling, with the agenda circulated the day before.
- Require a photograph at every decision point rather than a verbal assurance that a stage is complete.
- Confirm the critical path in writing whenever a date moves, including the knock-on effect on bulk and shipping.
- Keep the golden sample physically retained on the production side for the life of the programme.
- Treat the inspection standard as a commercial document, signed before bulk starts, not negotiated afterwards.
The practical test of a remote partner is how they handle the first disagreement. A good programme coordinator will show you the constraint — a material lot that failed, an operation the line cannot hold to tolerance, a freight window that has closed — and give you the options with their cost and schedule attached. That is the behaviour to look for, and it is the behaviour we aim to hold. Programmes start with a brief and a conversation; the contact page carries the direct routes to the programme team, including service@junyuanbags.com and WhatsApp +86 177 5002 0688.
Start a bespoke bag programme
Send the drawings, the target price and the volume you have in mind. The programme team will return a written feasibility note covering construction, material options, sampling window and cost band — before any commitment is made.
Frequently Asked Questions
What does bespoke mean when it is applied to bags?
Bespoke means the bag did not exist before you commissioned it. The silhouette is drawn from your brief, the pattern is drafted and graded from scratch, the materials and hardware are selected for that pattern, and the specification is engineered so that every unit in the run matches the approved reference. The practical test is that removing your branding still leaves a bag unlike anything else on the market.
How much do bespoke bags cost?
There is no list price, because unit cost is built from material consumption, purchased components, labour minutes, tooling amortised across the order, compliance testing and the commercial terms attached to the Incoterm. The dominant line in a leather programme is usually the hide, driven by grade, cut selection and panel yield. To compare bespoke bags price quotations, normalise them on the same bill of materials, packing, Incoterm and inspection standard first.
What is the difference between bespoke, custom and made-to-measure bags?
Bespoke drafts a new pattern and usually new tooling, giving defensible exclusivity at the highest fixed cost. Customised applies colour, hardware, lining or branding to an existing shared pattern. Made-to-measure adjusts an existing pattern to a dimension set such as a laptop bay or cabin allowance without redrawing the silhouette. Only bespoke produces a specification you can ring-fence contractually from other buyers.
What is the minimum order quantity for bespoke bags?
The standard threshold is 500 pieces per style and colourway, which is the level at which tooling, pattern grading and the line learning curve spread across enough units to hold the unit price down. Smaller runs are possible through a small-batch pilot, which is generally used to prove demand before committing to a full programme; the unit price on a pilot is higher because the fixed costs are spread more thinly.
How long does a bespoke bag programme take from brief to delivery?
Two windows govern the calendar. Sampling runs 6–10 working days for standard constructions, extending to 12–15 working days where the build is complex, hardware is bespoke or several components must be married. Bulk production runs 35–50 days after sample approval. Material reservation, compliance testing and freight sit around those windows, so any brief that compresses them is buying risk rather than time.
Can I order a single bespoke handbag?
A one-off piece is a craft commission rather than a production programme, and most production floors are not set up for it economically: the pattern, marker and setup cost the same whether one bag or five hundred are cut. The commercial route is a small-batch pilot run, which gives you a small physical quantity to photograph, sell from or gift, at a unit price that reflects the unamortised setup.
Can UK brands run a bespoke bags programme with an overseas production partner?
Yes, and it is the normal structure for most contemporary labels in the United Kingdom. The practical requirements are a written technical pack, a named approver on both sides, and compliance against the framework that applies at the point of import — REACH for restricted substances, with OEKO-TEX certification commonly requested for linings. Distance is manageable where specification changes travel as versioned documents rather than verbal instructions.
What should US buyers check before importing bespoke bags?
Confirm the compliance position for the destination market, including CPSIA where the product falls within its scope, and restricted-substance testing against the relevant state and federal requirements. Then fix the commercial terms: FOB Xiamen is the standard quotation, with EXW, CIF and DDP available on request, and T/T terms of 30% deposit and 70% before shipment. Agree the inspection standard before bulk starts, not after.
Which materials are best for bespoke leather bags?
It depends on the duty cycle and the price architecture. Full-grain leather gives the best ageing and the highest material cost; corrected-grain and top-grain offer consistency of surface at a lower price and a better cutting yield. Where a brand has a sourcing policy, ask for tannery traceability and Leather Working Group environmental audit status, and pair the outer with a lining certified to OEKO-TEX standards where required.
How do I brief a bespoke bag programme properly?
Start with the commercial frame: target retail price, target landed cost, volume and the date the goods must ship. Then supply dimensional drawings with tolerances and the internal clearances that drive the pattern, call out materials by reference or performance, specify hardware by finish and test expectation, define the branding method with vector artwork, and state the construction standard. Close with the approval protocol and your repeat intention.
What quality checks should I run before authorising bulk production?
Check stitch density against a written specification, reinforcement at handle roots and strap anchors, edge finish durability after flexing, grain direction and panel symmetry, hardware setting and cycle-test results, and dimensional tolerance measured across three units. Confirm the inspection protocol in writing: AQL 2.5 under ISO 2859-1, single sampling, general level II. Retain a sealed golden sample as the physical reference for the run.
Is a bespoke bag cheaper than a private-label bag?
Per unit, usually not. Private label spreads a shared pattern and existing tooling across the run, so the buyer avoids the fixed development cost. Bespoke buys exclusivity, pattern ownership and a silhouette nobody else can sell, which is worth the premium when the bag is the reason a customer chooses the brand. Where the bag is extending an existing range, customisation or private label is the more efficient instrument.
Can I put my logo on a bespoke bag?
Yes, and the method should be specified in the brief with artwork supplied in vector and a placement dimension. Embossing and debossing suit leather and need a bespoke plate; metal plates and badges carry a tooling charge; foil, print and woven labels are lower-cost options. Note that branding alone does not make a bag bespoke — it is the pattern, materials and construction that determine the tier.
What does made to measure mean for a bag in trade terms?
It means an existing pattern has been adjusted to a dimension set rather than redrawn. Typical adjustments are a laptop bay width, a garment bag fold length, a trolley handle height or a cabin allowance. It is the correct instrument for fit-driven categories because the development cost stays low and the sampling passes quickly, while the dimensional problem that actually matters to the customer is solved precisely.
How do I compare bespoke bag brands and production partners?
Compare on evidence rather than presentation. Ask for the bill of materials line by line, the published capacity and verification of the production site, the compliance certificates that apply to your market, and the inspection standard they will accept in writing. Then test responsiveness: send a brief with a genuine constraint in it and see whether you receive options with costs and dates attached, or assurances without them.