
The workflow from bag design to production runs through six stages: brief and concept, design and technical pack, sampling and iteration, material lock and pre-production preparation, bulk production, and inspection with delivery. Each stage produces a defined output that the next stage depends on, and each ends with a decision — approve, revise or hold. The value of the framework is not bureaucracy but sequencing: it keeps expensive stages from beginning before cheap ones are settled.
This article explains the six-stage workflow as it runs on a modern production floor, what each stage delivers, how long it takes and which decisions a brand has to make along the way. It is written for design teams and sourcing managers who want a single map from first idea to delivered carton rather than an overview of isolated tasks.
The workflow is deliberately front-loaded. Roughly the first half of the timeline is spent before any bulk material is cut, because decisions taken early — silhouette, construction, materials, tolerance — are cheap to change and decisions taken late are not. Stitch marks in leather do not lift out, so the workflow exists to make sure the bag is right on paper and in a sample before it is made in quantity.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The Six Stages at a Glance
The six stages are sequential, but they are not all equal in cost or in risk. The table below sets out what each stage does, what it delivers and what a brand must decide before moving on. Read together, the stages describe a single flow of commitment: from idea, to specification, to a physical reference, to a controlled run.
| Stage | Purpose | Output | Decision to unlock the next stage |
|---|---|---|---|
| 1. Brief and concept | Define the commercial and design intent | Concept direction and target price | Approve the concept to develop |
| 2. Design and technical pack | Convert concept into a buildable specification | Patterns, bill of materials, construction notes | Freeze the specification |
| 3. Sampling and iteration | Prove the design physically | Signed physical sample | Approve the sample for production |
| 4. Material lock and pre-production | Secure materials and prepare the line | Confirmed material lots and line slot | Release the run |
| 5. Bulk production | Reproduce the sample at volume | Produced units in work in progress | Complete the run |
| 6. Inspection and delivery | Verify and ship to standard | Inspected goods, cartons, documents | Dispatch and reorder planning |
Two stages — sampling and bulk — attract most of the attention because they produce something physical. The stages either side, specification and material lock, are quieter but decide whether the two visible stages succeed. A workflow that skips them is not faster; it simply defers the cost to a point where the cost is higher.
Stage One: The Brief and Concept
The brief is where intent is fixed. It should state who the bag is for, what it must do, roughly what it should cost to make and what market it enters. A brief that is only a mood board leaves the critical commercial questions unanswered, and those questions resurface later as design compromises rather than as deliberate choices.
- Target customer and use case, so construction follows function rather than styling alone.
- Price ceiling and target cost of goods, because these bound material and hardware choices.
- Format and key dimensions: tote, crossbody, backpack or structured handheld, with approximate sizes.
- Materials direction, whether full-grain leather, top-grain, suede or a combined build with coated fabric.
- Quantity expectation, since a first run at the 500-piece minimum per style and colourway changes tooling decisions.
- Timeline and launch date, which set the sampling and production windows in reverse.
A strong brief does not remove creativity; it gives it a frame. Designers work faster when the boundaries are known, and a well-framed brief usually reduces the number of sampling rounds because fewer early choices have to be revisited.
Stage Two: Design and the Technical Pack
Stage two translates the concept into something a production floor can build without guessing. The centre of this work is the technical pack: a document that specifies the bag precisely enough that two people, working in different rooms, would produce the same result. Sketches, dimensions, materials and construction methods are all captured here.
| Element | What it specifies | Why it matters downstream |
|---|---|---|
| Graded patterns | Component shapes with seam allowances | Determines whether panels fit and yield well |
| Bill of materials | Every leather, lining, thread and hardware item by part code | Prevents silent component substitution |
| Construction notes | Assembly sequence, seam types, stitch density | Keeps repeat runs identical to the first |
| Dimension schedule | Measurements with tolerances | Makes pass or fail objective rather than subjective |
| Branding placement | Deboss, foil, label or hardware logo position | Protects brand presentation across the range |
| Finishing specification | Edge treatment, lining, interior fit-out | Sets the standard for the final inspection |
The technical pack is the single most reusable asset in a programme. Once it is complete, sampling proceeds once rather than repeatedly, production repeats reliably and a future reorder can be raised without redevelopment. Where a brand intends to build a range, the pack is effectively the product's engineering file, and it is worth the effort it demands.
Stage Three: Sampling and Iteration
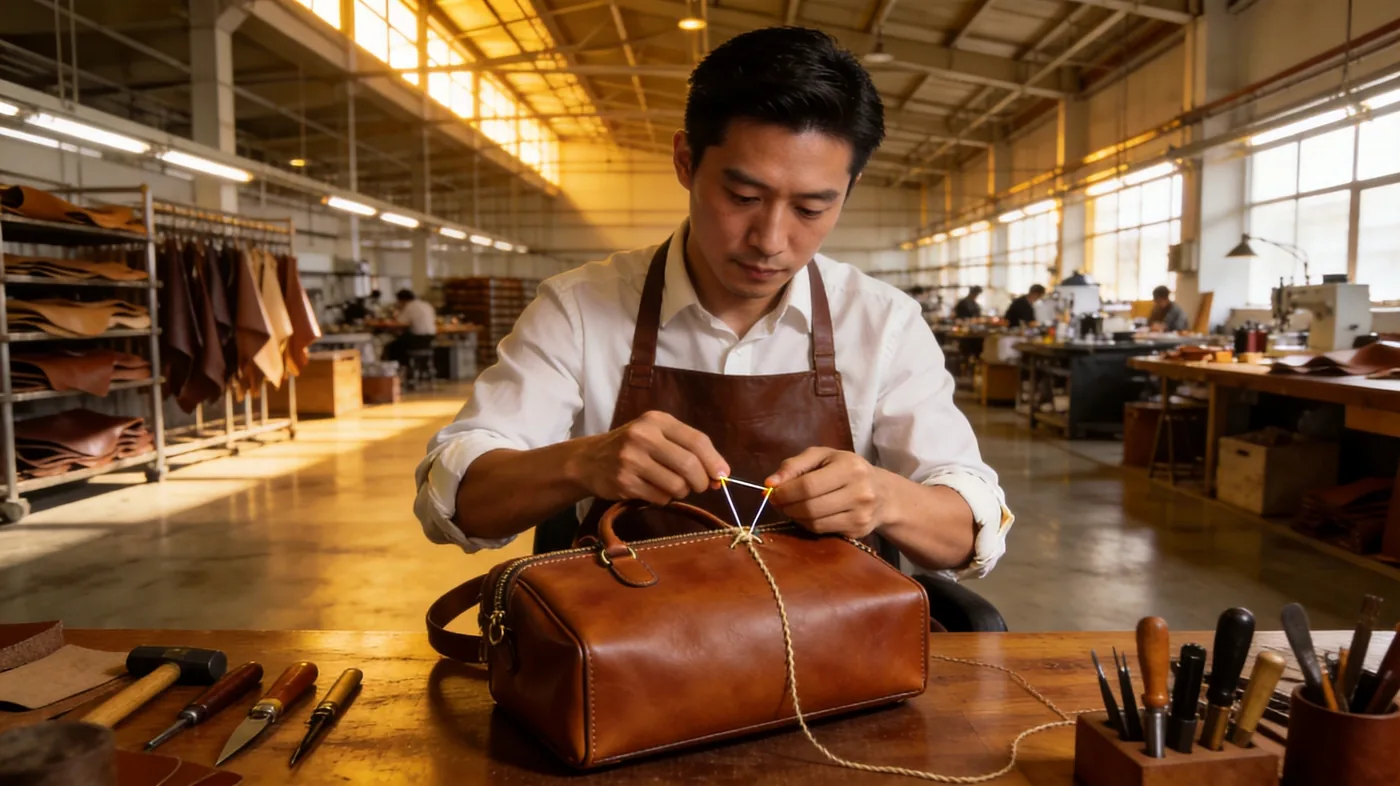
Sampling is where the specification meets physical reality. A sample is built in the intended materials and construction, then examined against both the design intent and the manufacturing realities — how the leather folds, how the hardware seats, how the bag hangs when loaded. Most styles sample in 6–10 working days; complex constructions take 12–15.
- Judge the sample against the specification first, then against the original sketch, so the assessment is objective.
- Test the function as well as the look: open and close zips, load the bag, check strap attachment and pocket access.
- Confirm hardware is the approved part number and finish, not a stand-in for development.
- Check all critical dimensions, since a sample that varies on paper will vary further at volume.
- Limit each revision round to defined changes, so that one round resolves specific issues rather than reopening the design.
- Sign and retain the approved sample, as it becomes the on-line reference for the whole run.
Iteration is normal, and a programme should budget for at least one revision round. What should not be normal is a revision caused by something the specification already covered. Distinguishing a genuine design change from an incomplete brief keeps the number of rounds — and the timeline — under control.
Stage Four: Material Lock and Pre-Production
Stage four is the point of no return for materials. Leather, linings, threads and hardware are ordered to the approved specification, and the material lots are fixed so that a run stays visually coherent. Unlike the visible stages, this work is largely administrative — and it is where the reliability of the whole run is settled.
A pre-production sample is the bridge between the development sample and the run. It is built from the actual production materials rather than from development stock, which is why it catches lot-based differences — a slightly different shade, a firmer or softer hand — that a development sample could not reveal. Where the pre-production sample matches the approved sample, the run can proceed with confidence.
Stage Five: Bulk Production
Bulk production turns the approved reference into a quantity of finished bags. It runs at 35–50 days after sample approval, and it is organised as a sequence of operations — cutting, preparation, assembly, hardware, finishing, packing — paced so that work moves steadily without piling up at any one stage.
| Operation | What happens | Principal control |
|---|---|---|
| Cutting | Hides assessed and panels extracted to the pattern | Panel dimensions and hide-grade consistency |
| Preparation | Skiving, reinforcement, creasing and basting | Thickness settings re-confirmed per material lot |
| Assembly | Panels, gussets, straps and lining joined in sequence | Stitch density, alignment and first-article check |
| Hardware and lining | Zips, locks, plates and interior fitted | Part-number and finish verification |
| Finishing | Edges painted or burnished and cured | Uniform finish and adequate cure time |
| Packing | Stuffing, wrapping and cartoning | Packing specification and carton count |
The controls during the run follow a simple pattern: check the first units against the full specification, check at intervals through the run on the attributes most likely to drift, and keep the signed sample physically present so that every operator has the same reference. On our SGS-verified production floor in Quanzhou, Fujian, seven lines and 149 machines across 4,950 m² support capacity up to 200,000 pieces per month, which means the binding constraint on any given run is availability at the required date rather than raw capacity.
Stage Six: Inspection, Packing and Delivery
The final stage verifies the run and gets it to the customer. Inspection samples the population against the agreed standard, packing protects the product in transit, and dispatch documentation completes the commercial side. It is also the stage where a brand gathers the information it needs to plan a reorder.
| Activity | What it confirms | Standard or note |
|---|---|---|
| Final inspection | The run meets the agreed defect standard | AQL 2.5 under ISO 2859-1, general level II |
| Defect classification | Major and minor defects carry agreed meaning | Classes fixed before inspection |
| Packing | Product protected and cartons configured to spec | Packing specification agreed in advance |
| Dispatch terms | Delivery responsibility and cost defined | FOB Xiamen default; EXW, CIF, DDP on request |
| Payment | Commercial settlement of the run | T/T — 30% deposit, balance before shipment |
| Reorder planning | Materials, lot references and sample retained | Locks in faster, cheaper repeat runs |
The workflow closes where it began, in a decision: whether to reorder, extend the range or revise the style. Retaining the technical pack, the approved sample and the material lot references means that decision can be acted on quickly, because the next run inherits the work already done. That inherited work is where the six-stage workflow pays back its discipline.
Map your design-to-production workflow
Tell the programme team where your design stands — a concept, a finished tech pack or a sample to refine — at service@junyuanbags.com or on WhatsApp at +86 177 5002 0688. We will set out a six-stage schedule, the sampling window and the run dates for your launch.
Frequently Asked Questions
What are the six stages of bag design to production?
The six stages are brief and concept, design and technical pack, sampling and iteration, material lock and pre-production preparation, bulk production, and inspection with delivery. Each stage delivers a defined output and ends with a decision to proceed. The sequence is fixed, because sampling cannot begin without a specification and bulk cannot begin without an approved sample and secured materials.
How long does the design-to-production workflow take in total?
The development half — design, technical pack and sampling — typically takes several weeks, with sampling at 6–10 working days for most styles and 12–15 for complex constructions. Bulk production runs at 35–50 days after sample approval. Adding brief and material lock, the whole journey from first idea to delivered carton is measured in weeks rather than days, and the early stages drive most of the variability.
What is the most important stage in the workflow?
Design and the technical pack, because it decides the quality of everything downstream. A complete pack lets a design sample once, produce reliably and reorder without redevelopment. A thin pack pushes unresolved decisions into sampling, where they cost more, and into production, where they cost most. The visible effort of sampling only pays off when the specification behind it is sound.
Why does the workflow spend so long before cutting material?
Because early decisions are cheap to change and late ones are not. Silhouette, construction, materials and tolerances can all be adjusted on paper or in a single sample at minimal cost, but changing them after a run has started means remaking patterns and cutting new panels. Front-loading the workflow protects the largest, least reversible spend — bulk production — from avoidable revision.
What is a pre-production sample and why does it matter?
A pre-production sample is a confirmation unit built from the actual production materials rather than from development stock. It matters because production lots can differ slightly from the leather used for the approved sample — a shade shift, a firmer or softer hand — and only a unit made from the real lot will reveal that. Where it matches the approved sample, the run can proceed with confidence.
How many sampling rounds should a brand expect?
Most programmes should budget for at least one revision round, and some complex constructions need two. What should be unusual is a revision caused by something the specification already covered; that signals an incomplete technical pack rather than a genuine design change. Limiting each round to defined changes keeps the number of iterations, and the timeline, under control.
When should production capacity be booked in the workflow?
Reserve the line slot at material lock rather than at sample approval. During peak windows capacity fills well ahead, and a run cannot start until both the sample is signed and a slot exists. Booking early commits capacity before the sample is final and so relies on an accurate forecast, but that risk is far smaller than discovering that no production time remains at the launch date.
What is material lock and why is it a point of no return?
Material lock is the stage at which leather, lining, thread and hardware are ordered to the approved specification and the lots are fixed. It is a point of no return because a run cannot look consistent if it draws from mixed lots, and because components ordered to a specification cannot easily be changed afterwards. Getting the lot and the part numbers right here is what keeps the run coherent.
How does the workflow differ for a first run and a reorder?
Development stages are largely skipped on a reorder. The brief, technical pack and sampling are already done, so the workflow begins at material lock with patterns, tooling and component specifications inherited from the first run. That is why reorders carry better economics and usually shorter lead times — the work of stages one to three has already been paid for once.
Who needs to be involved at each stage of the workflow?
The brief and concept stages need the brand's commercial and design owners. Design and technical pack need design and a technical partner who understands construction. Sampling needs both, plus agreement on what constitutes approval. Material lock and bulk production are the production partner's domain, with the brand confirming specification, and inspection involves the brand or an independent inspector at the release gate.
How is the specification frozen and what does that mean?
Freezing the specification means agreeing a single version of the design, its materials and its construction, and thereafter treating changes as formal revisions rather than informal adjustments. It gives sampling and production an unambiguous target and prevents the design from drifting during development. The signed sample and the technical pack together make the frozen specification tangible for everyone on the line.
What quality checks happen during bulk production?
Three levels work together. First-article inspection checks the first units off the line against the full specification. In-process inspection checks stitch density, alignment and finish at defined intervals during the run. Final inspection applies AQL 2.5 under ISO 2859-1, single sampling at general level II, with defect classes agreed in advance and the approved sample present as the reference.
Can the workflow be compressed to hit a launch date?
The development stages can be compressed modestly by working in parallel, but the physical times cannot. Sampling at 6–10 working days and bulk at 35–50 days are constraints of material and labour, not of administration, and edge finishing in particular needs cure time that cannot be rushed. Compressing beyond that point removes inspection or finishing work, which is exactly what protects quality.
What happens if the sample is rejected?
A rejection returns the design to stage three with a defined list of changes rather than a general instruction to improve. Each revision round should resolve specific issues, and the specification should be updated so the fix carries through to the next sample. A rejection early is far cheaper than a rejection discovered in bulk, which is one reason sampling earns its place in the workflow.
How is branding and logo placement handled in the workflow?
Branding is specified in the technical pack, with the deboss, foil stamp, stitched label or hardware logo marked on the pattern. It is then confirmed on the sample, so position, depth and finish are all approved physically before production. Treating branding as a specification item rather than a finishing touch keeps placement consistent across a run and across a whole range.
What information should a brand keep after the workflow ends?
Keep the frozen technical pack, the signed approved sample, the bill of materials with hardware part numbers, the material lot references and the dimensional record for each style. This retained information is what makes a reorder fast and reliable, because the next run inherits the specification, the reference and the material source rather than rebuilding them from scratch.