
Canvas, nylon and waxed cotton are not interchangeable substitutes for leather; each solves a different engineering problem. Cotton canvas carries structure and takes print and embroidery well, but it absorbs water and stains unless treated. Nylon delivers the highest strength-to-weight ratio and the best abrasion resistance per gram, and it dries quickly, though it reads as technical rather than luxury. Waxed cotton offers water resistance and a hand that develops character with use, at the cost of higher weight and a narrower thermal range. Choose by weight target, water exposure and intended ageing, then confirm the choice with the physical tests the bag will actually face.
Where fabric earns its place beside leather
Fabric enters a bag programme for three reasons: weight, cost and function. A leather body of the same volume can weigh more than twice a canvas or nylon equivalent, which matters in travel and in anything carried for more than an hour. Fabric also opens construction routes that leather resists: welded seams on technical nylon, printed patterns on canvas, and linings engineered for a specific task rather than a generic one. The trade-off is that fabric rarely delivers the same perception of permanence, so hybrid construction is usually the commercial answer.
Hybrid construction is where most of the interesting work now happens. A leather base and handles with a technical nylon body, or a waxed cotton shell with leather trim at the wear points, keeps the material where the hand and the eye fall and removes it where weight is the enemy. The engineering discipline is the same as for any mixed-material build: match the shrinkage, the stretch and the finishing tolerance before the panels are cut.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Canvas: cotton, linen and blended constructions
Canvas is the most forgiving of the three to work with and the most variable in performance. Cotton canvas in the twelve to twenty-four ounce range covers everything from a soft tote to a structured duffel; below that weight the fabric needs interfacing or a second layer, and above it the material becomes difficult to turn at corners. Linen canvas is lighter for the same strength, wrinkles readily and costs more, which is why it appears in limited runs rather than in volume programmes. Blends with polyester improve dimensional stability and reduce creasing.
The specification line that matters most is not weight but construction: yarn count, weave and finish. Two fabrics of identical weight can behave very differently at a seam, because a loosely woven cloth allows the stitch to pull under load while a tightly woven one resists it. Ask the mill for seam-slippage figures alongside the weight, and specify the finish, because an unfinished canvas will shrink unpredictably on the first wash or in a humid container.
| Canvas type | Typical weight range | Hand and appearance | Best application | Caution |
|---|---|---|---|---|
| Cotton duck, plain weave | Ten to eighteen ounces per square yard | Firm, flat, matte surface that softens with use | Tote bodies, linings, printed panels | Shrinkage must be controlled; pre-shrunk cloth avoids surprises after the first clean |
| Cotton canvas, heavy | Eighteen to twenty-four ounces per square yard | Rigid, holds shape without interfacing | Duffel bodies, tool bags, structured bottoms | Difficult to turn at tight corners; needs heavier needles and longer stitch length |
| Linen canvas | Eight to fourteen ounces per square yard | Dry hand, visible slub, creases readily | Limited editions and warm-weather collections | Higher cost and more creasing than a cotton equivalent |
| Cotton and polyester blend | Ten to sixteen ounces per square yard | More stable, less creasing, slightly less natural | Programmes requiring consistent repeat orders | Lower dye affinity with some pigment systems; confirm fastness |
| Recycled cotton canvas | Twelve to eighteen ounces per square yard | Comparable to virgin canvas with slight shade variance | Programmes with a documented recycled-content claim | Requires traceability documentation and the same restricted substance testing |
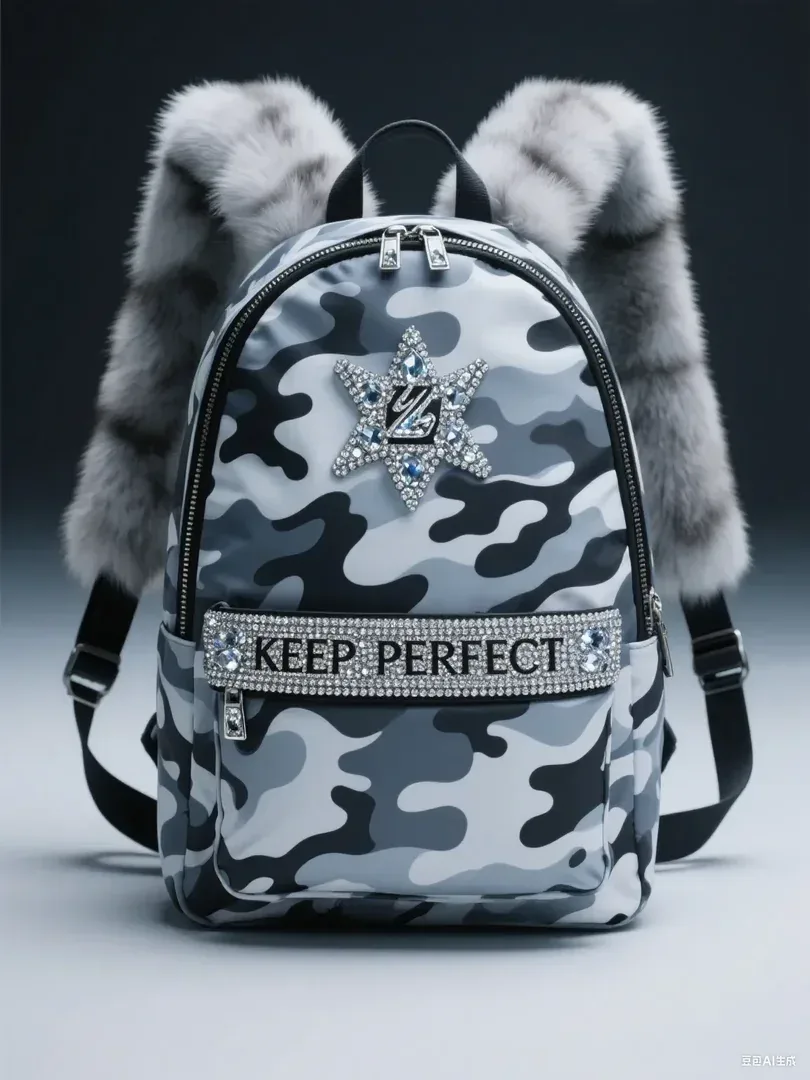
Nylon and polyester: denier, weave and coating
Nylon is specified in denier, and the number tells you most of what you need to know about the cloth's character. A seventy-denier fabric is light and packable, suited to linings and stuff sacks. Two hundred and ten to five hundred denier covers everyday bag bodies and travel pieces, where abrasion resistance and puncture resistance both matter. Above a thousand denier the fabric becomes stiff and heavy, and it is usually reserved for base panels and abrasion zones rather than for the whole shell.
Polyester costs less, holds colour well under ultraviolet exposure and resists mildew, which is why it dominates outdoor and promotional programmes. Nylon is tougher for the same weight and has better abrasion resistance, but it absorbs a little moisture and can yellow under prolonged ultraviolet exposure. Both are usually coated or laminated on the reverse face, and the coating governs water resistance and, in humid climates, service life, because polyurethane coatings can hydrolyse over time regardless of how well the face fabric performs.
| Specification | What it means | Typical use | Buying note |
|---|---|---|---|
| 70D nylon | Light ripstop or taffeta, very packable | Linings, stuff sacks, dust bags | Too light for a structural body without reinforcement |
| 210D nylon | Balanced weight and toughness | Lightweight daypacks and travel organisers | The practical entry point for a body fabric |
| 420D to 500D nylon | Abrasion resistant with reasonable drape | Everyday bags, backpack shells, base panels | The most common specification for a durable body fabric |
| 840D to 1000D nylon | Heavy, stiff, highly abrasion resistant | Base panels, tool bags, reinforcement zones | Heavy needles, slower sewing and a firmer silhouette |
| 600D polyester | Economical, colourfast, mildew resistant | Promotional bags, uniform programmes, budget travel | Better ultraviolet stability than nylon, lower abrasion resistance |
| Ripstop construction | Reinforcing grid arrests tears | Travel and technical applications | The grid is visible; it is a design element as well as a function |
| Polyurethane coating | Reverse-face polymer layer giving water resistance | Most coated bag fabrics | Hydrolysis risk in humid storage; specify a hydrolysis-resistant grade where relevant |
Waxed cotton: finish, hand and aftercare
Waxed cotton occupies the position furthest from technical performance and closest to craft. The cloth is cotton, usually a mid-weight canvas, impregnated with a paraffin or beeswax blend that sheds water and darkens with handling. Its appeal is behavioural: creases become patina, scuffs can be rubbed out with a thumb, and the finish can be renewed by the owner with a tin of wax. Its limitations are equally behavioural: the finish softens in heat, stiffens in cold, marks light-coloured clothing when new, and cannot be machine washed.
| Property | Behaviour in service | Specification implication | Aftercare requirement |
|---|---|---|---|
| Water resistance | Sheds rain effectively; resistance comes from the finish, not a membrane | Specify the wax loading and expect it to vary by colour | Re-waxing annually or after heavy use restores performance |
| Temperature response | Softens above roughly thirty degrees Celsius and stiffens in cold | Avoid for programmes shipping into very hot climates without ventilation | Store at room temperature; do not leave in a hot vehicle |
| Marking | Fresh wax can transfer to light fabrics and car interiors | A lighter wax loading reduces transfer but lowers water resistance | Warn the customer on the care label and the product page |
| Cleaning | Cannot be machine washed or dry cleaned | Plan for spot cleaning only, and design linings that can be wiped | Sponge with cold water; never use detergent |
| Aesthetics | Develops patina; creases and scuffs become character | A strength for heritage and outdoor positioning | Communicate the ageing behaviour as a feature rather than a defect |
| Weight | Heavier than an equivalent unwaxed canvas because of the impregnation | Factor the added mass into the target weight early | No special requirement beyond dry storage |
Coatings, laminates and water resistance
Water resistance is a system property, not a fabric property. A coated nylon shell with unsealed seams will leak at the stitch line long before the fabric is saturated, which is why seam sealing, zip selection and construction sequence decide the outcome as much as the cloth. Three approaches dominate: a reverse-face coating, a laminated membrane, and a durable water-repellent finish on the face. They can be combined, and most serious travel programmes combine at least two.
| Approach | How it works | Trade-off | Where it fits |
|---|---|---|---|
| Polyurethane reverse coating | A polymer layer on the reverse face blocks liquid water | Adds stiffness and carries a hydrolysis risk in humid storage | Everyday bags and most travel shells |
| Thermoplastic polyurethane laminate | A film bonded to the fabric, more durable than a coating | Higher cost and a firmer hand | Premium technical travel and marine applications |
| Durable water-repellent face finish | A surface treatment causing water to bead and run off | Wears off with abrasion and laundering; renewable | Any fabric body, as a complement to a coating |
| Silicone or wax impregnation | The finish sits within the cloth rather than on it | Breathable and repairable, with lower absolute resistance | Waxed cotton and heritage-positioned canvas |
| Seam sealing or welded seams | Tape or heat closes the stitch holes | Adds a production step and limits some design geometry | Where a water-resistance claim is made to the customer |
| Water-resistant zips and storm flaps | Closes the largest functional opening | Cost and a firmer opening action | Travel, outdoor and any bag sold on weather performance |
Weight, cost and yield: what fabric changes commercially
The commercial argument for fabric is strongest in travel, where a kilogram saved is felt directly by the user, and in entry price points, where a leather body cannot reach the target. Fabric also changes the cost structure: roll goods cut more predictably than hides, nesting waste is lower, and there is no natural marking to work around. Against that, fabric programmes depend on mill minimums per colourway, and a bespoke woven or printed cloth can carry a much higher development threshold than a stock leather colour.
| Factor | Canvas | Nylon | Waxed cotton |
|---|---|---|---|
| Relative material cost | Low to moderate, rising with weight and organic certification | Moderate, rising sharply with high denier and branded laminates | Moderate to high, because the impregnation is a separate process |
| Weight for a given strength | Heaviest of the three for equivalent performance | Lightest by a wide margin | Heavier than the base canvas because of the finish |
| Cutting yield | High; predictable widths and minimal waste | High; excellent nesting on rectangular panels | Moderate; waxed cloth is stiffer and harder to lay tightly |
| Development threshold | Low for stock colours, higher for bespoke weave or print | Low for stock deniers, high for custom colours and coatings | Moderate; finish variations are usually developed with the mill |
| Perceived value | Casual to premium depending on finishing and hardware | Technical; value comes from function and hardware | Heritage and craft; strong storytelling potential |
| Service life in daily use | Long, with edge wear at folds | Long, subject to coating hydrolysis | Long, provided the finish is maintained |
Testing fabric against the same standard as leather
Fabric is often specified with less rigour than leather, which is a mistake, because the failure modes are different and in some cases more abrupt. A coating can hydrolyse in a container and arrive as a sticky, delaminated panel, a printed canvas can crock onto a light garment, and a seam can slip under load without any visible prior damage. The tests below are the ones that prevent those failures reaching a customer, and they run in parallel with construction sampling rather than after it.
| Test | What it predicts | Typical method family | When to run it |
|---|---|---|---|
| Abrasion resistance | Face wear at corners, bases and strap contact points | Martindale or Wyzenbeek methods for textiles | At material selection and on any coating change |
| Tear and tensile strength | Resistance to running damage from a puncture or a snag | Standard textile tear and grab-test methods | Whenever denier or weave changes |
| Colour fastness to rubbing | Crocking onto light garments and linings | Standard textile rubbing fastness method | Per colourway, especially on saturated and printed cloth |
| Colour fastness to light | Fading in retail display and in sun-exposed use | Xenon-arc exposure method | For retail-facing collections and outdoor programmes |
| Water resistance | Whether the construction resists rain in practice | Spray test, hydrostatic head, or a shower test on the finished bag | Whenever a water-resistance claim is made |
| Hydrolysis resistance | Coating breakdown in humid storage and transit | Accelerated ageing under elevated humidity and temperature | For polyurethane-coated fabrics shipped to humid markets |
| Seam strength and slippage | Whether the stitch line holds under load | Seam strength and seam-slippage methods | On every new fabric and thread combination |
Specifying fabric in a hybrid bag programme
A hybrid programme succeeds or fails on the interfaces. Fabric and leather move differently under load and under humidity, so a panel that is perfectly flat at cutting can pucker after a week in a container. The sequence below is the order our programme team works through when a brief combines materials, and it is designed so that the incompatible combinations are eliminated during sampling rather than discovered in bulk.
- Fix the target weight for the finished bag before selecting any material; fabric choice follows from the number, not the other way round.
- Choose the fabric by denier or weight and confirm the finish, the coating and the shrinkage figure in writing.
- Match the stretch and recovery of the fabric to the leather at every joined seam, and reinforce where they differ.
- Specify thread, needle size and stitch length for the fabric rather than inheriting them from the leather specification.
- Run the physical panel on the assembled sample: abrasion, seam strength and water resistance together.
- Confirm the care label and aftercare instructions, because waxed cotton and coated nylon require different customer behaviour.
- Approve a retained reference sample from the bulk fabric lot so that repeat orders can be matched objectively.
Programmes that follow this order tend to move from brief to approved sample within the standard six to ten working days, or twelve to fifteen where the construction combines more than three material families. Bulk then runs thirty-five to fifty days after sample approval, inspected to AQL 2.5 under ISO 2859-1, single sampling, general level II, and shipped FOB Xiamen or on EXW, CIF or DDP terms where a programme requires them. Where a brand is uncertain between two fabrics, the most efficient next step is a side-by-side sample pair on the same pattern, because the difference in drape and weight becomes obvious only when the material is assembled.
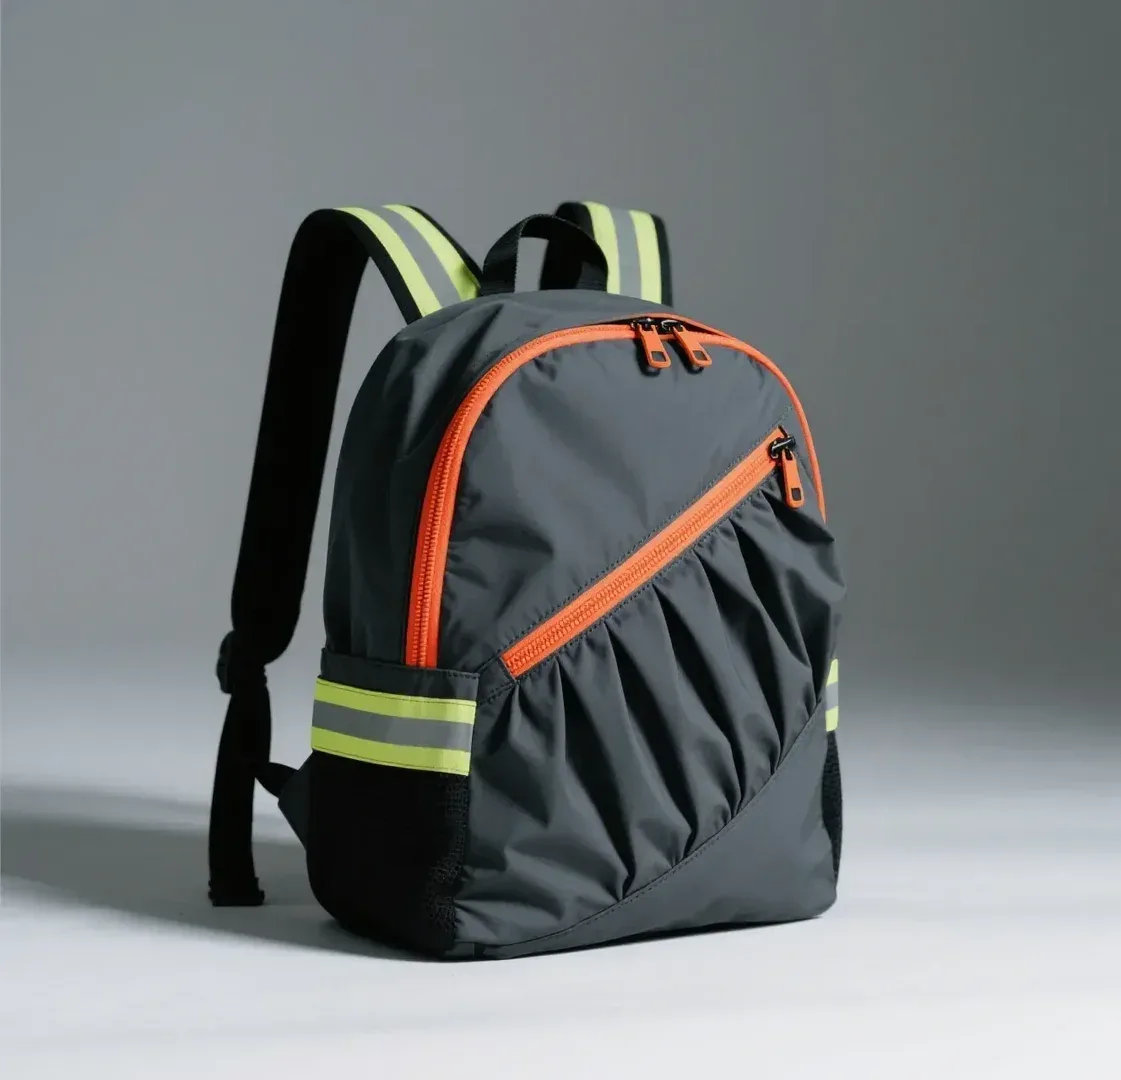
Test two fabrics on the same pattern before you commit
Send us your target weight, water-resistance requirement and price band, and we will build the same pattern in two candidate fabrics so you can compare drape, weight and assembly quality directly. Email service@junyuanbags.com or message the programme team on WhatsApp at +86 177 5002 0688.
Frequently Asked Questions
Which is the most durable bag fabric, canvas or nylon?
Nylon is more durable for the same weight and, in mid-to-high deniers, more durable outright in abrasion terms. Canvas is heavier for equivalent strength but fails more gracefully: it frays and softens rather than delaminating. Where the bag will be dragged over rough surfaces, a 420D to 500D nylon will outlast a comparable canvas; where it will be carried and set down, both perform well.
Is waxed cotton waterproof?
Waxed cotton is highly water resistant rather than waterproof. Water beads and runs off the surface, and the cloth resists a sustained shower, but the seams are not sealed and the finish is not a membrane. Prolonged immersion or pressure against a wet surface will eventually penetrate. For genuine waterproof performance you need a laminate or coating plus sealed seams and a water-resistant closure.
What denier of nylon should I specify for a backpack?
Between 210D and 500D for the body, depending on weight target and intended load. A 210D shell keeps a pack very light and suits day use, while 420D to 500D handles daily commuting and travel handling. Reserve 840D and above for base panels and abrasion zones, because those deniers add real weight and stiffness across a full shell.
Why do coated nylon bags sometimes become sticky or peel?
The usual cause is hydrolysis of the polyurethane coating, which breaks down under sustained heat and humidity. It is a storage and transit problem as much as a material problem, and it appears most often in containers that sit in humid ports. Specify a hydrolysis-resistant coating grade, control storage conditions, and run accelerated ageing on any fabric destined for a humid market.
Can canvas be made water resistant without changing how it looks?
Yes. A durable water-repellent finish on the face is almost invisible and causes water to bead, while a reverse-face coating adds resistance without altering the surface. Neither is permanent: the face finish wears with abrasion and the coating has a finite life. For a heritage look with real performance, combine a light face finish with a discreet coating.
How heavy should a canvas bag fabric be?
Ten to fourteen ounces per square yard suits soft totes and linings, fourteen to eighteen suits everyday bags with light structure, and eighteen to twenty-four gives a body that stands without interfacing. Above that range turning corners becomes difficult and the bag feels stiff. Match the weight to whether the design calls for structure from the cloth or from an internal frame.
Does fabric make a bag look less luxurious than leather?
Only if it is specified cheaply. A heavy waxed cotton with leather trim and solid brass hardware reads as heritage premium, and a dense matte nylon with machined hardware reads as technical premium. What undermines perception is a shiny coating, visible slippage at a seam or hardware that is out of proportion to the cloth, all of which are specification faults rather than material faults.
What is ripstop nylon and when is it useful?
Ripstop is woven with a reinforcing grid of thicker threads so that a tear stops at the grid instead of running across the panel. It is useful wherever puncture risk exists relative to fabric weight, such as lightweight travel packs and linings. The grid is visible in lighter deniers, so it functions as a design element as well as a performance one.
Can I print or embroider on canvas and nylon?
Canvas takes screen print, digital print and embroidery well, and it is the preferred substrate for graphic treatments. Nylon accepts print, though coatings and low surface energy can require pretreatment and curing trials, and embroidery needs a stabiliser to prevent puckering. Always run a crocking test on a printed panel, because pigment sitting on the surface can transfer.
How do I stop a fabric bag from shrinking after purchase?
Specify pre-shrunk or sanforised cloth, and confirm the residual shrinkage figure with the mill in both warp and weft. Where a natural canvas is required for its hand, allow for shrinkage in the pattern and pre-wash a sample panel before cutting. The residual figure should appear on the material specification, not only on the mill's technical sheet.
Are recycled fabrics as strong as virgin ones?
Recycled polyester and recycled nylon now perform close to virgin equivalents in tensile and abrasion terms, though consistency depends on the feedstock and the spinner. The practical difference is usually shade consistency between lots rather than strength. Ask for traceability documentation and run the same physical tests, because a recycled credential says nothing about mechanical performance.
Which fabric works best for a bag lining?
A smooth, tightly woven polyester or nylon in the 70D to 210D range is the usual choice: it resists abrasion from contents, allows items to slide in and out, and can be wiped clean. Cotton lining feels warmer and more natural but stains more readily and adds weight. Match the lining weight to the body so the bag does not collapse inward.
Can fabric and leather be combined in one bag reliably?
Yes, provided the interfaces are engineered. The two materials differ in stretch, recovery and moisture response, so joined seams need reinforcement and matched stitch specification. Reinforce the load paths with leather or webbing, test the assembled sample under load rather than the materials separately, and approve a retained reference from the bulk lot.
How long does it take to develop a bag in a new fabric?
Construction sampling runs six to ten working days, or twelve to fifteen for complex builds, with material testing running alongside. Fabric availability is usually the variable rather than assembly, because a stock colourway ships quickly while a bespoke weave, print or coating carries a mill minimum and a longer development window. Confirm fabric availability before you fix the sampling date.