Custom Leather Thermos Covers OEM — Insulated Bottle Holders
January 15, 2025
• Bespoke Bags Editorial Team • 12 min read
The global drinkware accessories market is experiencing a remarkable transformation, and at its center lies an unexpected hero: the leather thermos cover. What began as a niche product for outdoor enthusiasts has evolved into a mainstream accessory embraced by office professionals, fitness enthusiasts, and eco-conscious consumers worldwide. For brands looking to capitalize on this growing demand, partnering with a reliable OEM leather thermos cover manufacturer is the critical first step toward building a profitable product line.
At Bespoke Bags, we have been developing premium leather goods since 2004. Our 4,950 m² production floor in Quanzhou, China, has delivered millions of leather products for brands across the globe. In this comprehensive guide, we share everything you need to know about developing custom leather thermos covers — from material selection and manufacturing processes to pricing strategies and market trends.
Why Leather Thermos Covers Are a High-Growth Product Category
The insulated bottle holder market has expanded dramatically over the past decade, driven by several converging trends. The global reusable water bottle market was valued at over $8 billion in 2024 and continues to grow at a CAGR of approximately 6%. As consumers invest in premium insulated bottles from brands like Hydro Flask, Yeti, and Stanley, the demand for complementary accessories — particularly protective and stylish covers — has surged accordingly.
Leather thermos covers occupy a unique position in this market. They serve multiple functions simultaneously:
- Protection: Shielding expensive bottles from dents, scratches, and impact damage
- Insulation: Adding an extra thermal barrier to maintain beverage temperature longer
- Aesthetics: Elevating the visual appeal of utilitarian bottles with premium materials
- Brand Extension: Offering branded merchandise that complements core product lines
- Grip Enhancement: Providing a non-slip surface for easier handling
For brands in the outdoor gear, corporate gifting, lifestyle accessories, and premium drinkware sectors, leather thermos covers represent an accessible entry point into the accessories market. The product requires relatively low material investment compared to full bags, yet commands premium pricing when executed with quality materials and craftsmanship.
Leather thermos covers available in multiple styles, colors, and sizes for diverse brand requirements
Material Selection: The Foundation of Quality Leather Thermos Covers
The material composition of a leather thermos cover directly determines its durability, appearance, functionality, and retail price point. Understanding the available options is essential for brands developing their product specifications.
Outer Shell Materials
The exterior material is the most visible and tactile component of a thermos cover. It defines the product's perceived value and brand positioning.
Insulation and Lining Materials
The inner construction is equally critical. A leather thermos cover must deliver on its functional promise of temperature retention and bottle protection. The most common insulation materials include:
- Neoprene (3-5mm): The industry standard for thermal insulation. Provides excellent heat retention, moisture resistance, and cushioning. Closed-cell structure prevents water absorption.
- EVA Foam: Lightweight and rigid, offering structural support alongside thermal insulation. Ideal for covers that need to maintain their shape when the bottle is removed.
- PE Cotton (Pearl Cotton): An economical option providing basic thermal insulation and shock absorption. Commonly used in mid-range products.
- Reflective Aluminum Layer: Often combined with other insulation materials to reflect radiant heat, enhancing temperature retention by 15-20%.
- Microfiber Lining: Used as the innermost layer touching the bottle, providing a soft, scratch-free surface that protects bottle finishes.
Pro Tip: The most effective thermos covers combine multiple insulation layers. A typical high-performance construction might include: microfiber inner lining → PE cotton → reflective aluminum → neoprene → leather exterior. This multi-layer approach maximizes thermal efficiency while maintaining a slim profile.
Manufacturing Process: From Design to Finished Product
Understanding the manufacturing workflow helps brands plan their timelines, set realistic expectations, and identify opportunities for customization. At Bespoke Bags, our leather thermos cover production follows a meticulous multi-step process refined over 20+ years of leather goods development.
Step 1: Design and Pattern Development
Our design team works with clients to translate concepts into technical specifications. This includes determining the cover dimensions based on standard bottle sizes (commonly fitting 20oz, 30oz, 32oz, and 40oz bottles), selecting materials, designing closure mechanisms (magnetic snaps, zipper, Velcro, or slip-on), and planning branding placement.
Step 2: Material Sourcing and Preparation
Leather is inspected for quality, sorted by grade, and cut using precision dies or CNC cutting machines. Insulation materials are cut to specification. All components undergo incoming quality checks to ensure consistency and compliance with client requirements.
Step 3: Skiving and Edge Preparation
Leather edges are skived (thinned) at seam allowances to reduce bulk and ensure clean, professional finishes. Edge painting or burnishing is performed at this stage for exposed edges.
Step 4: Assembly and Stitching
Skilled artisans assemble the cover layers — bonding insulation to the leather shell, attaching lining, and sewing structural seams. Industrial sewing machines handle main construction while hand-finishing addresses detail work. Hardware (snaps, zippers, D-rings, handles) is attached during this phase.
Step 5: Quality Control and Finishing
Each unit undergoes thorough inspection: dimensional accuracy, stitching quality, hardware function, leather surface quality, insulation integrity, and overall appearance. Approved units are cleaned, conditioned (for genuine leather), and prepared for packaging.
Step 6: Packaging and Shipping
Products are packaged according to client specifications — from bulk poly bag packing to premium gift box presentation. We support full logistics coordination including FBA prep, retail-ready packaging, and direct-to-warehouse shipping.
Customization Options: Making Your Brand Stand Out
One of the greatest advantages of OEM manufacturing is the ability to create truly unique products. Bespoke Bags offers extensive customization capabilities through our OEM/ODM services and private label programs.
Branding Techniques
Design Customization Elements
- Size and Dimensions: Custom-fit to any bottle model, from standard 12oz tumblers to 64oz growlers
- Color: Full leather dyeing capability with Pantone color matching; hardware in gold, silver, gunmetal, rose gold, or custom finishes
- Closure Type: Magnetic snap, YKK zipper, Velcro hook-and-loop, button strap, or elastic band
- Additional Features: Carrying handles, shoulder straps, belt loops, carabiner clips, side pockets for accessories
- Interior Organization: Custom compartments for bottle plus additional items (keys, cards, earbuds)
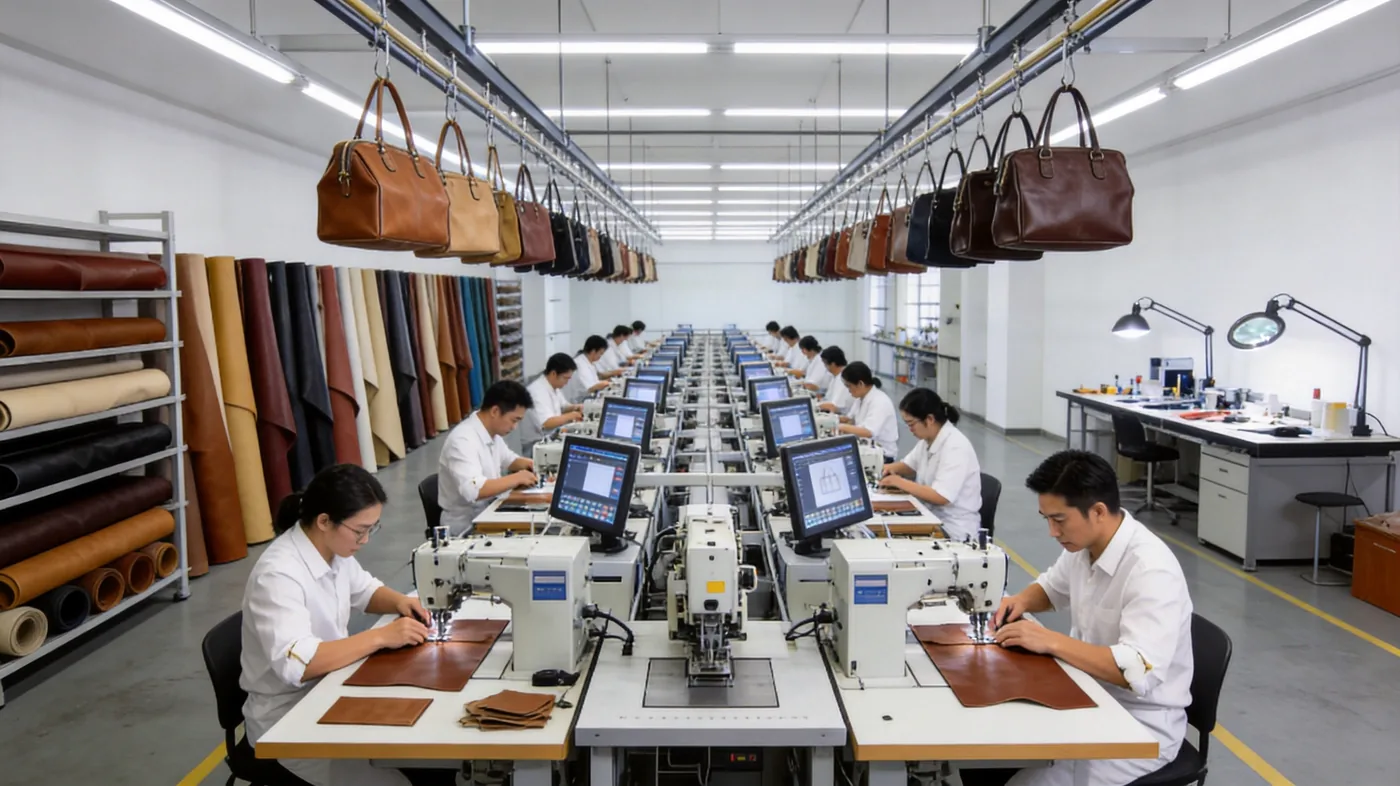
Precision stitching and premium material selection define every Bespoke Bags leather thermos cover
Target Markets and Application Scenarios
Leather thermos covers serve diverse market segments, each with distinct requirements and price sensitivity. Understanding your target market helps determine the optimal material specifications, design features, and pricing strategy for your OEM order.
Corporate and Promotional Products
Companies increasingly seek premium promotional items that convey brand quality. Leather thermos covers paired with branded drinkware create impressive executive gift sets. The combination of practicality and luxury positioning makes them ideal for client appreciation programs, employee onboarding kits, and conference giveaways. For corporate programs, our small batch capabilities enable cost-effective production even for initial order quantities.
Outdoor and Recreation Brands
Hiking, camping, and outdoor recreation brands benefit from leather thermos covers that combine rugged durability with aesthetic appeal. Waxed canvas and leather combinations, reinforced base plates, and integrated carabiner clips resonate strongly with outdoor consumers. These brands often require products that complement their broader gear ecosystem, making our custom collections service particularly valuable.
Lifestyle and Fashion Accessories
Fashion-forward consumers view thermos covers as style accessories rather than mere protective gear. This segment demands premium materials (full-grain leather, exotic leathers), fashion-forward colors, and design details that align with current trends. Brands in this space typically achieve the highest retail margins — often 5-8x manufacturing cost.
Drinkware Brand Extensions
Established insulated bottle brands frequently expand into accessory categories to increase customer lifetime value and average order value. Leather thermos covers represent a natural extension, and our custom design services help brands develop accessories that perfectly complement their existing bottle lines.
Pricing Structure and Order Economics
Understanding the cost structure of custom leather thermos covers helps brands set appropriate retail prices and forecast margins. Below is a general pricing framework based on our 20+ years of bag development experience.
Cost Breakdown by Component
Note: Prices above are indicative ranges for reference only. Actual pricing depends on specific material selections, design complexity, order quantity, and current material costs. Contact us at service@junyuanbags.com for a detailed quotation tailored to your specifications.
Quality Standards and Compliance
As an experienced OEM programme partner, Bespoke Bags maintains rigorous quality standards across all product categories. Our quality control system encompasses multiple checkpoints throughout the production process, ensuring every leather thermos cover meets both our internal standards and our clients' specific requirements.
Quality Testing Protocols
- Material Testing: Leather thickness verification, colorfastness testing, tensile strength measurement, and chemical compliance screening (REACH, Prop 65, CPSIA)
- Dimensional Accuracy: Each cover verified against technical specifications with tolerance of ±1mm
- Stitching Integrity: Stitch-per-inch verification, pull-strength testing on critical seams
- Hardware Function: Snap strength testing (minimum 30N pull force), zipper cycle testing (500+ cycles)
- Thermal Performance: Temperature retention testing comparing covered vs. uncovered bottles
- Visual Inspection: Surface defect screening, color consistency verification, edge finishing quality
Compliance Certifications
Our production facility maintains certifications and compliance documentation for major international markets, including material safety compliance for the US (CPSIA, Prop 65), European Union (REACH), and other regulated markets. We work with accredited third-party testing laboratories to provide certifications specific to each client's market requirements.
Market Trends Shaping the Leather Thermos Cover Industry
Several key trends are influencing product development and consumer preferences in the leather thermos cover segment:
- Sustainability Focus: Consumers increasingly prefer vegetable-tanned leathers, recycled insulation materials, and minimal-waste packaging. Brands that can communicate their environmental credentials gain competitive advantage.
- Personalization: Monogramming, custom color combinations, and made-to-order options are driving higher average selling prices and customer satisfaction.
- Multi-functionality: Covers that incorporate additional storage (for cards, keys, or small accessories) command premium pricing and receive higher customer reviews.
- Brand Collaborations: Partnerships between drinkware brands and fashion/accessory brands are creating limited-edition collections that generate significant buzz.
- E-commerce Optimization: Products designed with online retail in mind — photogenic aesthetics, compact shipping profiles, and gift-ready packaging — outperform traditional retail-only designs.
How to Get Started: Your OEM Development Process
Initiating a custom leather thermos cover project with an OEM manufacturer follows a structured process designed to minimize risk and maximize the likelihood of a successful product launch. Understanding each stage helps brands prepare effectively and set realistic timelines.
Step 1: Initial Inquiry and Consultation
The process begins with sharing your product concept, target market, estimated quantities, and budget range with potential manufacturers. At this stage, provide as much detail as possible — reference images, target bottle models, desired features, and brand positioning. This information enables the manufacturer to provide accurate pricing estimates and timeline projections. Reputable programme partners like Bespoke Bags offer free consultations and will ask clarifying questions to ensure they fully understand your requirements before providing a quotation.
Step 2: Sampling and Iteration
Once specifications are agreed upon and a deposit is placed, the manufacturer creates samples for your review. The sampling process typically involves two to three rounds. The first sample confirms overall construction, dimensions, and material feel. Subsequent rounds address refinements such as color adjustments, hardware preferences, closure mechanism improvements, and branding placement. Each sampling round takes approximately 7-14 days, and most projects reach final approval within three to four weeks.
Step 3: Production Planning and Bulk Manufacturing
After sample approval, production planning begins. The manufacturer schedules materials procurement, creates production patterns, and establishes quality benchmarks based on the approved sample. Bulk production follows the manufacturing process outlined earlier, with regular updates provided to the client throughout the production period.
Step 4: Quality Inspection and Shipping
Before shipment, clients typically have the option to conduct pre-shipment inspections — either personally, through a third-party inspection service, or via the manufacturer's own quality assurance team with photo and video documentation. Once approved, products are packaged according to specifications and prepared for international shipping. Our logistics coordination services handle all shipping arrangements, documentation, and customs clearance support to ensure smooth delivery to your destination.
Why Choose Bespoke Bags for Your Leather Thermos Cover OEM Program
With over 20 years of leather goods development experience, Bespoke Bags offers a combination of capabilities that make us an ideal manufacturing partner for leather thermos covers:
- Established Expertise: Operating since 2004, we bring two decades of leather craftsmanship to every product our production team develops
- Scale and Capacity: Our 4,950 m² production floor in Quanzhou supports high-volume production while maintaining artisan quality standards
- Flexible MOQ 500 pieces per style, we accommodate both emerging brands and established enterprises
- End-to-End Service: From initial design concept to global logistics, our wholesale and logistics services cover every step
- Material Access: Direct relationships with premium leather tanneries and material suppliers ensure consistent quality and competitive pricing
- Brand Protection: Strict confidentiality agreements, dedicated production lines for branded products, and secure IP protection protocols
Sizing Sprawl: Mapping a Cover Range to Real Bottle Geometry
A thermos cover programme almost never stays on one bottle. The shape that inspired the concept gets joined by two more before the line ships, and by then the pattern has to be reworked, another set of cutting dies ordered, and the closure position re-balanced. The cheapest moment to deal with that is before the first pattern is cut. We ask brands to write a dimensional matrix for the whole family they expect to carry over eighteen months, measured at three points per bottle rather than one, so a single internal standard governs every variant instead of six competing ones.
| Bottle family | Body diameter range | Height to shoulder | Internal ease we specify | Construction note |
|---|---|---|---|---|
| Slim can and 330 ml cooler | 64-67 mm | 115-125 mm | 2.0-2.5 mm | Straight wall; a pull-tab opener on the base helps the can leave the sleeve |
| Straight-wall tumbler, 20 oz | 70-73 mm | 140-150 mm | 2.0-2.5 mm | The reference shape; the base panel takes a concealed reinforcement disc |
| Tapered tumbler, 30 oz | Top 78-81 mm, base 69-72 mm | 180-195 mm | 2.5-3.0 mm tapered | Pattern is drafted on the taper, not parallel; the base seam carries the load |
| Wide-mouth bottle, 32 oz | 85-90 mm | 200-215 mm | 3.0-3.5 mm | Handle attaches to a load-bearing band rather than the shell itself |
| Sports bottle with concave grip | 72-76 mm at waist | 190-205 mm | 1.5-2.0 mm at waist | Negative ease at the waist keeps the sleeve from rotating in the hand |
| Insulated wine or olive-oil bottle | 78-84 mm | 290-320 mm | 3.0-4.0 mm | Long seams want a back panel; a base drawcord replaces a fixed closure |
Two practices keep that matrix honest. The first is to hold the physical bottles. We ask for two samples of every format — one to keep, one to send back with the development sample — because catalogue drawings omit the radius where the base meets the wall, and that radius is what decides whether the sleeve gathers or gapes. The second is to state the internal ease rather than the external measurement, since the insulation stack consumes space from the inside out. A neoprene layer that is 4 mm thick before compression does not stay 4 mm once the cover is sewn and turned.
- Measure every format yourself. Published dimensions describe the bottle, not the bottle plus the paint finish and the rubber boot some brands add later.
- Fix the closure position early. A magnetic snap set 12 mm lower changes how the mouth closes over a tapered shoulder.
- Decide the base treatment now. A bare leather base scuffs on stone worktops; a concealed disc costs pennies and removes that review complaint.
- Write tolerances into the tech pack. A stated ±1.5 mm acceptance band stops arguments at inspection about whether a cover fits.
Brands that work through this matrix usually find the range consolidates. Two patterns often cover what looked like five sizes, and the money saved on duplicate tooling funds better hardware elsewhere. Our custom design service supports that consolidation work, and the finished covers sit naturally alongside the rest of our leather accessories range.
Writing a Thermal and Durability Specification You Can Actually Test
"Keeps drinks cold for hours" is a marketing sentence, not a specification, and it gives you no recourse when a retailer asks what that means. A testable thermal clause has four parts: the starting temperature of the liquid, the ambient condition, the elapsed time, and the permitted loss. Write all four and you have something a laboratory — including ours, before we release a pre-production sample — can measure repeatably. Write two of them and every argument afterwards turns into an opinion.
| Clause | Typical written value | Why it matters |
|---|---|---|
| Fill temperature | 95 °C hot / 4 °C cold, ±1 °C | A 10 °C difference at the start moves the six-hour result more than any lining choice |
| Ambient condition | 22 °C ±2 °C, still air | Air movement across the shell is a bigger variable than the insulation stack |
| Elapsed interval | 1 h / 3 h / 6 h measurement points | Multiple points expose a slow leak that a single end-point check hides |
| Permitted loss | Hot: no more than 22 °C drop at 3 h; cold: no more than 9 °C rise at 6 h | The acceptance band, set at the point you are willing to defend to a retail buyer |
| Conditioning | 24 h at ambient before testing | Prevents the shell itself from absorbing or releasing heat during the run |
Durability deserves the same discipline, and it is where leather earns its keep. The exterior will be rubbed against bag linings, set down wet, and scraped past zips for years; a specification that only addresses temperature will pass while the product fails visually. We recommend pairing the thermal clause with abrasion, colourfastness and hydrolysis expectations written against the same numbers the market already uses — our quality control brief sets out how those checks are staged against AQL 2.5 under ISO 2859-1.
- Agree the target, not the test only. A rub test without a grey-scale rating leaves room for interpretation at the receiving dock.
- Test the finished cover, not the material. Skiving, folding and stitching all change how a hide behaves against abrasion.
- Run wet and dry cycles. Condensation is the normal condition for this product; a dry-only programme flatters the result.
- Keep golden-sample photographs. Every subsequent production run is judged against the approved unit, so before-and-after images are the cheapest reference you own.
It is worth adding a short clause about what happens when a result falls outside the band — who pays for the retest, whether a second round of samples is chargeable, and how long the buyer has to respond. Most disputes in this category are not technical; they are about silence on commercial mechanics. Clear writing at this stage keeps the relationship intact when a result goes the wrong way.
Failure Modes That Generate Returns — and How They Classify at AQL 2.5
Thermos covers are returned for reasons that have nothing to do with insulation. Condensation sits between the sleeve and the bottle, the leather darkens unevenly, the lining holds odour, and eventually the seam opens at the base where every owner pulls the bottle out. Each of those is a specification problem that shows up as a review problem. Mapping them onto defect classes before launch is what turns a fuzzy complaint into something the inspection plan can actually reject.
| Symptom in the field | Where it starts | Likely cause | Class at inspection | Specification response |
|---|---|---|---|---|
| Sleeve rotates or slips off | Waist or tapered shoulder | Uniform internal ease on a tapered body | Major | Specify tapered ease; add a negative-ease waist band |
| Base seam splits after repeated pulls | Base join under load | Insufficient reinforcement where the bottle exits | Major | Concealed reinforcement disc plus bar-tack across load lines |
| Lining holds odour | Interior after wet use | Closed-cell lining traps condensate | Minor to major by severity | Move to an open-cell or wicking lining with a stated dry-time |
| Uneven darkening of the leather | Panel exposed to hand contact | Absorption rate of a dry or lightly finished hide | Minor | Specify finish uptake and ask for a rub-resistant topcoat |
| Foil branding flakes at the fold | Logo over a stress line | Branding placed on a flex point | Major | Move the branding up from the closure line, or switch to debossing |
- A 500-piece lot inspected at AQL 2.5, ISO 2859-1, general level II, single sampling draws 50 units; three defects or fewer pass, four or more fail the lot.
- Critical failures — anything that makes the cover unsafe or unusable — are not traded off against an acceptance number; a single occurrence stops the release.
- Minor classifications still get counted. Persistent minor defects are how a product quietly loses its rating average.
- Defect definitions must be written before inspection day. Two inspectors reading the same brief should reach the same verdict on the same unit.
One practical point about boarding this early: our amendments take effect at the bulk stage, not the sample stage. Changes agreed after sample approval reset the schedule and, in the case of construction changes, the costed pattern. Defect definitions, though, cost nothing to write and can be updated as late as the pre-production review, which makes them the highest-leverage clause in the whole document.
Presentation Tiers, Carton Engineering and the Documentation Set
A thermos cover is frequently bought as a gift, and in gift channels the box decides the review as often as the leather does. Presentation also drives logistics: a rigid gift box doubles the volumetric weight of a shipment and changes how many units it is sensible to pack per carton. Choosing the tier early keeps the freight quote honest, and it determines whether the retail buyer sees something that belongs on a shelf or something that belongs in a warehouse.
| Presentation tier | Contents | Units per export carton | Best channel |
|---|---|---|---|
| Bulk poly bag | Individual sleeve, size label, barcode sticker | 120-200 | Promotional programmes, warehouse clubs, fulfilment prep |
| Printed sleeve band | Cover in a card band with brand artwork | 80-120 | Self-serve retail and counter displays |
| Rigid gift box | Two-piece board box, tissue wrap, care card | 24-40 | Department stores, brand boutiques, corporate gifting |
| Gift set configuration | Cover with a matching coaster or key fob | 12-20 | Executive gifting and seasonal programmes |
Two details decide whether the cartoning works. The first is that higher tiers are often nested rather than stacked, so the carton interior dimensions should be designed around the box, not around the cover. The second is labelling: carton marks, barcode placement and any country-of-origin marking belong in the specification rather than being worked out on the packing line. Export paperwork follows the same logic — our sleeves ship FOB Xiamen on T/T terms, 30% deposit and 70% before shipment, and the commercial documents are prepared against the carton list, so a change to that list on packing day costs you time at the port. The full sequence is set out in our export documentation guide.
- Confirm artwork deadlines against the sampling window, not the bulk window — packaging plates and boxes are ordered well before the covers are finished.
- Ask for a packed-carton photograph before shipment when using a new tier; it is the only record you will have of how the case was loaded.
- State the carton drop-test expectation in writing if your channel requires one; the requirement is cheap to meet and expensive to discover late.
- Keep one shipped carton aside per programme. It is your reference for the next reorder and for any damage claim.
Related Products and Services
Explore Our Capabilities
- → Leather Accessories — Discover our full range of custom leather accessories
- → Custom Collections — Build coordinated product lines for your brand
- → OEM/ODM Services — Full-service manufacturing from concept to delivery
- → Private Label Program — Your brand, our craftsmanship
- → Custom Design Services — Turn your vision into production-ready designs
- → Quality Control — Multi-point inspection ensuring consistent excellence
- → Small Batch Manufacturing — Flexible production for testing and niche markets
Frequently Asked Questions
What materials are used for custom leather thermos covers?
Custom leather thermos covers typically combine genuine leather (full-grain, top-grain, or vegetable-tanned) or premium PU leather with thermal insulation layers such as neoprene, EVA foam, or PE cotton. The outer layer provides aesthetic appeal and durability, while the inner insulation layer maintains beverage temperature. Some manufacturers also incorporate reflective aluminum layers for enhanced thermal retention.
What is the minimum order quantity for OEM leather thermos covers?
At Bespoke Bags, the MOQ is 500 pieces per style for leather bag-type products, and 500 pieces per style for small leather accessories. This MOQ accommodates both established brands launching new product lines and businesses testing new market segments.
How long does it take to manufacture custom leather bottle holders?
The standard production timeline for custom leather thermos covers is 25-35 days after sample approval. This includes material sourcing (7-10 days), cutting and assembly (10-15 days), quality inspection and finishing (5-7 days), and packaging (3-5 days). Rush orders can be accommodated with a 15-20 day timeline at an additional cost.
Can leather thermos covers be customized with brand logos and packaging?
Yes, full customization is available including embossed or debossed logos, laser engraving, custom hardware, branded zipper pulls, personalized color options, and custom packaging. Bespoke Bags offers comprehensive private label services, allowing brands to create completely unique thermos cover products that align with their brand identity.
What is the price range for custom leather thermos covers?
The pricing for custom leather thermos covers ranges from $3-19 per unit depending on material quality, design complexity, insulation specifications, and order quantity. Full-grain leather with premium insulation and complex construction typically falls in the $8-19 range, while PU leather with standard insulation starts from $3-6 per unit. Volume orders of 1,000+ pieces typically receive 10-20% cost reduction.
Whether you're launching a new accessory line, expanding your existing drinkware brand, or developing corporate gift programs, custom leather thermos covers offer an compelling combination of functionality, aesthetics, and profitability. With the right manufacturing partner, your brand can deliver premium quality products that resonate with consumers and drive sustainable growth.
Contact Bespoke Bags today at service@junyuanbags.com or WhatsApp +86 17750020688 to discuss your custom leather thermos cover project. Our team in Quanzhou, China, is ready to bring your vision to life with the quality and reliability that 20+ years of leather craftsmanship delivers.
Last Updated: August 14, 2026
How do we measure our own bottles so the cover actually fits?
Take the diameter at three points — base, waist and shoulder — rather than trusting a published figure, and note any rubber base or powder-coat finish that adds thickness. Then state the internal ease you want rather than the external dimension. Send two physical samples of each format with the brief: one is kept for measurement, the other returns with the development sample so you can judge the fit yourself.
Can one cover pattern be adapted across several bottle heights?
Yes, where the family shares a diameter. Straight-wall bodies of the same section can be graded by adding or removing length from the body panel, which costs a fraction of a new pattern. Where the taper differs, the section itself has to change and you are realistically drafting a second pattern rather than grading the first.
Which lining holds up best against daily condensation?
An open-cell lining that wicks and dries beats a closed-cell one for daily use, because condensation will sit inside the sleeve for hours regardless of how good the outer leather is. Brands routinely specify a stated dry-time in the brief. Where the cover will be used outdoors rather than at a desk, a micro-perforated lining trades a little insulation for far fewer odour complaints.
How much does a thicker insulation stack add to unit cost?
Insulation is usually the cheapest part of the build; the cost sits in the additional leather required to wrap it and in the labour of sewing a thicker stack. Moving from 3 mm to 5 mm neoprene typically changes material cost far less than it changes cutting size and cycle time, which is why we quote the two options side by side rather than quoting the insulation alone.
Can we put a thermal retention claim on the retail packaging?
Yes, provided the claim matches a written acceptance clause you can defend — starting temperature, ambient condition, interval and permitted loss. We test the pre-production sample against whatever clause you set and report the numbers, so the packaging artwork reflects a measurement rather than a hope. Ask your own counsel to review the wording for your market before it goes to print.
Should the cover be able to hang from a strap or carabiner?
It can, and it changes the load path. A strap loop or D-ring has to be anchored into a reinforcing band rather than stitched directly into the leather panel, because the bottle's weight is carried entirely through that point once it hangs. We usually specify the attachment with the first pattern rather than adding it later, since retrofitting reinforcement means reopening the seam.
What lead time should we plan for a first thermos cover order?
Sampling runs 6-10 working days, extending to 12-15 working days where custom hardware is involved, and bulk production takes 35-50 days after sample approval on the standard 500 pieces per style and colourway programme. Add freight from FOB Xiamen on top. For seasonal launches, plan backwards from the shelf date and leave two weeks of uncommitted buffer.
How many units should be packed per export carton?
It follows the presentation tier rather than the cover: bulk-packed sleeves go 120-200 to a carton, boxed gift runs 24-40. Cartons are also capped by weight for manual handling at the destination. Give us the tier and the destination handling rules and we will quote counts that survive both the freight bill and the warehouse.
Can a thermos cover sit alongside other accessories in one programme?
That is how most of these programmes grow. Coasters, key fobs and card holders cut from the same hide and branded with the same tooling make the range read as a family, and they share the 500 pieces per style and colourway requirement individually. Coordinating them in one brief means one set of colour approvals covers everything, which is usually where the real saving sits.