
A leather bag is made in nine sequential stages: design and pattern-making, material selection and sampling, cutting, skiving and preparation, assembly, hardware and lining attachment, edge finishing, inspection, and packing and dispatch. Each stage constrains the next — a pattern that is not worked out properly cannot be cut cleanly, and a panel that is not skived to the right thickness cannot be folded without bulk. The manufacturing process is therefore best understood as a chain of quality gates, not a single line.
This guide sets out the complete manufacturing process for leather bags as it runs on a modern production floor: what happens at each stage, how long each takes, which decisions remain reversible and which do not, and where quality is won or lost. It is written for brand owners, designers and sourcing managers who want to understand what they are commissioning rather than simply receiving.
Two framing points help before the stages. First, the process is broadly the same whether a programme runs at five hundred pieces or fifty thousand; what changes is the depth of documentation and the intensity of control. Second, leather is a natural material, so no two hides behave identically — the process is engineered to work with that variation rather than to pretend it away.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The Nine Stages of Leather Bag Manufacturing
The stages run in a fixed order because each depends on a decision made earlier. Cutting cannot begin before a pattern exists, and finishing cannot begin before the bag is fully assembled. Making the sequence explicit lets a brand see where its own input is required and where a delay in one stage pushes everything downstream.
| Stage | What happens | Typical duration | Quality gate |
|---|---|---|---|
| 1. Design and pattern-making | Silhouette, dimensions and construction translated into graded patterns and a tech pack | 5–15 working days | Pattern and specification approved before tooling |
| 2. Material selection and sampling | Leather, lining, thread and hardware chosen; a physical sample built | 6–10 working days | Signed sample becomes the reference |
| 3. Cutting | Hides assessed and panels cut by die or blade to the pattern | Hours to days per run | Panel dimension and hide-grade check |
| 4. Skiving and preparation | Edges thinned, panels creased and reinforced ahead of assembly | Hours per run | Thickness and fold-behaviour check |
| 5. Assembly | Panels, gussets and lining joined in sequence to build the bag | The largest labour block | In-process stitch and alignment checks |
| 6. Hardware and lining | Zips, locks, rings and plates set; interior fitted out | Hours per run | Component-by-part-number verification |
| 7. Edge finishing | Edges painted, burnished or bound and cured | Requires drying time | Uniform edge and cure check |
| 8. Inspection | Final inspection against the approved sample and specification | Sampling-based | AQL 2.5 under ISO 2859-1 |
| 9. Packing and dispatch | Stuffing, wrapping, cartoning and dispatch documentation | Days | Carton and packing-spec check |
The table shows why the early stages carry the highest leverage. A change made at design costs an afternoon; the same change discovered at stage five costs a partial run. This is the logic behind front-loading effort into specification and sampling rather than treating development as a formality to be cleared quickly.
Design, Pattern-Making and the Tech Pack
Design is where the bag exists only as intention. The work of this stage is to convert that intention into something a production floor can execute without interpretation: a set of patterns, a construction method and a written specification. A sketch alone is not enough, because a sketch does not state how thick the leather should be at a folded edge or where the seam allowance sits.
- A graded pattern set for every component, so panels fit together with defined seam allowances.
- A bill of materials naming each leather, lining, thread and hardware item by part code and finish.
- Construction notes that fix the assembly sequence and the stitch type at each seam.
- A dimension schedule with tolerances, so a measurement is either in or out of specification rather than 'close enough'.
- Branding placement marked on the pattern, whether that is a deboss, a foil stamp or a stitched label.
- A reference image or physical sample attached to the specification so intent is unambiguous.
A tech pack is the document that carries this information from design to the line. Where it is complete and unambiguous, sampling proceeds once and production repeats reliably; where it is thin, the sample stage is spent resolving questions that the specification should already have answered.
Material Selection and Sampling
Leather is chosen for how it will behave during making as much as for how it looks when finished. A hide that is beautiful but stretches unevenly will sag on a gusset; a hide that is firm enough to hold a structured silhouette may be too rigid for a soft tote. Material choice is a construction decision as well as an aesthetic one.
| Material | Typical use | Why it is selected | Constraint to plan for |
|---|---|---|---|
| Full-grain leather | Premium body panels and straps | Retains the surface grain; ages and patinas well | Limited cutting yield; visible natural marks |
| Top-grain leather | Everyday styles at accessible cost | Uniform surface after light finishing | Less patina and less breathability than full-grain |
| Suede or nubuck | Lining and soft bodies | Soft hand feel and warmth | Sensitive to moisture; needs protection |
| Microfibre lining | Durable interiors | Resists abrasion and cleans easily | Less luxurious feel than suede or leather |
| Coated canvas or nylon | Travel and utility formats | Light, water-resistant, hard-wearing | Different stitching behaviour to leather |
| Zinc-alloy and brass hardware | Zips, rings, buckles, feet | Strength and consistent plating | Plating must be matched across parts and batches |
Sampling converts the specification into a physical object and is the single most important approval point in the entire process. Sampling runs at 6–10 working days for most styles, extending to 12–15 for complex constructions with curled edges, multiple compartments or hard-shell elements. The sample is not a marketing mock-up; it is the reference that will be reproduced across the whole run, so it should be judged on construction as carefully as on appearance.
Cutting: Turning Hides into Panels
Cutting turns flat hides into the panels that will become a bag. The task is to extract the required panel set while respecting both the shape of the hide and its natural variation. Hides are not uniform rectangles: the neck is looser, the belly stretches, and the back is firmer and tighter. Where a panel lands on the hide changes how the finished bag behaves.
- Assess each hide and mark defects, scars and growth marks before cutting begins.
- Place structural panels such as gussets and body fronts on the firmest, most consistent areas of the hide.
- Nest patterns to reduce waste, since leather cost per bag is driven by how much of each hide is usable.
- Cut matching components for each bag from the same area of the same hide, so a finished pair cannot differ in grain or shade.
- Sort and label cut panels by set and by hide lot, so that parts for one bag stay together through assembly.
Cutting method matters to consistency. A clicker press produces panels that are dimensionally identical, which is why it is preferred for volume runs that need to match an approved sample. Hand cutting with a blade remains relevant for one-off pieces and for panels too large or too intricate for a die, but it introduces more operator judgment and therefore more variation.
Skiving and Preparation
Preparation is the stage buyers most often overlook and the one that most affects how a finished bag handles. Skiving reduces leather thickness at the edges that will be folded or joined, so that seams lie flat rather than bulking up. Preparation also covers creasing, reinforcing and backing, each of which stabilises a panel before it is assembled.
| Preparation step | Purpose | What it prevents if done well |
|---|---|---|
| Skiving | Thins edges and joints before folding and stitching | Bulky seams and uneven top lines |
| Reinforcing | Adds a stabilising layer behind a panel | Sagging, stretching and loss of shape |
| Creasing | Sets fold lines and decorative lines | Wandering, irregular folds |
| Edge folding and turning | Prepares a clean finished edge | Raw, untidy or inconsistent edges |
| Adhesive basting | Holds panels in position before stitching | Shift during stitching and misaligned seams |
| Component sorting | Groups parts by bag and by lot | Mixed-grain assemblies and error at the line |
Skiving thickness must be re-confirmed whenever the leather changes. A setting that suits a firm full-grain hide will thin a softer one too far and leave it weak at the fold. Because materials vary by lot, preparation is one of the stages where in-process checks carry real weight: an error here surfaces only later, usually as a tired-looking edge or a seam that pulls open with use.
Assembly: Bringing the Bag Together
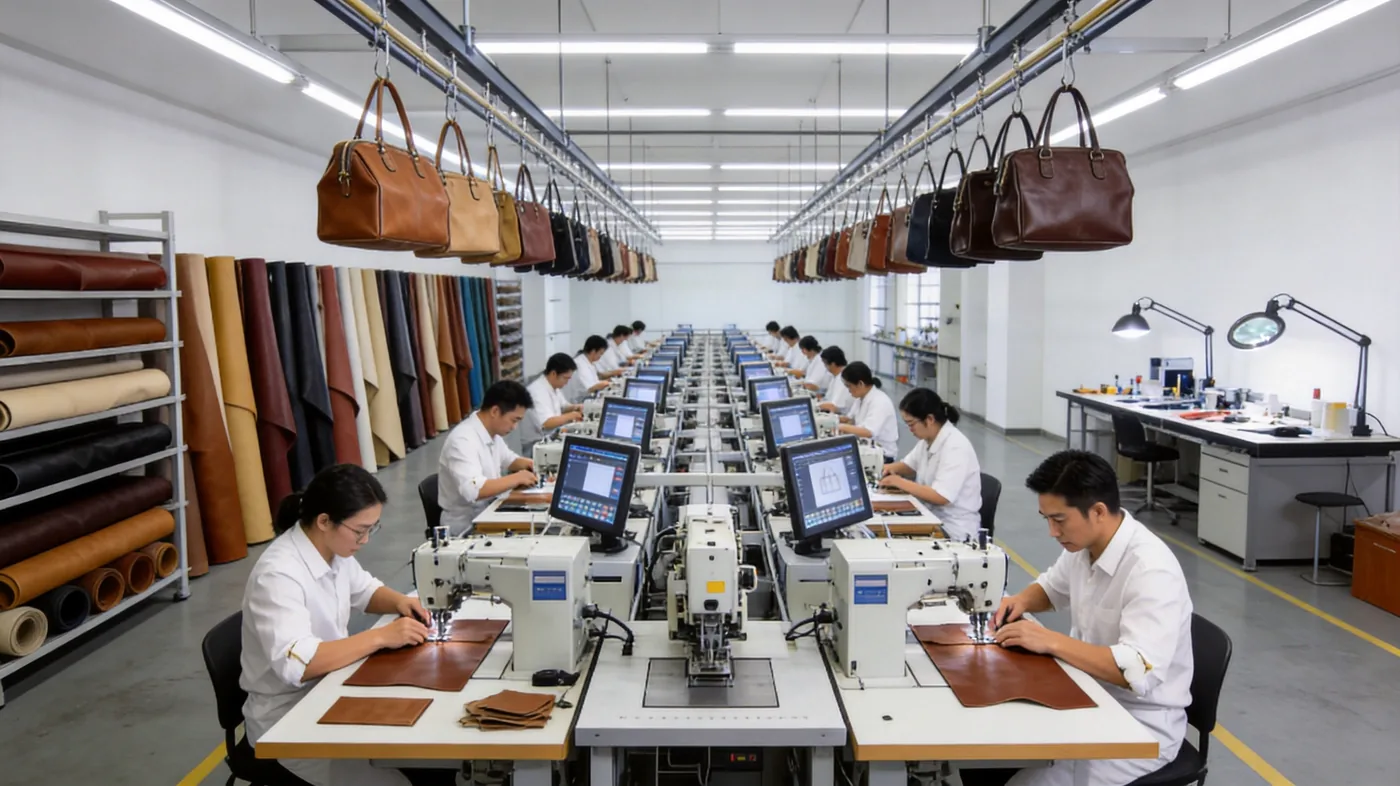
Assembly is the largest labour block in the process and the stage where the bag takes its final form. Panels, gussets, straps and lining are joined in a fixed sequence, working from the inside out so that unfinished seams and reinforcements are captured before the piece is closed. Sequence matters: an out-of-order assembly cannot be unstitched without leaving holes in the leather.
| Assembly stage | What is joined | Equipment | Control point |
|---|---|---|---|
| Sub-assembly | Straps, handles and any reinforced panels built as units | Flat-bed and post-bed stitching | Sub-assembly dimensions held before joining |
| Body assembly | Front, back and gussets joined to form the shell | Walking-foot machines | Stitch density and seam alignment |
| Lining attachment | Interior lining and pockets fitted | Flat-bed machines | Lining tension and pocket register |
| Closing and turning | Final seams closed and, where designed, the bag turned | Walking-foot and hand work | Seam integrity after turning |
| Hardware setting | Zips, locks, rings, plates and feet secured | Presses, setters and hand tools | Part-number and finish match |
Stitch density is agreed in specification and held through assembly, because it governs both strength and appearance. Too coarse and a seam is weak and visually loose; too fine and the leather can perforate along the stitch line and tear under load. Machines set for leather use a walking foot to feed material layers evenly, which is what keeps a long seam from drifting away from its reference line.
Hardware, Lining and Finishing
Hardware and finishing together decide how a bag feels in daily use. A zip that runs roughly, a plate that loses its plating or an interior that wears through in months will undo the impression created by a well-made exterior. These are the stages where the specification's detail pays off, because every component should already be named by part code and finish.
Edge finishing is slow because it is sequential: paint must dry between coats, and burnishing depends on friction and wax rather than on speed. Curing time cannot be compressed without cost to quality, which is why finishing often limits how quickly units can advance to inspection and packing even when assembly has kept pace.
Inspection, Packing and Dispatch
Inspection is the gate between making and shipping, and it works by sampling a population rather than checking every unit in fine detail. Final inspection runs at AQL 2.5 under ISO 2859-1, single sampling at general level II, with defect classes agreed beforehand so that 'major' and 'minor' mean the same thing to both parties. Pre-shipment inspection confirms the run matches the approved sample before goods leave the floor.
| Check | What it confirms | When it runs |
|---|---|---|
| First-article inspection | The first units match the full written specification | Start of the run |
| In-process inspection | Stitch, alignment and finish hold during production | At defined intervals |
| Final inspection | The population meets the agreed defect standard | AQL 2.5, ISO 2859-1 |
| Pre-shipment inspection | Quantity, specification, packing and labelling are correct | Before dispatch |
| Carton check | Packing protects the product and matches the agreed specification | At packing |
Packing is the final quality step rather than an afterthought. Bags are stuffed to hold their shape, wrapped to protect hardware and edges, and cartoned to the agreed count and configuration. Goods then move to dispatch, typically FOB Xiamen with EXW, CIF and DDP available on request, and payment on T/T — 30% deposit, balance before shipment. A complete process closes the loop: the bag that arrives matches the bag that was approved.
Understand the process before you commission it
Send your design, target quantity and launch date to service@junyuanbags.com, or message the programme team on WhatsApp at +86 177 5002 0688. We will map your programme against the manufacturing process and set out the sample, production and inspection stages for your bags.
Frequently Asked Questions
How long does it take to make a leather bag from start to finish?
Development and sampling take 6–10 working days for most styles, extending to 12–15 for complex constructions, and bulk production runs at 35–50 days after sample approval. Adding design and pattern-making ahead of sampling, the full journey from brief to delivered goods is typically measured in weeks rather than days, with the sampling and material stages the most variable.
What are the main stages of leather bag manufacturing?
There are nine: design and pattern-making, material selection and sampling, cutting, skiving and preparation, assembly, hardware and lining attachment, edge finishing, inspection, and packing and dispatch. The order is fixed, because each stage depends on decisions made earlier. Understanding the sequence lets a buyer see where their own input is required and where a delay pushes everything downstream.
What is the difference between cutting and skiving?
Cutting extracts the flat panels from a hide according to the pattern. Skiving then reduces the thickness of leather at the edges and joints that will be folded or joined, so that seams lie flat rather than bulking up. Cutting determines yield and shape; skiving determines how cleanly the bag folds and whether its top lines stay crisp with use.
Why is leather bag manufacturing described as a chain of quality gates?
Because each stage creates conditions the next stage can only partly correct. A poor cut cannot be rescued by good stitching, and a panel skived too thin will fail at the fold no matter how well it is assembled. Treating each stage as a gate — a point where the work either meets specification or is corrected — keeps problems from compounding into a finished bag that no later stage can fix.
How many pieces is the minimum for a leather bag production run?
The standard minimum stands at 500 pieces per style and colourway, with small-batch pilots available for brands validating a new format. The minimum applies per style and colourway rather than per programme, so widening a range multiplies the number of separate commitments rather than simply increasing unit volume. Many brands start with a pilot before committing to a full run.
What quality standard is used to inspect leather bags?
Final inspection runs at AQL 2.5 under ISO 2859-1, using single sampling at general level II. Defect classes are agreed beforehand, so that major and minor defects carry the same meaning for buyer and producer. Inspection works by sampling a population rather than checking every unit in exhaustive detail, and it is backed by first-article and in-process checks during the run.
How is the leather chosen for a bag?
Leather is selected for how it will behave during making as much as for how it looks. A hide must suit the construction: a structured silhouette needs a firmer hide that holds shape, while a soft tote suits a more pliable material. Full-grain, top-grain, suede and coated fabrics all carry different cutting yields, ageing behaviour and stitching characteristics, and the choice is matched to the style.
What happens during sampling?
Sampling converts the specification into a physical bag, built to the intended materials and construction. It is the reference that the whole production run will be reproduced against, so it is judged on construction and measurements as carefully as on appearance. Most samples are produced in 6–10 working days, and the signed sample is retained on the line during bulk so that finished units can be checked against it.
Can a leather bag be unstitched and remade if there is a mistake?
Largely no. Stitching leaves a row of holes in the leather, and while a seam can be undone, the original perforations remain visible and weaken the panel. This is why assembly sequence is fixed and why corrections must be made before stitching rather than after. It also explains why sampling — where errors cost a single bag — is so valuable compared with discovering the same fault mid-run.
Why does edge finishing take so long?
Because it is sequential and partly time-dependent. Edge paint is applied in several thin coats, each of which must dry before the next, and burnishing depends on friction and wax rather than on speed. Curing cannot be compressed without harming the finish, so although finishing occupies relatively little hands-on time, it sets a floor on how fast units can advance to inspection and packing.
How does leather cutting affect the cost of a bag?
Cutting determines how much of each hide becomes usable panels, and leather is priced by the hide rather than by the panel. Defects, scars and irregular hide shapes reduce the usable proportion, so nesting patterns well, placing structural panels on the firmest areas and cutting matched components from the same hide region all improve material economics. Yield measured on the sample should always be re-checked against the production lot.
What is hardware matching and why does it matter?
Hardware matching means drawing every zip, ring, lock, plate and foot from the same approved part number and plated finish. When components are permitted to drift — a zip from a different supplier, a ring in an unapproved tone — the finished bag looks assembled from mismatched parts. Naming each component by part code and finish is what keeps a run visually coherent and prevents silent substitution.
What is the difference between full-grain and top-grain leather?
Full-grain leather retains the original surface grain of the hide and ages with a patina, which is why it is used on premium body panels and straps. Top-grain leather has had the surface lightly buffed and finished to give a more uniform appearance at lower cost, with less patina and less breathability. Both are genuine leather; the choice is a trade-off between character and consistency.
When is a leather bag inspected?
Inspection runs at three levels. First-article inspection checks the first units off the line against the full specification. In-process inspection checks stitch, alignment and finish at defined intervals during the run. Final inspection applies AQL 2.5 under ISO 2859-1 to the population, and pre-shipment inspection confirms quantity, specification, packing and labelling before goods leave. Inspecting only at the end discovers problems after their cost is already sunk.
How are leather bags packed for shipment?
Bags are stuffed to hold their shape, wrapped to protect hardware and finished edges, and cartoned to the agreed count and configuration. Packing is treated as a final quality step rather than an afterthought, because a bag damaged in transit arrives as a defect regardless of how well it was made. Cartons are checked against the agreed packing specification before dispatch.
What incoterms and payment terms apply to leather bag manufacturing?
Goods typically ship FOB Xiamen as the default, with EXW, CIF and DDP available on request to suit different buyer preferences and logistics arrangements. Payment is on T/T — 30% deposit with the balance before shipment — which aligns the producer's material and labour costs with the buyer's commitment at each stage of the run.
Does the manufacturing process change at higher volumes?
The sequence does not change, but the depth of documentation and the intensity of control do. At sample volume, one experienced maker can hold the whole bag in mind; at scale, many people each perform part of the work, coordinated by specification rather than memory. Volume exchanges craft judgement for documented standard, which is why consistent specification and material lot control matter more as quantities rise.