
Skilled craft time in bespoke bag making typically runs from about 4 to 6 hours for a simple unlined tote to roughly 18 to 30 hours for a fully structured, hand-stitched handbag, with most mid-range styles sitting between 8 and 16 hours. Those hours are spread across cutting, skiving, stitching, edge finishing, hardware setting and final inspection rather than pooled into one operation. The range widens dramatically once hand saddle stitching, hand-painted edges or a complex lining are added.
The Short Answer on Hours Per Bag Style
There is no single number, because a bag is a stack of decisions rather than a fixed object. Two bags of identical silhouette can differ by a factor of three in craft time depending on the leather, the stitching method, the edge finish and the interior. The figures in this article are working estimates drawn from bespoke and small-batch practice, and they are best read as a planning guide rather than a quotation.
- Simple unlined tote or pouch: roughly 4 to 6 hours.
- Lined tote or shoulder bag with a pocket: roughly 7 to 10 hours.
- Structured handbag with hardware and a full lining: roughly 12 to 18 hours.
- Hand-stitched structured handbag with painted edges: roughly 18 to 30 hours.
- Large travel piece or holdall with reinforced handles: roughly 14 to 22 hours.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Why Hours Per Bag Style Vary So Widely
Four variables account for most of the spread. Change all four and a bag that takes five hours can take twenty. Understanding them is what allows a brand to plan a realistic timeline and a realistic cost rather than discovering the difference after the order is placed.
| Variable | Lower end of craft time | Upper end of craft time |
|---|---|---|
| Stitching method | Machine lockstitch throughout | Hand saddle stitch at visible and stressed seams |
| Edge finish | Single coat of edge paint | Layered paint, sanded and levelled, or hand burnished with wax |
| Interior | Unlined or a simple slip pocket | Full lining, zip pocket, card slots and a key leash |
| Structure | Soft, single-panel construction | Base board, interlining, reinforced gussets and a framed top |
| Hardware | Two fittings | Multiple fittings, each set with a dedicated die |
The compounding effect is what surprises buyers. Each choice is modest on its own, but they multiply rather than add, because a hand-stitched seam on a hand-painted edge on a fully lined, interlined body concentrates several slow operations on the same few centimetres of bag. That is why the difference between an entry-level line and a fine line is often felt most sharply in labour rather than in materials.
A Stage-by-Stage Time Breakdown
It helps to see where the hours actually sit. The table below shows how time typically distributes across a mid-range structured handbag of around fifteen craft hours. The pattern matters more than the exact figures, because it identifies which stages a brand can influence most directly.
| Stage | Share of craft hours | What drives the time |
|---|---|---|
| Cutting and preparation | About 10% | Nesting, grain matching and selecting clean areas of the hide |
| Skiving and assembling panels | About 15% | Thinning folds, joining panels and pre-shaping components |
| Stitching | About 30% | Seam length, stitch method and the number of separate runs |
| Edge finishing | About 15% | Number of coats, drying time between them and burnishing |
| Lining and interior | About 15% | Pockets, dividers and fitting the interior cleanly to the shell |
| Hardware and final assembly | About 10% | Setting each fitting and closing the bag |
| Final check and finishing | About 5% | Cleaning, trimming threads and inspection against the sample |
The biggest single block is stitching, and it is also the block most sensitive to method. A machine-sewn seam of one metre is a matter of seconds; the same seam hand-stitched with a saddle stitch may take close to an hour once marking, awling and two-needle work are counted. Edge finishing surprises people because its time is not all active; multiple thin coats require drying intervals, so the clock on an edge can run long even when hands-on work is brief.
Hours by Bag Style: A Reference Table
The figures below reflect a typical specification for each style at a quality level suited to a premium line. They assume a mix of machine and hand work, with hand stitching reserved for the visible and load-bearing seams. Where a style moves to full hand stitching or a hand-burnished edge, add several hours.
| Bag style | Typical craft hours | Time pressure points |
|---|---|---|
| Unlined tote | 4 to 6 | Minimal structure, few seams, simple edge treatment |
| Lined shoulder bag | 7 to 10 | Lining fit and interior pocket construction |
| Crossbody bag | 8 to 11 | Strap making, skiving and adjustable hardware |
| Structured handbag | 12 to 18 | Base board, interlining, framed top and multiple fittings |
| Hand-stitched handbag | 18 to 30 | Saddle stitching and layered, levelled edge paint |
| Holdall or travel bag | 14 to 22 | Reinforced handles, base and stress-point assembly |
| Fully hand-finished clutch | 10 to 16 | Frame fitting, fine edges and small-scale precision |
Two entries repay attention. The crossbody carries more time than its size suggests because a strap is a small piece of engineering, cut, skived, folded, stitched and fitted with an adjuster. The holdall carries less than its volume suggests, but its hours are concentrated in the handle roots and base, where reinforcement and multi-layer stitching consume far more time per square centimetre than the body panels.
Where the Hidden Hours Sit
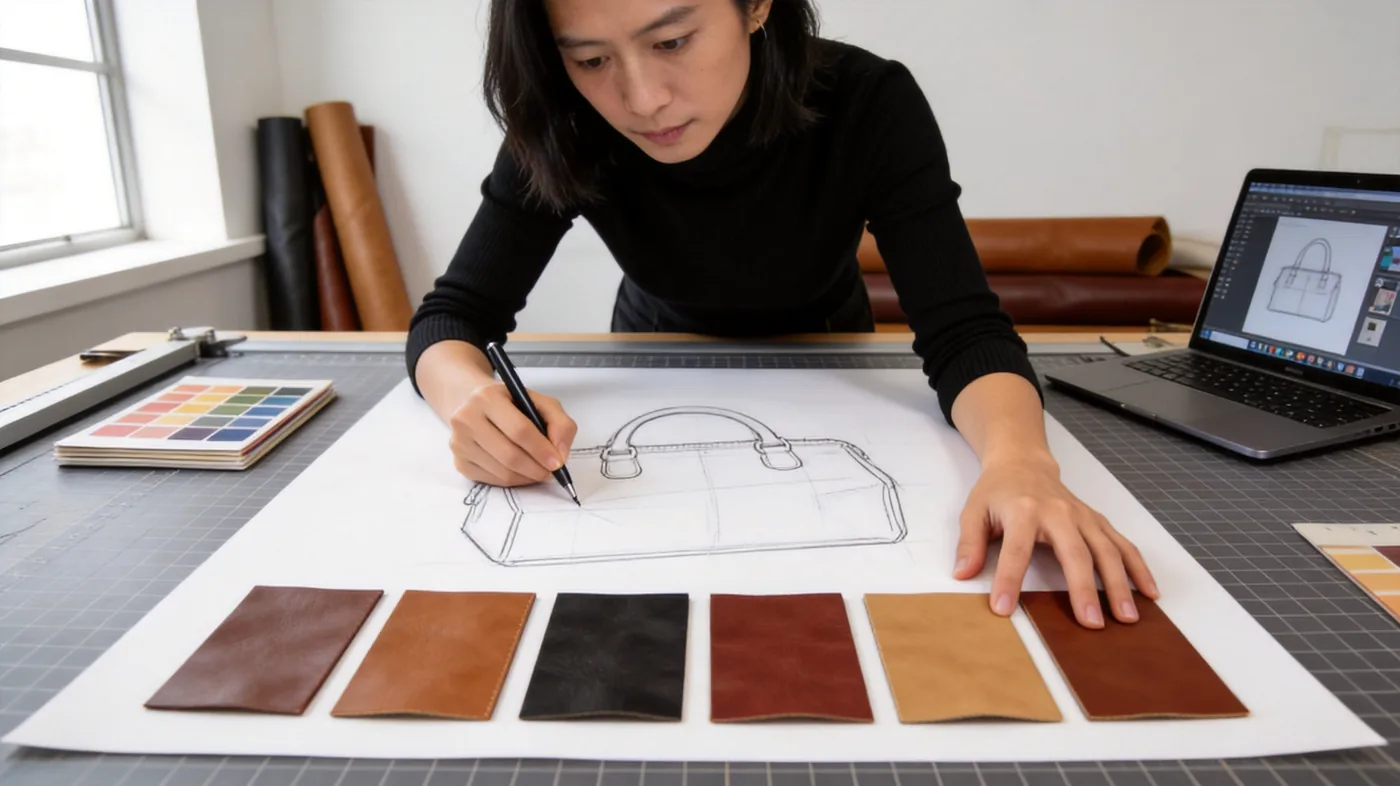
Not all craft time shows up as visible work. Some of the longest intervals are spent selecting, measuring and waiting, and a programme that ignores them will consistently underestimate a run. These are the hours that are easiest to miss on a bench visit and hardest to remove from a schedule.
- Selecting the hide: rejecting the scarred, stretched or discoloured areas and planning around them.
- Grain matching: cutting panels so that the texture runs consistently across the assembled bag.
- Drying between edge coats: several thin coats cannot be rushed without a poor finish.
- Thread and needle preparation: waxing, cutting to length and threading for each stitch run.
- Re-fitting during assembly: lining and hardware are often set, checked and adjusted more than once.
- Final inspection and touch-up: catching a flaw at the last stage and correcting it on the spot.
None of these operations looks like craft in the romantic sense, and none of them can be removed without cost. Grain matching is a good example: a hide has a grain that changes direction across its area, and a bag cut carelessly from it will show a visible break where two conflicting directions meet. The minutes spent planning the cut keep that from happening, and they are very hard to recover later.
Sampling Hours Versus Bulk Hours
Sampling is slower per unit than bulk production, and brands are frequently surprised by this. A sample is made as a one-off by a senior maker, working from a fresh pattern, solving problems for the first time and revising as they go. Bulk production repeats an approved construction many times, so the per-unit time falls even though the total craft content stays similar.
| Stage | Typical duration | Craft character |
|---|---|---|
| Sampling | 6 to 10 working days | One-off construction, first-time problem solving, revisions |
| Complex sampling | 12 to 15 working days | New construction, unusual hardware or an unframed shape |
| Bulk production | 35 to 50 days after approval | Repeated approved construction, shared setup, steady rhythm |
| Reorder | Typically shorter than a first run | Pattern and die already exist; the time sits in material and line scheduling |
The practical implication is that the sampling stage should be budgeted as its own effort rather than treated as a free preview of bulk. It is where the pattern is proven, the tolerances are set and the construction is solved. Cutting the sampling stage short to save time almost always returns the cost later, in bulk, when a fault that was never caught in the sample has to be corrected across hundreds of units.
Hand Work Versus Machine Work and the Time Difference
The gap between hand and machine work is real but narrower than folklore suggests, because machines also need setup, matching and checking. The question for a programme is where the extra hand time buys something a customer can see and feel, and where it does not.
| Operation | Machine time | Hand time | What the extra time buys |
|---|---|---|---|
| One metre of structural seam | Seconds per seam | Close to an hour hand saddle stitched | A seam that cannot unravel and a controllable stitch pitch |
| Edge finishing | Fast application of paint by roller | Multiple coats with drying, sanding and levelling | A deep, even edge that survives wear |
| Panel cutting | One strike per panel from a die | Hand cutting against a template for curves | Freedom of shape where no die exists yet |
| Hardware setting | Press at a fixed depth, repeated rapidly | Setter and maul, judged by feel | Adjustment on the spot for delicate surfaces |
A well-run programme does not treat this as a moral question. It places hand work where it shows, at the handle roots, the top edge and any seam a customer will hold, and it lets machines handle the long interior seams where consistency across thousands of units matters more than an individual stitch. The result is a bag that reads as hand-made where it counts and holds a reliable standard everywhere else. Our production floor in Quanzhou schedules the hand operations as distinct steps so that the craft time is visible in the plan rather than hidden inside a lump sum.
Planning a Programme Around Craft Hours
Once craft hours are understood as a set of choices rather than a mystery, they can be planned like any other input. The table below sets out the working parameters a brand should hold when it maps craft time onto a launch schedule.
Craft hours are ultimately a language for talking about value. When a brand asks for eighteen hours of hand work, it is not buying time for its own sake; it is choosing a construction, a finish and a feel that a cheaper build cannot reproduce. The useful discipline is to spend the hours deliberately and to know, before the order is placed, exactly where they are going. Related hand and machine techniques are set out across the leather craftsmanship techniques pillar.
Price the hours you actually want
Send the styles, the craft level and the launch date. The programme team will map the craft hours per style, confirm the sample and bulk timeline, and return a plan that shows where the hand work goes before a single unit is cut.
Frequently Asked Questions
How many hours does it take to make a bespoke bag?
It depends on the style and the craft level. A simple unlined tote runs roughly 4 to 6 hours, a lined shoulder bag 7 to 10 hours, a structured handbag 12 to 18 hours, and a fully hand-stitched handbag with hand-painted edges 18 to 30 hours. These are working estimates drawn from bespoke and small-batch practice rather than fixed figures, and each choice of method moves the number.
Why does a hand-stitched bag take so much longer?
Saddle stitching is done a hole at a time with two needles, so one metre of visible seam can take close to an hour once marking the pitch, awling the holes and drawing the thread are counted. A machine sews the same seam in seconds because it operates continuously. The extra time buys a seam that cannot unravel and a stitch pitch the maker controls deliberately rather than a fixed setting.
Does a bigger bag always take longer to make?
Not proportionally. A large holdall can take less time than a small, highly structured handbag, because craft hours concentrate at details rather than in surface area. A structured handbag carries a base board, interlining, a framed top and multiple fittings, all slow operations on a small object. A large soft holdall spends its hours mainly at the handle roots, the base and the reinforcement.
How long does the sampling stage take before bulk production?
Standard sampling runs 6 to 10 working days, extending to 12 to 15 working days for complex constructions such as an unframed shape or unusual hardware. Sampling is slower per unit than bulk because a senior maker is solving the construction for the first time and revising as they go. Bulk production then follows 35 to 50 days after sample approval.
Which stage of bag making takes the most time?
Stitching is typically the largest single block, at roughly 30 per cent of craft hours on a structured handbag, because seam length, stitch method and the number of separate runs all accumulate. Edge finishing, lining and interior work each take about 15 per cent, and the remaining time spreads across cutting, skiving, hardware setting and the final check.
How long does edge finishing add to a bag?
Edge finishing accounts for roughly 15 per cent of craft hours on a structured bag, and its time is not all hands-on. Multiple thin coats of paint must dry between applications, and a hand-burnished edge is worked with heat, wax and friction until the fibre seals. A single coat is quick; a deep, even, layered finish built up coat by coat takes considerably longer.
Is a machine-made bag faster to produce than a handmade one?
Faster per operation, yes, but the difference is narrower than people assume once setup, matching and checking are counted. A machine reduces a seam to seconds and repeats a hardware set at a fixed depth, yet the leather still has to be selected, matched and assembled around it. The choice is usually about where hand work shows, not about replacing craft wholesale.
How long does a reorder take compared with a first order?
A reorder is typically faster than a first run because the pattern, dies and construction are already proven and approved. The remaining time sits in material procurement and line scheduling rather than in development. It still follows the same bulk window of 35 to 50 days, but without the sampling stage and the problem solving that a new style requires.
Do craft hours include drying time?
They should, and a plan that ignores them will run late. Edge coats, adhesive lines and any wet finishing stage need intervals before the next operation. Some of the longest stretches of a bag's production are drying periods rather than active work. A realistic schedule builds these intervals in rather than treating them as slack that can be absorbed elsewhere.
How many bags can a craftsperson make in a day?
It depends entirely on the style. A maker working on simple unlined totes might complete several in a day, while a single hand-stitched structured handbag at twenty or more craft hours can occupy the same maker for close to three working days. This is why the unit of planning in bespoke work is the style rather than the maker, since the hours per unit vary so widely.
Can craft hours be reduced without losing quality?
Some can, and sensibly. Moving a long interior seam to a machine, or simplifying the interior from several pockets to one, removes hours without touching the parts a customer feels most. What cannot be reduced without cost is the hand work on visible seams, load-bearing handle roots and well-finished edges, because those are precisely the areas where the hours are the quality.
How do I decide how many craft hours my style needs?
Start from the customer's experience rather than the clock. Decide where hand stitching and hand finishing will be visible, how the bag will be used and how long it needs to last, then let those answers set the hours. A programme can then show the craft time per style and confirm the sample and bulk timeline before the order is placed, so the choice is deliberate rather than assumed.
Is hand-painted edge finishing worth the extra time?
It depends on the positioning of the line. Hand-layered paint gives a deep, even edge that resists wear far better than a single quick coat, and it is one of the details a discerning buyer notices first. For an entry line a simpler finish may be the right call, but for a premium handbag the extra edge hours are usually the difference between a bag that ages well and one that does not.
How does lining complexity affect craft time?
Lining and interior work generally account for about 15 per cent of craft hours on a structured bag, but that share rises quickly with complexity. A single slip pocket is a short operation; a full lining with a zip pocket, card slots and a key leash is a sequence of small, precisely fitted components that must sit cleanly inside a finished shell. Each added feature carries its own construction time.
Where does craft time concentrate most in a travel bag?
In the handles, the base and the stress points rather than the body panels. A holdall spends a disproportionate share of its hours at the handle roots, where reinforcement and multi-layer stitching consume far more time per square centimetre, and at the base, which typically needs a reinforced or boarded construction. The large body panels are often the quickest part of the build.