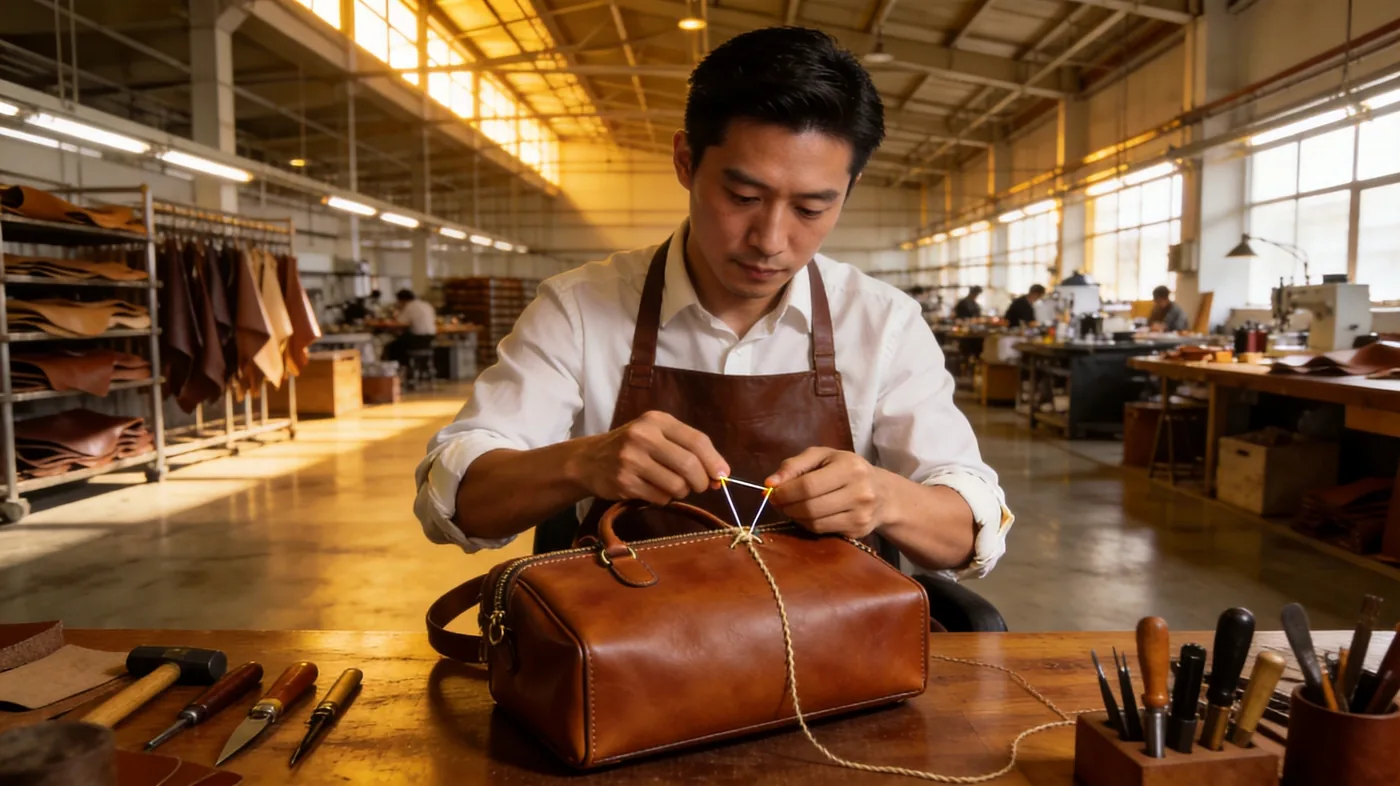
Leather sewing machines differ from textile machines chiefly in feed, needle and drive: most use a walking-foot or compound feed that moves the material from above and below at once, they take leather-point needles that cut a clean hole rather than pierce and split, and they run slowly with high torque to push thick, layered work through. On a bespoke bag the result is straighter seams, fewer skipped stitches and edges that stay even, which is why the machine class chosen at the sampling stage shapes the finish of every unit that follows.
The confusion is understandable, because at a glance a leather machine and a garment machine look alike: a needle, a presser foot, a bed and a handwheel. The difference is in how the material is transported and how the stitch is formed where several millimetres of hide and lining meet. A textile machine is built to move thin, flexible cloth at speed; a leather machine is built to move thick, dense, low-friction material at controlled pace without the plies slipping against one another.
This guide is written for brand owners, designers and sourcing managers who specify bags rather than operate machines, but who need to understand why two stitching lines can produce very different results from the same pattern. The stakes are commercial: stitching defects are among the most visible and most rejecting faults in a bespoke bag, and most of them trace back to the machine, the needle or the setup rather than to operator care.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Three subsystems do the differentiating work, and it helps to name them before examining any of them in detail. The feed system decides how the material moves and whether the layers stay aligned. The needle and thread decide how the stitch forms and how strong the seam is. The drivetrain decides how slowly and how forcefully the machine can push a thick assembly through. Everything else, from bed shape to bobbin capacity, is a refinement of those three.
What Makes a Leather Machine Different
The defining difference is friction. Woven cloth grips itself and the machine's feed dogs, so a drop feed that pushes from below is enough. Leather and thick synthetics are slick and often laminated, so the top ply can shift forward or lag behind while the bottom ply is being pulled. A standard drop feed advances only the layer it can grip, which is why thin-machine stitching on leather so often opens into wavy, mismatched seams at the end of a run.
| Property | Textile machine | Leather machine | Why it matters |
|---|---|---|---|
| Feed | Drop feed from below | Walking foot / compound feed | Keeps thick plies aligned |
| Needle | Round or sharp point | Leather point (wedge or twist) | Clean hole, less splitting |
| Speed | High, often 3,000+ spm | Low, often 500–1,500 spm | Control over thick work |
| Torque | Moderate | High, gear-reduced | Pushes layered leather through |
| Presser lift | Modest | High, for thick stacks | Clears layered assemblies |
| Stitch length | Short | Long, up to 8–10 mm | Suits visible topstitch |
| Bobbin | Standard | Large M-size | Fewer changes on long seams |
Each row is a consequence of the material rather than a marketing choice. The slow speed is not a limitation but a feature: at walking pace the operator can steer a curved seam and keep the edge even, which is impossible at garment-line speeds on thick leather. The large bobbin exists because a long topstitch run with heavy thread exhausts a small bobbin quickly, and a mid-seam change leaves a visible mark.

The Feed System: Walking Foot and Compound Feed
A walking-foot or compound-feed machine has an upper foot that moves in time with the needle and the lower feed dog, so the material is advanced from above and below simultaneously. This is the single most important feature on a leather machine. Because the top and bottom of the assembly are driven together, the plies do not slip, and the seam stays straight and even from the first stitch to the last.
There are several feed arrangements, and they differ in how much control they give. A true triple feed, sometimes called unison feed, drives the needle, the walking foot and the feed dog together, which is the highest level of control and the standard on serious leather machines. A needle feed alone moves the needle bar forward and back with the material but leaves the presser foot static. A puller, added after the needle, draws the work steadily and helps on very long, straight runs.
- Triple feed (unison): needle, walking foot and feed dog move together; best control on thick, layered work.
- Walking foot only: upper foot and feed dog move; common and effective for most bag leathers.
- Needle feed: needle bar advances material; useful on slick or coated leathers where skipping is a risk.
- Drop feed: feed dog only; found on light machines, poor at holding thick plies aligned.
- Puller attachment: external roller draws work after the needle; reduces drag on long straight seams.
- Roller feed: a single roller replaces the foot; suited to curved or small-radius work.
The practical effect of a good feed system is visible at the end of a seam, not the middle. On a sliding-feed machine a thick seam will drift, the layers will fan apart and the topstitch line will wobble. On a walking-foot machine the same seam closes flat and even. For a structured bag where several panels meet at a corner, that difference decides whether the assembly sits square or skews.
| Feed type | Best for | Weakness |
|---|---|---|
| Triple feed (unison) | Thick multi-layer assemblies, topstitching | Higher machine cost and complexity |
| Walking foot | General bag leather and coated canvas | Less control than full unison on thick work |
| Needle feed | Slick, coated or laminated leathers | Limited on very thick stacks |
| Drop feed | Light linings and thin seams | Ply slippage on thick or slick material |
| Puller assisted | Long straight runs on heavy material | Needs tuning; can stretch soft leather |
Bed Types: Flat, Cylinder and Post
The bed is the surface the material rests on and the shape of the machine beneath the needle. It determines what geometry the machine can sew. A flat-bed machine has a horizontal surface, which suits flat panels and long, straight seams. A cylinder-bed machine narrows to a tube, which lets a tube-shaped or assembled bag be rotated over it. A post-bed machine raises the work area on a vertical column, which brings the needle into tight corners and around curved gussets.
Most production lines run a mix. Flat beds handle the large body panels, gusset seams and long runs. Cylinder beds take assembled or partly assembled bags where the work has to pass over a tube. Post beds reach into the ends of a tote, the corners of a structured bag and detailed areas near a curve. Matching the machine to the job is what keeps the seam following the pattern rather than the pattern bending to the machine.
| Bed type | Shape | Typical bag work | Limitation |
|---|---|---|---|
| Flat bed | Horizontal surface | Panel joins, topstitching, long seams | Cannot pass a closed tube |
| Cylinder bed | Narrow tube arm | Assembled bags, gusset runs, curved seams | Limited access near ends |
| Post bed | Raised vertical column | Tight corners, small-radius curves, end seams | Small work area; slower |
| Long arm | Extended flat bed | Large panels, travel and luggage | Still cannot pass a tube |
For a brand, the bed question shows up in whether a design is buildable as drawn. A seam that can only be reached with a post bed is possible, but it may be slow and costly if the line has to divert the piece. Discussing bed access at the sampling stage is cheaper than discovering a difficult corner after the pattern is frozen and the panels are cut.
Needles for Leather: Point Geometry Matters
A needle is not a universal tool. Textile needles have a round or sharp point that pushes between the fibres of a woven material; a leather needle has a cutting point that makes a clean hole so the thread can pass without tearing the hide. Using the wrong point on leather causes skipped stitches, a ragged needle hole and, over time, a seam that weakens because the perforations join up.
The main leather points are the wedge point, a triangular blade that cuts a crisp slit, and the twist point, which cuts at an angle and suits dense or coated material. The needle system and size must also match the machine and the thread: too fine a needle for the thread will fray the thread and skip, too coarse a needle for the material will leave needle holes that show on the finished bag.
- Wedge point: cuts a clean straight slit; good for softer and medium leathers.
- Twist point: angled cut; suits dense, firm or coated leathers and many synthetics.
- Leather-point round blade: cuts without tearing; used where fibre damage must be minimal.
- Needle size must match thread weight; mismatch causes skipping and thread damage.
- Replace needles on a schedule, not when they fail; a dull point tears and marks.
- A blunt needle leaves needle holes that remain visible after the seam settles.
Needle choice also interacts with stitch appearance. Because a leather-point needle cuts the material, the hole does not close behind the thread the way it does in woven cloth. That is why visible topstitching on leather tends to sit slightly proud, and why the point geometry and the needle size have to be right: a hole that is too large shows around the thread, and a hole made with a torn point frays at the edges.
Thread, Tension and Stitch Formation
Leather stitching usually uses a lockstitch, where the needle thread and the bobbin thread interlock in the middle of the material. For strength, the thread is typically bonded nylon or bonded polyester, both of which resist abrasion and hold tension better than soft garment thread. Bonded thread is stiff and does not flatten under the foot, which helps the stitch stay even across a thick assembly.
Tension is the balance between the needle thread and the bobbin thread. The knot of a lockstitch should sit in the middle of the material, hidden, with the two threads pulling evenly against each other. If the top tension is too tight the bobbin thread is pulled up and a loop shows on the underside; if it is too loose the needle thread shows on top. On leather this is especially visible, because the dense surface holds the thread where it lands.
| Symptom | Likely cause | Adjustment |
|---|---|---|
| Loops on the underside | Top tension too tight | Reduce upper tension |
| Needle thread visible on top | Top tension too loose | Increase upper tension |
| Skipped stitches | Wrong needle, wrong size, timing | Match needle to thread; check timing |
| Thread fraying or breaking | Too fine a needle, rough eye, heat | Larger needle, replace needle, slow down |
| Wavy seam | Feed and pull unbalanced | Adjust foot pressure and feed timing |
| Puckered seam | Too much tension, too small stitch | Relax tension; lengthen stitch |
Stitch length is set longer on leather than on cloth, often in the range of four to eight millimetres for a visible topstitch, because a long, even stitch reads as deliberate on a leather surface and because a very short stitch perforates the material more densely, weakening the seam line over time. The chosen stitch length becomes part of the design: it should be specified in the technical pack, not left to the operator for the day.
A lockstitch is judged by what you cannot see. If the knot is buried in the middle of the leather, the two threads are working together; if you can find it on either face, one of them is doing all the work.
Machine Classes and What They Cost
Leather machines fall into rough classes by capacity and construction. A light walking-foot machine suits thin leathers, coated canvas and linings. A medium compound-feed machine handles most bag leathers and is the workhorse of a bag line. A heavy harness or stitcher-class machine pushes through thick multi-layer assemblies and long, heavy straps. Each class costs more than the last, in machine price, in space and often in the skill needed to run it well.
For a brand specifying production, the class of machine is a proxy for capability. If a design calls for a thick, folded, multi-layer seam at the handle root and the line only runs light machines, the seam will either fail or be stitched in a way the design did not intend. Matching the design to the machine class is a sourcing decision, and it belongs in the brief alongside the material and the construction.
| Class | Typical capacity | Bag work | Trade-off |
|---|---|---|---|
| Light walking foot | Thin leather, coated canvas | Linings, flat panels, light topstitch | Cannot handle thick stacks |
| Medium compound feed | Most bag leathers | Body panels, gussets, topstitching | Slower than garment machines |
| Heavy harness / stitcher | Thick multi-layer work | Handles, straps, structured bases | Costly; needs skilled operation |
| Cylinder bed | Assembled work | Gusset runs, curved seams | Restricted access at ends |
| Post bed | Tight geometry | Corners, end seams, small curves | Small work area, slow |
| Long arm | Large panels | Travel bags, luggage, large totes | Large footprint |
Setup cost is a second factor. Dies, guides, folders and special feet are often specific to a seam or a shape, and a line set up for one programme may need new attachments for another. Where a brand expects reorders, those attachments become an asset that keeps the seam consistent across seasons, in the same way a cutting die does. It is worth asking early which setups will be shared and which will be dedicated.
Setting Up and Maintaining a Stitching Line
Machine capability is only half of stitch quality; setup and maintenance are the other half. A correctly classed machine that is out of time, fitted with a blunt needle or set to the wrong tension will produce worse work than a humbler machine that is well maintained. The routine matters more than the badge on the machine, and it is one of the first things a quality audit should inspect.
- Needles replaced on a set schedule, not only on failure.
- Timing checked so the needle meets the hook at the correct point.
- Tension set for the thread and material in use, and rechecked after changes.
- Presser foot pressure matched to the material thickness.
- Bobbin wound evenly to avoid tension variation mid-seam.
- Machine cleaned of lint and adhesive build-up between runs.
- Feed timing and foot height checked after any service.
Where a programme is inspected to AQL 2.5 under ISO 2859-1, single sampling at general level II, stitching is one of the fault classes that most often drives a reject. That points to where the effort should go: not merely at final inspection, but at the machine and the setup, because a fault that begins as a skipped stitch at the needle is already a defect by the time an inspector sees it.
Specifying Stitching for Your Bags
The stitching specification belongs in the technical pack, and it should be specific enough that a different line could reproduce the intended look. It should state the thread type and weight, the stitch length and type, the seam allowance, the needle point for the material, the tension target described as the knot position, and which seams are visible topstitch and which are concealed. Ambiguity here is what produces a reorder that does not match the first run.
| Specification line | What to state | Why it matters |
|---|---|---|
| Thread | Type and weight | Controls strength and look |
| Stitch type | Lockstitch or other | Determines how the seam behaves |
| Stitch length | Millimetres per stitch | Visible design feature |
| Needle point | Wedge or twist, size | Prevents tearing and marking |
| Seam allowance | Distance from edge | Keeps panels aligned |
| Tension target | Knot position in the material | Prevents surface loops |
| Stress points | Extra stitching or reinforcement | Handle roots, strap anchors |
It is worth naming the stress points explicitly. Handle roots, strap anchors and any seam that carries load usually take back-stitching, a bar tack or a second row, and the machine has to be capable of stitching that reinforced section cleanly, which often means the heaviest seam in the bag, not the lightest. The stitching spec should identify those points so the machine class is chosen around them.
The programme team can translate a design into a stitching specification that names the machine class, the feed arrangement, the needle and thread, and the appearance of the intended seam, then verify it on samples before bulk. Getting that right at the sampling stage keeps stitch quality consistent across a run and, just as importantly, across reorders, so a customer who returns a year later finds the same seam they bought first time.
Specify the stitch, not just the look
Share your design and the seams that matter most. The programme team will advise on machine class, feed arrangement, needle and thread, and set a stitching specification that holds across the run and the reorder.
Frequently Asked Questions
What makes a leather sewing machine different from a normal sewing machine?
The main differences are the feed, the needle and the drive. Leather machines use a walking foot or compound feed that moves the material from above and below together, so thick plies stay aligned. They take leather-point needles that cut a clean hole rather than split the hide, and they run slowly with high torque to push dense, layered work through without slipping.
Why do leather sewing machines use a walking foot?
Leather is slick and often laminated, so a drop feed that pushes only from below lets the top ply shift or lag. A walking foot moves the top ply in step with the feed dog underneath, so the whole assembly advances together. This keeps seams straight and even and prevents the layers from fanning apart at the end of a long run.
What needle should be used for sewing leather bags?
Leather work normally uses a leather-point needle, either a wedge point that cuts a clean straight slit or a twist point for dense, firm or coated material. The needle size must match the thread weight, because too fine a needle frays the thread and skips, while too coarse a needle leaves visible holes on the finished bag.
What thread is best for leather bag stitching?
Bonded nylon or bonded polyester thread is standard for leather bags. Bonded thread resists abrasion, holds tension well and does not flatten under the presser foot, which keeps the stitch even across thick assemblies. The thread weight is chosen to match the needle and the strength the seam needs at load-bearing points.
Why does my lockstitch show loops on the underside?
Loops on the underside usually mean the upper tension is too tight, so the bobbin thread is pulled up to the surface. The remedy is to reduce upper tension until the interlock knot sits buried in the middle of the material. If the needle thread instead shows on top, the upper tension is too loose and should be increased.
What is a compound feed machine?
A compound feed machine advances the material using both an upper walking foot and a lower feed dog moving together. A true triple feed, also called unison feed, also drives the needle bar forward and back with the material. Compound and triple feeds give the highest level of control on thick, layered leather assemblies.
What is the difference between a flat-bed, cylinder-bed and post-bed machine?
A flat bed is a horizontal surface for flat panels and long seams. A cylinder bed narrows to a tube so an assembled or tube-shaped bag can rotate over it. A post bed raises the work area on a column to reach tight corners, end seams and small-radius curves. Most leather lines use a mix of all three.
How long should the stitch length be on a leather bag?
Stitch length is set longer on leather than on cloth, commonly about four to eight millimetres for a visible topstitch. A long, even stitch reads as deliberate on leather and perforates the material less densely than a short one, which helps seam strength over time. The chosen length should be specified in the technical pack.
Why does the machine skip stitches on thick leather?
Skipped stitches usually come from a needle that is too fine for the thread, a dull or wrongly pointed needle, incorrect needle-to-hook timing, or too little pressure on a thick stack. On leather the fix is normally to match needle size to thread weight, replace the needle, and check the timing, rather than to increase speed or force.
Do leather sewing machines run slower than textile machines?
Yes, and deliberately. Garment machines can run above three thousand stitches per minute, while leather machines often run between about five hundred and one thousand five hundred. The slower speed gives the operator time to steer a curved seam and keep the edge even, which is impossible at garment-line speeds on thick leather.
Can a normal domestic sewing machine sew leather bags?
A domestic machine can handle thin leather for small items but struggles with bag-weight material. It typically has a drop feed that lets thick plies slip, limited presser lift, low torque and a small bobbin. For a bespoke bag with layered seams and long topstitch runs, an industrial walking-foot machine is the realistic tool.
What causes puckered seams on leather?
Puckering usually comes from excessive thread tension or a stitch that is too short for the material, which pulls the leather together along the seam line. It can also result from feed and pull being unbalanced. Relaxing the tension and lengthening the stitch generally resolve it, since leather does not spring back the way woven cloth does.
Why is a large bobbin important on a leather machine?
A long, heavy topstitch seam using thick thread uses a lot of bobbin thread quickly. A small bobbin forces frequent changes, and each change risks a visible interruption in the stitch line. A large M-size bobbin lets the operator complete a long seam in one pass, which keeps the topstitch continuous and even.
How is stitch quality checked in production?
Stitch quality is checked by looking for a buried interlock knot, even stitch length, no skipped stitches and no surface loops on either face. On programmes inspected to AQL 2.5 under ISO 2859-1, single sampling at general level II, stitching is one of the fault classes most likely to drive a reject, so it is monitored closely.
What is the best machine for stitching handles and straps?
Handles and straps are usually the heaviest seams in a bag, sometimes several layers thick at the root. They call for a heavy harness or stitcher-class machine with high presser lift and strong torque, and often a cylinder bed to reach the assembled handle attachment. Choosing the machine class around these seams, not the lightest one, prevents failure at load points.
How does leather-point needle geometry affect the finished bag?
Because a leather-point needle cuts the material, the hole does not close behind the thread as it does in woven cloth, so the stitch sits slightly proud. The point geometry and needle size must be right: too large a hole shows around the thread, and a torn point frays the edge. This is why needle choice is part of the seam's appearance, not only its strength.
What maintenance keeps a stitching line consistent?
Consistency comes from routine: replacing needles on a schedule rather than on failure, checking needle-to-hook timing, setting tension for the thread in use, matching presser-foot pressure to material thickness, winding bobbins evenly and cleaning lint and adhesive build-up between runs. Setup and maintenance often matter more to stitch quality than the machine's badge.
Can the same machine sew different leather thicknesses?
Within limits, yes, by adjusting presser-foot pressure, stitch length and tension. But a very light machine cannot cleanly push a thick multi-layer seam, and a heavy stitcher handles thin linings poorly. Programmes usually match machine class to the thickest seam in the design and use lighter machines for linings and flat panels.
How long does production take once stitching is specified?
Sampling normally takes six to ten working days, or twelve to fifteen for complex constructions, and this is when the stitching specification is proven on real material. Bulk production follows sample approval and typically runs thirty-five to fifty days, with the stitching set up repeated for each run to keep results consistent.
Does stitching specification matter for small-batch runs?
Yes, though the emphasis shifts. A small batch may not justify dedicated attachments, so the specification focuses on thread, needle, stitch length and tension, which are quick to set. Small-batch pilots are available where a brand is still testing demand, and the same specification scales to a full order at the standard minimum of five hundred pieces per style and colourway.