
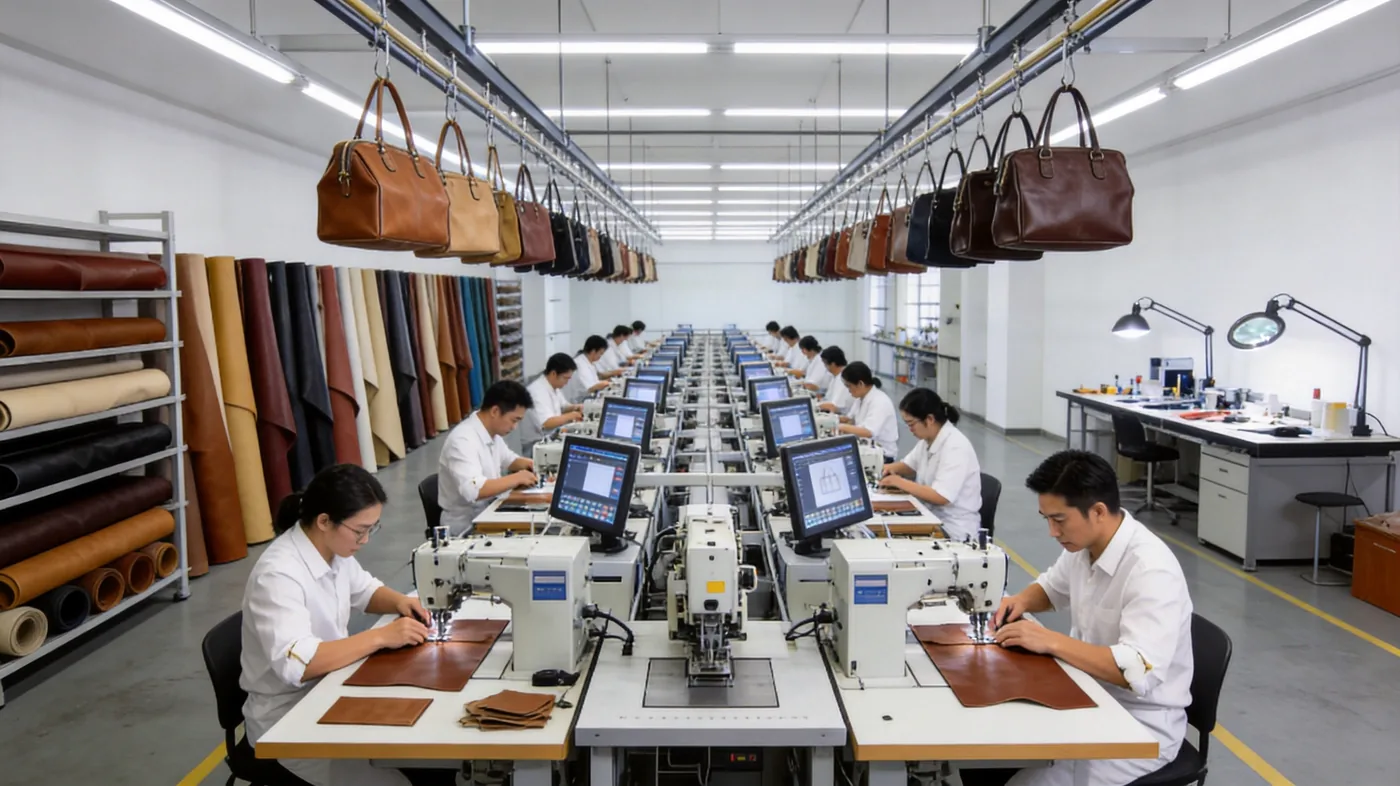
Private label tote bags are the most reliable opening category for a new brand because the silhouette is simple to specify, tolerant of fit variation, generous as a branding surface and cheap to extend into a capsule. A tote has no closure geometry to solve, no complex framing and no sizing risk beyond proportion. It is also where construction quality is most visible: handle attachment, base reinforcement and edge finishing are exposed to daily load. Programmes open at 500 pieces per style and colourway, sample in 6 to 10 working days and run 35 to 50 days in bulk.
Simplicity is often mistaken for ease, and that is where new brands lose money on totes. Because the silhouette is well understood, the difference between a tote that lasts and one that fails is concentrated in three places: how the handles are anchored, how the base carries load, and how the top edge is finished. None of those are visible in a sketch, which is why the specification matters more here than it appears to.
The commercial case is equally clear. A tote spans price bands without changing construction, works across direct and wholesale channels, photographs well at low cost and carries a brand mark at a readable scale. It is also the category most likely to be bought as a second purchase, which makes it useful for building repeat custom early in a brand's life. Customers who own one tote from a label are measurably easier to sell a second bag to than customers who own none, and the tote is usually the piece that starts that relationship.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Why the tote works as a first category
The tote's advantages are structural rather than fashionable. Each of the attributes below reduces a specific risk that a young brand faces, and together they explain why the category appears in so many successful launch ranges.
| Attribute | Commercial consequence | Risk reduced |
|---|---|---|
| Open-top geometry | No closure alignment or hardware tolerance issues | Fit and function returns |
| Simple panel count | Lower unit cost for a given material grade | Budget overrun |
| Large flat surfaces | Branding is readable at a distance | Weak brand recall |
| Proportion tolerance | A few millimetres rarely affect usability | Sizing disputes |
| Cross-channel suitability | Works direct, wholesale and corporate | Channel mismatch |
| Easy extension | One pattern family gives several sizes | Development cost of breadth |
The last row is worth planning around deliberately. Because a tote pattern scales cleanly, a brand can offer a small, medium and large version sharing hardware, lining and edge treatment. Three apparent products can come from one development effort, which is the most capital-efficient breadth available in bags.
Fit tolerance is the other reason the category suits a first range. Unlike a structured handbag, where a few millimetres can prevent a closure from meeting, a tote accommodates variation without functional consequence. That tolerance extends to photography and to customer expectation, since buyers assess a tote on proportion and material rather than on precise dimension.
Construction fundamentals
A tote is a small number of decisions executed carefully. Each element below has a standard solution and a more expensive one, and the choice between them should follow the price band rather than enthusiasm.
| Element | Options | Specification note |
|---|---|---|
| Body panels | Single panel wrapped, or front and back with gusset | Gussets add capacity and cost; wrapped panels show fewer seams |
| Base | Flat reinforced, folded, or with feet | State stiffener type and whether feet are fitted |
| Top edge | Turned, bound, or painted | Painted edges need a defined coat count and finish |
| Lining | Drop-in or attached | Attached linings hold shape; drop-in linings are cheaper |
| Interior | Slip pocket, zip pocket, key hook | Each addition adds operations and cost |
| Closure | None, magnetic, zip or snap | Magnetic closures need reinforcement behind the panel |
The closure decision deserves more thought than it usually receives. An open tote is cheaper and lighter, but many customers expect some security. A magnetic closure is a small cost addition that materially changes perceived usefulness, and it requires a hidden reinforcement plate, which should be specified rather than assumed.
Interior organisation is where cost quietly accumulates. Each slip pocket, zip pocket or key hook adds operations, and a fully organised interior can add a meaningful share to the unit cost without changing the exterior at all. For an entry or core tier, one zip pocket and one slip pocket is usually sufficient; reserve fuller organisation for premium tiers where the retail price supports it.
Sizing and proportion
Proportion is the design language of a tote, because there is little else to differentiate it. Height-to-width ratio, handle drop and base depth together determine whether a bag reads as architectural, relaxed or utilitarian. Standardising these across a capsule creates family resemblance.
| Size | Typical use | Proportion note |
|---|---|---|
| Small | Evening, essentials, secondary bag | Taller ratio; shorter handle drop |
| Medium | Daily carry, work essentials | Balanced ratio; drop sized for shoulder carry |
| Large | Travel, shopping, laptop carry | Wider ratio; longer drop and reinforced base |
| Oversized | Weekend or beach | Soft structure; consider a lining that resists sag |
Handle drop is the dimension customers feel most directly, and it is the one most often left vague. Specify it in millimetres measured from the top edge of the body to the underside of the handle at its highest point, and state whether the measurement is taken loaded or unloaded. A drop that works empty may not clear a shoulder when the bag is full, which is why the loaded measurement is the one worth specifying and the one worth testing on the first sample.
Materials and linings
Material choice determines both the price band and how the bag ages. Because a tote uses large panels, material cost per unit is higher than for most categories, which makes yield an important part of the quotation rather than a footnote.
| Material | Character | Consideration |
|---|---|---|
| Full-grain bovine | Develops patina; most durable | Higher cost; natural markings must be accepted |
| Top-grain with finish | Consistent surface; scratch resistant | Less character over time |
| Saffiano or embossed | Structured, uniform, marks resist | Very consistent; suits graphic branding |
| Canvas or waxed cotton | Lighter, casual, lower cost | Needs a leather trim to read premium |
| Recycled or plant-based | Supports a sustainability claim | Verify documentation before claiming |
Lining weight should be specified relative to the shell, not independently. A heavy lining on a light shell distorts the silhouette and can cause the body to collapse inward at the top edge. A medium-weight lining with a compatible drape preserves the intended shape, and matching the lining colour to the hardware finish is a low-cost way to make the interior feel deliberate.
Cut yield deserves a mention specific to large panels. Because a tote front is one continuous surface, the material must be free of natural markings across its full width, which raises the effective cost of the hide considerably. Specifying an acceptable marking tolerance, and where markings may fall, gives the cutting room latitude and lowers material cost without visible compromise.
Handles: the dominant failure point
Almost every structural warranty claim on a tote traces back to handle attachment. The handle carries the entire load of the bag and its contents, repeatedly, often over one shoulder and often overloaded. Specifying the attachment method is more important than specifying the handle itself.
- Stitched attachment: the handle is stitched through the body panel, with reinforcement behind.
- Riveted attachment: rivets supplement stitching and distribute load; state rivet type and backing plate.
- Extended strap: the handle material continues down the body as a load path, which is the strongest option.
- Box-stitched reinforcement: a rectangular stitch pattern with an X inside, distributing stress across a wider area.
- Stitch density at the root: specify a higher density here than on the body, and state the thread type.
Handle width and padding should be specified alongside attachment. A narrow handle concentrates load on the hand and looks refined; a wider handle distributes it and reads more casual. Where a leather handle is wrapped or padded, state the core material and the seam position, because a seam running along the underside of the handle is the detail most likely to cause discomfort under load.
| Load test | What it simulates | Typical acceptance |
|---|---|---|
| Static load | Bag filled and suspended for a period | No stitch failure or elongation |
| Cyclic load | Repeated lifting and setting down | No progressive stitch damage |
| Strap pull | Force applied directly to the handle root | Defined minimum force in newtons |
| Abrasion | Handle edge rubbing against the body | No visible wear beyond an agreed grade |
Testing should be written into the specification rather than requested afterwards. A pull test costs little during development and prevents the expensive scenario in which a design is approved, tooled and produced before anyone discovers that the attachment method cannot carry the intended load.
Branding placement on a tote
A tote offers the largest uninterrupted branding area of any bag category, which is an opportunity and a temptation. Placement should be chosen relative to panel seams and to how the bag is carried, because a mark visible when the bag is on a shoulder may be invisible when it is held by hand.
| Position | Visibility | Suitability |
|---|---|---|
| Centre front, lower third | High when carried by hand | Strong for logo plates and deboss |
| Upper front near the edge | High when worn on the shoulder | Suits small marks and foil |
| Base corner | Low while carried, high when set down | Discreet; good for second-tier marks |
| Interior lining | Seen by the owner each time | Printed lining or woven label |
| Handle root or tab | Seen in use and in photography | Strong for a repeated house detail |
Consistency across sizes matters more than the exact position. A mark placed at a fixed distance from a panel seam reads as deliberate across a small, medium and large version; a mark centred proportionally on each will sit at visibly different heights. Naming the datum in the specification prevents that drift.
Packaging is part of the branding plan for this category. A tote ships flat or lightly stuffed, and the way it is presented on arrival is the first physical contact a customer has with the brand. Tissue, a dust bag and a card explaining the material and its care cost little relative to the product and are read more carefully than most marketing.
Cost, minimums and where the money goes
Tote cost is dominated by material, because panel area is large relative to the operations involved. That has a useful consequence: simplifying construction saves less than expected, while choosing a slightly lower grade of leather saves more. The reverse also applies, which is why upgrading material is often better value than adding features.
| Cost driver | Relative weight | Lever |
|---|---|---|
| Shell material and yield | High | Panel layout, grade selection, hide size |
| Handle construction | Medium to high | Attachment method and strap length |
| Edge finishing | Medium to high | Method and number of finished edges |
| Lining and interior | Medium | Attachment method and pocket count |
| Hardware | Low to medium | Standard fittings instead of custom tooling |
| Packing | Low | Flat packing where construction allows |
The standard opening point of 500 pieces per style and colourway applies as it does elsewhere. Because a tote pattern scales, brands can sometimes treat a size range as one style for minimum purposes, which makes the category one of the most accessible ways to reach apparent range breadth within a single minimum.
Extending a tote into a capsule
A tote should not remain a single product. The pattern family supports several extensions, each of which shares materials and hardware, and together they form a coherent opening range rather than a one-product brand.
- Develop the medium size first, since it is the reference against which the others are judged.
- Scale to small and large, keeping handle proportion and edge treatment identical.
- Add a zip-top variant of the medium for customers who want security.
- Introduce a canvas or seasonal material version using the same pattern and hardware.
- Add a matching small leather good that uses the same leather and hardware finish.
- Standardise packaging across the capsule so the set reads as one range.
The sequence matters for cash as well as for design. Developing the medium first and adding variants later means the later pieces reuse approved patterns, tooling and materials, so each subsequent style costs less and arrives faster than the one before it. That compounding is what turns a single product into a range within one season's budget, and it is also why the tote remains commercially useful long after the launch: every subsequent season can add one variant at a fraction of the original development cost.
Build your opening range around a proven silhouette
The programme team develops tote capsules from one core pattern, with sampling in 6 to 10 working days, bulk in 35 to 50 days and a 500-piece minimum per style and colourway, coordinated from Quanzhou, Fujian. Send your sizes, material direction and branding placement to service@junyuanbags.com, or message the team on WhatsApp at +86 177 5002 0688.
Frequently Asked Questions
Why are tote bags a good first product for a new brand?
Because the construction is simple to specify, the fit is forgiving, the surface is generous for branding and the pattern scales into several sizes from one development effort. That combination lowers development risk and capital requirement at the same time. The trade-off is that quality is highly visible, so handle attachment and edge finishing must be specified carefully.
What sizes should a tote capsule include?
Start with a medium and scale to small and large from the same pattern family. Three sizes give apparent range breadth while sharing hardware, lining and edge treatment, so the development cost stays close to that of a single style. A zip-top variant of the medium is usually the next addition, because it serves customers who want security.
How do I stop tote handles from failing?
Specify the attachment method, not just the handle. The strongest options extend the handle material down the body as a load path or use rivets with a backing plate to supplement stitching. Add box-stitch reinforcement at the root, specify a higher stitch density there than on the body, and require a pull test during development.
What handle drop should a tote have?
Specify it in millimetres from the top edge of the body to the underside of the handle at its highest point, and state whether the measurement is taken loaded or unloaded. A drop that clears a shoulder when empty may not do so when the bag is full. Around 230 to 280 millimetres suits shoulder carry for most proportions.
Which materials work best for a private label tote?
Full-grain bovine offers the best durability and patina; top-grain with a finish gives consistency; saffiano or embossed finishes resist marks and suit graphic branding; canvas with leather trim lowers cost while reading premium. Choose according to the price band, and pair the lining weight to the shell so the silhouette does not distort.
Should a tote have a closure?
It depends on the customer and the use. An open tote is lighter and cheaper, but many buyers expect some security. A magnetic closure is a modest cost addition that changes perceived usefulness, and it requires a hidden reinforcement plate behind the panel, which should be specified rather than assumed.
How much does a private label tote cost to develop?
Development cost is driven by material rather than by operations, because the panels are large relative to the work involved. Expect the shell to dominate the unit cost, with handle construction and edge finishing next. Simplify construction modestly and spend where customers notice: material quality, edge finish and hardware.
What is the minimum order for private label tote bags?
The standard opening point is 500 pieces per style and colourway. Because a tote pattern scales cleanly, a size range can sometimes be treated as one style for minimum purposes, which makes the category one of the most accessible ways to achieve apparent breadth within a single minimum. Confirm the treatment at quotation stage.
Where should the logo go on a tote bag?
Centre front in the lower third reads best when the bag is carried by hand; a mark near the upper edge is more visible when worn on the shoulder. Choose one and fix its position relative to a named panel seam so that it stays consistent across sizes. Proportional centring on each size produces visibly different heights.
How long does it take to develop a tote range?
Sampling runs 6 to 10 working days for standard constructions, with two to three revision rounds typical for a genuinely new pattern. Bulk takes 35 to 50 days after sample approval, followed by inspection and freight. Developing the medium size first and scaling later means subsequent sizes reuse approved patterns and arrive faster.
Can I make a tote in a sustainable material?
Yes. Recycled leather, plant-based alternatives and responsibly sourced bovine leather are all workable for a tote, because the construction is simple and does not demand extreme material performance. Verify documentation before making any claim, and check that the chosen alternative can carry handle loads without elongation over time.
How do I make my tote different from competitors?
Differentiate through proportion, hardware and interior rather than through the silhouette, which is inherently shared. A distinctive handle root detail, a signature lining and a consistent edge treatment create recognition that is difficult to copy quickly, whereas a novel outline is usually neither protectable nor commercially necessary.
How should a tote be packed for shipment?
Totes are usually shipped flat or lightly stuffed to protect the panels, with tissue between surfaces that might abrade. Carton quantity should balance protection against volumetric freight cost, since bags are bulky relative to weight. Confirm whether retail-ready packing is required, because that changes both the carton specification and the labelling applied at origin.
Should the tote be lined?
Usually yes. A lining hides construction, holds shape and provides a surface for interior branding and pockets. Specify the weight relative to the shell so the silhouette is not distorted, and decide between a drop-in lining, which is cheaper, and an attached lining, which holds shape better and reads as more considered.