
Quality assurance in bag manufacturing is the system that makes consistent quality a property of the process rather than a lucky outcome of the final check. Where inspection measures what has already been made, assurance shapes what is made in the first place through documented specifications, controlled materials, verified setups, in-process checks, trained operators and a feedback loop that corrects root causes. AQL 2.5 single sampling under ISO 2859-1 is one part of that system, not the whole of it, and programmes that rely on inspection alone always carry a higher cost of failure.
Why Inspection Alone Is Not Quality Assurance
Inspection is necessary and it is not sufficient. A final check can only report on a finished lot; by the time defects appear there, the value of the material and labour is already embedded, and the options narrow to rework, sort or reject. Assurance works earlier, where a correction is cheap, and it treats inspection as the last line of defence rather than the first.
- Inspection: measures the finished output and decides whether a lot is acceptable.
- Assurance: shapes the inputs, the process and the people so fewer faults are created.
- Prevention: corrects root causes so a fault does not recur on the next run.
- Records: make quality objective, traceable and reviewable rather than anecdotal.
- Improvement: turns each run's data into a change for the following one.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The Quality System: Policy, Plan and Records
A quality system is not a binder on a shelf. It is the set of documents, decisions and habits that together determine what a floor produces. Its components are interdependent: a policy without a plan is a slogan, a plan without records cannot be audited, and records without improvement merely document the same mistakes repeatedly.
| Component | What it is | Why it matters |
|---|---|---|
| Quality policy | The standard the programme commits to | Sets expectations for the whole team |
| Specification | Measurements, materials and tolerances | Gives the line something precise to build to |
| Inspection plan | Checkpoints, sampling and acceptance rules | Makes judgement consistent rather than personal |
| Defect list | Faults pre-classified critical, major, minor | Removes argument at the point of decision |
| Records | Reports, logs and retained samples | Make quality traceable and reviewable |
| Feedback loop | Review of results and corrective action | Turns each run into an improvement for the next |
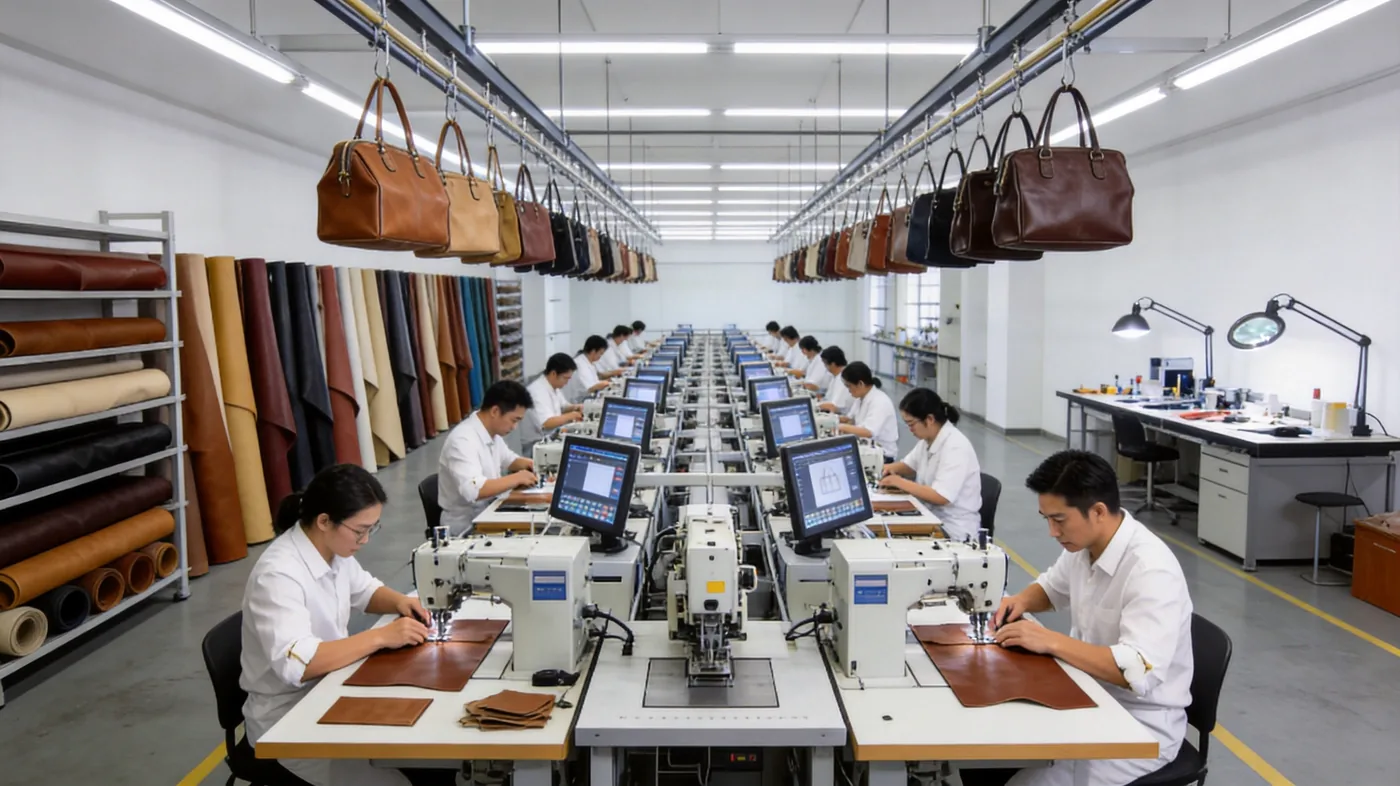
The specification deserves particular attention because it is where most quality arguments actually begin. A brief that says an edge should be clean invites disagreement, while one that states the method, the continuity and the acceptable tolerance gives both the operator and the inspector a standard that can be checked. Assurance starts by writing down what good looks like in terms precise enough to be measured.
Prevention at Source: Materials and Setup
The cheapest defect is the one that never enters the line. Two gates in particular carry a disproportionate share of prevention: the incoming material check and the verification of machine setup before a run begins. Both catch systematic faults before they are multiplied across hundreds of units.
| Gate | What is checked | What it prevents |
|---|---|---|
| Incoming material | Hide colour, thickness and grain against the retained swatch | Panels that will not match or will fail in use |
| Hardware inspection | Finish, dimension and function of zips, clasps and plates | Fittings that fail after assembly |
| Lining and textiles | Weight, colour and stretch against the specification | Puckered or mismatched interiors |
| Pattern check | Dimension and condition of the pattern itself | Systematic dimensional drift across every unit |
| Machine setup | Tension, needle and guides for the leather in question | Skipped or loose stitches repeated across the lot |
| First-article check | The first unit of the lot against the specification | A systematic fault propagating through the run |
Building Quality Into the Process
Beyond the gates at the start, quality is designed into the flow of work itself. Processes arranged so that a fault is difficult to commit, and easy to detect if committed, produce better output than the same floor trying to catch faults at the end.
- Sequence operations so each stage feeds the next, reducing handling and the risk of damage in transit.
- Use jigs, guides and templates so stitch runs and hardware placement are repeatable rather than dependent on memory.
- Place in-process checks at the operations most prone to drift, such as skiving, seam alignment and hardware setting.
- Give operators the reference they need at the station, so the standard is visible where the work happens.
- Confirm dimensions and alignment at defined points rather than only at the end of the run.
This is the practical meaning of building quality into the process: the arrangement of work carries part of the responsibility for the result, so that a competent operator producing an ordinary day's work naturally meets the standard. Where the process is good, quality depends less on individual heroics and more on the system the operator works within, which is what makes consistency achievable across a large run.
Verification: Sampling and Independent Audit
Assurance does not ignore verification; it places it correctly. Verification confirms that the system is working, at defined points, using a consistent method. Two forms matter to most programmes: statistical sampling of finished lots, and independent audit by a third party.
| Method | What it confirms | Notes |
|---|---|---|
| AQL 2.5 sampling | The finished lot meets the agreed standard | Single sampling, ISO 2859-1, general level II |
| In-process checks | The process is holding during the run | Catches drift before the lot is complete |
| Independent audit | The system operates as described | Verifies the internal system rather than replacing it |
| Retained sample | The physical standard remains available | Gold-sealed and held by both parties |
The distinction between verifying an internal system and substituting for one is important. A third-party inspector adds independence and applies a documented standard consistently, but they cannot inspect every unit or manage the process daily. Their value is highest when the internal system is already sound, because then the audit confirms something real rather than discovering that there was nothing to confirm.
Continuous Improvement and the Feedback Loop
A quality system that never changes is a quality system that has stopped learning. Continuous improvement closes the loop by using the data from each run, especially reject rates, rework records and recurring defects, to make a specific change before the next one.
The loop only works if the data is honest, which is why records matter so much. A programme that reports only pass rates hides the information that would allow improvement, while one that logs what went wrong and why has something to act on. Over several runs, the difference between these two approaches compounds: one keeps paying to correct the same faults, and the other gradually stops creating them.
Training and the Human Element
No system runs itself, and leather goods production depends on skilled hands in a way few industries do. Training is therefore a quality assurance activity, not an overhead, because an operator who understands why a standard exists meets it more reliably than one who has only been told what to do.
- Understanding the standard: operators who know what good looks like can recognise when they are drifting.
- Authority to stop: a culture where raising a problem is expected rather than penalised catches faults early.
- Skill development: edge finishing, hardware setting and skiving improve with deliberate practice and mentoring.
- Cross-training: coverage across stations keeps quality stable through absences and seasonal peaks.
- Feedback: operators who hear how their work performed learn to adjust, rather than repeating an unrecognised error.
The human element is where assurance becomes culture. A floor where people take pride in the object and feel able to speak up will outperform one with a better binder and a worse atmosphere, because the daily decisions that determine quality are made by individuals at their stations. Systems set the frame; people fill it.
Making Quality Assurance a Brand Advantage
For a brand, assurance is not only a way to avoid problems. It is a source of confidence that can be built into pricing, positioning and customer promises, because a consistent product is the foundation on which a brand's reputation rests.
| Benefit | How assurance delivers it |
|---|---|
| Consistency across runs | A stable specification and a retained reference keep each run aligned |
| Fewer returns | Prevention and in-process checks reduce faults that reach customers |
| Predictable lead times | Less rework means less disruption to the 35–50 day bulk window |
| Defensible claims | Documented standards support what a brand says about quality |
| Scalable growth | A system that holds at 500 pieces holds at 5,000 |
The commercial argument is straightforward once stated. A brand that can rely on its product does not build contingency into its pricing for returns and replacements, does not spend the season managing complaints, and can make promises to retail partners that it knows it can keep. That reliability is itself a form of margin, because it removes a cost that less disciplined programmes carry whether or not they account for it. Assurance is not a tax on production; it is the reason production can be trusted.
Taken seriously, assurance becomes a competitive asset rather than a cost centre. It is the reason a brand can promise a standard and keep it, season after season, across changes of style and scale. For a wider view of how assurance sits within the making of a bag, the leather bag manufacturing process guide traces the sequence, and the quality control service page sets out how the plan is applied in practice.
Build assurance into the programme, not just the inspection
Send the styles and the quality commitments your brand needs to keep. The programme team will set out a specification, a pre-classified defect list, the in-process checkpoints and the AQL 2.5 plan, so quality is designed into every run rather than hoped for at the end.
Frequently Asked Questions
What is quality assurance in bag manufacturing?
It is the system that makes consistent quality a property of the process rather than a lucky outcome of the final check. It includes documented specifications, controlled materials, verified machine setups, in-process checks, trained operators and a feedback loop that corrects root causes. Inspection measures what has already been made; assurance shapes what is made in the first place. AQL 2.5 sampling is one part of that system, not the whole of it.
How does quality assurance differ from quality control?
Quality control is inspection and testing, measuring the finished output and deciding whether a lot is acceptable. Quality assurance is the broader system that prevents faults from being created at all, through specifications, setup verification, process design, training and improvement. Control catches what has gone wrong; assurance reduces how much goes wrong. Programmes that rely on control alone always carry a higher cost of failure because problems are found late, when value is already embedded.
Why is inspection alone not enough?
Because a final check can only report on a finished lot, by which point material and labour are already spent and the options narrow to rework, sort or reject. Inspection is necessary but it is the last line of defence, not the first. Assurance works earlier, at the material gate, the machine setup and the first article, where a correction costs a few minutes rather than a whole lot. The two complement each other, but prevention carries more of the load.
What are the main components of a quality system?
A quality policy, a precise specification, an inspection plan, a pre-classified defect list, records and a feedback loop. The components are interdependent: a policy without a plan is a slogan, a plan without records cannot be audited, and records without improvement merely document the same mistakes repeatedly. Together they give a floor a standard to build to, a consistent way to judge output, and a mechanism for getting better over successive runs.
What is a first-article check and why does it matter?
It is the sign-off on the opening unit of a lot, or the first piece after a line change, taken before the run is allowed to continue. Checking that piece confirms the machine settings, the pattern and the operator's reading of the brief all line up with the specification. It matters because a fault caught on unit one is fixed once, while the same fault discovered on unit five hundred becomes a rework programme. The check takes minutes and spares the whole lot.
How do incoming material checks prevent defects?
They stop the wrong material before it enters the line, which is the cheapest possible moment. Hides are checked for colour, thickness and grain against the retained swatch, hardware is checked for finish and function, and linings are checked for weight and stretch against the specification. A hide that will not match its neighbours or a fitting that will fail in use is far easier to remove at the store than after it has been cut and assembled.
What role do records play in quality assurance?
They make quality objective, traceable and reviewable rather than anecdotal. Inspection reports, defect logs and retained samples turn a dispute into a review of evidence and allow a programme to see patterns across runs. Without records, improvement is impossible because there is nothing to analyse. With them, each run produces data that can be used to change the process before the next one, which is where assurance begins to pay for itself.
How does continuous improvement work in bag production?
By using the data from each run, especially reject rates, rework records and recurring defects, to make a specific change before the next. The loop tracks the data, finds the pattern, corrects the cause rather than only the affected units, sets a target and reviews progress with the partner. It only works if the data is honest, because a programme that reports only pass rates hides the information that would allow improvement.
Why is training part of quality assurance?
Because leather goods production depends on skilled hands, and an operator who understands why a standard exists meets it more reliably than one who has only been told what to do. Training in the standard, authority to stop and raise problems, skill development, cross-training and regular feedback all lift quality at the point where the work is actually performed. Systems set the frame; people fill it, and the daily decisions are theirs.
Can a third-party inspector replace internal quality assurance?
No. An independent inspector verifies an internal system rather than substituting for one, adding independence and applying a documented standard consistently at a defined point. They cannot inspect every unit or manage the process daily. Their value is highest when the internal system is already sound, because then the audit confirms something real rather than discovering there was nothing to confirm. Verification and assurance work together rather than as alternatives.
How does quality assurance reduce production costs?
By moving corrections to the cheapest possible point. A fault caught at the material gate or the first article costs minutes; the same fault found at final inspection may mean unpicking finished work or scrapping a completed bag. Fewer rejects also mean less disruption to the 35–50 day bulk window, so lead times become more predictable. Over several runs, the savings compound because the process stops creating the same faults repeatedly.
What is the difference between a defect policy and a defect list?
A policy states the standard the programme commits to, while a defect list names every foreseeable fault and pre-classifies it as critical, major or minor. The policy sets the ambition; the list makes it enforceable by removing argument at the point of decision. When both sides have already agreed that a skipped stitch on a load-bearing seam is major and a cosmetic mark is minor, the inspection becomes a record of a standard rather than a negotiation.
How does quality assurance help a brand scale?
A system that holds at five hundred pieces holds at five thousand, because consistency comes from the process rather than from individual attention. A stable specification and a retained reference keep each run aligned, and documented standards mean a new line or a new operator can be brought up to the same level. Without that system, scaling tends to dilute quality, because growth outruns the informal habits that once kept a small run consistent.
What does AQL 2.5 have to do with quality assurance?
It is the verification element of assurance rather than the whole of it. Under ISO 2859-1 at general level II, a single sampling plan fixes how many defective units a random sample may contain before the lot is rejected. That gives both sides an objective, pre-agreed threshold for acceptance, but it operates at the end of the run. Assurance adds the prevention, setup verification, in-process checks and improvement that reduce how many defects the lot contains in the first place.
How should a brand set quality standards with a production partner?
By writing down what good looks like in terms precise enough to be measured, then agreeing the inspection plan and defect classes before bulk begins. State tolerances numerically rather than as adjectives, define the gold-sealed sample, specify AQL 2.5 single sampling in the quotation, and require a first-article check at each lot and line change. Finally, review the defect log at the end of every run and correct the recurring cause, so the standard improves over time.
Is quality assurance only relevant to large orders?
No, and small brands often benefit most, because a single defective run can be proportionally more damaging when volumes are modest. The same specification, first-article check and inspection plan apply whether the lot is five hundred pieces or five thousand. What changes is the scale, not the discipline. A small-batch pilot built to a documented standard also gives a young brand the feedback it needs to scale with confidence later.