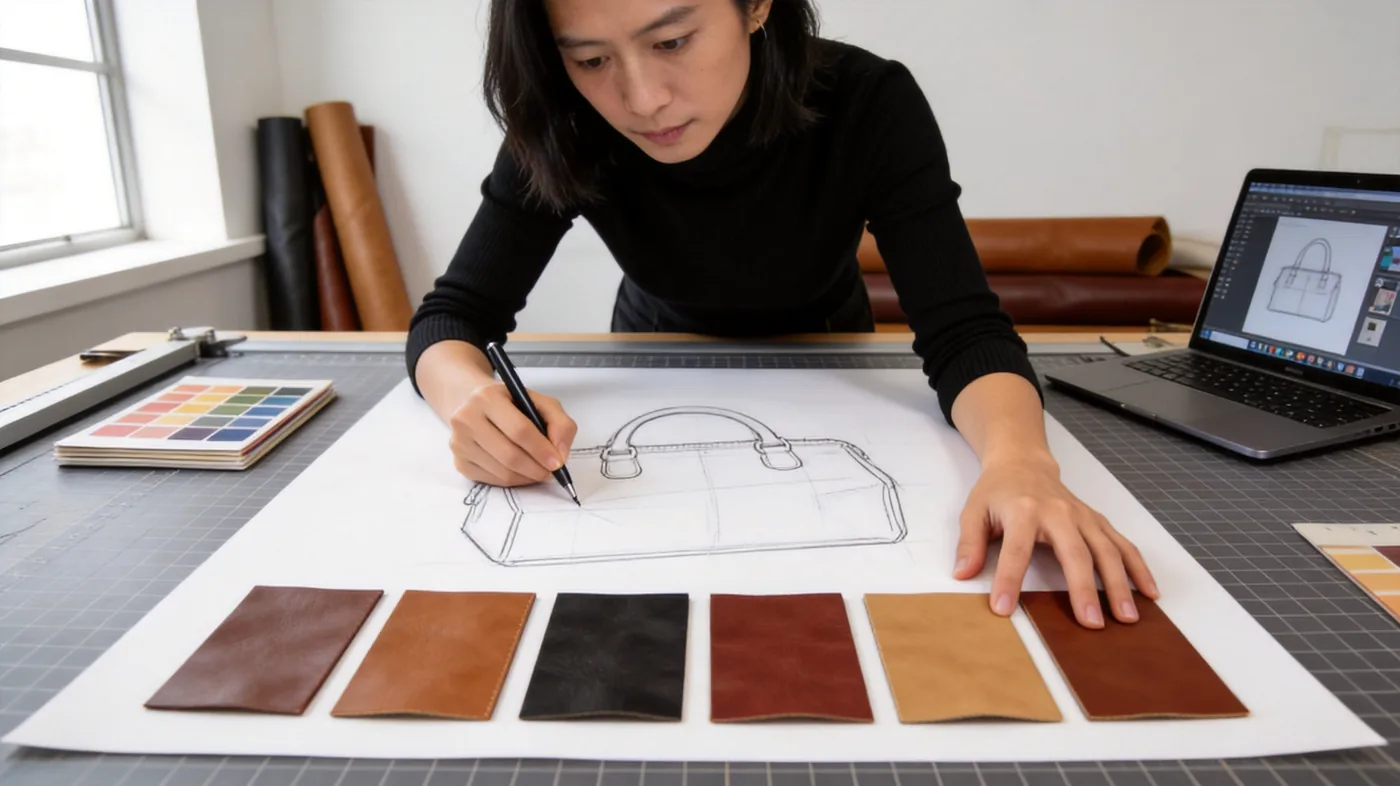
Recycled leather is a genuine waste-recovery material and a misunderstood one: it is a bonded sheet made from reclaimed fibre, not a reconstituted hide, and its performance ceiling is set by the binder rather than by the fibre. Used correctly it delivers stable cost, lower material waste and a defensible recovery story on linings, gussets, small goods and structured panels that are not carrying primary load. Used as a like-for-like substitute for full-grain hide it disappoints, because tensile strength, thickness range and refinishability all fall short. The specification decision is therefore about placement, binder chemistry and documented fibre content.
What recycled leather actually is
The material begins as offcuts, shavings, buffing dust and finished-article waste that would otherwise be landfilled or incinerated. The feedstock is milled back into fibre, blended with a binder and a small proportion of additives, then formed into a sheet under heat and pressure and finished with a coating or embossed grain. The result is dimensionally stable and consistent in thickness, which is precisely what irregular recovered fibre is not, and that stability is what makes the material commercially useful.
Two distinctions matter commercially. The first is between post-industrial and post-consumer feedstock: post-industrial offcuts are cleaner and easier to certify, while post-consumer waste carries more contamination and usually a lower fibre content after cleaning. The second is between a sheet whose fibre content is disclosed and one where it is not, since a material sold as recycled leather can legally contain a modest share of recovered fibre.
Feedstock sources and how quality is graded
Feedstock quality sets the ceiling for what the finished sheet can achieve, and suppliers grade it along lines that are familiar to anyone who has bought hides: fibre length, cleanliness, colour consistency and the chemistry already present in the waste. Chrome-tanned offcuts and vegetable-tanned offcuts are rarely mixed, because their behaviour under heat and their colour base differ, and a batch with mixed tannage produces visible shade problems in the finished sheet.
| Feedstock | Typical source | Character of the resulting sheet | Usual application |
|---|---|---|---|
| Cutting offcuts | Panel waste from bag and upholstery cutting | Long fibre, good strength, clean and consistent | Higher-grade sheets, structural components |
| Shavings and skiving waste | Thinning operations on the production floor | Short fibre, lower strength, uniform colour | Linings, gussets, small goods |
| Buffing dust | Surface finishing operations | Very short fibre, requires higher binder share | Moulded components, packaging, backing boards |
| Post-consumer article waste | Used bags, footwear and upholstery | Variable, needs cleaning and often dechroming | Lower-grade sheets, non-visible components |
| Tannery wet-blue trimmings | Trimming at the tannery before finishing | Consistent tannage, predictable colour base | Mid-grade sheets with stable supply |
A practical consequence for buyers: a supplier quoting a low price is often quoting a sheet with a high buffing-dust share and a correspondingly high binder load. That is a legitimate product, but it performs differently from an offcut-based sheet and should not be specified into the same applications. Asking which feedstock grades a sheet contains is the fastest way to understand a quote that looks too good.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Programme parameters and recycled material interact favourably on one point: because sheet is sold by the metre and cut with tight nesting, yield is predictable and offcut recovery improves further, since the material itself accepts re-milling. Our standard MOQ is 500 pieces per style or colourway, and small-batch pilots are available where a brand wants to test how a recycled sheet behaves on the line before committing a full run.

Binder systems and what they determine
If fibre sets the ceiling, the binder sets the actual performance. It governs flexibility, how the sheet ages, whether it can be heat-formed, and what happens at end of life. A latex-bound sheet is soft and flexible but sensitive to heat and to solvents. A resin-bound sheet is firmer and more heat-stable but less supple. A polyurethane-bound sheet sits between the two and is the most common choice where a leather-like hand is wanted.
| Binder | Hand and flexibility | Heat and solvent behaviour | End-of-life implication |
|---|---|---|---|
| Natural latex | Soft, supple, closest to a milled leather | Sensitive to heat and to solvent contact | Higher bio-content; still bonded, so limited recyclability |
| Synthetic resin | Firmer, holds embossed grain well | Good heat stability, good chemical resistance | Difficult to recover; incineration with energy recovery typical |
| Polyurethane | Balanced hand, good drape | Good resistance, moderate heat stability | Bonded structure limits fibre recovery |
| Bio-based binder | Varies with formulation, improving each cycle | Depends on cross-link system | Best current option, though supply is limited and priced accordingly |
The end-of-life column deserves honesty. A recycled leather sheet is difficult to recycle a second time, because separating cured binder from fibre is not practical at commercial scale. The material's environmental case rests on diverting waste once and displacing virgin material, not on indefinite circularity. Brands that understand this tend to communicate the recovery story rather than a recycling claim, which is also the version that survives scrutiny.
Where recycled leather performs in a bag
Placement is where recycled leather earns its place in a premium programme. It is consistent, stable and cost-predictable, and it takes embossing and edge finishing well. What it does not do is carry high tensile load over a long span, so the design work is about giving it applications that suit a firm, dimensionally stable sheet and keeping structural duties on materials that handle them.
- Linings and interior pockets, where stability and consistency matter more than tear strength
- Gussets and side panels, which benefit from a material that holds shape without springing
- Base reinforcements when laminated to a stronger substrate and protected from abrasion
- Small leather goods: card holders, key fobs, tech sleeves and desk accessories
- Structured panels on framed or semi-framed bags, where the frame carries the load
- Packaging components: rigid boxes, backing boards and presentation inserts
- Trims, binding and welting, where a consistent embossed grain reads as deliberate
The placement list also implies the exclusion list. Recycled sheet is a poor choice for a thin turned edge, because the bonded structure frays rather than burnishing; for a long unstructured strap, because creep under load is higher than hide; and for an unlined bag where the reverse face is visible, because the back of the sheet is not finished to be seen. Each of these is solvable with a construction change, and each is expensive to discover after bulk approval.
Performance limits and how to engineer around them
Engineering around a limitation is straightforward once the limitation is named. Lower tensile strength is addressed by shortening unsupported spans and laminating to a substrate. Fraying at edges is addressed with binding, paint or a turned-and-stitched construction rather than a raw burnish. Creep under sustained load is addressed by reinforcing with a webbing core. None of these are exotic; they are standard techniques applied deliberately.
| Limitation | Why it occurs | Engineering response | Design alternative |
|---|---|---|---|
| Lower tensile strength than hide | Fibre is discontinuous; load is carried by the binder matrix | Shorten spans, add reinforcement, laminate to a substrate | Use hide or a strong textile at load paths |
| Edges fray rather than burnish | Bonded fibre has no continuous grain to compress | Bind, paint or turn and stitch the edge | Choose a construction with covered edges |
| Creep under sustained load | Binder matrix relaxes over time under constant tension | Introduce a webbing or textile core in straps | Reduce strap length and carried load |
| Thickness range is narrow | Sheet formation favours a limited grammage band | Build thickness by lamination instead of skiving | Specify a laminated construction from the outset |
| Cannot be refinished | There is no fibre structure to absorb conditioning or dye | Plan panel or component replacement as the repair route | Design with removable panels |
One further caution concerns humidity. Bonded sheets with a latex binder can soften and, in sustained humid conditions, develop a faint odour as the binder ages. Storing finished goods in a climate-controlled warehouse and specifying a binder appropriate to the destination market prevents almost all of it. Where a programme ships to tropical markets, the programme team will normally specify a resin or polyurethane binder instead.
Certification and traceability for recycled content
Recycled content is an area where documentation matters more than for most materials, because the claim is about what went into the sheet rather than what can be tested in it. Recovered fibre percentage cannot be measured reliably in a finished article, so the evidence is procedural: input records at the mill, and a chain-of-custody arrangement that connects those inputs to the sheet a brand buys.
- Request the declared recovered fibre percentage with the method used to calculate it, by mass or by dry solids
- Ask whether the feedstock is post-industrial or post-consumer, and in what proportion
- Obtain an OEKO-TEX certificate matched to the specific sheet reference, since binders and additives are the risk
- Obtain a REACH statement naming tested substances for goods placed on the EU market
- Confirm CPSIA limits on lead and phthalates where goods enter the United States
- Check whether the mill operates under ISO 14001, which evidences controlled input and waste records
Traceability to the original hide is a separate and harder question. Once fibre is milled and blended, the tannery of origin cannot be established, so a recycled sheet cannot carry an LWG attribution in the way a full-grain hide can. This is not a defect in the material, but it does mean a brand should not imply that its recycled leather comes from audited tanneries. What can be said is that the recovered fibre displaces virgin material, which is a real and defensible benefit.
Cost, yield and programme planning
The economics of recycled sheet are more stable than most buyers expect. Feedstock is abundant and largely independent of hide price movements, sheet is sold by the metre, and nesting is efficient because the material has no natural irregularities to work around. The result is a material whose unit cost is easier to forecast than virtually anything else in a sustainable specification.
| Economic factor | Effect on unit cost | Planning note |
|---|---|---|
| Material price | Generally below mid-grade hide on a per-unit basis | Rises with declared fibre content and with bio-based binder |
| Cutting yield | High and predictable; sheet has no natural defects | Nesting gains are the main cost advantage over hide |
| Offcut re-milling | Clean offcuts can re-enter the same supply stream | Requires segregation by binder type at the production floor |
| Testing | Fixed per sheet reference per test cycle | Test at sheet level, not per colourway |
| Tooling | Standard clicker tooling works; no special dies required | Slight adjustment needed for tighter bend radii |
| Freight | Neutral; similar volumetric profile to coated sheet | Consolidated sea freight remains the lowest-impact option |
For planning purposes, treat recycled sheet as a mid-priced stable material with a modest sustainability story and clear performance boundaries. Sampling runs 6–10 working days for standard constructions and 12–15 for complex ones, and bulk runs 35–50 days after sample approval with inspection at AQL 2.5 under ISO 2859-1. On our SGS-verified production floor in Quanzhou (4,950 m²), offcuts are segregated by material family so that leather fibre can be recovered cleanly rather than mixed with synthetic backing.
- Identify which components will use recycled sheet and which will carry load in another material
- Request fibre content, feedstock grade and binder type together with the compliance file
- Set minimum tear, abrasion and colour-fastness thresholds appropriate to the placement
- Select an edge treatment that suits bonded sheet: bound, painted or turned and stitched
- Confirm the destination market's climate and specify the binder accordingly
- Record the approved sheet reference and test reports in the tech pack before bulk cutting
Put reclaimed fibre to work in the right places
Send us the components you want to specify in recycled sheet and the markets you ship to. We match the binder to the climate, engineer the edge treatment and document fibre content before bulk. Email service@junyuanbags.com or WhatsApp +86 177 5002 0688.
Frequently Asked Questions
How is recycled leather made?
Recovered offcuts, shavings and buffing dust are milled back into fibre, blended with a binder and additives, then formed into a sheet under heat and pressure. A coating or embossed grain is applied last. The result is dimensionally stable and consistent in thickness, unlike the irregular recovered fibre it began as.
Is recycled leather as strong as genuine leather?
No. Because the fibre is discontinuous, tensile and tear strength fall well below full-grain hide, and the sheet creeps more under sustained load. That is manageable through design: shorter spans, reinforcement and lamination. It is not manageable by simply substituting sheet for hide in an existing structural pattern.
What percentage of recycled leather is actually recycled?
It varies by product and is not reliably measurable in a finished sheet, so the figure should come from the mill as a declared percentage with the calculation method stated. Sheets with a high buffing-dust share carry more binder and less fibre. Ask for the number and the method together.
Can recycled leather be recycled again?
Not practically. Separating a cured binder from the fibre is not viable at commercial scale, so the material's environmental case rests on one cycle of waste diversion and on displacing virgin material. Brands should describe it as waste recovery rather than as an infinitely recyclable input.
Where does recycled leather work best in a bag?
Linings, gussets, base reinforcements when laminated, structured panels on framed bags, small leather goods, trims and packaging. It suits applications that value dimensional stability and consistency over tear strength. It performs poorly as a thin turned edge or as a long unstructured strap.
Does recycled leather pass REACH and OEKO-TEX requirements?
It can, but compliance depends on the binder and additives rather than on the fibre. Request an OEKO-TEX certificate matched to the specific sheet reference and a REACH statement naming tested substances for the EU market. Confirm CPSIA limits separately where goods are placed on the US market.
Can recycled leather carry an LWG tannery rating?
No. Once fibre is milled and blended, the tannery of origin cannot be established, so the sheet cannot inherit an LWG attribution. A brand should not imply audited-tannery provenance for a recycled sheet. The defensible claim is that recovered fibre displaces virgin material.
Why do some recycled leather sheets smell?
The odour usually comes from the binder ageing, particularly latex-bound sheets held in warm humid conditions. Resin and polyurethane binders are more stable. Specifying a binder appropriate to the destination climate and storing finished goods in a controlled warehouse prevents most reported cases.
Is recycled leather cheaper than full-grain leather?
Generally yes on a per-unit basis, and the gap widens once cutting yield is counted, since sheet has no natural defects or irregularities to work around. Price rises with declared fibre content and with bio-based binder systems. It remains the most cost-predictable option in a sustainable specification.
How should edges be finished on a recycled sheet?
Edges on bonded sheet fray rather than burnish, so the practical options are binding, edge paint or a turned and stitched construction. A raw burnished edge is not achievable. Choosing an edge treatment at the design stage avoids a costly change after the first prototype.
Does recycled leather take embossing and branding well?
Embossing works well because the sheet is uniform and holds a pressed grain cleanly. Foil hot-stamping and woven labels also perform reliably. Fine debossing can look slightly soft compared with hide, so a metal plate or foil stamp generally gives a crisper brand mark.
What is the difference between post-industrial and post-consumer feedstock?
Post-industrial feedstock is factory and tannery waste, which is cleaner and easier to document. Post-consumer feedstock comes from used articles, which requires cleaning and often dechroming, and yields a lower fibre content after processing. Post-consumer material carries a stronger story and a weaker sheet.
How does recycled leather affect the minimum order quantity?
It usually helps, because sheet is sold by the metre against predictable mill terms rather than by hide availability. Our standard MOQ is 500 pieces per style or colourway, and consolidating colourways keeps costs down. Small-batch pilots are available to validate the construction before a full run.
Can recycled leather be used for a structured bag shell?
Yes, where the structure is carried by a frame or by a laminated substrate rather than by the skin itself. That is how most successful applications are built. Asking the sheet to carry load across a long unsupported span will produce creep and eventual distortion.
How long does a recycled leather component last?
With correct placement and edge treatment, several years of regular use is realistic, and small goods often last far longer. Abrasion resistance depends on the applied finish, so a specified topcoat matters. Components should be designed for replacement rather than refinishing, since bonded sheet cannot be reconditioned.
How should a brand describe recycled leather in marketing?
Describe it as a bonded sheet made with recovered leather fibre, state the declared fibre percentage if it is published, and name the recovery source as post-industrial or post-consumer. Avoid implying the article is fully recyclable or that it originates from audited tanneries. Precision here is what protects the claim.