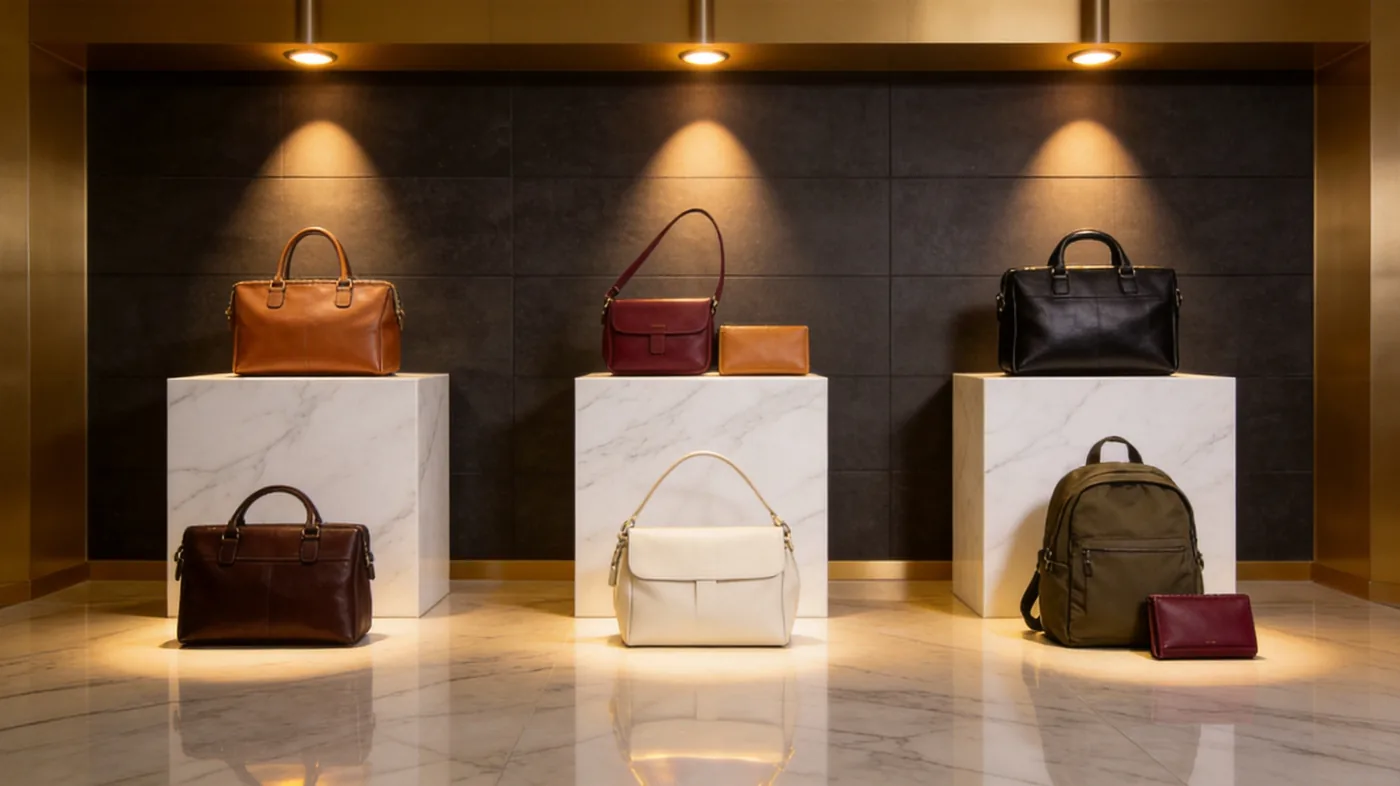
Eco leather has no legal or industry-standard definition, so the term on a specification means nothing until it is broken into the claim behind it. In practice it is shorthand for six separate assertions: reduced tanning chemistry, lower-impact finishing, traceable raw material, audited facility, bio-based or recycled content, or extended service life. Each assertion is testable or auditable in its own way, and each carries a different cost and performance consequence. Buyers should write the specific claim into the material brief, name the evidence that supports it, and avoid the umbrella term in any consumer-facing copy that a regulator might read.
Why eco leather has no agreed definition
Leather is a by-product of the meat industry processed through a long chemical chain, and every step of that chain has been improved by someone. That is why the vocabulary is crowded: a tannery may legitimately describe a leather as eco because it reduced water consumption, while a brand uses the same word for a leather whose merit is that it will outlast three synthetic replacements. Neither is dishonest, but they are describing different things, and a buyer cannot compare them until the underlying attribute is named.
Regulators have started to close the gap. The European Union has been moving towards a framework requiring environmental claims to be substantiated and independently verified before they are used in marketing, and the United States Federal Trade Commission Green Guides have long required claims to be specific and supported. The direction of travel is consistent: generic environmental language is becoming a liability, and specific, evidenced language is becoming the norm.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The claims behind eco leather, and what each one commits you to
The practical way to work with eco leather is to treat it as a set of switches rather than a single material category. A programme can adopt lower-impact chemistry, an audited tannery and a long-life construction without adopting bio-based content, and each switch has its own implication for cost, lead time and appearance. The table below sets out the claims we see most often in briefs and the commitment each one creates downstream.
| Claim | What it actually asserts | Evidence that supports it | What it commits you to |
|---|---|---|---|
| Vegetable-tanned | Tannage using plant tannins instead of chromium salts | Tannery process declaration, supported by laboratory screening for chromium | Longer processing time, a narrower shade range, firmer temper and visible patina development |
| Chrome-free | No chromium in the tanning system | Declaration plus laboratory testing to ISO 17075 for chromium VI | Alternative retannage chemistry that must still be screened for formaldehyde and other residues |
| Metal-free | No metal salts used in tannage | Full process declaration from the tannery | A small supplier base, higher material cost and fewer substance options |
| Low-water or low-impact processing | Measured reductions in water, energy or effluent load per unit | Facility audit data, or a tannery environmental report | A specific tannery rather than a specific leather, so supply is tied to that site |
| Bio-based content | A stated percentage of renewable biological origin | A percentage with the test method named, or input documentation from the supplier | Clarity on which fraction is bio-based: the fibre, the coating or the binder |
| Recycled content | Recovered fibre or recovered polymer in the material | Mass-balance documentation or a recognised recycled-content standard | Performance testing, because recovered fibre bonded with resin behaves differently from full-grain leather |
| Audited supply chain | The facility has been assessed against a published protocol | A current audit report with the site and date matching your order | Renewal discipline: an expired audit weakens the claim at the point it is made |
| Long service life | The article is designed and warranted to last | Construction specification, repairability, spare-part availability | Design decisions that support repair, not only material selection |
Vegetable tanning, chrome-free and metal-free: the chemistry in plain terms
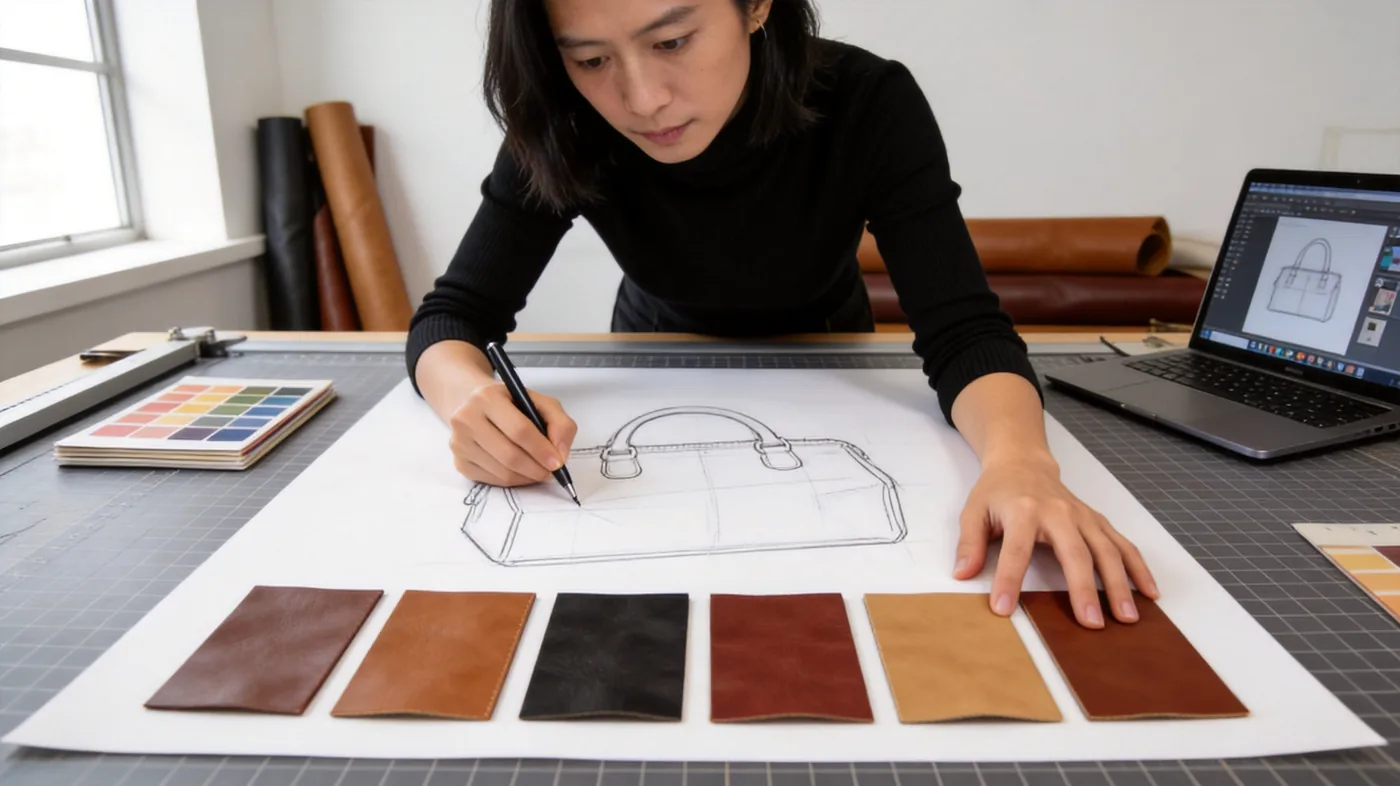
Tanning stabilises the collagen in a hide so that it will not putrefy. Chromium salts do this in roughly a day and produce a soft, dye-receptive, heat-stable leather that underpins most of the world's production. Vegetable tannins do the same job over weeks, building molecular bulk inside the fibre rather than cross-linking it, which is why vegetable-tanned leather is firmer, deeper-toned and slower to make. Aldehyde and synthetic systems sit between the two and are what most chrome-free leathers actually use.
The environmental merit of each route is genuinely contested, and honest sourcing acknowledges this. Vegetable tannage uses large quantities of water and produces a high organic load in effluent, though that load is more readily treated than chromium-bearing sludge. Chrome tannage is efficient in water and energy terms but requires closed-loop management of chromium and disciplined control to prevent chromium VI formation. What is defensible is not a claim that one route is clean, but a statement that a named tannery manages its chosen route to an audited standard.
| Tanning route | Process character | Resulting hand and appearance | Sourcing implication |
|---|---|---|---|
| Chromium | Fast, one to two days, high dye affinity, stable to heat | Soft, supple, wide shade range, uniform from hide to hide | Broadest availability and the tightest cost control; requires chromium VI testing per lot |
| Vegetable | Slow, several weeks in pits or drums, plant tannins | Firm, warm-toned, develops patina, marked natural variation | Longer lead time and a narrower palette; excellent for structured bags and natural edges |
| Aldehyde or synthetic | Chromium-free but still chemical, often used for white and pale shades | Soft, pale base, good light fastness | The common route for chrome-free claims; screen for formaldehyde and confirm the specific system |
| Combination | A light chrome or syntan pre-tannage followed by vegetable retannage | Balanced softness and body with better water resistance | A pragmatic middle ground where a brand wants a lower-impact story without losing performance |
| Metal-free | No metal salts anywhere in the system | Depends on the substitute chemistry; often softer and lighter | Smallest supplier base; expect to qualify the material against physical tests before committing to bulk |
Alternative and bio-based materials: what holds up in a bag
Plant-derived and mycelium-based materials have moved from concept capsules to commercial sampling, and the trade estimate is that their share of the luxury accessories market remains small but is growing quickly. The engineering question is unchanged from any other material: how does it behave at the fold, at the stitch line and at the load point. Plant-fibre sheets are generally a non-woven or a fabric coated with a resin or bio-based binder, so the binder governs abrasion resistance and hydrolysis life far more than the fibre does.
Recovered leather fibre deserves separate mention because it is frequently misunderstood. Bonded leather made from recovered fibre is not equivalent to full-grain leather in tensile or tear performance, and it is usually specified for stiff components, internal reinforcement or small goods rather than for a load-bearing panel. Used in the right place it is a legitimate route to higher material utilisation; used in the wrong place it produces warranty claims.
| Material family | Typical composition | Where it performs in bags | Principal caution |
|---|---|---|---|
| Pineapple leaf fibre sheet | Agricultural residue fibre with a resin coating | Flat panels, trims, linings and small leather goods | Coating dominates durability; flex resistance at fold lines should be tested before committing |
| Cactus and other succulent-derived sheets | Milled biomass with a bio-based binder on a carrier | Body panels where a soft, slightly dry hand is acceptable | Batch-to-batch shade variation is wider than leather; set broader tolerances |
| Apple and fruit-residue composites | Food-industry residue blended with polyurethane or bio-based binder | Linings, trims, structured panels | Confirm the bio-based percentage, because it often applies to the fibre fraction only |
| Mycelium-based sheets | Grown fungal biomass, finished with coatings and embossing | Panels and flat constructions in limited runs | Availability is constrained and mechanical data sets are still maturing |
| Recovered leather fibre | Reclaimed fibre bonded with latex or resin | Stiffeners, internal frames, small goods and backing materials | Lower tensile and tear strength than full grain; do not specify for straps or load points |
| Cork fabric | Cork veneer on a textile or non-woven backing | Lightweight panels, linings, trims and accents | Edge finishing behaves differently; plan for binding rather than painted edges |
| Recycled polyester canvas | Post-consumer or post-industrial polymer spun into fabric | Linings, lightweight bodies and travel constructions | Requires the same restricted substance evidence as a virgin polymer, plus traceability documentation |
Durability, repair and the lifecycle argument
The strongest sustainability claim available to a bag is not about its material at all: it is about how long it lasts and whether it can be repaired. A full-grain leather bag that remains in service for a decade displaces several replacement purchases, and that displacement is larger than most of the differences between tanning routes. This is why construction choices matter as much as material choices: a replaceable lining, a riveted rather than glued strap attachment and a hardware finish that can be re-plated all extend service life.
The counter-argument is that leather's advantage depends on use. A bag that is worn twice and stored badly has no lifecycle benefit over a synthetic equivalent, and a synthetic bag that is genuinely used for a decade is the better environmental outcome. Honest brand communication acknowledges the condition rather than asserting a universal rule, and this is also the position that survives scrutiny under green claims regulation.
| Design decision | Lifecycle effect | Effect on service life | Cost and production note |
|---|---|---|---|
| Full-grain rather than corrected-grain leather | Fewer processing stages and a surface that ages instead of cracking | Longer, provided the finish is maintained | Higher material cost and more visible natural marking |
| Replaceable or washable lining | The body outlasts the part that wears first | Extends usable life materially on daily-carry bags | Adds a construction step and needs a documented repair procedure |
| Riveted and stitched strap attachment | Repairable without replacing the panel | Extends life at the most common failure point | Slightly slower assembly; requires reinforcement at the load path |
| Standardised hardware sizes | Spare parts remain available after the collection closes | Enables repair years after purchase | Limits decorative hardware freedom slightly |
| Painted and sealed edges | Protects the edge from abrasion and moisture ingress | Delays the most visible form of wear | Requires a compliant edge finish and a controlled curing window |
| Documented aftercare and repair offer | Keeps articles in service and supports the claim with evidence | The largest single lever available to most brands | Operational cost sits with the brand, not the material supplier |
Making a claim you can defend
A defensible claim has three properties: it is specific, it is substantiated, and it is not the strongest reading of the evidence. Writing 'vegetable-tanned full-grain leather from an audited tannery' is defensible if both halves are documented. Writing 'eco leather' is not, because no document can support an undefined word. The same discipline applies to what is left out: if a bag has a chrome-free leather body and a polyurethane-coated lining, the claim must not imply the whole article is chrome-free.
- Name the attribute, not the adjective: state vegetable-tanned, chrome-free, or a specific bio-based percentage.
- Hold the document before the copy is written, and date it, because an expired audit does not support a current claim.
- Qualify the scope: if the claim covers the outer material only, say so on the product page and the hangtag.
- Avoid absolute terms such as chemical-free, toxin-free and non-toxic, which are rarely true of any processed material.
- Keep a substantiation file with the certificate numbers, test reports and the reasoning behind the wording.
- Review copy annually, because standards, protocols and candidate-list entries all change.
What sustainable sourcing looks like on a production floor
Material selection is only half of the footprint conversation; the other half is what happens between the hide arriving and the carton leaving. Cutting efficiency, waste segregation, solvent management and the energy profile of the site are all measurable, and a production partner that can show those numbers is more useful to a brand than one that simply offers a certified material list. Our SGS-verified production floor in Quanzhou operates 4,950 square metres with seven lines and 149 machines, and material utilisation is tracked per style because offcut volume is the most immediate lever available.
| Operational lever | What it changes | How it is evidenced | Typical barrier |
|---|---|---|---|
| Marker and nesting optimisation | Reduces offcut volume per unit | Cutting reports and yield percentage per style | Complex panel shapes limit theoretical yield |
| Offcut segregation by material family | Makes recovery and recycling practical instead of nominal | Waste records by stream and weight | Mixed-material laminates are difficult to separate |
| Water-based adhesives and finishes | Reduces solvent load and simplifies compliance | Chemical inventory and supplier declarations | Longer curing windows affect line scheduling |
| Energy monitoring per line | Identifies the true cost centres | Sub-metering data and utility records | Requires capital investment in monitoring equipment |
| Reusable packing and right-sized cartons | Cuts transit volume and single-use material | Packing specification and carton utilisation data | Retailer packing requirements can override the specification |
| Repair and spare-part stockholding | Keeps articles in service after sale | Service records and parts inventory | Requires a commitment beyond the delivery date |
How to brief a sustainable material for a bag programme
A brief that produces the right material in the first sampling round states the claim, the evidence, the performance floor and the commercial envelope together. Omitting the performance floor is the most common failure: a brand asks for a bio-based material without saying what abrasion or hydrolysis resistance it must meet, receives something beautiful that fails at the fold line, and concludes that sustainable materials do not work. The sequence below keeps the four elements in the same document.
- State the claim precisely, including any percentage and the test method behind it.
- List the evidence that must accompany the quotation: audit report, article certificate, laboratory panel.
- Set the performance floor: abrasion, tear, hydrolysis or flex resistance, and colour fastness to rubbing.
- Set the commercial envelope: target landed cost, minimum quantity per colourway, and acceptable lead time.
- Confirm the service-life intent, including whether the lining and hardware must be replaceable.
- Agree the sampling plan: which materials are qualified first, and which tests run in parallel with construction.
- Record the fallback, because a single-source bio-based material needs a second option before bulk is committed.
Programmes that follow this sequence tend to reach approval in the standard sampling window of six to ten working days, or twelve to fifteen where the construction is complex, with bulk following thirty-five to fifty days after sample approval. Inspection is carried out to AQL 2.5 under ISO 2859-1, single sampling, general level II, and shipments leave FOB Xiamen or on EXW, CIF or DDP terms as the programme requires. Where a brand is still choosing between tanning routes, the most useful first step is a qualified sample set: two or three leathers tested side by side, with the documents attached to each, so the decision is made on evidence rather than on a swatch.
Qualify a sustainable material against real evidence
Tell us which claim you intend to make and which tests the material must pass, and we will assemble a qualified sample set with the supporting documents attached to each option. Email service@junyuanbags.com or reach the programme team on WhatsApp at +86 177 5002 0688.
Frequently Asked Questions
What does eco leather actually mean?
It has no standard definition, so on its own it means nothing verifiable. In trade use it usually refers to one of six claims: reduced tanning chemistry such as vegetable or chrome-free tannage, lower-impact finishing, traceable raw material, an audited facility, bio-based or recycled content, or extended service life. A buyer should replace the term with the specific claim and then request the document that supports it.
Is vegetable-tanned leather better for the environment than chrome-tanned leather?
The honest answer is that the comparison is contested. Vegetable tannage avoids chromium and produces a readily treated organic effluent load, but it uses more water and takes weeks rather than a day. Chrome tannage is efficient in water and energy but requires closed-loop chromium management. What is defensible is a statement about a named tannery managing its chosen route to an audited standard.
Does chrome-free leather mean the material contains no chemicals?
No. Chrome-free means chromium salts were not used in the tannage; the material has still been processed, usually with aldehyde or synthetic tanning agents, dyes, fatliquors and finishes. It should be screened for formaldehyde and tested against the same restricted substance panel as any other leather. Marketing language describing chrome-free leather as chemical-free is not supportable.
What is the difference between chrome-free and metal-free leather?
Chrome-free excludes chromium salts but may still use other metal salts such as aluminium, titanium or zirconium in the tanning system. Metal-free excludes metal salts entirely and is the stricter claim. Metal-free materials come from a smaller supplier base, cost more and offer fewer substance options, so the choice is usually driven by whether the brand intends to make the metal-free claim publicly.
Are plant-based leather alternatives durable enough for bags?
They can be, provided the specification matches the application. Most plant-derived sheets are a fibre carrier with a resin or bio-based binder, and the binder governs abrasion resistance and flex life. Flat panels, linings and small goods are realistic applications; load-bearing straps and tight fold lines need qualification testing first. Ask for flex and abrasion data rather than relying on the material story.
What is bonded or recycled leather, and where should it be used?
It is recovered leather fibre bonded with latex or resin. Its tensile and tear strength are well below those of full-grain leather, so it belongs in stiffeners, internal reinforcement, backing materials and small goods rather than straps or load points. Specified correctly it raises material utilisation and reduces waste; specified as a substitute for full grain it produces warranty claims.
How can a bag brand make a sustainability claim that survives scrutiny?
Make it specific, substantiated and conservative. Name the attribute rather than the adjective, hold the certificate or test report before the copy is written, and qualify the scope when the claim covers only part of the article. Avoid absolute words such as chemical-free or non-toxic. Regulators in both the European Union and the United States are moving towards requiring substantiation and independent verification.
Does a vegan leather bag automatically have a lower footprint?
Not automatically. Most vegan leathers are polyurethane or PVC coatings on a textile carrier, and their footprint depends on the polymer source, the coating chemistry and how long the bag lasts. A synthetic bag used for a decade can beat a leather bag worn twice and discarded. Service life dominates material choice in most lifecycle comparisons, so design for repair first.
Which certificates support a sustainable leather claim?
A tannery environmental audit such as the Leather Working Group protocol evidences process management at the facility, while OEKO-TEX LEATHER STANDARD evidences the chemical content of the article. Neither is a sustainability certificate on its own. Recycled content is usually evidenced by a recognised recycled-content standard or mass-balance documentation, and bio-based content requires a percentage together with the test method.
Does choosing a sustainable material increase the cost of a bag?
Usually, but the size of the increase depends on which claim is chosen. Vegetable-tanned and metal-free leathers carry a material premium, and bio-based sheets are priced at a premium while volumes remain low. The larger commercial risk is unplanned qualification: testing three materials late in the calendar costs more in delay than the difference in unit price.
Can a small brand order sustainable leather at 500 pieces?
Yes, with one condition. Most tanneries hold certificates for the articles they sell routinely, so a programme at 500 pieces per style and colourway can select from leathers that already carry evidence. Commissioning new testing for a bespoke shade at that volume is harder to justify, so choosing an existing certified colourway for the first run is usually the practical route.
How long does it take to sample a sustainable material?
Construction sampling runs six to ten working days, or twelve to fifteen for complex builds, and the material qualification tests run alongside it. Most laboratory panels take five to ten working days, so the calendar should be planned around the slowest test rather than the assembly. Booking laboratory slots when the brief is signed avoids the most common cause of delay.
What performance tests should a sustainable material pass before bulk?
At minimum: abrasion resistance, tear or tensile strength, colour fastness to rubbing, and hydrolysis or flex resistance for coated materials. Add formaldehyde and chromium VI screening for any leather, and phthalate or PFAS screening for coated fabrics. The floor should be written into the brief so that a beautiful material which fails at the fold line is rejected in sampling rather than in bulk.
Is leather a by-product, and does that make it sustainable?
Most hides are a by-product of the meat industry, and using them avoids a waste stream, which is a genuine argument in leather's favour. It does not by itself make any particular leather sustainable, because tanning, finishing and transport dominate the footprint. The by-product argument is strongest when combined with a long service life and a repairable construction.