
A bespoke bag maker and a bag manufacturer are not the same thing, and confusing them is the most common sourcing mistake in this category. A maker develops a single piece, adapting construction decisions to the material in hand, and is optimised for singularity. A manufacturer engineers a specification that can be repeated, holds tolerances across a run, and is optimised for consistency at volume. Neither is superior; they answer different questions, and the right choice depends on whether you need one object or five hundred.
The confusion is understandable because the vocabulary overlaps. Both cut leather, both stitch, both set hardware. Many businesses described as makers run small teams and produce in the dozens; many operations described as manufacturers can also handle development. What separates them is not the tools but the underlying discipline: whether the working method is adaptation or repetition. That distinction drives cost, lead time, tolerance and the legal terms you can negotiate.
For a brand, the practical question is rarely which is better in the abstract. It is which model fits the current stage of the programme. Early validation usually favours a maker, because flexibility is worth more than unit cost when the design is still moving. Commercial scale favours a manufacturer, because the specification is stable and consistency becomes the governing requirement. The transition point between the two is where most programmes encounter difficulty.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Two Models Answering Different Questions
The clearest way to separate the models is to look at what each is protecting. A maker protects the integrity of the individual object: if a hide has a scar, the panel is repositioned; if a grain behaves unexpectedly at a fold, the construction is adjusted. A manufacturer protects the integrity of the specification: the same scar would trigger a cutting rule, and the same fold would be resolved by changing the pattern for all units rather than one. Both responses are correct within their own logic.
| Dimension | Bespoke bag maker | Bag manufacturer |
|---|---|---|
| Primary goal | A singular, fully resolved object | Repeatable output at agreed quality |
| Typical quantity | One to a few dozen | Set minimums, commonly 500 per style/colourway |
| Response to material variation | Adapt the construction to the hide | Apply a cutting and grading rule |
| Tolerance discipline | Judged by eye and hand | Stated numerically and inspected |
| Cost driver | Skilled hours | Material yield, line loading, tooling amortisation |
| Documentation | Often minimal | Specification, inspection reports, test evidence |
| Best fit | Prototypes, one-offs, gifts | Commercial ranges, reorders, retail onboarding |
There is a third pattern worth naming, because it is how many contemporary programmes actually run. A development team with maker-level skill handles pattern drafting, prototype construction and detail resolution, then hands a fully documented specification to a structured production programme. The buyer gets the flexibility of a bench during development and the consistency of a line at volume. This arrangement works only where the handover is disciplined; where it is informal, the old failure mode returns.
What a Bespoke Bag Maker Optimises For
The maker's advantage is responsiveness. When a design problem appears halfway through construction, a skilled maker solves it in the moment, drawing on judgement built over years. This is genuinely valuable during development, because it compresses the distance between an idea and something you can hold. It is also why good makers are worth engaging even when the eventual production run will happen elsewhere.
- Material-led decisions: the hide in front of the bench shapes the construction.
- Hand finishing: edge work, skiving and setting are judged by feel as well as measurement.
- Iteration speed on single pieces: changes can be made without re-cutting a full set.
- Low commitment: one unit can be made without tooling or minimum orders.
- Craft depth: techniques that are uneconomic at volume remain available.
The limitation is equally clear. A maker's output is not automatically reproducible, because the decisions that produced it were situational. Hand the same design to a production line and the line cannot read the tacit adjustments — the extra millimetre of skiving here, the altered stitch path there. Unless those decisions were captured in a specification, they vanish at the point of handover. This is the single largest cause of disappointment when a programme moves from development to bulk.
What a Bag Manufacturer Optimises For
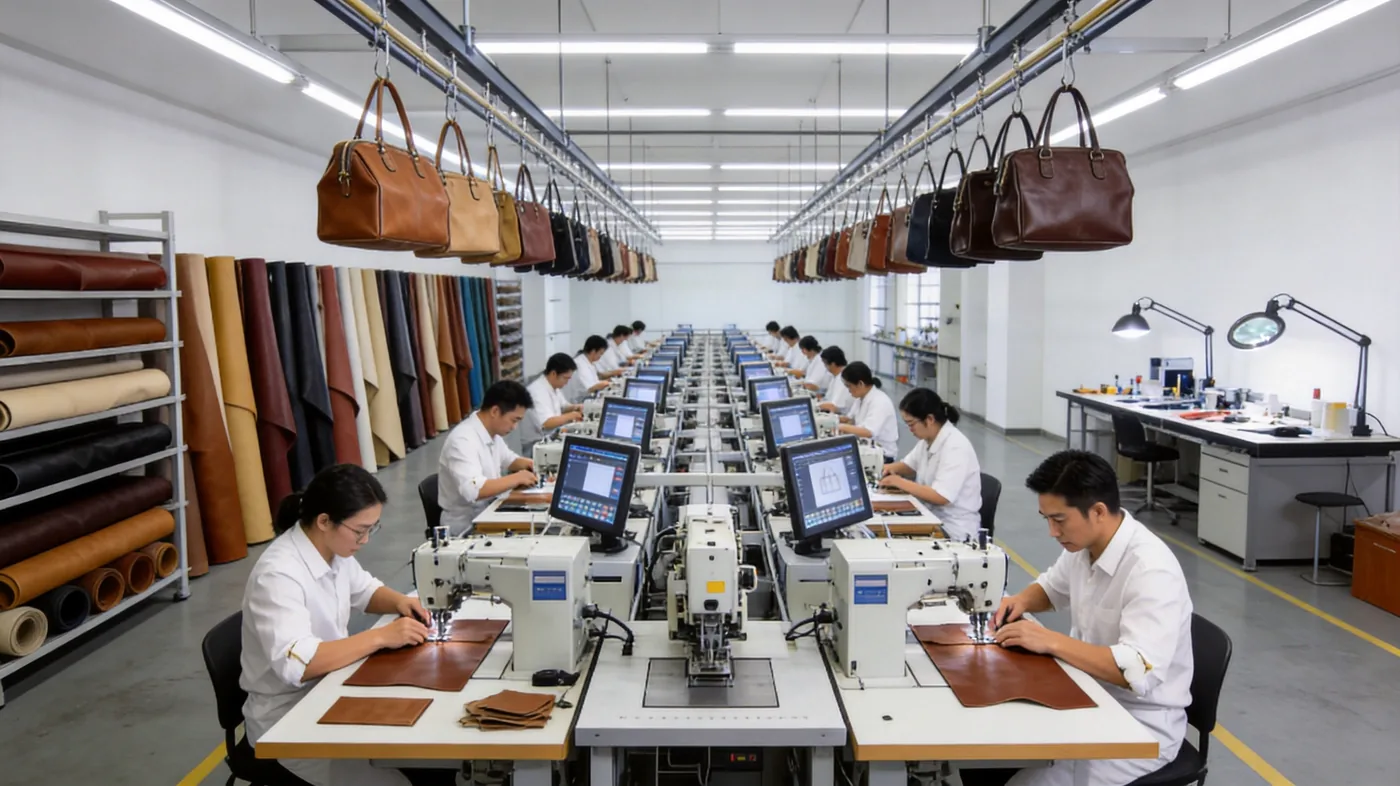
A manufacturer optimises for sameness. The value delivered is not that one bag is excellent but that five hundred are identical within a stated tolerance, produced to a schedule, at a cost that supports the retail price. Achieving that requires things a maker's studio does not need: graded patterns, cutting markers, standard operating procedures, station-by-station quality checks and inspection sampling plans. The discipline is procedural rather than intuitive.
- Graded patterns and cutting markers that fix yield and panel geometry.
- Standard operating procedures that make each station's output consistent.
- Tooling and jigs that remove operator-dependent variation.
- In-process checks at defined stations rather than at the end only.
- Final inspection to a stated AQL with documented results.
- Capacity planning that converts a delivery date into a line schedule.
This is why manufacturers ask for things that feel bureaucratic to a designer. A tolerance is not pedantry; it is the boundary within which the line can work without stopping. A graded pattern is not red tape; it is what makes size two the same object as size one. A pre-production sample is not a formality; it is the reference against which five hundred units will be judged. Understanding this makes the relationship considerably more productive.
The second advantage of the maker is material judgement. An experienced maker reads a hide — where it will stretch, where a scar will weaken a fold, which part of the panel should sit at a stress point — and that judgement is not easily written down. In development it prevents problems before they occur. In production it has to be converted into rules: cutting templates, panel placement guides and reinforcement specifications. The conversion is the work of documentation, and it is what makes craft scalable.
Capability, Capacity and the Gap Between Them
Capability and capacity are frequently conflated, and the confusion is expensive. Capability is whether a partner can build your bag at all: the construction, the material, the tolerances, the finishing standard. Capacity is whether they can build it in the quantity and timeframe you need. A workshop may be perfectly capable of your product and entirely unable to deliver five hundred units by your launch date. Both questions must be answered separately, and the second is the one buyers forget to ask.
| Question | What to ask | What a good answer contains |
|---|---|---|
| Capability | Have you built this construction before? | Comparable examples, a named construction method, known pitfalls |
| Capacity | Which lines are allocated to my programme? | Named lines, a date range, a contingency if a line is lost |
| Consistency | How is tolerance held across a run? | In-process checks, inspection standard, corrective action process |
| Continuity | What happens on reorder? | Retained patterns and tooling, a defined price review mechanism |
| Escalation | Who resolves a specification question? | A named person, an authority level, a response-time commitment |
Capacity questions are easy to ask and easy to answer badly. A monthly output figure tells you what a facility can do in aggregate, not what it will do for you. The useful question is narrower: which lines, in which weeks, for which product type. A partner who answers that specifically is describing a plan; a partner who answers with a headline number is describing a brochure. For programmes with a fixed delivery date, the difference is the entire risk.
Cost Structure: Where the Money Actually Goes
The two models price differently because they consume different resources. A maker's price is dominated by skilled hours, which is why complexity and finishing standard move the number and quantity barely does. A manufacturer's price is dominated by material yield, line loading and tooling amortisation, which is why quantity moves the number sharply and a single unit costs a great deal. Understanding which model is pricing your programme explains most surprises in a quotation.
| Cost component | Maker model | Manufacturer model |
|---|---|---|
| Skilled labour | Dominant, roughly linear per unit | Significant but optimised by line method |
| Materials | Bought in small quantities, higher unit cost | Bought by lot, better pricing, yield engineered |
| Tooling | Minimal; general-purpose tools | Itemised; jigs, dies and moulds amortised across the run |
| Sampling | Often folded into making the piece | Separate, scheduled, usually charged per round |
| Quality assurance | Maker's own judgement | Documented inspection to a stated AQL |
| Volume sensitivity | Low; unit price changes little with quantity | High; unit price falls materially with volume |
One cost element deserves particular attention because it catches first-time buyers repeatedly: cutting yield. Leather is sold by area and hides are irregular, so the number of panels obtainable from a given quantity varies markedly with panel size, shape and the cutting rules applied. Two quotations for the same bag can differ substantially purely because of assumptions about yield. Asking how the yield figure was derived is a reasonable question and often reveals the quality of the costing behind it.
Consistency, Tolerance and the Five-Hundredth Bag
Tolerance is the concept that most cleanly separates the two worlds, and it is the one buyers most often fail to specify. Every dimension varies in production; the question is by how much, and at what point the variation becomes a defect. A maker resolves this implicitly, because the piece in front of them either looks right or it does not. A line cannot operate that way. It needs a number, and it needs to know who checks it and how often.
Tolerance also governs what a buyer can reasonably reject. Without a stated figure, an inspection becomes a negotiation between two reasonable people with different thresholds, which is an argument nobody wins. With one, the same conversation becomes a measurement. This is why experienced buyers treat the tolerance table as the most commercially significant page in the specification, even though it is usually the least interesting to write.
Intellectual Property, Tooling and Exclusivity
The two models also differ sharply on intellectual property. A maker usually works to your design and has no interest in reusing it. A manufacturer holds patterns, tooling and process knowledge, and the commercial terms around them need to be explicit. This is not an accusation; it is the ordinary consequence of industrial production, where tooling exists because somebody paid for it and can be redeployed.
- Confidentiality: a written agreement covering designs, specifications and sampling.
- Tooling ownership: state who owns dies, jigs, moulds and cutting files, and on what terms.
- Exclusivity: ring-fence signature silhouettes and custom hardware from other programmes.
- Design registration: register in the markets where you sell, where protection is available.
- Pattern custody: confirm where graded patterns are held and what happens at the end of the relationship.
- Reorder rights: define how price and capacity are reviewed across seasons.
Confidentiality deserves one further practical note. Where a design has genuine commercial value, discuss it at the level of detail necessary to obtain a quotation, and hold back the elements that constitute the signature until terms are agreed. Most partners will sign a confidentiality agreement without difficulty. The ones who resist are telling you something important about how they will behave once your tooling is on their floor.
Choosing the Right Route for Your Programme
In practice most brands use both at different points. A maker resolves a difficult detail or produces the piece that appears in a lookbook. A production programme turns a settled specification into stock. The skill lies in recognising which stage you are in and briefing accordingly, because asking a manufacturer to improvise is as frustrating as asking a maker for five hundred units.
| Situation | Right route | Reason |
|---|---|---|
| Concept not yet settled | Maker | Adaptation is faster than specification revision |
| One-off commission or gift | Maker | No minimum, no tooling, full craft range |
| Specification approved, 500+ needed | Manufacturer | Tolerance, yield and schedule are engineered |
| Repeat seasonal replenishment | Manufacturer | Patterns and tooling already exist |
| Complex detail needs resolving first | Maker, then manufacturer | Resolve the problem, then document and scale |
| Retail onboarding with technical review | Manufacturer | Requires documented specification and test evidence |
A useful test applies when a programme is ready to move from development to production: could the specification be handed to a different facility and produce the same bag? If the answer is no, the specification is incomplete, and the programme is dependent on individual skill rather than documented process. That dependency is entirely acceptable for a one-off piece. It is a serious risk for a commercial range intended to reorder across seasons.
Whichever route you take, the handover discipline is the same. Capture what was decided, why it was decided, and what the acceptable variation is. That record is what turns a successful prototype into a successful production run, and it is the difference between a programme that scales and one that stalls at unit fifty.
Choose the right route for your programme
Tell the programme team where your design currently sits. You will receive an honest view of whether development support or a production run is the right next step, and what each would involve.
Frequently Asked Questions
What is the main difference between a bespoke bag maker and a bag manufacturer?
A maker builds a singular object and adapts the construction to the material in hand. A manufacturer engineers a specification that can be repeated, holding tolerances across a run of hundreds or thousands of units.
Is a bespoke bag maker better quality than a manufacturer?
Not inherently. A maker can apply techniques that are uneconomic at volume, while a manufacturer delivers consistency a single bench cannot. Quality depends on the specification, the material and the discipline applied, rather than the model itself.
Can a bag manufacturer make a single bespoke piece?
Most commercial programmes are structured around minimum quantities, commonly 500 pieces per style and colourway, because tooling and line set-up must be amortised. A one-off is usually better handled by a maker or a dedicated development route.
When should a brand move from a maker to a production programme?
Move when the specification is stable and the requirement becomes repetition rather than exploration. Signs include repeated orders at similar volumes, fixed material choices and a defined retail or launch date to plan against.
Why do manufacturers insist on written tolerances?
A line cannot judge quality by feel. Tolerance defines the boundary within which production can continue without stopping, gives inspectors an objective test, and provides both parties a shared basis for accepting or rejecting a batch.
Who owns the tooling for a bespoke bag design?
Ownership is contractual and should be stated before tooling is paid for. Buyers typically want written confirmation that tooling is exclusive to their design and will not be redeployed for other programmes without consent.
How long does sampling take with a production partner?
Standard sampling runs six to ten working days per round, extending to twelve to fifteen for complex constructions such as framed openings or multi-material panel work. Two rounds is typical on a first programme.
How long does bulk production take after approval?
Bulk runs 35 to 50 days after sample approval. The range reflects material lead time, cutting yield scheduling, line loading and finishing, and buyers should plan against the upper end rather than the lower.
What inspection standard should I specify for a bulk order?
State AQL 2.5 under ISO 2859-1, single sampling, general level II, in the purchase order. Add a defect classification matrix defining critical, major and minor defects for your specific product.
Do bespoke bag programmes include material testing?
Testing should be scoped per material and per market. Leather raises questions about substances in dye and finish; coated fabrics raise questions about plasticisers; hardware raises questions about nickel release and heavy metals.
How is a bespoke bag quotation structured?
A useful quotation separates unit price, tooling, sampling charges and testing costs. Add freight, insurance, duty, goods and services tax and clearance charges to reach a landed cost per unit at your actual volume.
What payment terms are standard?
T/T with 30 per cent deposit and 70 per cent before shipment is standard, with letters of credit available for larger programmes. Releasing the balance against an inspection pass preserves leverage until quality is evidenced.
Can I keep a maker involved after moving to production?
Yes, and it is often worthwhile. A maker can resolve specific construction problems, refine a detail or produce show pieces, while the production programme handles volume. Capture any resolved detail in the specification.
What causes a prototype to fail in bulk production?
Most failures trace to undocumented decisions: an unrecorded skiving adjustment, a substitute component, or a tolerance nobody stated. The specification is what carries a design from the bench to the line.
How do small brands reach minimum order quantities?
Consolidate colourways within a style, simplify hardware, and start with a small-batch pilot to validate demand. Unit cost will be higher, but the commitment is lower and the learning is faster.
Are sustainability certifications available for both routes?
Documentation is more consistently available through a production programme, which typically holds tannery audit references and test reports. A maker can source certified materials but may not hold formal certification records.
What should be in a specification sheet?
External dimensions with tolerances, material specification with substance and finish, hardware schedule with finish codes, internal layout, branding method and position, packing specification and the inspection standard.
How do I protect a bespoke bag design?
Use written confidentiality agreements, confirm tooling ownership and exclusivity in the contract, register designs where protection is available, and define custody of graded patterns at the end of the relationship.
Is China the only sourcing option for bespoke bags?
No, but the concentration of material supply, hardware manufacturing and skilled assembly in a single region is difficult to replicate. Quanzhou, Fujian combines all three, which is why many programmes are developed there.
How much faster is a reorder than a first order?
Meaningfully faster. With patterns, tooling and material supply established and the construction already familiar to the line, the sampling phase largely disappears and the cycle typically shortens by several weeks.