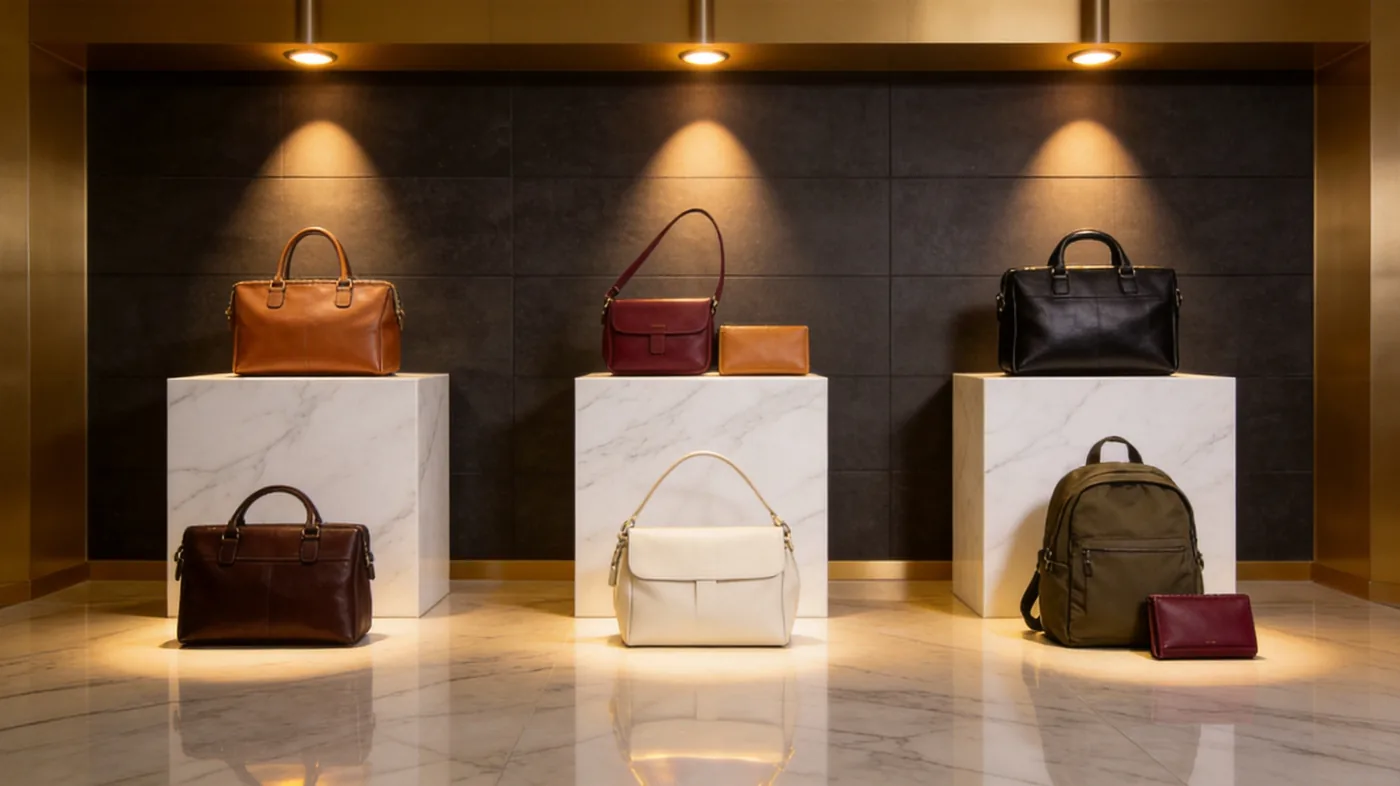
Top-grain leather is full-grain hide whose surface has been sanded to remove defects and then refinished, which trades the densest fibre layer for uniformity, higher cutting yield and more predictable costing. It is the grade most commercial bag programmes are genuinely built on, because it delivers a consistent appearance across a long run at a unit cost that full grain cannot match on large panels. The compromise is real but bounded: corrected leather resists staining better, ages less gracefully and has slightly lower tear strength at equal substance. This article sets out how correction works, how quality is graded, what it costs and where the grade should be specified instead of full grain.
Most of the confusion surrounding the grade comes from retail shorthand. Top grain sits directly beneath full grain in common hierarchies, which invites the assumption that it is a cheaper, weaker version of the same thing. It is more accurate to think of it as a different engineering decision: the surface is rebuilt rather than preserved, and the consequences follow from that single fact.
For sourcing teams the relevant question is not which grade is better in the abstract, but which grade holds a specified appearance and cost across a production run of several thousand pieces. On that measure top grain frequently wins, and it wins for reasons that are worth understanding before the next costing round.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
What correction does to a hide
Correction begins with abrasion. The outermost surface of the hide is sanded lightly or heavily depending on the severity of the defects being removed, which eliminates scars, insect damage and wrinkle marks along with the pore structure that gave the surface its character. What remains is the upper corium, still a strong and serviceable layer, but one that no longer carries the densest fibre arrangement. The tannery then rebuilds a surface by applying pigment, embossing a grain pattern or both.
Because the rebuilt surface is engineered rather than grown, it is repeatable. Two hides corrected to the same specification will look alike, where two full-grain hides never will. That repeatability is the commercial asset, and it is what makes the grade viable for programmes in which a customer may compare two units side by side on a shelf or receive a replacement years after the original purchase.
- Selection: hides are graded on defect count and severity before correction begins.
- Abrasion: the surface is sanded to the depth required to remove the defects present.
- Impregnation: resins and fillers are applied to stabilise the abraded layer.
- Finishing: pigment, binder and protective topcoat are applied in sequence.
- Embossing: a grain pattern is pressed into the surface where uniformity is required.
- Grading: the finished leather is re-graded on surface quality and substance consistency.
How quality is judged after correction
Once the natural surface has been removed, quality is judged on attributes the tannery controls rather than on attributes the animal provided. Substance consistency across the hide matters, because a variable panel behaves inconsistently in cutting and skiving. Finish adhesion matters, because a coating that parts from its substrate under flex will fail in the field long before the leather underneath does. Colour consistency between batches matters most of all for programmes that reorder a colourway across seasons.
| Quality attribute | Why it matters | How it is checked |
|---|---|---|
| Substance consistency | Skiving, folding and edge finishing behave unevenly | Measurement across multiple points per hide |
| Finish adhesion | Coating separation appears as cracking at flex points | Flex testing over a defined cycle count |
| Colour consistency | Reorders must match previous deliveries | Comparison against a retained standard under controlled light |
| Surface defects | Pinholes and loose grain reduce usable area | Visual grading under standard lighting |
| Hand and drape | Determines whether a pattern sits as drawn | Physical assessment on the actual pattern |
The grade also rewards discipline on storage. Corrected leather with a heavy finish can block or transfer in a hot container, and pigment surfaces can mark against one another under pressure. These are logistics failures rather than tannery failures, but they arrive on the same returns report, so packing specification should be agreed alongside material specification.
Finish families and what each delivers
The finish is where the commercial character of the grade is decided. A light semi-aniline treatment keeps some grain readability and a relatively natural hand, and is often chosen for bags positioned just below a full-grain hero piece. A full pigmented finish gives maximum uniformity and stain resistance, and is the default for volume programmes, corporate gift ranges and any product where the surface is expected to survive daily urban use without visible ageing.
- Semi-aniline corrected: some grain visible, good hand, moderate protection, suits mid-premium positioning.
- Pigmented corrected: uniform colour, high stain resistance, pores closed, suits volume and gift programmes.
- Embossed corrected: engineered grain pattern, hides residual defects, excellent repeatability across batches.
- Saffiano-style cross-hatch: pressed pattern with wax finish, scratch resistant, structured appearance.
- Pebble-embossed corrected: soft irregular grain, forgiving in use, popular on slouchy shapes.
- Matte corrected: low sheen, contemporary appearance, shows handling marks less than gloss.
Finish selection should be driven by the service environment rather than by trend. A pale pigmented bag intended for daily commuting will show soil at the handles within a season; the same bag in a darker tone with a protective topcoat may not. That is a specification decision available to the designer, and it costs nothing to make early.

Where the money is saved
Top grain costs less per finished bag primarily because of yield rather than hide price. With defects removed at the tannery, a cutter can nest pattern pieces efficiently, and usable area per hide rises noticeably against full grain. The effect is largest on big, uninterrupted panels, which is precisely where full grain is most expensive. On small components the saving narrows, which is why many programmes specify full grain for handles and top grain for bodies without any visible inconsistency.
There is a second saving in risk. Because the surface is uniform, the cost of a rejected panel falls, and because batches are repeatable, a reorder placed a year later can be matched to the original. For a brand carrying inventory across seasons, that repeatability is worth more than the difference in material cost.
| Cost driver | Behaviour in top grain | Behaviour in full grain |
|---|---|---|
| Usable area per hide | High, defects removed before cutting | Lower, defects must be cut around |
| Batch-to-batch matching | Repeatable within tolerance | Varies by hide and season |
| Rejected panel rate | Low | Higher on large panels |
| Reorder matching | Straightforward against retained standard | Can require fresh selection |
| Price volatility | More stable, wider supplier base | Tighter supply, more selection pressure |
Applications across bag categories
Top grain is the working grade of the bag industry. It appears on volume handbags, corporate gift programmes, travel pieces that need to resist handling, and on any construction where a large panel must look identical across a long run. It is also the natural choice where the design calls for an embossed logo, a saffiano-style cross-hatch or a strongly pebbled surface, all of which depend on a rebuilt grain to read correctly.
Pairing matters as much as selection. A corrected leather with a firm hand behaves differently against a light lining than against a heavier one, and a bag that looks correct empty can slump once it is loaded. The programme team normally tests the shell, the interlining and the lining as a single assembly on the production pattern, because a change in any one of the three alters how the other two behave.
Where it is less appropriate: unlined interiors designed to show natural character, heritage pieces sold on visible patina, and products positioned at the top of a price ladder where the customer expects to see grain variation. In those cases the appearance top grain delivers is the wrong appearance, regardless of how well it performs.
Performance limits and realistic service life
Corrected leather performs well on abrasion and staining, moderately on tear strength and poorly on graceful ageing. The coating that gives it stain resistance is also the layer that eventually wears, and when it wears through, the substrate beneath is a different colour. That failure mode reads as damage where a full-grain scuff reads as character. Expectations should be set accordingly, and care instructions written for the finish actually applied.
Flex behaviour is the other limit. A heavy coating on a soft substrate will crack at a fold eventually, and the remedy is a finish system matched to the tannage rather than a thicker coating. Testing across a defined number of flex cycles before approval is inexpensive and prevents the most common field complaint in this grade.
| Failure mode | Usual cause | Mitigation |
|---|---|---|
| Coating wear at handles and corners | Abrasion beyond the finish rating | Higher rub fastness, reinforced contact points |
| Cracking at fold lines | Heavy coating over a soft substrate | Match finish system to tannage, flex test first |
| Colour transfer onto clothing | Insufficient wet rubbing fastness | Test wet rub, adjust dye fixation |
| Surface blocking in transit | Heat and pressure during shipping | Interleaving, controlled carton density |
| Gloss change at contact points | Topcoat polishing under handling | Specify matte or satin for high-contact panels |
Storage and transit deserve a line in the specification as well. Finished leather can block, transfer or take pressure marks in a hot container, and those defects are discovered at destination rather than at dispatch. Interleaving, carton density and container conditions are inexpensive to control and expensive to remedy once goods have landed.
Writing a specification suppliers can quote
A top-grain specification should name the correction level, the finish family, the embossing pattern where one applies, the substance range, the colour reference with tolerance, and the tests the finished material must pass. Restricted substance declarations under REACH and, where textiles are involved, OEKO-TEX certification should be requested with the quotation rather than after approval. Tannery environmental performance is commonly benchmarked against Leather Working Group audit protocols, and finished goods released from our production floor in Quanzhou are inspected to AQL 2.5 under ISO 2859-1, single sampling, general level II.
Sampling takes 6 to 10 working days for standard constructions and 12 to 15 working days for complex ones, with bulk production running 35 to 50 days after sample approval. Those windows assume the material is settled before the first pattern is cut, which is why the specification is worth writing carefully rather than quickly.
- Name the correction level and state whether an embossed pattern is required.
- State the finish family and the protective topcoat specification.
- Give the substance range in millimetres with an accepted tolerance.
- Hold a retained colour reference and declare the acceptable matching tolerance.
- List the laboratory tests and pass criteria for each, with the method named.
- Request REACH declarations and OEKO-TEX certificates alongside the quotation.
- Specify interleaving, packing and carton density for the intended shipping route.

Compare grades before you cost
Send your pattern and price target, and the programme team will return a grade-by-grade comparison covering yield, finish options, compliance documents and sampling lead time. Email service@junyuanbags.com, or use WhatsApp on +86 177 5002 0688.
Frequently Asked Questions
What is top-grain leather?
Top-grain leather is hide taken from the upper layer of the corium after the natural surface has been sanded to remove defects and then refinished. Correction removes scars and insect marks, after which pigment, binder and sometimes an embossed grain pattern are applied. The result is uniform, repeatable and more stain resistant than full grain, with slightly lower tear strength at equal substance.
Is top-grain leather lower quality than full grain?
It is different rather than inferior. Correction removes the densest fibre layer, so tear strength is somewhat lower, and the engineered finish eventually wears rather than developing patina. Against that, top grain offers uniform appearance, higher cutting yield, better stain resistance and reliable batch matching. For volume programmes and corporate ranges those attributes usually matter more than maximum tensile performance.
How much cheaper is top-grain leather than full grain?
The saving varies with panel size and selection criteria. Because defects are removed at the tannery, usable area per hide rises, and the benefit is largest on the big uninterrupted panels where full grain is most wasteful. On small components the difference narrows. Evaluate cost per finished bag rather than cost per square metre, since yield rather than hide price drives most of the gap.
Does top-grain leather peel or crack?
A heavy coating applied over a soft substrate can crack at fold lines after extended flexing, and when a pigmented finish wears through, the colour beneath differs from the surface. Both failures are prevented by matching the finish system to the tannage rather than by thickening the coating. Flex testing over a defined cycle count before approval is the practical safeguard and is inexpensive to arrange.
What is the difference between top grain and genuine leather?
Top grain describes a specific position and treatment: the upper corium, sanded and refinished. Genuine leather is a broad trade description that can cover corrected splits and lower grades as well as top grain, so it conveys far less information. When buying, specify top grain together with correction level, finish family and substance, and avoid relying on the word genuine in any specification.
Can top-grain leather be embossed?
Embossing suits corrected leather particularly well, because the rebuilt surface accepts a pressed pattern cleanly and repeats it identically across batches. Cross-hatch, pebble and saffiano-style patterns are all produced this way, and brand logos deboss crisply into firmer corrected substrates. Test the artwork on the actual production leather, since soft or heavily waxed finishes recover differently after pressing.
Which finish should I choose for a daily-use handbag?
A pigmented finish with a protective topcoat is usually the right answer for a bag carried daily in an urban environment, because it resists staining and marks far better than a semi-aniline treatment. Choose a darker tone if the bag will be handled frequently. Semi-aniline corrected leather keeps a more natural hand and suits mid-premium pieces that are not expected to endure daily commuting.
How consistent is colour between top-grain batches?
Batch consistency is one of the strengths of the grade, because the finish is applied to a controlled specification rather than inherited from the animal. Reputable tanneries work to a retained standard under controlled lighting and can match reorders across seasons. Require a retained reference panel from the first delivery and specify the tolerance in writing, then verify reorders against it before bulk cutting begins.
Is top-grain leather suitable for structured bags?
Yes. Corrected leather skives and folds consistently, which makes edge finishing and reinforcement more predictable than with variable full grain, and firm tannages hold shape well. Structured business bags and top-handle designs are commonly built on corrected material for exactly this reason. Specify a tannage with sufficient body, and confirm that substance is consistent across the hide before cutting.
What substance should top-grain leather be for a tote?
Substance depends on whether the design is structured or relaxed and on how much reinforcement the pattern carries. A structured tote needs enough body to hold its shape without visible collapse, while a relaxed shape can run lighter and more comfortable on the shoulder. Handles and bases may run heavier than the panels. Build samples at two substances and compare them loaded before deciding.
How long does a top-grain leather bag last?
Service life is long relative to synthetic alternatives and shorter than well-cared-for full grain. The limiting factor is normally the finish rather than the substrate: pigmented coatings wear at contact points such as handles and corners, and the underlying colour then shows. Regular cleaning, careful storage away from heat and light, and prompt attention to handle wear extend useful life considerably.
Does top-grain leather require special compliance documentation?
The same documentation regime applies as for any leather placed on regulated markets: restricted substance declarations under REACH for European delivery, OEKO-TEX certification where textile components or coatings are covered, and tannery environmental performance commonly benchmarked through Leather Working Group audits. Where a product is sold in the United States, or is intended for children, additional CPSIA testing may be required.
Can top grain be mixed with full grain in one bag?
Mixing grades is standard practice and often improves both cost and performance. A common arrangement uses full grain on handles and exterior panels, corrected leather on gussets and interiors, and a coated textile for the lining. The requirement is that each grade is named and approved before sampling, so that any substitution made for yield reasons is agreed rather than discovered.
Why is top grain so common in corporate gift ranges?
Corporate programmes need several hundred or several thousand units that look identical, arrive on schedule and can be reordered next year in the same colour. Corrected leather delivers that repeatability, resists handling marks better than aniline finishes, and takes branding cleanly. Uniformity across a long run matters more to a gift recipient than grain character, which makes the grade a rational fit.
How is top-grain leather tested before approval?
Typical testing covers rubbing fastness dry and wet, flex resistance, finish adhesion, tear strength and light fastness, with methods drawn from ASTM or ISO series depending on the market. Pass criteria should be fixed before sampling begins so results are unambiguous. Where the bag will be carried against light clothing, wet rubbing fastness deserves particular attention, since colour transfer is the most frequent complaint.
When should I choose full grain instead of top grain?
Choose full grain when visible grain variation and patina are part of the product story, when the price point absorbs lower cutting yield, or when the customer is buying longevity as the principal value proposition. Heritage-style pieces and unlined designs usually fall into this group. In most other commercial situations corrected leather gives a better balance of appearance, cost and consistency.