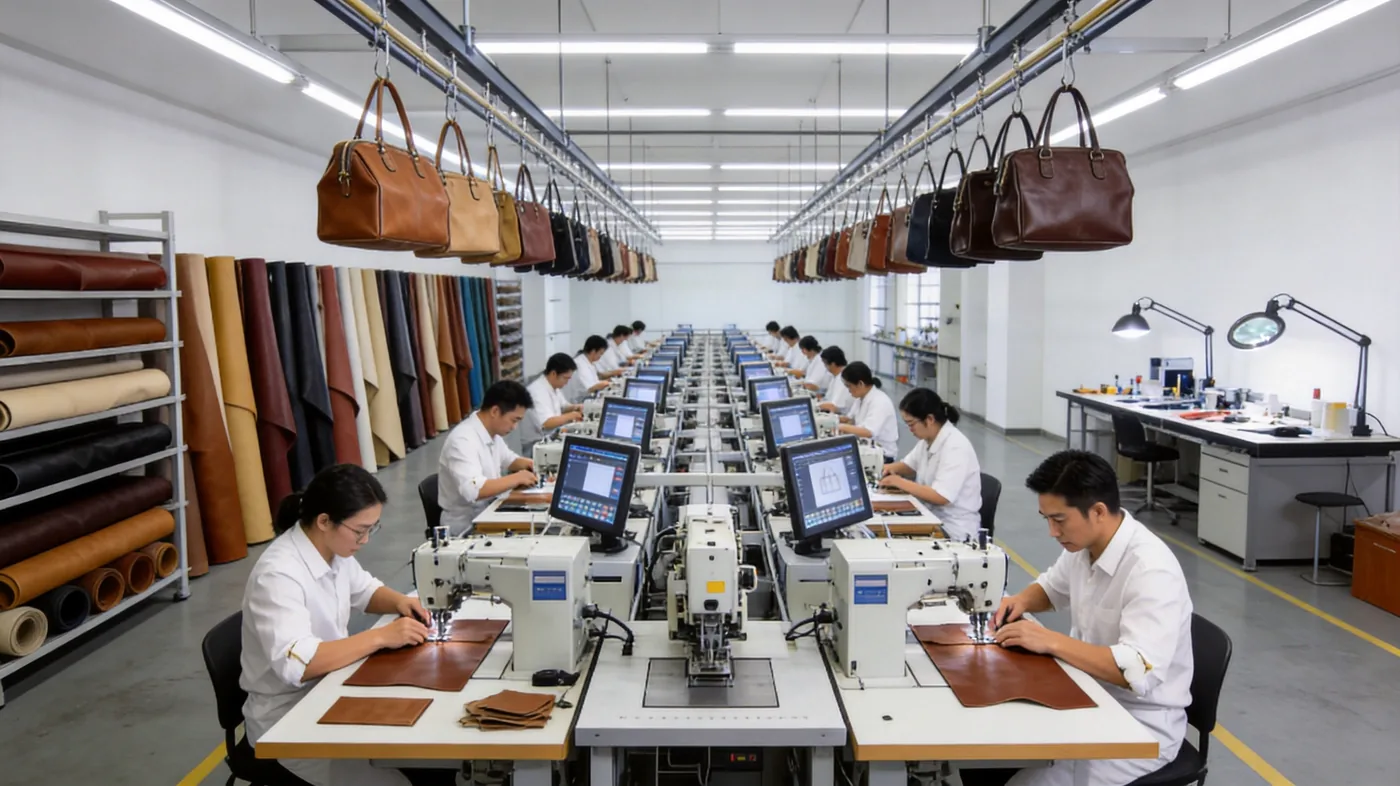
Bespoke leather bags are bags built to a written specification rather than selected from a catalogue: the leather is chosen by grade, tannage and substance; the pattern is cut for one silhouette; the hardware is specified or tooled; and the edges are finished by hand. That path typically costs two to five times a comparable mass-produced bag, because full-grain hides, painted edges, skived joins and solid-brass fittings carry both a material and a labour premium. In exchange, a well-specified bespoke leather bag outlasts several cheaper replacements and develops a patina rather than failing. This guide sets out the leather types worth specifying, the grading logic behind hide pricing, the craftsmanship markers that predict service life, and the cost structure a brand should expect when commissioning a programme.
What Counts as a Bespoke Leather Bag
A bespoke leather bag is defined by specification, not by price tag. The buyer fixes the silhouette, the leather grade and tannage, the substance, the hardware, the lining, the stitch specification and the branding; the bag is then patterned, cut and assembled to that document. If a change can be made to the specification before cutting, the programme is bespoke. If the only variable is colour or logo, it is not.
- The pattern exists only for you. A dedicated pattern set is drafted from your dimensions and reference, and it is graded and nested for your leather rather than reused from an existing model.
- The leather is specified technically. Not beige calfskin, but full-grain bovine, chrome-tanned, 1.2-1.4 mm, aniline finish, colour tolerance within one dye lot.
- Hardware is chosen or tooled. Stock fittings from a library are acceptable; a custom die or a branded zip pull moves the programme into true bespoke territory.
- You approve a physical sample before bulk. A bespoke programme cannot be signed off from a rendering or a swatch alone.
- The specification is version-controlled. Every revision is dated and numbered so the bulk run matches the approved sample rather than an earlier draft.
Two adjacent terms cause confusion in sourcing conversations. Made-to-order usually means a factory's existing model produced in your leather and colour; the pattern, the construction sequence and the hardware are already fixed, so development cost is low and the result is familiar. Private label is broader still — an existing bag is rebranded, often with a logo and packaging change only. Bespoke sits above both: you own the specification, you carry the development cost, and you get a product nobody else can buy. For brands building a recognisable design language, that ownership is the point; for brands testing demand, a made-to-order pilot is often the cheaper first move.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Leather Types Explained
Most disputes about bespoke leather bags begin with a vocabulary problem. Full-grain, top-grain, split, saffiano and suede are not marketing adjectives; they describe where a cut sits in the hide and what has been done to its surface. The table below sets out the seven families a brand is realistically choosing between, with the hand feel, service life, relative cost and ageing behaviour of each. Cost is expressed as an index against full-grain at 100, because absolute hide prices move with the raw market quarter by quarter.
| Leather type | How it feels | Durability | Cost index | How it ages |
|---|---|---|---|---|
| Full-grain | Dense, warm, faintly irregular; pores and natural grain intact | Highest — 15+ years with routine care | 100 (baseline) | Darkens and burnishes into patina; scars soften rather than disappear |
| Top-grain | Smooth, even, lightly corrected; softer and more uniform hand | High — 8 to 12 years | 70-85 | Even colour shift; the finish dulls before the leather itself wears |
| Split (often sold as genuine leather) | Slightly fuzzy underside, embossed or coated to imitate grain | Moderate — 3 to 6 years; coating can crack at folds | 25-40 | Coating flakes and crazes; does not develop a true patina |
| Saffiano | Crisp cross-hatch emboss, firm and dry to the touch | High — 8 to 12 years; strongly scuff resistant | 75-95 | Holds structure and colour; resists marks rather than absorbing them |
| Suede | Velvety nap, dry and matte, cool in the hand | Moderate — 4 to 8 years; nap flattens under friction | 45-65 | Darkens at touch points; bruises and shines rather than patinas |
| Exotic (crocodile, ostrich, python) | Sculptural scale or quill pattern; firm and architectural | High with conditioning — 10+ years; scales lift if allowed to dry | 300-900 | Colour deepens; requires regular conditioning to prevent scale lift |
| Vegan / plant-based | Varies widely, from coated polyurethane to mycelium sheets; cooler hand | Moderate and improving — 3 to 7 years | 30-70 | May craze or delaminate at folds; does not patina in the leather sense |
Two clarifications save buyers time. Saffiano is not a grade; it is a cross-hatch emboss and wax finish applied most often to a corrected top-grain base, which is why a saffiano bag can be both durable and less expensive than a full-grain equivalent. And the term genuine leather is the least informative phrase in the trade — it means only that the material contains leather fibre, which comfortably includes bonded split with a sprayed surface. Where a specification says genuine leather, ask which cut of the hide and which finish.
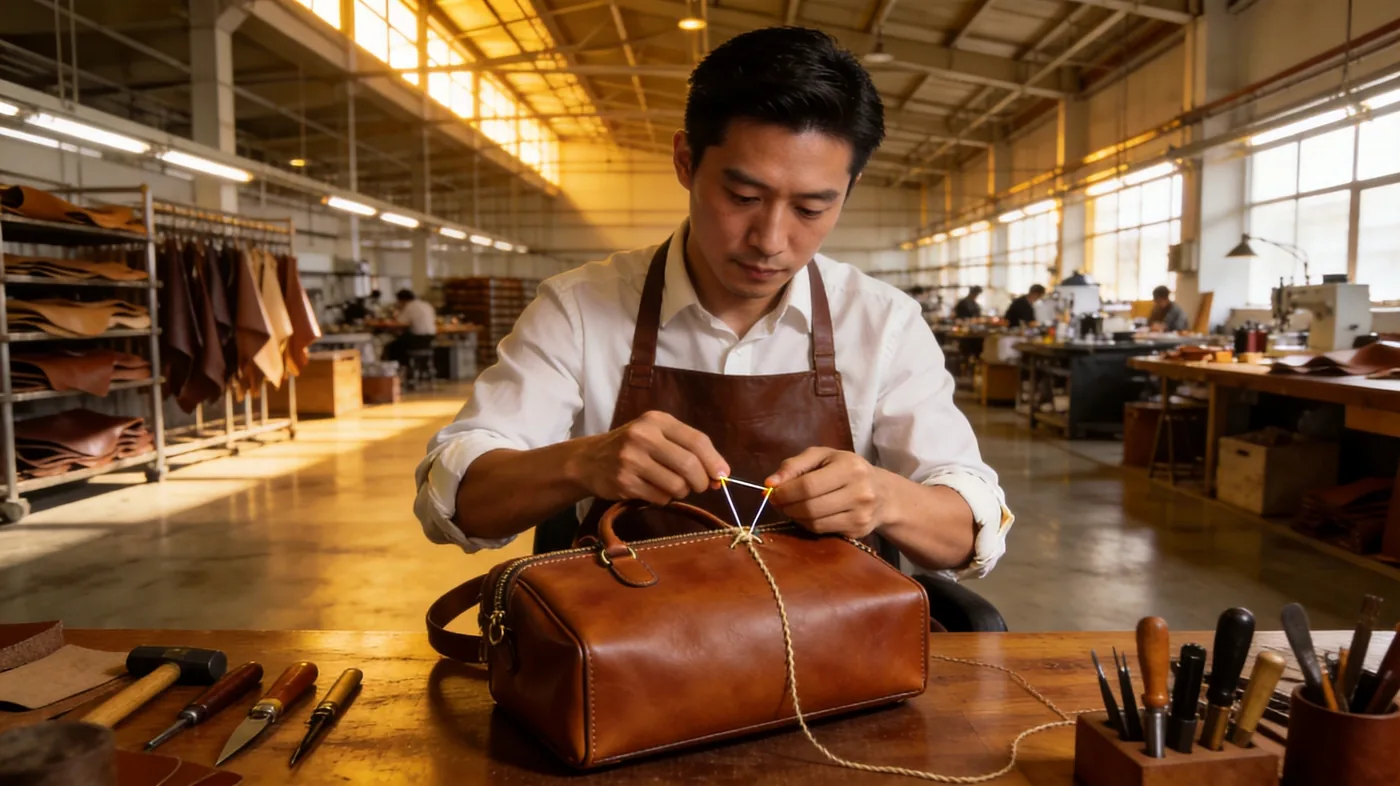
Tannage matters as much as cut. Chrome tanning is fast, produces a supple and colour-stable leather, and dominates volume handbag production. Vegetable tanning is slower, yields a firmer and paler leather that darkens markedly and can be burnished to a bare edge; it is the standard for heritage briefcases and for small leather goods where an untreated edge is part of the aesthetic. Combination tanning sits between the two. A full specification names the cut, the tannage, the substance in millimetres and the finish, because any one of those four missing variables is an invitation to substitute.
How Leather Is Graded and Priced
Leather grading is not a single global standard. Tanneries grade to their own internal systems, and the Leather Working Group audits environmental performance rather than grading hides for quality, so a buyer should treat any grade label as a claim to be verified rather than a certificate. In practice, grading answers three questions: how much of the surface is free of damage, how much of the hide can be cut into usable panels, and how consistent is the colour from one hide to the next.
| Grade | What it means | Indicative usable yield | Where it is used | Cost index |
|---|---|---|---|---|
| Full-grain | Grain left unsanded; natural marks, pores and scars retained | Roughly 55-70% of a hide cuts clean panels | Luxury handbags, briefcases, heritage goods | 100 |
| Top-grain | Surface lightly sanded or buffed to remove defects, then finished | Roughly 70-85% | Mid to premium handbags, linings, small leather goods | 70-85 |
| Corrected grain | Heavily buffed, embossed and pigment-coated to mask damage | Roughly 85-95% | Volume handbags, corporate gifts at a defined price | 40-60 |
| Split / bonded | Lower fibre layer, or fibres bonded to a synthetic backing | Near 100% of the split layer | Trim, linings and straps on entry-level goods | 20-35 |
| Exotic (documented) | Farmed crocodile, ostrich or python with traceability paperwork | Cut to scale symmetry rather than raw area | Top-tier designer handbags and limited runs | 300-900 |
The yield column is the one that explains pricing. Two hides of identical area can produce very different numbers of bags, because a scarred hide forces the cutter to work around damage and a clean hide can be nested tightly. Industry estimates suggest that moving from a tight full-grain selection to a looser one changes the leather line of a unit cost more than any other single decision in the specification. Buyers who accept small natural marks in non-visible panels routinely recover a meaningful share of that cost without the customer ever noticing.
Pricing follows the same logic a buyer already knows from textiles: the more of the raw material you can use, and the less sorting it requires, the lower the unit cost. Exotics invert the model — yield is dictated by scale symmetry rather than surface damage, which is why a single crocodile bag can consume several hides and why the cost index runs to multiples rather than percentages.
Craftsmanship Markers: Stitching, Edges, Hardware
Construction quality is where a bespoke leather bag justifies its price, and it is also where a cheap bag discloses itself within a season. The checklist below is written to be used physically, on a sample, with the bag in your hands. It covers stitching, edges, hardware and internal structure in the order an inspector would work through them.
| Element | What good looks like | What to reject |
|---|---|---|
| Stitch density | 7-9 stitches per inch on structural seams, even and straight, with consistent tension | Fewer than 6 per inch, or visibly wavering lines and puckering at the seam |
| Thread | Bonded nylon or polyester for machine work; waxed linen for hand saddle stitching | Cotton thread, which absorbs water and rots, or thread lighter than the leather it joins |
| Seam construction | Skived and turned joins, or saddle stitch where two needles cross in the same hole | Butted raw edges glued and topstitched, which open under load |
| Backstitching | Three to four reverse stitches at the start and end of every run; no loose tails | Open ends, or tails trimmed flush with the surface and left to unwind |
| Edge finishing | Four passes minimum on painted edges — sand, dye, sand, seal — or turned and burnished on vegetable-tanned leather | A single heavy coat of paint that hides a ragged cut, or a tacky edge that marks paper |
| Edge behaviour | Flexible, uniform in colour, no cracking when the strap is folded back on itself | Crazing at the fold, bubbling, or paint that lifts in a sheet |
| Skiving | Straps and turnovers thinned to 0.8-1.2 mm so joins lie flat without bulk | Unthinned turnovers that create a hard ridge at every join |
| Reinforcement | Rivets or hidden bar tacks at handle roots and strap joins, plus an internal stiffener | Handles stitched straight into the body with no load path into a reinforcement panel |
| Hardware | Solid brass or stainless steel, cast bodies, smooth action, consistent plating colour | Folded zinc-alloy bodies, plating that chips to a green base, or a zip that catches |
| Lining | Pigskin, microsuede or cotton twill cut to the pattern and set in cleanly | Bonded foam laminate, or a lining glued to the leather with visible ripples |
| Base and feet | Feet set through a reinforced panel, or a structured base that holds shape empty | Feet glued to the underside leather, or a base that collapses when the bag is empty |
| Pattern discipline | Grain direction consistent across panels; no mirrored panels from a flipped cut | Mismatched grain or colour shade between the front panel and the gusset |
Two of those markers are worth singling out because they predict failure better than any other. Edge finishing is the most common point of return on leather bags: an edge painted in one pass over a poorly sanded cut will crack within months, and no amount of topstitching will save it. Handle attachment is the second: the load path from a filled bag runs through the handle roots, and if those roots are stitched into a single thickness of body leather with no stiffener and no reinforcement, the stitch line will tear out regardless of how good the thread is.
On the hardware question specifically, ask for the salt spray test hours on any plated fitting and for the base metal, not only the finish name. A fitting described as gold colour tells a buyer nothing; a fitting described as solid brass with a defined plating thickness and a stated test result is a specification. For programmes sold into the United States, hardware and coatings also need to sit inside CPSIA limits for lead and phthalates, and for the European market REACH restrictions apply to the same inputs. Those tests are cheap at material stage and expensive at finished-goods stage.
Cost Breakdown of a Bespoke Leather Bag
Where the unit cost actually goes
The table below shows how cost typically distributes across a bespoke leather bag quoted FOB Xiamen. Shares are indicative industry ranges for a mid-complexity handbag at standard volumes, expressed as a percentage of the FOB unit cost; the figures shift with leather grade, hardware choice and order size, and they are intended to show structure rather than to serve as a quotation.
| Cost element | Share of FOB unit cost | What drives it | Control lever |
|---|---|---|---|
| Leather | 35-50% | Grade, tannage, substance, cutting yield and colour tolerance across dye lots | Loosen the colour tolerance, accept natural marks in hidden panels, nest patterns for yield |
| Hardware | 10-20% | Solid brass or stainless versus plated zinc alloy; custom dies and tooling | Use stock fittings from the supplier library for the first season, then tool a signature piece |
| Lining and interlining | 8-12% | Fibre content, coating, and whether the structure is fused or sewn | Specify one lining across the collection to buy at scale |
| Labour | 15-25% | Stitch count, number of edge-finishing passes, and any hand operations | Design seams that a machine can close cleanly; reserve hand work for visible hero seams |
| Sampling and tooling, amortised | 3-8% | Pattern count, cutting dies, moulds, and the number of sample rounds | Freeze the specification before the second sample round |
| Packaging and branding | 3-6% | Dust bag, box, printed inserts, branded hardware | Standard packaging with a branded card and a woven label |
| Compliance and testing | 1-3% | REACH, CPSIA, OEKO-TEX and physical performance tests on leather and hardware | Test materials before bulk, not finished goods after |
| Quality control and inspection | 1-2% | AQL level, number of checkpoints, third-party inspection fees | Fix inline checkpoints so defects never reach final inspection |
| Freight and duty | Quoted separately | Incoterm, mode, destination market and seasonal rate movement | Compare FOB Xiamen against CIF or DDP before awarding the order |
Three patterns recur in programmes that come in over budget. The first is specification drift: each sample round adds a detail, and the accumulated details add labour minutes that nobody costed. The second is leather selection tightened late in the process, after the price was agreed on a looser grade. The third is hardware tooling started before the design is frozen, which produces a die that has to be remade. None of these are quality problems; all of them are discipline problems, and all of them are avoidable with a written specification that carries a version number.
Best Leather Choices by Use Case
The right leather is a function of what the bag has to survive. A structured top-handle bag that stands on a shelf needs different material behaviour from a slouchy tote that gets thrown into a car. The matrix below maps common use cases to a recommended cut and tannage, with the reasoning and the specification to avoid.
| Use case | Recommended leather | Why | Avoid |
|---|---|---|---|
| Daily commuter briefcase | Full-grain, vegetable-tanned or firm chrome-tanned, 1.6-2.0 mm | Takes knocks, holds structure, and patinas rather than scuffing | Heavily pigmented corrected grain, which shows creases as white lines |
| Structured top-handle handbag | Saffiano or top-grain with sewn interlining | Holds a crisp silhouette and resists the marks of daily handling | Soft milled leather with no internal structure, which slumps within weeks |
| Soft hobo or slouchy tote | Milled full-grain or soft top-grain, 1.0-1.2 mm | Drapes cleanly and stays light despite a large volume | Firm vegetable-tanned leather, which fights the intended slouch |
| Travel duffel or weekender | Full-grain, 1.4-1.8 mm, with a reinforced and footed base | Abrasion resistance at the base and strap roots | Suede at the base panels, which flattens and stains on contact with surfaces |
| Evening or occasion clutch | Suede, metallic top-grain, or an exotic front panel | Surface interest reads well under low light; low abrasion exposure | Aniline full-grain, whose natural marks read as damage on a formal piece |
| Corporate gift at volume | Top-grain with a house emboss and standard packaging | Predictable cost, consistent colour, and a clean branding surface | Exotic materials or custom hardware, which blow a fixed gift budget |
| Vegan-positioned collection | Mycelium sheet or a high-grade plant-based coated material | Matches the brand position without the failure modes of cheap PU | Thin coated polyurethane on a bag expected to carry weight |
| Small leather goods | Vegetable-tanned full-grain, or full-grain offcuts used for burnished edges | Burnishes to a bare edge and darkens with handling | Corrected grain, which cannot be burnished and must be painted |
A short buyer checklist helps convert that matrix into a decision.
- Start from the load. What is the heaviest thing the bag will carry, and where does that weight land? The answer sets the substance and the reinforcement, not the colour.
- Decide whether you want patina or stability. Full-grain and vegetable-tanned leather change visibly; saffiano and pigmented leather do not. Neither is better, but customers have strong expectations either way.
- Match the finish to the retail channel. Natural marks sell well in a heritage context and generate returns in a mass channel.
- Set the colour tolerance in writing. One dye lot, or a defined tolerance against a reference swatch, prevents the most common bulk dispute.
- Specify the hardware base metal. Not the finish name. This single line prevents more quality complaints than any other clause in the specification.
- Confirm the compliance scope early. REACH for Europe, CPSIA for the United States, OEKO-TEX where a brand's own standard demands it.
- Ask for a cutting yield estimate. A factory that can tell you the expected yield on your pattern is a factory that understands your cost structure.
Related construction detail is covered in leather craftsmanship techniques, and the material side in greater depth in luxury leather materials.
Care and Longevity
Longevity is a specification outcome long before it is a care outcome. A full-grain bag with skived joins, four-pass edges and riveted handle roots should deliver fifteen years or more of daily service; the same silhouette in corrected-grain with single-pass edges will typically show its first structural failure inside three. Care extends that curve but cannot rebuild it.
| Leather | Routine care | Frequency | Main risk |
|---|---|---|---|
| Full-grain aniline | Dry cloth after use; neutral cream conditioner; store stuffed and away from direct heat | Condition every three to six months | Water spotting and sun bleaching if left untreated |
| Full-grain vegetable-tanned | Allow even sun exposure early to develop tone; condition lightly; burnish minor scratches with a clean finger | Condition every four to six months | Uneven darkening if exposure is inconsistent |
| Top-grain and saffiano | Wipe with a damp cloth; mild soap for marks; no heavy conditioning needed through the finish | As needed | Finish dulling under abrasion; hard to reverse |
| Suede | Brush the nap in one direction; use a suede block for scuffs; protect before first wear | Brush after every few uses | Flattened nap and oil staining, both difficult to correct |
| Exotic | Condition with a product formulated for exotics; never saturate; store in a breathable bag | Condition every two to three months | Scale lifting caused by dryness |
| Vegan and plant-based | Wipe clean; avoid solvents and heat; do not machine wash | As needed | Crazing or delamination at folds over time |
Three habits do more for service life than any product. Empty the bag fully at the end of each week so the leather is not held under constant load. Store it stuffed with acid-free tissue so panels keep their shape, and in a breathable dust bag rather than plastic, which traps moisture. Rotate between bags if you can, because leather benefits from rest periods in which it can release absorbed humidity. And treat water as an event rather than a disaster: blot, do not rub, then dry slowly at room temperature away from any heat source.
How to Commission a Bespoke Leather Bag
Commissioning runs in a fixed sequence. Skipping a step does not save time; it moves the cost from the development phase into the bulk phase, where it is far more expensive.
- Write the brief. Silhouette, dimensions, target retail price, quantity per colourway, leather preference, hardware direction, branding method and delivery window. References help — photographs of bags you admire, and a note on what you like about each.
- Build the specification. The programme team turns the brief into a costed document: materials by grade and substance, hardware by base metal, linings, stitch specification, packaging and compliance scope. This is the document that gets priced.
- Select materials. Leather is proposed by grade and tannage with a cost consequence attached to each option, so the choice is made against a number rather than in the abstract. Hardware is drawn from the library or specified for tooling.
- Sample. Physical samples in 6-10 working days, or 12-15 for complex constructions. The first sample tests the pattern; the second tests the specification as amended. Expect and plan for two rounds.
- Approve and freeze. The approved sample, plus the specification version that produced it, becomes the reference standard for bulk. Bulk cannot be judged against a sample that was never documented.
- Run bulk. 35-50 days on the SGS-verified 4,950 m² production floor in Quanzhou — 137 staff across 7 lines with 149 machines and monthly capacity of 200,000 pieces.
- Inspect. Incoming, inline and final checkpoints to AQL 2.5 (ISO 2859-1), single sampling, general level II. Third-party inspection can be arranged if your own protocol requires it.
- Ship and review. FOB Xiamen, with EXW, CIF and DDP available. Payment is T/T 30% deposit and 70% before shipment. A post-delivery review of returns and QC data feeds the next season's specification.
Two pieces of advice hold across every programme we develop. First, decide what you will not compromise on before you see the first quotation, because the temptation to trim a specification to hit a price target is strongest at exactly the moment you have least information. Second, treat the first season as a specification-building exercise: launch with stock hardware and a proven construction, learn from the returns data, then spend the second season's development budget on the detail that differentiates you.
Brands exploring lower-impact materials should read sustainable luxury leather before fixing the material spec; traceability requirements and tannery audit expectations are easier to design in than to retrofit.
Commission your leather programme
Send the brief — silhouette, quantity, leather direction and delivery window — to service@junyuanbags.com or WhatsApp +86 177 5002 0688. Sampling can begin within days of specification sign-off, on MOQ 500 pieces per style/colourway.
Frequently Asked Questions
What is the difference between full-grain and top-grain leather?
Full-grain keeps the natural grain surface intact, including pores and minor scars, so it is the strongest cut of the hide and the one that develops a patina. Top-grain is lightly sanded or buffed to remove surface defects and then finished, which produces a more uniform appearance at slightly lower strength. Both are genuine top-layer leather; the trade-off is character versus uniformity.
How much does a bespoke leather bag cost to produce?
Cost depends on leather grade, hardware, labour minutes and volume, so no single figure is useful. Structurally, leather accounts for roughly 35-50% of an FOB unit cost and labour 15-25%, with hardware at 10-20%. A bespoke build typically lands at two to five times a comparable mass-produced bag. The fastest way to a real number is a costed specification, which we can produce from a brief and references.
Which leather lasts longest on a daily-use handbag?
Full-grain leather, in a substance of 1.4-1.8 mm for the body, lasts longest because the densest fibre structure of the hide is left intact. With sound edge finishing and reinforced handle roots, fifteen years or more of daily use is a realistic expectation. Saffiano is the best choice where scuff resistance and colour stability matter more than patina.
Is saffiano leather real leather?
Yes. Saffiano is a finish rather than a grade: a cross-hatch emboss pressed into the leather and sealed with a wax treatment, usually over a corrected top-grain base. The emboss makes the surface highly scuff resistant and water resistant. Because the base is typically corrected grain, a saffiano bag can be durable and uniform while costing less than a full-grain equivalent.
How can you tell if a leather bag is full-grain?
Look for irregular pores, faint scars and slight variation in grain density across a panel; a perfectly repeating pattern usually indicates an embossed corrected grain. Full-grain also feels denser and warmer than coated leather, and it warms quickly to the touch. On a cut edge, full-grain shows a tight fibre structure rather than a sprayed surface layer.
What does leather grading actually measure?
Grading assesses how much of a hide surface is free of damage, how much of the hide can be cut into usable panels, and how consistent colour is between hides. Tanneries use internal systems rather than one global standard, and Leather Working Group audits cover environmental performance, not hide quality. Treat a grade label as a claim and verify it against a physical cutting yield.
Why does full-grain leather cost more than top-grain?
Because yield is lower and sorting is harder. Only a minority of hides are clean enough to sell as full-grain, and the cutter must work around natural marks, so fewer clean panels come off each hide. Top-grain and corrected grain can use a far larger share of the same hide, which spreads the raw cost across more sellable area.
How long does a bespoke leather bag last?
A full-grain bag with four-pass edge finishing, skived joins and reinforced handle roots should deliver fifteen years or more of daily service with basic conditioning. Top-grain and saffiano typically give eight to twelve years, and corrected-grain or split constructions three to six. Longevity is decided at specification stage; care extends the curve but cannot rebuild a weak construction.
Is vegan leather a credible choice for a luxury collection?
It can be, if the material is specified as seriously as leather. High-grade plant-based and mycelium sheets perform acceptably for three to seven years and support a clear brand position. Thin coated polyurethane does not carry weight well and tends to craze or delaminate at folds. Specify the base material, backing and coating by name, and test at fold points.
What thickness of leather should a handbag use?
Handbag bodies generally sit at 1.2-1.4 mm for soft constructions and 1.4-1.8 mm where the bag must hold shape. Straps and handles run 1.8-2.2 mm, and linings and turnovers are skived to 0.8-1.2 mm so joins lie flat. Getting substance wrong is a common and expensive error: too thin and the bag slumps, too thick and it will not close cleanly.
Can you commission exotic leather bags, and what paperwork is needed?
Yes, for documented farmed crocodile, ostrich and python. Exotic programmes require CITES documentation and traceability for every hide, plus import permits in the destination market, so lead times and administrative workload are materially higher than for bovine leather. Cost indices run from roughly 300 to 900 against full-grain at 100, mainly because scale symmetry dictates yield.
How should a full-grain leather bag be cared for?
Wipe it with a dry cloth after use, condition with a neutral cream every three to six months, and store it stuffed with acid-free tissue in a breathable dust bag away from heat and direct sun. Blot water rather than rubbing it, then dry slowly at room temperature. Avoid silicone sprays and heavy oils, which can clog the grain and dull the patina.
What is the minimum order quantity for a bespoke leather bag programme?
MOQ is 500 pieces per style and colourway. Small-batch pilots are available for brands validating a first collection or a new silhouette before committing to full volume. Because leather is bought by the hide and cutting yield is fixed per pattern, volume below the standard MOQ raises unit cost disproportionately rather than proportionally.
How long do sampling and bulk production take?
Sampling runs 6-10 working days for standard constructions and 12-15 for complex builds such as framed bags or multi-panel exotics. Bulk takes 35-50 days after sample approval, depending on volume, leather availability and hardware lead times. Custom hardware tooling and exotic hide procurement are the two items most likely to extend that window, so both should be booked early.
Which certifications should leather and hardware carry?
For the European market, REACH compliance on leather and coatings is the baseline; for the United States, CPSIA limits on lead and phthalates apply to hardware and trims. OEKO-TEX certification is often requested by brands with their own restricted substance lists, and Leather Working Group audit status signals tannery environmental performance. Testing is far cheaper at material stage than on finished goods.