
A bag factory tour of a modern leather bag facility is, at its most useful, an exercise in reading flow. A well-run floor is organised so that material enters at one end and finished, inspected goods leave at the other, with each stage positioned to feed the next without backtracking. On a tour you are looking for that flow, for the presence of defined quality stations, and for evidence of the housekeeping and discipline that separate a competent operation from a crowded room of machines.
What a Facility Tour Actually Reveals
A tour is not a performance, though the best facilities can present well. What it reveals, if you look past the staging, is how the floor is managed day to day: whether work-in-progress piles up or moves steadily, whether operators have the tools and light they need, and whether quality is checked continuously or only at the end.
- Flow: whether material moves in a straight line or doubles back between stages.
- Housekeeping: clear aisles, labelled bins and an absence of debris under the machines.
- Lighting: bright, even light at cutting, stitching and inspection points.
- Work-in-progress: moderate, orderly queues rather than mountains of unsorted panels.
- Quality presence: dedicated inspection stations and reference samples visible on the floor.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The Floor Plan: How Space Is Organised
Scale matters, but layout matters more. Our SGS-verified production floor in Quanzhou runs to 4,950 m² across seven lines with 137 staff and 149 machines, and the value of that space lies in how it is zoned. A floor of the same size that is poorly arranged will produce less and inspect worse than a smaller one that is structured around flow.
| Zone | Function | What good looks like |
|---|---|---|
| Materials store | Leather, lining and hardware held and matched | Racked, labelled and protected from light and damp |
| Cutting and pattern | Panels cut to pattern and skived | Presses and tables positioned to feed assembly directly |
| Stitching lines | Panels joined into a formed bag | Operators seated sequentially along the assembly sequence |
| Finishing and hardware | Edges finished, hardware set, branding applied | Separate bench area with dedicated tools and finishes |
| Inspection | Lots compared against the approved sample | Bright, neutral viewing area with the gold-sealed reference present |
| Packing and dispatch | Goods cartoned, labelled and staged for loading | Clean area with boxes, protective wrap and export labels to hand |
The logic behind the zoning is that distance costs time and time costs money. If the cutting room sits at the far end of the floor from assembly, every bundle must be carried across the building, and each trip adds handling that can crease a panel or lose a batch. A well-planned floor minimises that travel so that the physical arrangement itself does some of the work of quality control. When you walk through, the sequence of zones should feel like a story told in order, and any point where the story doubles back is worth a question.
The Cutting and Pattern Room
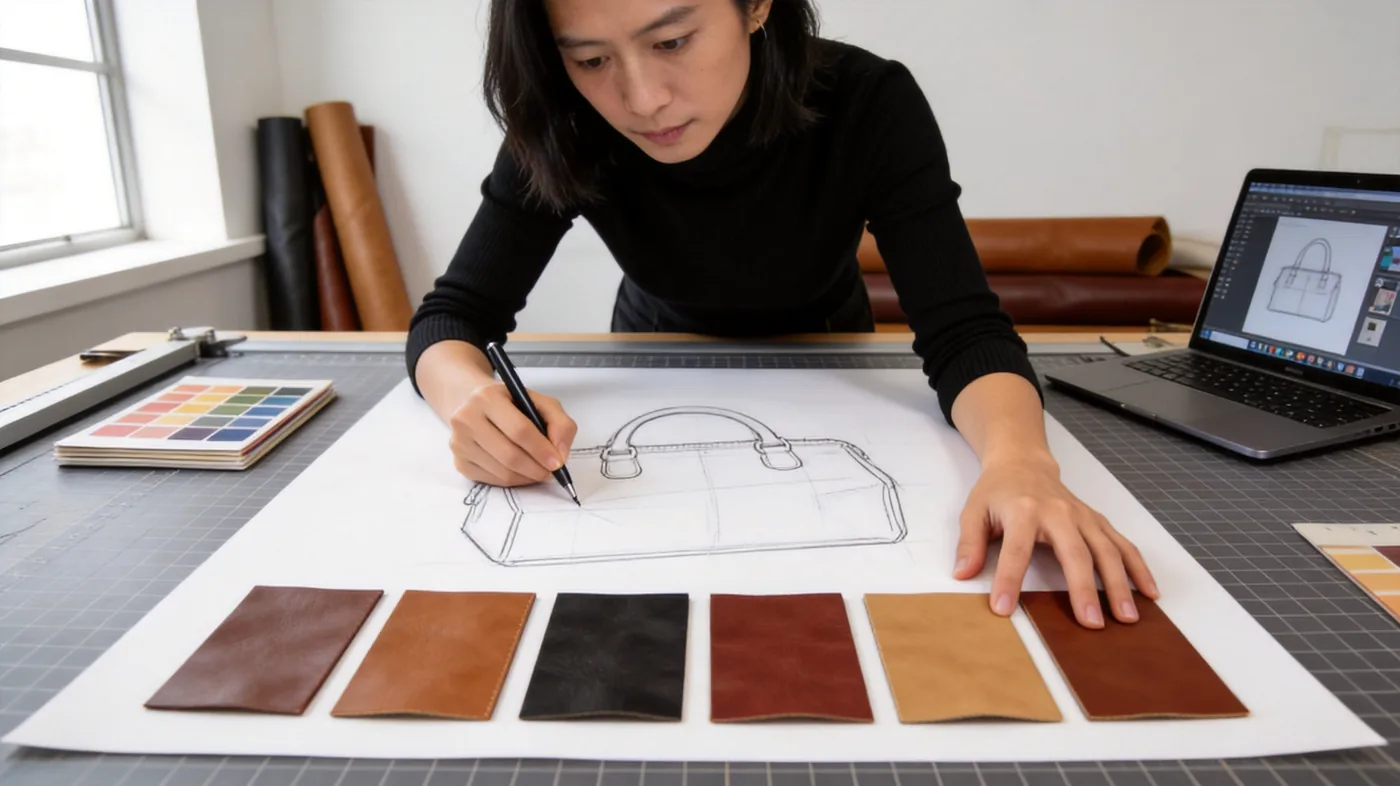
Cutting is where yield, quality and consistency are decided. This is the stage where a hide is inspected and matched, where the grain direction is aligned across panels, and where defects are avoided by nesting the pattern around them. A strong cutting room shows evidence of all three, and of the discipline that keeps a wrong panel from ever reaching assembly.
| Element | Why it matters | What to look for |
|---|---|---|
| Hide inspection | Catches flaws before they are cut in | Trained eyes, good light, hides checked against swatches |
| Nesting and yield | Controls material cost and consistency | Patterns laid to avoid defects and align grain |
| Skiving | Thins leather at folds and seams | Correct machinery set to the thickness on the tech pack |
| Panel marking | Keeps matched panels together | Numbered or bundled panels ready for assembly |
On a tour, it is worth pausing at the cutting tables rather than hurrying past them. The way hides are stored, the way patterns are laid and the way panels are bundled tell you a great deal about how carefully the rest of the process is likely to go. A cutting room running to habit and guesswork will be matched by an assembly line running the same way.
The Stitching and Assembly Lines
The stitching lines are usually the busiest and loudest part of the floor, and the temptation is to watch the fastest operator. It is more informative to follow the sequence: how a bag moves from one station to the next, how lining is attached, and how hardware is set relative to the seams that carry load.
- Sequential stations: operators arranged so the bag moves forward rather than back and forth.
- Consistent jigs and guides: templates that keep stitch runs and hardware placement repeatable.
- Reinforcement: visible at handle roots, gusset corners and strap anchors.
- Lining attachment: clean interiors with no puckering, slack or stray adhesive.
- In-process checks: stitch density and alignment spot-checked during the run, not only afterwards.
The point of an assembly line is not speed for its own sake but consistency. When every bag passes through the same stations in the same order with the same jigs, the variation between unit one and unit five hundred narrows. That is the mechanism behind a predictable bulk run, and it is far more valuable to a brand than any single impressive operator.
There is also a craft dimension that a tour should not obscure. Assembly lines are excellent at consistency, but some operations, edge finishing especially, remain partly by hand and depend on the judgement of a trained finisher. A floor worth trusting balances the two: templated and jigged operations where repeatability is essential, and skilled hands where touch and eye cannot be templated. Watching a finisher work an edge around a tight corner is one of the quickest ways to gauge the true ceiling of a facility's quality.

Finishing, Hardware and Inspection
Finishing is where craft and process meet, and it is often the stage most revealing of a facility's true standard. Edge painting, burnishing, hardware setting and branding are also where the smallest lapses read most loudly to a customer, so a floor that treats them as an afterthought is telling you something important.
| Operation | What is checked | Pass standard |
|---|---|---|
| Edge finishing | Continuity, even thickness, no beading or creep onto the grain | Level film or consolidated fibre as per the method and sample |
| Hardware setting | Finish, orientation, firm engagement, no scratches | Correct, secure and silent, matching the approved specification |
| Branding | Placement, depth and legibility of embossing or foil | Matches the approved sample exactly |
| Final inspection | Whole bag against the gold-sealed reference | AQL 2.5 single sampling under ISO 2859-1, general level II |
Materials Storage and Traceability
What happens before the first cut is decided by how materials are stored and tracked. Leather is a natural material that responds to light, heat and moisture, and a store that exposes hides to any of these will deliver panels that vary in colour and hand. Traceability, meanwhile, is what allows a problem to be traced to a batch rather than shrugged at.
A store run to these habits signals a programme that takes materials seriously. It also makes the sampling and bulk stages more predictable, because the leather specified at sampling is the leather that reaches the line, matched and documented rather than substituted under pressure.
From Packing to the Loading Bay
The last stretch of the tour is easy to overlook, yet packing and dispatch are where a well-made bag can still be spoiled. Protective wrapping, correct cartoning and accurate export labelling are all part of the product, and a narrow or cluttered packing area will throttle output no matter how fast the lines run.
- Finished, inspected bags are counted and confirmed against the order.
- Each unit is protected with wrapping or a dust bag before cartoning.
- Cartons are labelled with the correct export marks and quantities.
- Goods are staged for loading, typically for FOB Xiamen shipment.
- Documents and inspection reports are prepared to accompany the shipment.
Questions to Ask as You Walk
A tour is an opportunity to ask questions that a brochure cannot answer. The most useful ones are open and specific, and they reveal whether the person showing you around understands the floor or only the sales story.
| Question | What a good answer sounds like |
|---|---|
| How is capacity stated? | A named reference mix, not a bare monthly number |
| Where is the approved sample kept? | A specific, accessible location on the floor |
| What happens when a lot fails inspection? | A defined remediation: rework, sort or reject |
| How long is sampling? | 6–10 working days, or 12–15 for complex builds |
| What is the bulk window? | 35–50 days after sample approval |
| Which materials are certified? | Specific claims, such as LWG or OEKO-TEX, with records |
Taken together, the answers and the floor give you a rounded picture that no document can. Where the arrangement of the space, the discipline of the staff and the answers to these questions all point the same way, you have found a programme you can build on. To see how the stages you observe fit into the whole, the leather bag manufacturing process guide traces the sequence from design to dispatch.
See the floor before you commit
Tell the programme team which stage of your launch you are planning and which questions matter most. They can arrange a walkthrough of the Quanzhou production floor, in person or by video, and answer the same questions a buyer would ask on the day.
Frequently Asked Questions
What should I look for on a bag factory tour?
Look for flow, housekeeping and quality presence. Material should move in a straight line from store to dispatch without doubling back. Aisles should be clear, bins labelled and floors free of debris under the machines. Most importantly, look for dedicated inspection stations with the approved sample physically present, because that shows quality is a scheduled stage rather than a final glance. Lighting at cutting, stitching and inspection points is a quick way to judge how seriously the floor takes its work.
How can I tell if a leather bag facility is well organised?
Organisation shows up as flow and order. Panels move forward through the line rather than back and forth, work-in-progress sits in moderate, sorted queues instead of unsorted piles, and each zone feeds the next without congestion. Labelled materials, retained swatches and a clear inspection area are further signals. A floor of any size that is arranged around the sequence of production will outperform a larger one that is arranged around available space.
What does the cutting room tell me about a factory?
A great deal, because cutting decides consistency and yield. Look at how hides are inspected and matched, how patterns are nested to avoid defects and align grain, and how skiving is set to the thickness on the tech pack. Panels should be numbered or bundled so matched pieces stay together. A cutting room run to habit and guesswork is usually matched by an assembly line doing the same, so it repays close attention rather than a hurried walk past.
What happens on the stitching lines in a leather bag facility?
Panels are joined into a formed bag at sequential stations arranged along the assembly sequence. The useful thing to observe is not the fastest operator but the movement of the bag: whether it advances steadily, whether jigs and guides keep stitches and hardware repeatable, and whether reinforcement is present at handle roots, gusset corners and strap anchors. In-process checks of stitch density and alignment during the run are a sign of a disciplined line.
Why is finishing the most revealing stage of a tour?
Because finishing is where craft and process meet, and where the smallest lapses are most visible to a customer. Edge painting or burnishing, hardware setting and branding are checked against the approved sample, and each has its own pass standard. A floor that treats finishing as an afterthought, with poor light or scattered tools, is signalling how it will treat your order. A dedicated finishing bench with the right tools tells the opposite story.
How should leather be stored in a factory?
Hides should be stored flat or rolled on racks, off the floor and away from direct light, heat and moisture, because leather is a natural material that responds to all three. Each bundle should be labelled by colour, thickness and supplier reference, and a retained swatch library should exist so incoming leather can be matched. Certification records for materials such as LWG-certified leather should be on file, not merely claimed.
What questions should I ask during a factory tour?
Ask how capacity is stated and whether it is tied to a named reference mix, where the approved sample is kept, and what happens when a lot fails inspection. Confirm the sampling time of 6–10 working days and the bulk window of 35–50 days after approval. Ask which materials are certified and whether records exist. Open, specific questions reveal whether the person guiding you understands the floor or is only repeating a sales story.
What does a well-lit inspection area tell me?
It tells you that quality is treated as a defined stage rather than an afterthought. Neutral, even lighting is essential for judging colour and finish, and the presence of the gold-sealed approved sample at the station shows that inspectors compare each unit against the reference rather than against a neighbour. If the reference sample is nowhere on the floor, ask where it lives, because its location tells you how it is used.
Is a bigger facility always better?
No. Scale matters, but layout and discipline matter more. A floor of the same size that is poorly arranged will produce less and inspect worse than a smaller one structured around flow. When assessing a facility, weigh how the space is zoned, how work-in-progress is managed and how quality is embedded, rather than the headline square footage alone. Capacity is a ceiling, and how well the floor is organised determines how much of that ceiling you actually get on any given order.
How is packing and dispatch handled in a leather bag facility?
After inspection, bags are counted and confirmed against the order, protected with wrapping or a dust bag, and cartoned. Cartons are labelled with the correct export marks and quantities, and goods are staged for loading, typically for FOB Xiamen shipment, with documents and inspection reports prepared to accompany them. Packing is part of the product: a well-made bag can still be spoiled in transit by careless wrapping or weak cartoning.
What is the difference between a showroom visit and a floor visit?
A showroom presents finished goods in ideal conditions; a floor visit shows the process that produced them. The floor reveals housekeeping, flow, work-in-progress and the presence or absence of quality stations, none of which a showroom can demonstrate. If a facility invites you only to a showroom, ask to see the production floor, because that is where the questions you actually care about are answered.
Can I verify a factory without travelling to China?
Yes. A structured video walkthrough covering the same zones a buyer would visit, combined with an independent third-party audit such as an SGS verification, can substitute for much of a physical visit. Request footage of the cutting room, the lines, the finishing bench and the inspection area, and ask the same open questions you would ask in person. Where possible, an unannounced or agency-conducted inspection adds confidence that the floor operates as described.
What red flags should worry me on a facility tour?
Watch for cluttered aisles, unsorted work-in-progress, poor lighting at inspection, and an absence of the approved sample. Staff who cannot explain the sequence they are working in, or who deflect questions about defect handling, are a further warning. A floor that looks busy but disorganised will carry higher rework risk, and a facility unwilling to show you the production area at all is telling you something before you have asked a single difficult question about quality or timelines.
How long does a useful factory tour take?
A meaningful walkthrough of the main zones takes around an hour to ninety minutes, plus time for questions. Rushing through in twenty minutes rarely gives you more than an impression, whereas following the flow from materials store to dispatch, pausing at cutting, assembly, finishing and inspection, allows you to see how each stage feeds the next. Allow additional time if you want to review documentation or discuss sampling and lead times in detail.
What role does the gold-sealed sample play on the floor?
It is the physical benchmark against which production units are judged, retained and marked by both buyer and supplier. On a tour, its presence at the inspection station shows that quality checks compare each bag against an agreed reference rather than a personal impression. Its absence is a signal worth probing, because an inspection cannot confirm compliance with a standard that is not physically available at the point of checking.
How does a facility tour help me choose between two suppliers?
A tour turns a comparison of quotes into a comparison of operations. Two suppliers may state similar capacity, lead times and prices, yet differ sharply in how their floors are organised, how work-in-progress is managed and how visibly quality is embedded. Seeing both floors lets you weigh those intangibles, which are often the real predictor of whether your order ships on time and to standard, rather than relying on numbers that look identical on paper and may behave very differently in production.
What technology should I expect to see on a modern production floor?
Expect cutting presses alongside skilled hand cutting, jigged and templated stitching stations, skiving machinery set to the tech pack, and a finishing bench with the tools each method requires. Increasingly, floors also use digital tools such as computer-aided pattern development, PLM systems for specifications, and digital inspection reports. These support the physical craft rather than replacing it, and their presence usually signals a programme that values both consistency and traceability across every stage of the run.