
Luxury standards in bag development are specifications rather than sentiments: a stated leather grade and temper, a defined stitch density, an edge finish described against a physical reference, a hardware finish with a durability requirement, and documented traceability for every material in the build. Premium houses expect all five to be written before sampling begins and verified before bulk is released. The cost of that discipline is real, and it is recovered through lower return rates, fewer disputes and a reputation that survives contact with the customer.
The word luxury is used loosely in sourcing conversations, which is precisely why it needs operational definition. Two brands can both be positioned at the top of the market and require entirely different things: one may prioritise a hand-finished edge and accept a longer timeline, another may prioritise flawless machine consistency and accept a slightly firmer temper. Both are legitimate. What matters is that the requirement is stated rather than assumed.
This article sets out the standards that premium programmes typically specify, how each is verified, and what the discipline costs in time and money. It reflects the specification work the programme team undertakes on our SGS-verified production floor in Quanzhou, Fujian.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
What a Luxury Standard Means Operationally
An operational standard has three parts: a measurable attribute, a stated tolerance, and a physical reference against which the tolerance is assessed. A requirement expressed only as an adjective cannot be verified, and an unverifiable requirement is one that will be argued about at inspection. Converting adjectives into those three parts is the first task of a premium specification.
| Adjective | Measurable attribute | Tolerance | Physical reference |
|---|---|---|---|
| Supple leather | Temper and thickness | Stated range in millimetres | Approved swatch |
| Flawless finish | Surface defect count per panel | Zero within defined zone | Photographed standard |
| Precise stitching | Stitches per centimetre | Stated count plus or minus one | Approved sample |
| Clean edges | Edge paint coverage and gloss | No visible gaps or ridges | Approved edge standard |
| Durable hardware | Plating thickness and cycle count | Stated minimum | Test report |
| Consistent colour | Shade against standard | Agreed visual tolerance | Approved dye-lot swatch |
The physical reference is the part most often omitted, and it is the part that makes the other two work. A tolerance has no meaning without something to measure against, and a colour code is not a physical object. Premium programmes hold approved standards for every visible attribute, and both parties keep a set, which is what allows a dispute to be settled by comparison rather than by assertion.
Material Standards at the Top of the Market
Material specification begins with grade and continues through temper, thickness, finish and provenance. Grade is the easiest to state and the least informative on its own: a full-grain hide can be excellent or mediocre depending on the selection within the grade. Temper and thickness determine how the material behaves in construction, and provenance determines whether the brand can make a defensible public claim about it.
Provenance has moved from a marketing question to a compliance one. A house publishing a sustainability statement needs the tannery status behind it, and needs that status to be current and in scope for the material actually used. Where a brand's own reporting requires it, the programme team holds those documents on file and supplies them with the specification rather than waiting to be asked at shipment.
Selection criteria deserve particular attention, because they are what separates a premium result from an average one within the same grade. Stating the maximum acceptable incidence of natural markings, and where on the panel those markings may appear, costs nothing in the specification and removes the most common source of disagreement about whether a hide is acceptable.
Construction Expectations: Edges, Stitching and Structure
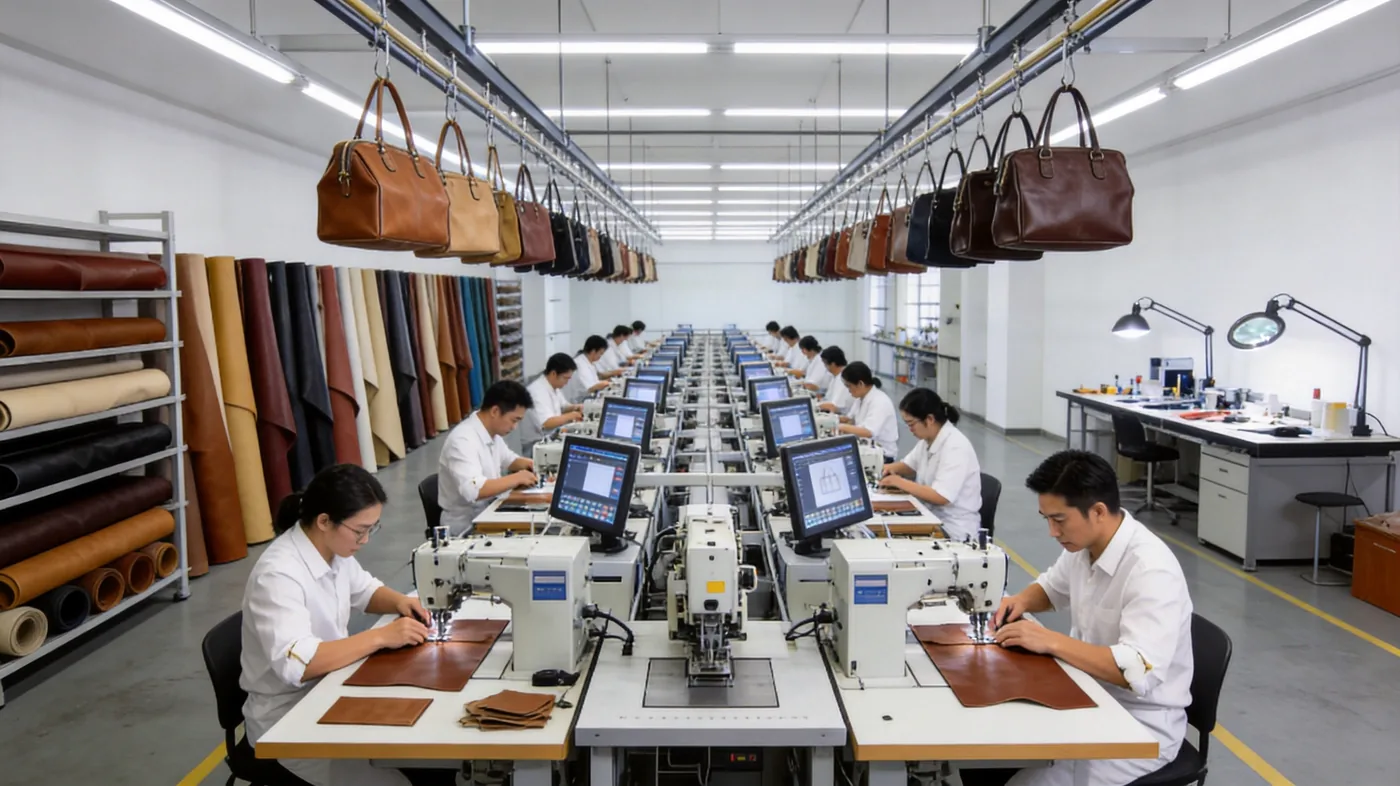
Construction is where luxury is most visible and most expensive. Edge finishing, stitch density and structural reinforcement are the three elements a customer assesses, often without knowing they are doing it, within seconds of picking a piece up. All three are specification decisions rather than consequences of skill alone.
| Element | Premium expectation | Common failure | Control |
|---|---|---|---|
| Edge finish | Even coverage, consistent gloss, no ridges | Uneven thickness, visible gaps | Photographed standard and defined application sequence |
| Stitch density | Stated count per centimetre, even spacing | Drifting spacing near corners | Defined count with tolerance; in-line check |
| Stitch line | Straight, consistent distance from the edge | Wandering at transitions | Stated offset from edge in millimetres |
| Structure | Holds shape, corners defined | Slumping or soft corners | Reinforcement specified by panel |
| Turning | Clean at corners and curves | Puckering at radii | Pattern notch and easing sequence specified |
| Interior | No visible adhesive, clean seams | Adhesive residue at seams | Defined assembly sequence and cleaning step |
Hand work and machine work are both capable of meeting these expectations, and the choice is commercial rather than moral. Hand saddle stitching is slower and produces a distinctive result; machine stitching at high density with good tension control is more consistent across a large run. Premium programmes frequently combine them, using machine work for long runs and hand finishing at the points a customer touches.
The specification should say where each applies. A requirement for hand finishing stated globally is expensive and slows the run; the same requirement applied to the handle attachment and the visible top edge delivers most of the perceived benefit at a fraction of the labour content.
Hardware Standards and Finish Durability
Hardware is judged on three things: how it looks when new, how it looks after a season, and how it feels in the hand. The first is a specification question about finish; the second is a testing question about plating and coating durability; the third is a sourcing question about the base metal and the weight of the component.
- Plating thickness stated in microns, with a minimum rather than a nominal figure.
- Salt spray or equivalent corrosion testing with a stated hours-to-failure requirement.
- Cycle testing on zips, locks and clasps against a defined count rather than by feel.
- Colour consistency across the run, assessed against a physical approved fitting.
- Weight and base metal specified, since lightness is noticed immediately at this level.
- Lead and nickel content compliant with REACH for the EU and CPSIA where applicable.
Colour consistency across a run is the hardware failure most often discovered too late, because a single approved sample looks correct and tells the buyer nothing about the distribution. Requesting a small production batch of fittings for approval, separate from the bag sample, costs very little and removes that risk entirely.
Compliance on metal content is straightforward to specify and easy to forget. REACH restricts certain substances in articles sold into the EU, and CPSIA sets limits for products within its scope in the United States. Stating the requirement at specification means the hardware is sourced to it, rather than tested after the fact and potentially rejected.
Interior Standards: What the Customer Finds Second
The exterior sells the piece and the interior keeps the customer. Lining material, pocket construction, closure quality and the absence of visible adhesive are all assessed at the moment of first use, which is also the moment the purchase decision is either confirmed or regretted. Interior specification deserves the same rigour as the exterior and frequently receives less.
| Interior element | Premium expectation | Where programmes under-specify |
|---|---|---|
| Lining material | Matched to the exterior in quality perception | A generic lining on a premium shell |
| Pocket construction | Reinforced at stress points, cleanly bound | Raw edges inside pockets |
| Device sleeve | Suspended and padded, sized to a stated device | A flat sleeve that transmits shock |
| Closure | Smooth operation, silent, aligned | Stiff zips and misaligned magnets |
| Adhesive visibility | None visible anywhere | Residue at seam junctions |
| Branding inside | Consistent with the exterior method | An interior label cheaper than the exterior one |
The device sleeve is the most functionally consequential element and the most frequently improvised. A sleeve that is flush with the bag's base transmits every knock directly to the device, and a suspended, padded sleeve costs very little more. Stating the device dimensions the sleeve must accommodate converts this from a judgement call into a measurable requirement.
Documentation, Traceability and Audit Readiness
Premium houses increasingly treat documentation as part of the product. A material cannot be described publicly as responsibly sourced unless the chain behind it can be evidenced, and that evidence has to exist at the point of claim rather than be assembled after a challenge. Audit readiness is therefore a specification output, not an administrative afterthought.
Batch traceability is the element that most programmes lack and most audits request. Linking a production batch to the material lots used and to the inspection record for that batch allows a specific question about a specific shipment to be answered with evidence. Without it, the answer is a general assurance, which is rarely sufficient once a retailer or regulator is involved.
A change log is the least glamorous document in a programme and one of the most useful. Every amendment to the specification, however small, should be recorded with the date, the reason and the approver, because the questions that arise months later are almost always about when a decision was taken and by whom. Without the log, both parties reconstruct events from memory, and memory is generous to whoever is speaking.
Inspection and Acceptance Criteria for Premium Runs
Acceptance criteria should be agreed before production, because everything agreed afterwards is a negotiation under time pressure. The standard release basis is AQL 2.5 under ISO 2859-1, single sampling at general level II, with defects classified as critical, major and minor. Premium programmes frequently tighten the major defect threshold, which is reasonable and should be priced, since it increases rework.
| Defect class | Typical example | Premium programme position |
|---|---|---|
| Critical | Broken hardware, failed closure, unsafe component | Zero tolerance in every programme |
| Major | Visible surface damage, misaligned panel, colour variation beyond tolerance | Tighter limit than standard; often zero on visible faces |
| Minor | Slight stitch irregularity, minor edge variation on a hidden face | Standard AQL 2.5 limit |
| Functional | Stiff zip, weak magnet, strap slip | Tested by cycle count, not by appearance |
| Packaging | Damaged or incorrect presentation | Inspected as part of the shipment |
The classification of what counts as a visible face is worth specifying explicitly, because it determines how many pieces in a run are assessed against the strictest threshold. A structured handbag has more visible faces than a soft tote, and the inspection plan should reflect the style rather than apply one rule to every piece in the range.
What Premium Standards Cost, and Where They Pay Back
Higher standards cost money in three places: better materials, more labour per unit, and a slower line. They pay back in four: lower return rates, fewer rejected shipments, longer selling life, and the ability to hold price. The net effect across a programme is usually positive within two seasons, which is why established premium houses specify tightly and new entrants should build towards it.
| Cost | Incurred | Return | Realised |
|---|---|---|---|
| Better material selection | Per unit, at purchase | Lower return rate | Season one onward |
| Hand finishing at touch points | Per unit, in labour | Higher perceived value | At point of sale |
| Tighter inspection limits | Per run, in rework | Fewer rejected shipments | Immediately |
| Documentation and traceability | Per programme, one-off | Audit and retail readiness | On first audit or listing |
| Longer development phase | Once, at specification | Fewer sample rounds | From the second style |
The one-off costs are the easiest to justify, because they do not repeat. Documentation and a longer specification phase are paid once and serve every subsequent style in the programme, which is why the discipline becomes cheaper the longer a brand stays with the same partner and the same specification language.
Set a premium specification with the programme team
Share your positioning, target price band and market list, and we will return a written specification with measurable tolerances, physical reference standards and an inspection plan. Development is coordinated from our production floor in Quanzhou, Fujian. Write to service@junyuanbags.com or message WhatsApp +86 177 5002 0688.
Frequently Asked Questions
What standards do luxury labels expect from a bag programme?
A stated leather grade, temper and thickness, a defined stitch density, an edge finish described against a physical reference, hardware with a durability requirement, and documented traceability for every material. Premium houses expect all of these written before sampling and verified before bulk release, rather than expressed as adjectives.
How is a luxury standard defined in a way that can be verified?
By giving each attribute three parts: a measurable characteristic, a stated tolerance, and a physical reference to measure against. A tolerance without a physical reference cannot be assessed, and a colour code is not a physical object, which is why approved standards held by both parties are essential.
What leather specification do premium programmes use?
Grade, temper, thickness, finish and provenance, with selection criteria stated within the grade. Grade alone is the least informative element, since a full-grain hide varies considerably. Stating the acceptable incidence of natural markings and where they may appear removes the usual disagreement about whether a hide is acceptable.
Should premium bags be hand-stitched or machine-stitched?
Both are capable of meeting premium standards, and the choice is commercial. Hand saddle stitching is slower and distinctive; high-density machine stitching is more consistent across large runs. Many premium programmes combine them, using machine work for long seams and hand finishing at handle attachments and visible edges.
What hardware standards apply at the luxury level?
Plating thickness stated in microns as a minimum, corrosion testing with a stated hours-to-failure requirement, cycle testing on zips and clasps rather than assessment by feel, colour consistency across the run against an approved fitting, and REACH or CPSIA compliance on metal content as the market requires.
How is colour consistency managed in a premium run?
Through a physical approved standard held by both parties, with tolerance expressed as a comparison against that standard. For hardware, approving a small production batch of fittings separately from the bag sample removes the risk, since a single sample says nothing about distribution across the run.
What documentation should a luxury programme hold?
Material declarations covering composition and origin, Leather Working Group tannery status where a claim is published, OEKO-TEX and REACH documentation as applicable, an AQL inspection record per run, batch traceability linking production to material lots, and a change log recording every specification amendment.
What is batch traceability and why does it matter?
It links a production batch to the material lots used and to the inspection record for that batch. It allows a specific question about a specific shipment to be answered with evidence. Without it, the response to an audit or retailer enquiry is a general assurance, which is rarely sufficient once a regulator is involved.
What inspection standard applies to a luxury production run?
Release is made against AQL 2.5 under ISO 2859-1, single sampling at general level II, with defects classified as critical, major and minor. Premium programmes often tighten the major defect threshold, particularly on visible faces. That is reasonable and should be agreed and priced in advance.
How should visible faces be defined for inspection?
Explicitly, and per style. The definition determines how many pieces in a run are assessed against the strictest threshold, and a structured handbag has considerably more visible faces than a soft tote. Applying one rule across an entire range is the common error and produces either unnecessary rejects or avoidable escapes.
What does a premium specification cost?
More, in three places: better materials, higher labour content per unit and a slower line. It returns that cost through lower return rates, fewer rejected shipments, longer selling life and the ability to hold price. Across a programme the net effect is usually positive within two seasons.
Why does documentation matter for a luxury brand?
Because a public claim has to be defensible. A material cannot be described as responsibly sourced unless the chain behind it can be evidenced, and the evidence must exist when the claim is made rather than be assembled after a challenge. Documentation is therefore a specification output.
How are interior standards specified for premium bags?
Lining material matched in perceived quality to the exterior, pockets reinforced and cleanly bound, a suspended and padded device sleeve sized to a stated device, closures aligned and smooth, no visible adhesive, and interior branding consistent with the exterior method.
What is the most commonly under-specified element in a premium bag?
The device sleeve. A sleeve flush with the bag's base transmits every knock to the device, while a suspended and padded sleeve costs very little more. Stating the device dimensions that must be accommodated converts the question from a judgement call into a measurable requirement.
How long does development take at premium standards?
Sampling runs six to ten working days and twelve to fifteen for complex constructions, with bulk production thirty-five to fifty days after approval. Premium standards lengthen the specification phase rather than production, and front-loaded specification work usually reduces the number of sampling rounds needed.
What is the minimum order for a premium bespoke programme?
Five hundred pieces per style and colourway is the standard starting point, reflecting material purchasing and line setup economics. Small-batch pilots are available for houses testing a silhouette or managing a limited launch, and the programme team will advise which structure suits the positioning and channel.