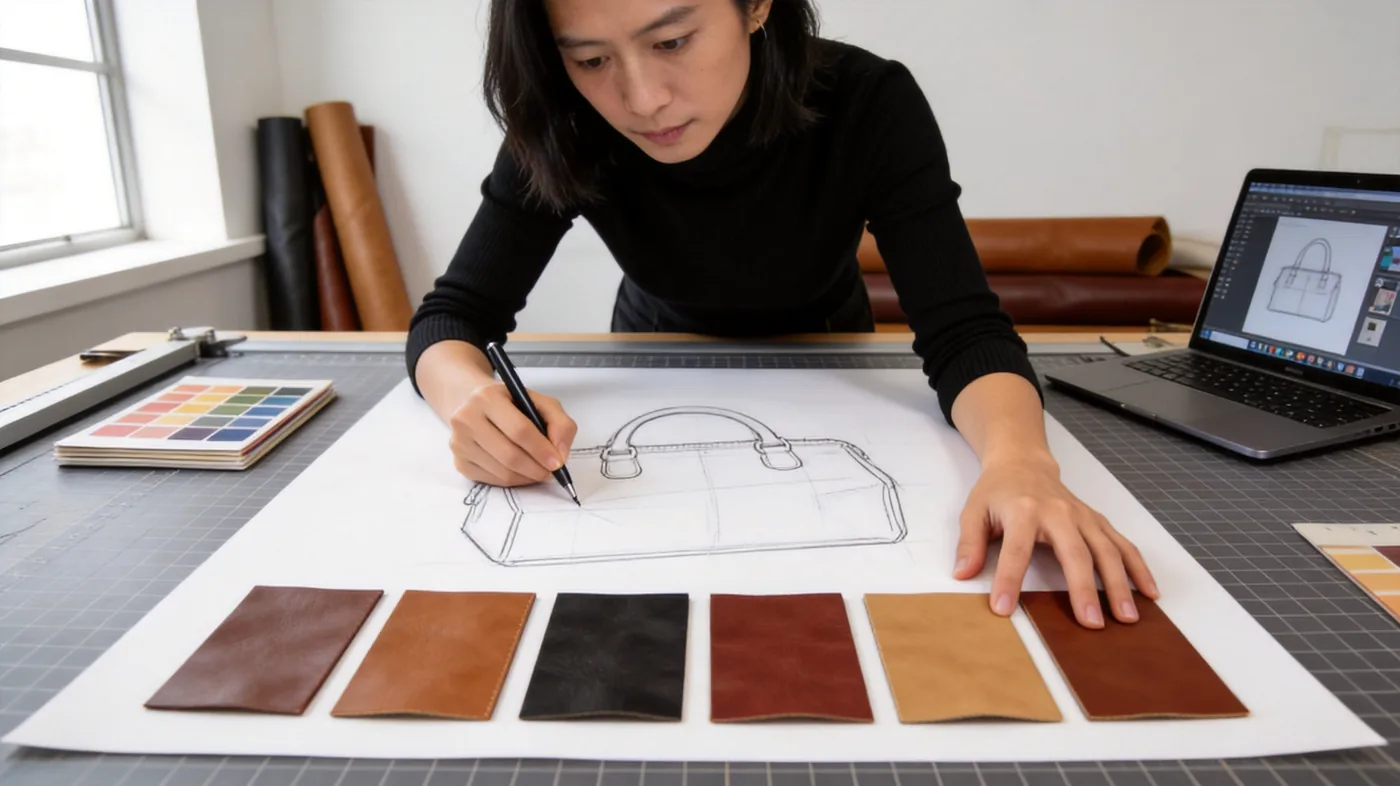
Custom leather handbags are defined less by their silhouette than by three specification layers: the hide, the hardware and the finish. The hide sets hand, weight and how the bag ages; the hardware sets the tactile impression and the mechanical life; the finish — edges, seams, lining, branding — is where a customer subconsciously judges whether a bag was made carefully. This article walks through each layer in specification order, with the trade-offs that matter at production scale rather than at sample scale.
The ordering is deliberate. Material and hardware decisions are expensive to reverse once cutting has begun, while finish decisions can often be adjusted on the second sampling round. Specifying in this order means the costly variables are resolved first, when they are still cheap to change.
Choosing the Hide: Temper, Weight and Grade
Three independent variables describe a hide, and conflating them is the most common specification error. Grade describes where in the hide the panel comes from and how much natural character it retains. Temper describes how stiff or supple it is. Thickness describes its weight in millimetres, and is only partly related to either.
| Variable | What it governs | Typical range in handbags | Specification risk |
|---|---|---|---|
| Grade | Surface character, durability, price and yield | Full-grain, top-grain, corrected grain, bonded | Assuming a grade name means the same thing across tanneries |
| Temper | Whether the bag holds shape or drapes | Firm, medium, soft | Specifying shape without specifying temper |
| Thickness | Weight, structure and edge bulk | Roughly 0.8 mm to 2.2 mm depending on element | Specifying one thickness for every panel |
| Cut area | Yield and cost, plus consistency of grain direction | Panel size relative to hide size | Ignoring that large panels cost disproportionately more |
| Finish type | Marking resistance, colour consistency, ageing | Aniline, semi-aniline, pigment, waxed | Expecting an aniline hide to behave like a pigmented one |
A single bag usually needs more than one thickness. Handles, strap ends and base panels want a heavier substance; gussets and linings want something lighter so that seams do not bulk. Specifying one figure across the whole bag produces either a heavy, awkward object or one that fails at the handle attachment.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Surface Finishes and What They Actually Do
A finish is a treatment applied after tanning, and it determines three things a customer will notice: how the surface catches light, how it resists marking, and how it changes over years. The same base hide can be finished several ways and read as entirely different products.
| Finish | Appearance | Marking resistance | Ageing behaviour | Suited to |
|---|---|---|---|---|
| Aniline | Transparent, shows natural grain and pores | Lowest; absorbs moisture and marks | Develops rich patina | Craft-led and heritage positioning |
| Semi-aniline | Mostly natural with light protective layer | Moderate | Develops patina more slowly | Mainstream luxury |
| Pigmented | Opaque, uniform colour, consistent | High | Little change over time | Volume programmes needing consistency |
| Saffiano and pressed grain | Cross-hatch or pebbled embossed texture | High; texture hides wear | Very stable | Daily-use and travel-adjacent styles |
| Waxed and pull-up | Mottled, lightens where flexed | Moderate; marks can be rubbed out | Pronounced, characterful change | Casual luxury and menswear |
| Patent and high-gloss | Mirror surface | High on the surface, vulnerable to scuffing | Can yellow or craze over years | Evening styles |
Choose a finish by intended use rather than by appearance alone. An aniline hide on a bag carried daily through a commute will acquire character, which some brands intend and some customers will read as damage. Where the brand promise is consistency across a global assortment, a pigmented or pressed finish reduces returns far more effectively than any care instruction.
Colour: Specification, Dyeing and Consistency
Colour is the specification most likely to fail silently. A shade approved on a swatch in one city, viewed under different lighting, cut from a different dye lot, will not match the bag that ships. The controls that prevent this are procedural rather than technical.
- Approve against a physical reference, retained by both parties, rather than a photograph or a screen colour.
- State the lighting under which approval was given, since metamerism makes two panels match under one source and not another.
- Reference a dye lot and ask whether the same lot will be available for the reorder, because re-dyeing is rarely exact.
- Specify a tolerance using a recognised grey scale or an agreed pair of limit swatches, so acceptance is measurable.
- Approve lining and thread together with the shell, because a lining approved separately frequently clashes once assembled.
For bespoke colourways, expect a minimum dye quantity that may exceed what the first order consumes. That is not a padding exercise; dyeing is a batch process and the minimum is set by the vat. The surplus is normally reserved against future reorders, which is useful for consistency and inconvenient for working capital.
Hardware: Base Metal, Plating and Mechanical Life
Hardware carries two separate responsibilities. Aesthetically it sets the temperature of the bag — warm, cool, bright or subdued. Mechanically it is the only part of a bag that has a cycle life, and it is the part most likely to generate a warranty claim.
| Element | Common options | Aesthetic effect | Mechanical consideration |
|---|---|---|---|
| Base metal | Zinc alloy, brass, stainless steel, aluminium | Determines weight and sound | Brass and steel tolerate wear better than plated alloy |
| Plating | Gold, palladium, nickel, gunmetal, antique brass, ruthenium | Sets the house finish | Plating thickness governs how long the finish survives |
| Zips | Metal teeth, coil, with metal or leather pull | Weight and smoothness of travel | Test full travel repeatedly on the sample |
| Closures | Turnkey, twist, magnetic, snap, zip | Recognition and ritual | Magnetic closures need shielding consideration |
| Feet and studs | Set into a reinforced base | Signals construction care | Must sit flush or they mark furniture |
| Chain and rings | Welded or cast links, split rings | Jewellery-like detailing | Weight affects both cost and freight |
Specify plating thickness rather than merely naming a colour. Two suppliers quoting "gold" may be quoting different thicknesses over different base metals, and the difference becomes visible within months of daily use. Where a bag will be carried daily, a thicker plating over brass or steel is usually a better specification than a thicker casting over alloy.

Edge and Seam Finishes
Edges are the most reliable indicator of finishing discipline in a finished bag, because they cannot be faked at the last moment. A clean edge requires the underlying plies to have been prepared properly; a poor one reveals every shortcut taken earlier.
| Finish | Method | Appearance | Cost and durability |
|---|---|---|---|
| Painted edge | Coats applied, dried and sanded between applications | Smooth, uniform, colour-matched or contrast | Higher labour; durable when applied correctly |
| Burnished edge | Heat, wax and friction on a bare fibre edge | Slightly rounded, natural, subtle sheen | Moderate labour; excellent on vegetable-tanned |
| Turned edge | Leather wrapped and folded over a seam | Soft, rounded, no visible cut | Highest labour; the most refined result |
| Raw or cut edge | Left as cut, sometimes sealed | Utilitarian, softens with use | Lowest cost; absorbs moisture |
| Bound or piped edge | Separate strip folded and stitched over the edge | Defined, decorative, structural | High labour; adds a design element |
Seam specification runs alongside. Stitch density affects both appearance and strength; too dense perforates the leather, too sparse weakens the seam. Thread material matters as much: bonded nylon and polyester behave differently from cotton under load and over time, and a thread that fades faster than the hide produces a visibly aged bag within a season.
Lining and Interior Specification
The interior is where a customer forms a private judgement about value. Nobody photographs it, everybody touches it, and a poor lining undermines a good shell more reliably than any exterior flaw.
Where the interior carries a print or weave, remember that textile components fall under OEKO-TEX confidence schemes and, in the European Union, under REACH restricted-substance requirements. Specifying a lining without confirming its documentation is a common cause of a delayed retailer onboarding.
Branding and Logo Finishes
Branding should be chosen for permanence and legibility at the distance a customer actually views it. Many programmes over-invest in an interior logo and under-invest in the one element seen in every photograph.
| Method | Process | Best substrate | Durability | Cost structure |
|---|---|---|---|---|
| Blind deboss | Heated die pressed into the surface with no colour | Vegetable-tanned and aniline leather | Permanent; deepens with patina | Die cost; negligible per unit |
| Foil stamp | Heat and pressure transferring metallic or pigment foil | Pigmented and smooth finishes | Good; can abrade at high-wear points | Die plus foil; low per unit |
| Emboss | Raised relief from a matched die pair | Firm, thicker hides | Permanent; vulnerable to crushing | Two dies; moderate per unit |
| Metal logo plate | Cast or stamped plate riveted or stitched in place | Any; reinforces the attachment point | Very high | Tooling plus unit cost |
| Woven or printed label | Applied to lining or interior seam | Textile linings | Moderate; may curl with cleaning | Low tooling; low per unit |
| Laser marking | Controlled surface ablation | Certain coated and synthetic surfaces | Variable by substrate | No tooling; per-unit time |
Placement deserves as much attention as method. A logo placed over a seam, near a stress point, or where the panel flexes will distort regardless of how well it was applied. Mark the exact position on the tech pack in two dimensions, and confirm it on the sample rather than assuming the pattern room will choose well.
Matching Specification to Price Point
Every specification decision sits somewhere on a cost curve, and the skill is spending where customers perceive it. The table below distributes a fixed budget across the three layers for three broad positions.
| Position | Hide | Hardware | Finish | Where the money shows |
|---|---|---|---|---|
| Accessible luxury | Corrected or top-grain with a pressed finish | Catalogue fittings in a consistent single finish | Machine-applied edge paint, clean interior | Consistency and clean assembly |
| Mid luxury | Full-grain or top-grain with a semi-aniline finish | Selected catalogue plus one bespoke element | Multi-coat painted edges, signature lining | Material hand and one distinctive fitting |
| Top luxury | Full-grain aniline or a specified exotic, sorted panels | Bespoke fittings with specified plating thickness | Turned or hand-finished edges, detailed interior | Everywhere, including the interior nobody photographs |
The most common misallocation is spending on interior complexity while the exterior material reads cheaply. Customers assess the shell at arm's length and the interior only after purchase. Where the budget is genuinely fixed, upgrading the hide by one tier usually delivers more perceived value than any interior addition.
It is also worth deciding the specification in two passes. The first pass sets the ideal combination without reference to cost; the second brings it back inside the landed ceiling by changing one layer at a time, starting with hardware tooling and interior complexity. Working in that order keeps the material hand intact, which is the layer customers judge first and the one most easily lost to across-the-board cost cutting.
Specify materials, hardware and finishes
Send your target price point, silhouette and intended market. The programme team in Quanzhou will return a layered specification with hide, finish, hardware and branding options that fit the budget.
Frequently Asked Questions
What leather is best for custom leather handbags?
It depends on the silhouette and the use. Full-grain bovine suits structured bags because it holds shape and develops patina. Top-grain with a pressed finish suits volume programmes needing colour consistency. Soft nappa suits slouchy shapes but marks easily. Specify grade, temper and thickness separately, because a single bag usually needs more than one thickness.
What is the difference between aniline and pigmented leather?
Aniline leather is dyed with transparent dye and retains its natural surface, so it shows grain and pores, absorbs moisture and develops a rich patina. Pigmented leather carries an opaque surface coating, which gives uniform colour and strong marking resistance but little change over time. Choose aniline for character and pigmented for consistency.
How thick should leather be for a handbag?
There is no single figure. Heavy elements such as handles, base panels and strap ends want a heavier substance, while gussets and linings want something lighter so seams do not bulk. Specifying one thickness across the whole bag produces either an awkward heavy object or a bag that fails at the handle attachment.
Which hardware finish lasts longest?
Plating thickness and base metal matter more than colour. A thicker plating over brass or stainless steel outlasts a thin plating over alloy, whatever the shade. Specify thickness in the technical pack rather than naming a colour, and check that every fitting in the bag shares one plating standard to avoid visible mismatch.
What is the most durable edge finish?
A turned edge is the most refined and, when executed well, among the most durable, because the leather is wrapped rather than cut. Multi-coat painted edges perform well when each coat is dried and sanded properly. Burnished edges suit vegetable-tanned leather. Raw cut edges are cheapest but absorb moisture and wear visibly.
How do I keep leather colour consistent across orders?
Approve against a physical reference swatch retained by both parties, state the lighting used, and reference the dye lot. Ask whether the same lot will be available at reorder, because re-dyeing is rarely exact. Specify a measurable tolerance using a grey scale or agreed limit swatches so acceptance is a measurement rather than an argument.
Is branded hardware worth the tooling cost?
It is worth it for one element, usually the closure or the zip pull, because those are the components customers touch and photograph most. Using bespoke tooling across every fitting consumes development budget with diminishing recognition. Catalogue fittings in a consistent, distinctive finish deliver much of the same impression at far lower cost.
What lining materials work best in leather handbags?
Microfibre suede gives a soft, luxurious hand with better marking resistance and lot consistency than split suede. Cotton twill and canvas are natural and inexpensive but need treatment in light colours. Performance synthetics suit daily-use and travel-adjacent bags. Confirm textile documentation such as OEKO-TEX before specifying a printed lining.
Does sustainability certification affect material choice?
It narrows the field and should be decided early. Leather Working Group tannery protocols support traceability claims, OEKO-TEX covers textile components, and REACH governs restricted substances for the European Union. Naming these in the brief at selection stage avoids the common problem of discovering mid-season that a chosen material lacks documentation.
How do I choose hardware that matches the leather?
Decide one metal family for the whole programme and hold it across every style. Warm finishes such as brass and gold tend to suit vegetable-tanned and aniline hides; cooler finishes such as palladium, nickel and ruthenium suit pigmented and pressed surfaces. Consistency across the range matters more than matching any individual bag.
What is the difference between debossing and embossing?
Debossing presses a heated die into the surface so the mark sits below it, and it can be blind, with no colour, or filled with foil. Embossing raises the mark above the surface and needs a matched pair of dies. Debossing is more common on leather, more durable at wear points, and cheaper because it requires one die.
Can I mix leather and textile in one bag?
Yes, and it is often a good way to manage weight and cost. The practical issues are that each material needs its own marker and yield calculation, seam allowances differ, and the two may need different adhesives. Mixed-material construction raises labour minutes, so it should be a deliberate design decision rather than a cost-saving measure.
How does hardware weight affect the finished bag?
Weight affects perceived quality, user comfort and freight cost. Heavy cast fittings read as substantial but add load at their attachment points, so panels behind them need reinforcement or the fitting will print through. They also raise dimensional weight in shipping, which matters more than most buyers expect on a large programme.
Should thread match the leather or contrast?
It is a design decision that should be made explicitly rather than left to the pattern room. A matching thread gives a quiet, refined result; a contrast thread makes construction visible and reads as crafted. Either way specify the thread material, because one that fades faster than the hide will make the bag look prematurely aged.
What causes plating to wear off hardware?
Thin plating over an unsuitable base metal, abrasion at contact points such as feet and zip pulls, and exposure to moisture or cosmetics. Specify plating thickness and base metal in the technical pack, and consider a more robust specification on the components that touch surfaces most. Testing against recognised abrasion methods gives comparable evidence.
How much does material choice affect unit cost?
Material usually dominates the quotation, and not only through purchase price. Yield, handling difficulty and reject rate compound the effect: a hide that costs more to buy may cost less per finished unit if it cuts cleanly, while a cheaper one requiring extensive sorting can reverse the arithmetic entirely.
What should be on a hardware schedule?
Every fitting by function, each with its base metal, plating and thickness, finish reference, quantity per bag, attachment method and reinforcement requirement. Including the attachment method and reinforcement prevents the most common hardware failure, which is a fitting that pulls through a panel never specified to carry it.
Do exotic materials need extra documentation?
Yes. Species covered by trade controls require permits, and the usable area of a skin is defined by those documents rather than by the skin itself. This adds administrative labour and constrains panel layout, which is why exotic specifications carry both a higher material cost and a higher development cost.