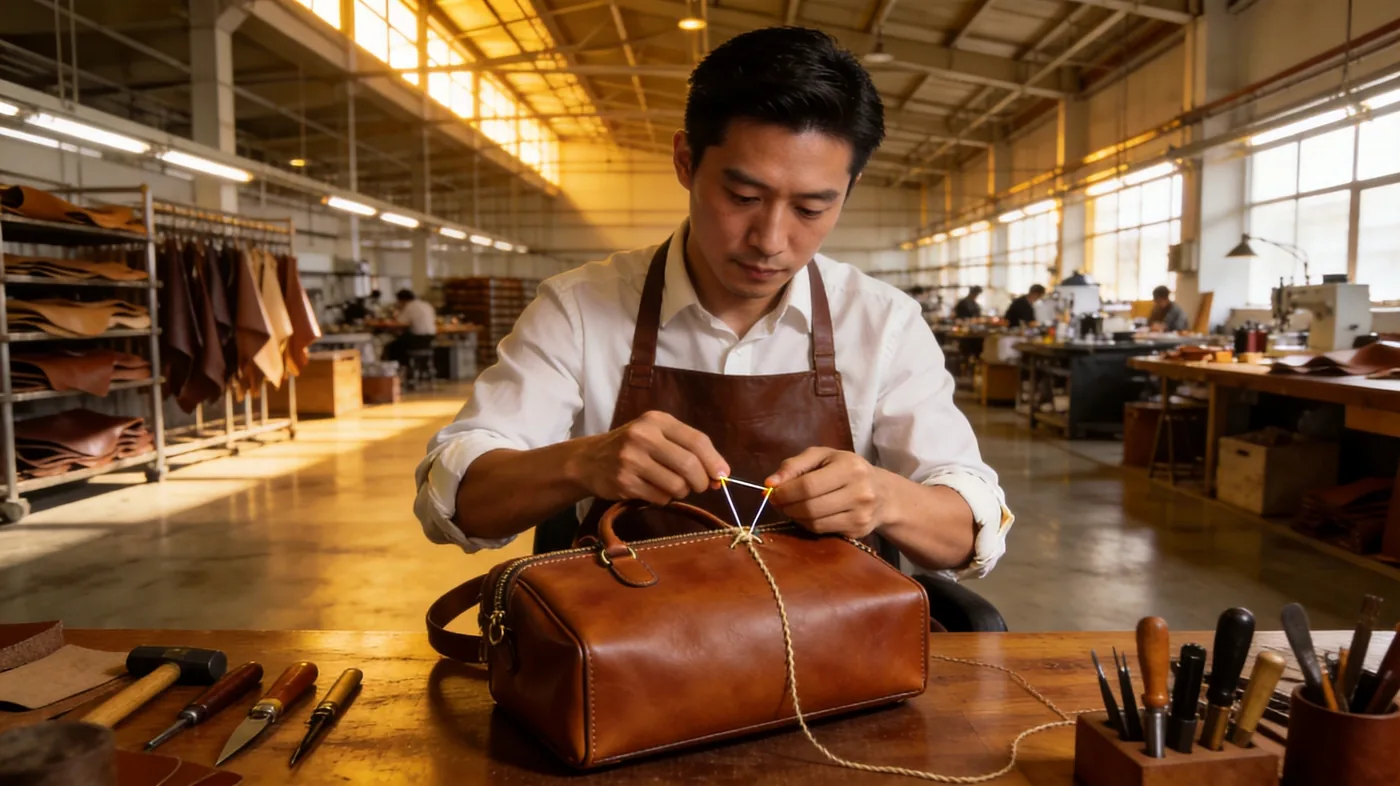
Full-grain leather keeps the hide's dense outer layer and its natural grain intact, with no sanding or correction to remove surface marks, which is why it is stronger, more breathable and more characterful than any lower grade. It is also the most demanding grade to buy well, because selection waste is higher and cutting yield per hide is lower than for corrected leathers. Full grain suits bags designed to age visibly at premium price points; corrected top-grain serves programmes where uniformity and yield matter more. This article sets out how the grade is defined, how tannage and finish change performance, and how to write a specification that suppliers can quote against without interpretation.
The phrase gold standard is used loosely in retail copy, and that looseness is the reason so many full-grain briefs produce disappointing samples. The grade describes an anatomical fact about the hide, not a guarantee of quality. A full-grain hide of poor selection, badly tanned and heavily finished will underperform a well-made corrected leather in almost every measurable respect. What full grain offers is the highest ceiling, not an automatic result.
For designers the practical question is narrower: which parts of a collection justify the ceiling, and which parts are better served by a grade that costs less and behaves more predictably. Answering that question requires understanding what happens to a hide between the abattoir and the cutting table.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
What full grain actually means
A hide has two principal layers. The corium, or grain layer, sits at the top where the hair once grew; the fibrous layer below is looser and less dense. Full grain is the top cut, retaining the grain surface with its pores, follicle pattern and natural markings intact. Nothing has been sanded away, so the fibre structure that gives leather its tensile strength remains whole. Any hide that has been abraded to remove scars, insect bites or stretch marks has, by definition, become top grain rather than full grain, regardless of how it is described in a quotation.
Natural markings are therefore a feature rather than a fault. Neck wrinkles, healed scratches and variation in pore density are the evidence that the surface has not been altered. Designers who want a perfectly uniform panel are, in effect, asking for the one thing full grain cannot give, and the honest answer in that case is a corrected grain with an embossed or pigmented finish.
- Grain surface intact: pores and follicle pattern visible under magnification, no abrasion marks.
- No correction: scars, wrinkles and healed defects remain part of the surface character.
- Full fibre density: the strongest layer of the hide is retained across the whole panel.
- Breathable hand: an open grain surface absorbs and releases moisture differently from a coated one.
- Variable appearance: every hide differs, so panels from one bag to the next will never match exactly.
Tannage: how the hide is stabilised
Tanning converts a perishable raw material into a stable one, and the method chosen shapes everything that follows. Vegetable tannage uses plant-derived tannins and produces a firm, warm-toned leather that darkens with light and use, and that can be burnished to a smooth edge without additional finish. Chrome tannage is faster, yields a softer and lighter leather with good thermal stability, and dominates volume production. Combination tannage sits between the two and is frequently used on bag leathers where a designer wants some of the vegetable character without the full cost and stiffness.
Retannage, fatliquoring and drying complete the picture, and each step is a place where cost is either spent or saved. A leather rushed through drying will be boardy and will crack at fold lines; insufficient fatliquor produces a dry handle that fails flex testing. These are process failures rather than grade failures, and no amount of selection at the cutting table will correct them.
| Tannage | Hand and appearance | Best suited to | Watch for |
|---|---|---|---|
| Vegetable | Firm, warm tone, darkens with age | Structured bags, burnished edges | Longer tannage cycle, firmer hand |
| Chrome | Soft, light, supple, stable colour | Slouchy shapes, linings, volume runs | Less natural patina development |
| Combination | Balanced firmness with softer drape | Most designer bag programmes | Specification varies widely by tannery |
| Chrome-free or aldehyde | Pale base, firm, good for light colours | Brands with chrome restrictions | Narrower supplier base, higher cost |
Finish systems: aniline, semi-aniline and pigmented
The finish is where many full-grain specifications quietly collapse. Aniline finish uses soluble dyes with no pigment layer, leaving the grain fully visible and the hand at its most natural; it is also the least protected treatment available and marks readily. Semi-aniline adds a small amount of pigment for uniformity and protection while keeping the grain readable. A pigmented finish lays a polymer coating across the surface, which improves stain resistance and hides defects but closes the pores and changes how the leather feels and ages.
A full-grain leather with a heavy pigmented finish is technically full grain and practically behaves like a corrected leather. That is not a criticism; it is often the right commercial answer for a bag that will be carried daily in a city. It is, however, a decision the designer should make deliberately rather than discover when a sample arrives shinier than expected.

Strength, patina and the argument for ageing
The durability case for full grain rests on fibre density rather than on romance. Because the grain layer has not been abraded, tear strength and abrasion resistance are measurably higher than in corrected equivalents at comparable substance. The second part of the case is behavioural: an unfinished or lightly finished surface records use rather than resisting it, so a scuff becomes part of the appearance instead of a defect against it. Corrected leather with a polymer coating cannot do this; its coating wears through to a different colour, which reads as damage.
| Property | Full grain | Corrected top grain |
|---|---|---|
| Tear strength | Highest at equal substance | Reduced by abrasion of grain layer |
| Abrasion behaviour | Records wear, develops sheen | Coating wears through, shows base |
| Breathability | Open pore structure | Substantially closed by finish |
| Panel uniformity | Low, varies by hide and position | High, engineered surface |
| Cutting yield | Lower, defects must be cut around | Higher, fewer defects to avoid |
Patina is the visible record of that process, and it is the reason heritage houses build their identity on full-grain materials. It is also a commercial risk for brands whose customers expect a bag to look new after a season. The decision belongs with the brand positioning, not with the tannery.
Cutting yield, grading and what the grade costs
Full grain costs more per finished bag for a reason that has little to do with the price of the hide. Cutting yield does. A hide carries its defects in unpredictable places, and a cutter working with full grain must place pattern pieces around them, which reduces the number of usable panels per hide against a corrected leather of the same area. On structured bags with large uninterrupted panels, that reduction is material, and it is the single largest driver of the cost gap between grades.
Grading practice amplifies the effect. Tanneries grade hides on the number and severity of surface defects, and a designer who specifies a tight grade is paying for scarcity as much as for quality. Relaxing the grade by one step, or accepting natural marks in defined positions, frequently reduces unit cost by more than any negotiation on the tannery price. The programme team normally reviews the pattern against hide size before confirming a grade, because pattern layout and grade interact.
- Large uninterrupted panels: highest yield loss, specify grade carefully and allow for panel placement.
- Handles, straps and bindings: small pieces, defects easily avoided, full grain economical here.
- Gussets and interiors: interior surfaces can often run a lower grade without visible compromise.
- Multi-panel constructions: more seams but better yield than a single large panel.
- Colour consistency: darker shades conceal natural variation better than pale ones.
Where full grain belongs in a collection
A collection rarely needs one material. Full grain earns its place on hero pieces where the customer will touch the surface, where the price supports the waste, and where the brand wants visible ageing: structured totes, top-handle bags, weekenders and the outer faces of small leather goods. It is harder to justify on linings, on hidden structural layers and on high-volume promotional pieces where consistency across a large run is the governing requirement.
| Position in the collection | Grade typically specified | Reasoning |
|---|---|---|
| Hero tote, outer panels | Full grain | Surface is touched and seen, price absorbs yield loss |
| Gussets and bases | Full grain or heavy top grain | Strength required, natural marks barely visible |
| Straps and handles | Full grain | Small pieces, defects easy to cut around |
| Interior linings | Sueded split or microfibre | Cleanability and uniformity outweigh patina |
| High-volume promotional pieces | Corrected top grain | Uniform appearance across a long run |
The mixed approach is standard practice. A bag can carry full grain on its outer panels, a corrected or split leather on its gussets and interior, and a coated textile on its lining, with the specification stating where each is permitted. What matters is that the substitutes are named and approved before sampling, so that a substitution made for yield reasons does not become a surprise at pre-production.
Specifying and testing full grain before bulk
A full-grain specification worth quoting names the animal origin, the tannage, the finish system, the substance range, the colour reference with its tolerance, and the tests the material must pass. Common tests cover tear strength, flex resistance, rubbing fastness on both dry and wet cloth, and light fastness, with methods drawn from ASTM and ISO series depending on the market. The tannery tier is normally benchmarked against Leather Working Group audit protocols, and restricted substance declarations under REACH are standard for European delivery.
Finished goods released from our production floor in Quanzhou are inspected to AQL 2.5 under ISO 2859-1, single sampling, general level II, which is the point at which a material weakness that survived sampling becomes visible at scale. Sampling itself runs 6 to 10 working days for standard constructions and 12 to 15 for complex ones, so the material decision needs to be settled before that clock starts rather than during it.
- State animal origin and hide selection grade, not simply the word full grain.
- Name the tannage and the finish system, and confirm which of the two governs the hand.
- Give the substance range in millimetres with a tolerance the pattern can accept.
- Attach a physical colour reference plus the accepted tolerance under retail lighting.
- List the laboratory tests and the pass criteria for each, referencing the method used.
- Request tannery audit status and restricted substance declarations with the quotation.
- Approve the substitute grade in writing before the first sample is cut.
Buyers pay for full grain twice: once at the tannery and once in the cutting room.
Discuss a full-grain specification
Send your pattern, target price and intended finish, and the programme team will advise on grade, tannage and cutting yield before sampling begins. Contact service@junyuanbags.com, or reach the team on WhatsApp at +86 177 5002 0688.
Frequently Asked Questions
What does full-grain leather mean?
Full-grain leather is the top cut of a hide, retaining the outer grain layer with its pores and natural markings, without sanding or correction. Because the dense grain layer is intact, tear strength and abrasion resistance are higher than in corrected grades at equal substance. Natural marks such as healed scratches and neck wrinkles remain visible and are considered evidence that the surface has not been altered rather than defects.
Is full-grain leather worth the extra cost?
It is worth the premium where the customer touches the surface, where the price point absorbs the lower cutting yield, and where visible ageing supports the brand story. It is harder to justify on linings, hidden structural layers or high-volume promotional runs where uniformity governs. The yield loss on large uninterrupted panels is usually the deciding factor, so evaluate cost per finished bag rather than cost per square metre of hide.
How can I tell full grain from corrected top grain?
Examine the surface under magnification. Full grain shows an irregular pore and follicle pattern that follows the anatomy of the animal, with wrinkles and healed marks present. Corrected grain has been sanded and usually embossed, so the pattern repeats uniformly across the panel and pores are largely closed by finish. Ask the supplier to state whether any abrasion or embossing has been applied to the surface.
Does full-grain leather scratch easily?
Aniline and lightly finished full grain marks more readily than a pigmented corrected leather, because there is no polymer coating to absorb the abrasion. In practice the mark often rubs out or blends into the developing patina rather than remaining as a visible blemish. Pigmented full grain behaves much like a corrected leather. Choose the finish according to how the customer is expected to treat the bag rather than by grade alone.
What is the difference between full grain and top grain?
Top grain is the layer immediately below the surface once the grain has been sanded to remove defects, so it is full grain that has been corrected. The sanding produces a uniform surface and improves cutting yield, but it removes the densest fibre layer and closes the pore structure with finish. Full grain retains that layer and its natural markings. Both are genuine leather; they differ in strength, breathability and how they age.
Which tannage is best for a structured handbag?
Vegetable tannage gives the firmness and burnishing behaviour that structured bags need, along with a warm tone that darkens with use, but it is a longer process and a firmer hand. Combination tannage is the pragmatic choice for most designer programmes, offering body with a softer drape and broader colour availability. Chrome tannage is generally too soft for a bag that must hold its shape without reinforcement.
How thick should full-grain leather be for a handbag?
The right substance depends on whether the bag is structured or slouchy and on how much reinforcement the pattern carries. Structured designs need enough substance to hold shape, while soft shapes can run thinner and lighter. Handles and bases can run heavier than body panels. The reliable method is to build samples at two substances and compare them loaded and empty rather than choosing from a data sheet.
Does full-grain leather darken over time?
Most full-grain leather darkens, because light, handling and absorbed oils change the surface gradually. Vegetable-tanned and pull-up leathers darken most noticeably, while heavily pigmented full grain changes least. The rate depends on finish, colour and how the bag is carried. Brands should treat this as a design feature and show customers an aged reference, since expectations about ageing are a common source of dissatisfaction.
Can full-grain leather be embossed with a logo?
Yes, full grain takes blind embossing, foil stamping and debossing well, and the intact grain gives a crisp impression. Embossing works best on firmer tannages and on panels without heavy natural wrinkling, because wrinkles interrupt the impression. Always test the actual artwork on the production leather, since fine detail behaves differently on aniline and pigmented surfaces and the difference is visible on a shelf.
How does full-grain leather affect the minimum order quantity?
A standard programme starts at 500 pieces per style and colourway, and commercial full-grain lines carry that volume comfortably. Custom colours, tight selection grades and unusual tannages may carry tannery minimums above that figure or longer lead times, since the tannery must run a dedicated batch. Where a brand wants to evaluate the material first, small-batch pilots are available before a full commitment is made.
What tests should full-grain leather pass before bulk production?
Common requirements cover tear strength, flex resistance, dry and wet rubbing fastness, light fastness and, where relevant, perspiration fastness. Methods are usually drawn from ASTM or ISO series depending on the destination market, and pass criteria should be fixed before sampling. Finish adhesion and edge paint compatibility also deserve testing, because those failures appear in assembly rather than in the laboratory report.
Is full-grain leather more sustainable than other grades?
Full grain uses the strongest part of a hide that is already a by-product of the meat industry, and it tends to last longer than corrected or bonded materials, which supports a durability argument. Tannery environmental performance is assessed separately, commonly through Leather Working Group audit protocols covering water, energy and chemical management. Restricted substance compliance under REACH is a distinct requirement and should be documented independently of any durability claim.
Why does cutting yield matter so much for this grade?
Because defects in a full-grain hide sit in unpredictable places and cannot be removed by sanding, the cutter must lay pattern pieces around them. On a bag with large uninterrupted panels this reduces the number of usable pieces per hide against a corrected leather of the same area, and that reduction falls directly on unit cost. Relaxing selection grade by one step often saves more than negotiating the tannery price.
Can full-grain leather be used for bag linings?
It can, but it is rarely the best value. Lining surfaces benefit from uniformity, colour fastness and cleanability, and a sueded split or microfibre often performs better on those criteria at lower cost. Where a brand wants an unlined interior or a visible leather interior as a design statement, full grain makes sense on the panels the customer sees. Many programmes mix grades deliberately for this reason.
How should full-grain leather bags be cared for?
Care depends on the finish. Aniline and pull-up leathers benefit from occasional conditioning and should be kept away from prolonged moisture, while pigmented surfaces generally need only a soft dry cloth. All leather should be stored stuffed, away from direct heat and strong light, and allowed to dry naturally if it gets wet. Supply a care card matched to the actual finish rather than a generic one.
When should a designer choose corrected leather instead?
Choose corrected grain when surface uniformity across a large run is the governing requirement, when the price point cannot absorb the yield loss, or when the customer is expected to treat the bag hard and wants it to look new. It also suits embossed logos and pale colours where natural marking would show. Many successful collections use full grain on outer faces and corrected leather elsewhere in the same bag.