
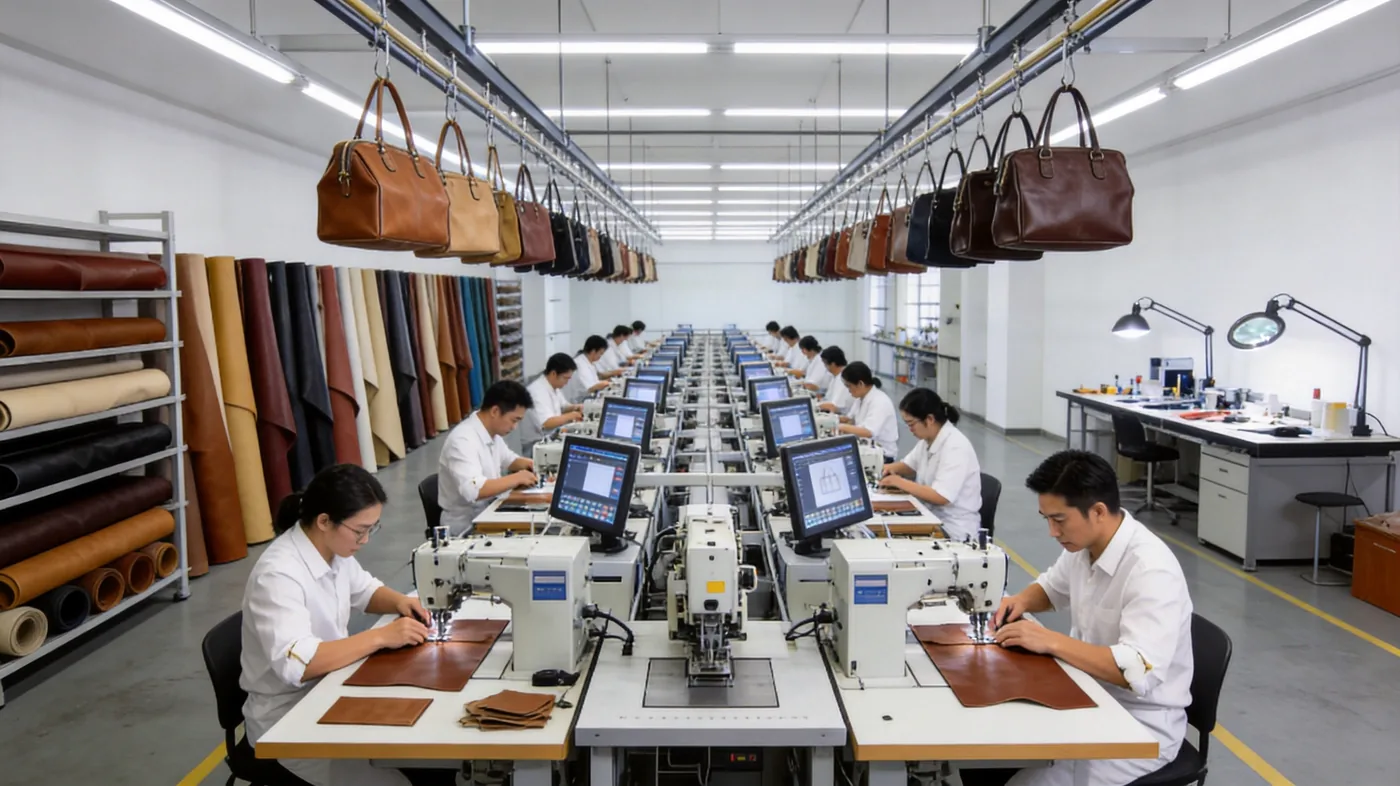
Hand stitching and machine stitching represent two different cost structures rather than two grades of quality. Hand work costs operator minutes on every unit and delivers redundancy, repairability and a craft signal that customers can read. Machine work costs capital, settings and training up front, then delivers uniform output at a low marginal cost. A bag programme should decide the proportion of each by product positioning and by consequence of failure at each seam, not by a general belief that one method is superior.
Two Cost Structures, Not Two Quality Grades
The distinction matters because the two behave differently as volume rises. Machine sewing has a high fixed element and a low variable one: the equipment, the settings and the operator training are incurred once, after which each additional unit adds a small, predictable increment. Hand sewing is almost entirely variable, because every unit absorbs the same operator time regardless of how many have gone before. A programme that intends to scale should understand which parts of its construction scale with it.
- Machine sewing: fixed investment and settings, then a low and stable marginal cost per unit.
- Hand sewing: minimal setup, but a variable labour cost that does not fall with volume.
- Training time: short for a defined machine operation, considerably longer for hand work.
- Capacity ceiling: machine output rises with shifts and equipment; hand output rises with skilled people.
- Quality profile: machine gives uniformity; hand gives redundancy and a visible craft signal.
- Reorder behaviour: machine settings are recoverable; hand consistency depends on retaining trained staff.
What Quality Means in Each Case
Quality in machine sewing means repeatability: the hundredth unit matches the first because the feed, tension and guide are fixed. Quality in hand sewing means judgement at the bench: a maker compensates for a thickness change or a curve without stopping. Neither is inherently better, and each fails in a characteristic way. A machine drifts when settings slip or a needle wears; hand work varies with fatigue and with the individual. The control for the first is measurement, and for the second it is approval limits and supervision.
| Quality dimension | Machine sewing | Hand sewing |
|---|---|---|
| Uniformity | High, provided settings are checked periodically | Variable between operators and across a long shift |
| Damage tolerance | A cut thread can release the run | Damage stays local to the affected stitches |
| Thickness transitions | Can pucker or skew if the feed is not compensated | Compensated by feel on each pass |
| Repairability | Usually requires opening the whole run | A section can be re-sewn in isolation |
| Customer perception | Neutral unless the finish is poor | Read as evidence of craft and justifies price |
| Measurement | Density, tension and edge distance are measurable | Assessed visually and by tactile approval limits |
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
A useful way to frame the decision is to ask which failure the brand would rather explain. A machine-sewn seam that comes apart is a warranty event with a clear cause. Hand work that varies between units is a brand-consistency problem that shows up in photography and in reviews. Both are avoidable, but they need different controls, and a specification that does not say which is being optimised tends to optimise neither.
What Hand Content Actually Buys
Hand content is purchased for three separate reasons, and conflating them leads to poor specification. The first is structural: redundancy at a seam whose failure would be consequential. The second is commercial: a visible craft signal that supports a higher price. The third is narrative: a story that can be told in product copy and in retail training. Only the first is measurable in service; the second and third are marketing assets, and should be budgeted as such rather than justified with engineering arguments.
Capacity and Lead Time Consequences
Hand content constrains the schedule in a way that machine content does not. Adding machine capacity is a question of equipment and shifts; adding hand capacity is a question of people who take months to reach standard. A programme that specifies hand work late, or that increases hand content after the schedule is fixed, will feel that constraint immediately. Sampling runs 6 to 10 working days for standard constructions and 12 to 15 for complex ones, and hand-heavy designs belong in the longer bracket.
| Scenario | Machine-led programme | Hand-led programme |
|---|---|---|
| Doubling the order | Achievable with shifts and line balance | Requires additional trained operators in advance |
| Rush reorder | Recoverable through overtime | Constrained by available skilled capacity |
| Repeat order next season | Settings recovered from the process sheet | Consistency depends on retaining the same team |
| Complex construction | Slower setup, faster running | Slower throughout; sample time extends to 12 to 15 days |
| Capacity risk | Equipment availability and maintenance | Staff retention and training pipeline |
| Planning horizon | Can be committed closer to the launch date | Should be booked earlier in the season |
Choosing by Product Category
Different categories justify different proportions. A structured city bag sold on craft can carry visible hand content at its junctions. A promotional or gifting line sold on price cannot, and would be better served by reinforcement and good hardware. Travel pieces take abrasion and load, so reinforcement matters more than stitch type. Small leather goods are short-seam products where hand content is proportionally affordable and highly visible.
| Category | Suggested hand content | Reasoning |
|---|---|---|
| Premium structured handbag | Moderate, at junctions and handles | Supports the price and the craft narrative |
| Entry luxury or diffusion line | Minimal, decorative only | Margin does not absorb variable labour |
| Travel and duffel | Low; favour reinforcement | Abrasion and load matter more than stitch type |
| Small leather goods | Moderate to high | Short seams; the work is visible and affordable per unit |
| Corporate gifting | Low to none | Volume and price sensitivity dominate |
| Heritage or equestrian styling | High, and expected | The construction is part of the product identity |
Reinforcement: The Middle Path Between the Two
Between a full machine construction and a hand-converted one sits a third option that programmes often overlook: keep the seam on the machine and change what surrounds it. Reinforcement addresses the same failure modes that hand work addresses, at a fraction of the labour cost, and it can be tuned zone by zone. For brands whose margin will not absorb significant hand content, this is usually where the best value sits.
| Reinforcement | What it addresses | Cost character |
|---|---|---|
| Bar tack at run ends | End-of-run release, the most common machine seam failure | Seconds of machine time per position |
| Internal reinforcement tape | Tear-out and hole elongation under sustained load | Material cost plus one operation |
| Rivet or washer at anchors | Concentrated pull at a strap or handle root | Component cost plus setting labour |
| Wider seam allowance | Tear resistance through more material behind the stitch | Slight material yield impact |
| Second pass over a stress run | Redundancy without full hand conversion | Additional machine cycle only |
| Interlining or backing panel | Stiffness and load spreading on a flexible panel | Material plus assembly time |
The limitation is honest and worth stating: reinforcement raises the load at which a seam fails, but it does not change what happens after a thread is cut. A reinforced machine seam that is abraded through will still release along its length. Where the consequence of that release is severe, or where repairability matters to the brand promise, hand work remains the better answer. Where the seam is one of several carrying the same load, reinforcement is usually sufficient and considerably cheaper.
Controlling Quality in Mixed Construction
Most programmes end up with a mix, and the risk sits at the interface. A hand-sewn section that meets a machine-sewn run must align in density, thread and edge distance, or the join will be visible. The process sheet should state where each method starts and stops, and the approved sample should be photographed at those transitions so an inspector knows what conformity looks like. Bulk inspection runs to AQL 2.5 under ISO 2859-1, single sampling, general level II.
- Mark the changeover point between methods on the pattern and photograph it on the approved sample.
- Match thread, density and edge distance across the join so the transition is not visible.
- Set separate acceptance limits for hand and machine work rather than one generic standard.
- Check density on the machine side at intervals; drift is more likely than a step change.
- Record who sewed the hand sections on the sample, and retain that reference for reorders.
- Grade structural seam faults as major and cosmetic variation as minor, before production starts.
Building a Costed Specification
The practical method is to cost two versions of the same design and compare them against the intended retail price. One version uses machine construction with reinforcement; the other converts named seams to hand work. The difference is the true price of the craft signal, and it is usually smaller than brands expect on a targeted specification and larger than they expect on a blanket one. Seeing the number makes the decision commercial rather than rhetorical.
| Step | Action | Output |
|---|---|---|
| 1 | List every seam and classify it as structural, visible or concealed | A seam inventory for the style |
| 2 | Assign a method to each seam and note reinforcement | A zone map for the pattern |
| 3 | Cost the machine-led version including bar tacks and tape | Baseline unit cost |
| 4 | Cost the hand-converted version for the named seams | Incremental cost per unit |
| 5 | Compare the increment against the retail margin | A commercial decision, not a technical one |
| 6 | Fix the result in the tech pack and photograph the sample | A reproducible specification for reorder |
Trade commentary in titles such as Vogue Business and Business of Fashion has repeatedly returned to the same point: craft language only sustains a price when the product delivers something the customer can perceive. Hand stitching is one of the few construction decisions that is both perceptible and defensible, which is why it is worth specifying deliberately. On our production floor in Quanzhou the programme team quotes both versions as a matter of routine, so the choice is made with a number in front of the buyer rather than a claim.
Thread and Needle: The Inputs Behind Every Seam
Two inputs sit behind every seam and are specified less often than almost anything else in the technical pack: thread and needle. Both are usually chosen at the bench by whoever is setting up the operation, and both change how the seam behaves in service. Thread determines tensile strength, elongation, abrasion life and how much the seam puckers when a panel is flexed. The needle determines the size and shape of the hole the thread passes through, which in leather is permanent rather than elastic. A thread and needle decision made once at sampling is cheap; the same decision left open is re-made differently on every reorder.
| Input | What belongs in the specification | Failure when it is left open |
|---|---|---|
| Thread construction | Filament or spun, bonded or unbonded, plus the supplier reference | A substitute sharing the ticket number can elongate differently and change tension behaviour |
| Thread size | Ticket number matched to leather thickness and to the seam's role | Oversized thread crowds the run; undersized thread abrades well before the leather does |
| Thread material | Polyester, nylon or a natural fibre appropriate to the article | Mismatched shrinkage and light-fastness between seam and substrate |
| Needle point | Point type and size suited to the material being pierced | A cutting point leaves scalloped holes that weaken a load-bearing run |
| Needle change interval | Replacement by unit count rather than by breakage | A dull point generates heat, skipped stitches and visible damage around the hole |
| Colour reference | A supplier shade number rather than a description | Batch drift between seasons with nothing to compare against |
Cost is not the argument here, because thread is a small line in any quotation. Consistency is: once the construction, the size and the reference are recorded alongside the density and the edge distance, a repeat order starts from the seam that was approved rather than from a seam that resembles it. Programmes that record these six items rarely need a third sample round to recover the approved appearance.
Machines and Workstations: Which Equipment Suits Which Seam
Ask what equipment a style will actually run on, because the answer constrains the design. A seam that is easy to reach on a flat panel becomes a different proposition once the body is closed, and a seam through four layers behaves differently from the same seam through two. The equipment list therefore belongs in the costing conversation rather than after it, since each configuration below carries a different setup cost and a different operating window.
| Machine configuration | Suited to | Limitation |
|---|---|---|
| Flat-bed lockstitch | Long straight seams on panels accessible from above | Awkward once the body is closed or the seam curves in three dimensions |
| Cylinder-arm machine | Bag bodies, gussets and tubular constructions | Needs operators experienced at feeding curved work at speed |
| Post-bed machine | Strap ends, anchors and small closed shapes | Restricted working area and frequent repositioning |
| Walking-foot compound feed | Thick or multi-layer sections that would otherwise shift | Heavier setup and more frequent adjustment than a standard feed |
| Computerised saddle-stitch unit | Reproducing hand appearance at volume | Higher capital cost; less tolerant of irregular input thickness |
When a design needs two of these in sequence, the style carries a handling cost that has nothing to do with stitch method, and it usually belongs in the longer sampling bracket of 12 to 15 working days rather than 6 to 10. Our Quanzhou production floor runs all five configurations across its seven lines, which is why the second question we ask after reviewing a drawing is always which seams will need machinery the average line does not keep.
Reading a Line During a Walk-Through
Most stitch quality is assessed on finished units laid out on a table, which is the least informative place to assess it. Fifteen minutes beside the operation answers questions no inspection report will. The point is not to audit the operator but to see whether quality is a property of the process or of whoever happens to be having a good morning, because those two behave differently under schedule pressure.
- Watch three consecutive units being made; the variation between them tells you more than any single finished piece.
- Turn the work over as it comes off the machine and look at the underside, where tension problems appear first.
- Ask where a unit goes when the operator is unhappy with it, and how it gets back into the flow.
- Look at how a run is started: whether there is a physical guide or jig, or whether each operator chooses the starting point.
- Ask when the needle was last changed, and whether that is scheduled by unit count or decided on the day.
- Watch how a change in thickness is handled mid-seam, which is where puckering and skewed panels originate.
- Pick one difficult corner and compare it across the three units rather than admiring one good example.
None of these observations require specialist knowledge, and none of them can be faked during production. A line that uses guides, schedules its needle changes and can explain how it handles a step in thickness will produce consistent work under pressure. One that relies on individual judgement will produce excellent units and mediocre ones in the same carton, which is the more expensive outcome of the two.
Writing the Stitching Clause So It Cannot Be Misread
The stitching clause in a technical pack is short, rarely read, and the source of most disputes about whether a bulk lot matches its sample. Its purpose is not to describe quality in general terms but to remove the decisions a machinist would otherwise make alone. Every field below exists because leaving it open produces variation between operators, between shifts and between repeat orders.
The wording matters as much as the content. Instructions such as stitch neatly or reinforce lightly describe nothing anybody can inspect, and they guarantee a disagreement at final inspection. Instructions such as eight stitches per inch plus or minus one, two millimetres from the edge, terminated with three reverse stitches can be measured on the first unit off the line, which is exactly when you want to know whether the specification has been understood.
Cost both versions before you decide
Send a sketch, tech pack or reference sample and the programme team will return two costed constructions, with physical samples in 6 to 10 working days and bulk in 35 to 50 days after approval. Email service@junyuanbags.com or WhatsApp +86 177 5002 0688.
Frequently Asked Questions
Is hand stitching always better than machine stitching?
No. The two are different cost structures with different failure behaviours. Hand work gives localised damage tolerance and a craft signal that customers can see; machine work gives uniformity at a low marginal cost. The right answer depends on the seam, the price point and the volume, which is why most programmes use a deliberate mix rather than choosing one method throughout.
How much does hand stitching add to unit cost?
It depends entirely on how many seams are converted and how long they are, because the driver is operator minutes per unit. Converting four or five stress points is usually a modest increment; converting a whole bag is substantial. The practical approach is to request two quotations on the same design and compare the difference against the retail margin the product has to carry.
Does hand stitching make a bag last longer?
It makes specific seams more tolerant of damage, which is different. A hand-sewn seam survives a cut thread locally instead of releasing along its length, and it can be repaired in isolation. The parts of a bag that usually wear out first are edges, corners and hardware, so stitch type is one input among several rather than a guarantee of longevity.
Why is hand stitching harder to scale than machine stitching?
Because machine output scales with equipment and shifts, while hand output scales with trained people who take months to reach standard. Doubling a machine order is largely a scheduling exercise; doubling a hand-heavy order requires capacity that has to be built in advance. This is why hand content should be fixed before the production schedule is committed.
Can machine stitching be made as durable as hand stitching?
It can be made durable enough for most applications through reinforcement rather than conversion. Bar tacks, rivets, internal reinforcement tape, a wider seam allowance and disciplined backtacks at every run end address the same failure modes. What reinforcement cannot reproduce is the localised damage tolerance of independent locks, which matters most at handles and anchors.
What is decorative hand stitching?
Decorative hand stitching is hand sewing laid over a machine-sewn seam purely for appearance. It photographs identically to structural hand work and is a legitimate design choice, but it adds no strength. Buyers should ask which seams are genuinely hand-constructed, because the answer determines both the service-life benefit and the honesty of the craft claim in product copy.
How should a brand decide where to use hand stitching?
Start with a seam inventory: classify every seam as structural, visible or concealed. Assign hand work to structural seams with high consequence of failure and to visible seams that support the price. Leave concealed, low-load seams on machine. Then cost both versions and compare the increment against the margin, which turns a craft debate into a commercial decision.
Does hand stitching affect the production lead time?
Yes. Hand-heavy designs belong in the longer sampling bracket of 12 to 15 working days rather than the standard 6 to 10, and they constrain how quickly a bulk run can be accelerated. Bulk production runs 35 to 50 days after sample approval. Programmes with significant hand content should be booked earlier in the season to protect the launch date.
How is consistency maintained in hand-sewn production?
Through approval limits and supervision rather than machine settings. The approved sample sets the reference for density, angle and termination; supervisors check against it at intervals; and difficult seams are allocated to the most experienced operators. Retaining the same team between repeat orders is the single most effective control on hand consistency across seasons.
What defects are most common in mixed construction?
The join between methods is the usual problem. Differences in thread, density or edge distance make the transition visible, and a hand section that starts or stops without a proper termination leaves a weak point. Photographing the changeover on the approved sample and setting separate acceptance limits for each method prevents most of these issues.
Should a startup brand use hand stitching?
Rarely at launch. Early programmes benefit more from reliable machine construction, good reinforcement and strong hardware, because those protect the customer experience while the brand validates demand. Hand content can be introduced on a second season once volume and margin are known. A targeted introduction is far safer than building the launch collection around it.
How is stitching graded during bulk inspection?
Inspectors working to AQL 2.5 under ISO 2859-1 assess each sampled unit against an agreed defect list. Structural seam faults such as skipped stitches, missing backtacks or loose tension are normally graded as major, while cosmetic variation on a concealed run is graded as minor. Agreeing the grading before production removes most disputes at final inspection.
Does hand stitching justify a higher retail price?
It supports one, provided the customer can perceive it and the rest of the product is consistent with the claim. Visible hand work at a junction that the customer handles is perceptible; hand work inside a lining is not. Craft language sustains price when the evidence is visible, so budget hand content where it will be seen rather than where it is technically convenient.
Can hand stitching be added after a design is approved?
It can, but it changes cost, sample timing and capacity planning all at once. Adding hand content late usually means a fresh sample, a revised quotation and a longer lead time. It is far better to decide at the specification stage, when the zone map and the cost comparison can be done once and recorded for reorder.
What should the process sheet record for hand work?
The seams assigned to hand work, the thread and density, the edge distance, the termination method, and ideally who sewed the approved sample. Recording the operator is unusual but useful, because it lets a repeat order start from the same reference. Machine settings should be recorded alongside so the two methods can be reproduced together.
Is machine stitching less sustainable than hand stitching?
Not in any simple sense. Machine sewing uses power and produces less labour per unit; hand sewing uses little power and considerably more human time. Durability is the more meaningful environmental variable, and both methods can produce a long-lived bag when specified properly. The waste that matters most comes from defects and rework, not from the choice of method.
How do I compare quotations that use different stitch methods?
Normalise them first. Check the stitch density, thread specification, reinforcement and termination on each quotation, because a cheaper price often reflects a coarser seam or a missing bar tack rather than genuine efficiency. Once both quotes describe the same construction, the difference becomes a real number that can be weighed against the margin.