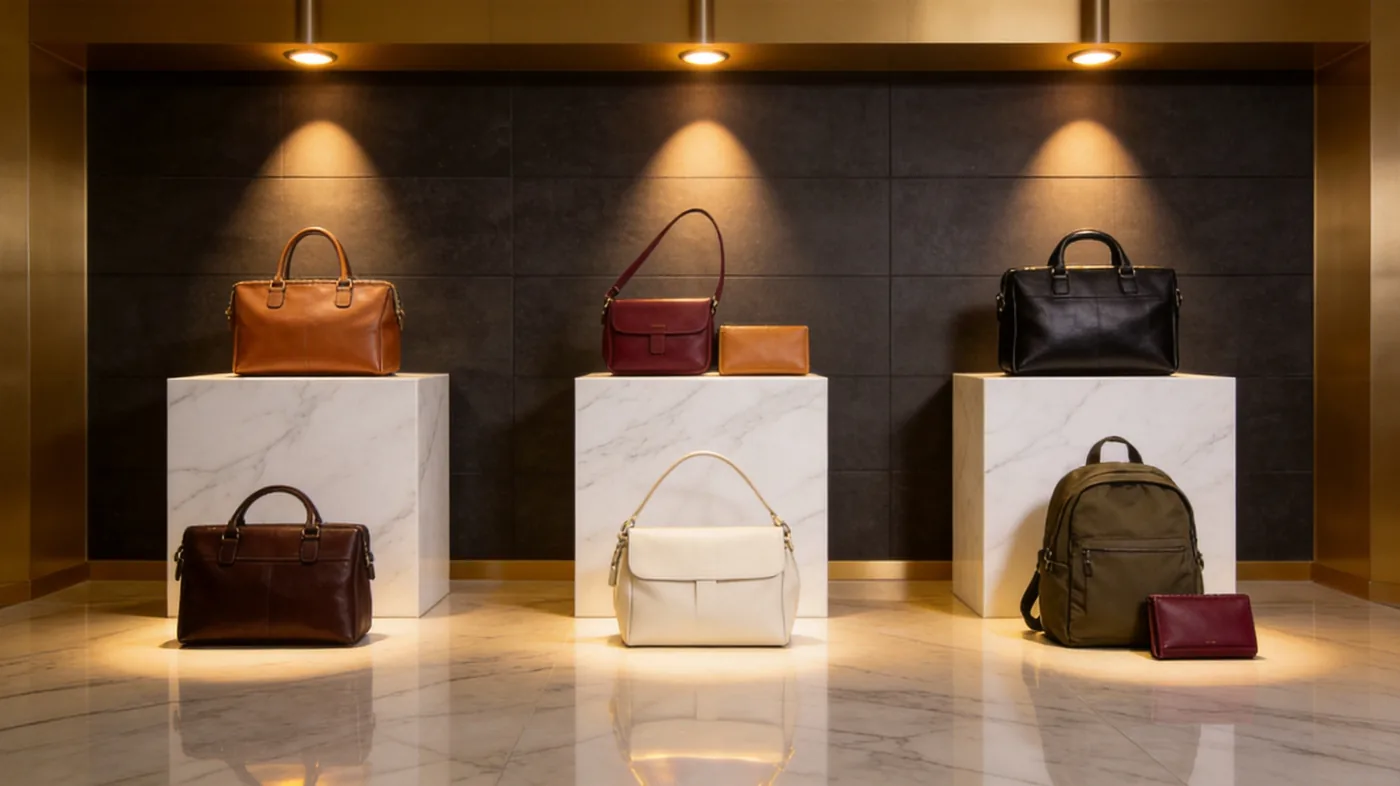
Real leather is identified by four observable things working together: an irregular pore and grain structure that never repeats, a fibrous cut edge rather than a woven or plastic one, a characteristic warm absorption of water, and a distinctive smell under gentle warming. No single test is conclusive on a modern finished bag, because coatings, laminates and high-grade synthetics defeat each of them individually. The practical method is a sequence — surface, edge, flex, absorption, then documentation — and the last step is the only one that settles a commercial dispute.
Why Identification Still Matters Commercially
Two decades of material innovation have made casual identification unreliable. Coated splits embossed with a convincing grain, polyurethane films over a textile base, and microfibre nonwovens engineered to imitate the hand of nappa all pass a glance and several of the traditional tests. Meanwhile the labelling vocabulary has been weakened by terms that sound like grades but legally describe almost nothing. The result is that a buyer can be sold a material that is technically described correctly and still not be the material they believe they specified.
The consequence for a programme is straightforward. Material is normally the largest single line in the cost of a leather bag, and the difference between a full-grain bovine hide and a coated split of similar appearance can be a multiple rather than a margin. It also determines durability: a split used on a strap will fail at the stitch line long before a grain leather will. Identification is therefore not an academic exercise but a procurement control, and it belongs in the specification and inspection process rather than in a showroom conversation.
| Material | Leather content | Typical appearance | Structural behaviour | Where it legitimately appears |
|---|---|---|---|---|
| Full-grain | Whole grain layer intact | Irregular pores, natural markings | Strongest; resists tear at stitch lines | Visible panels, handles, straps |
| Corrected top-grain | Top section, surface refined | Uniform, sometimes embossed | Good; slightly reduced surface strength | Branded production runs |
| Finished split | Lower layer, coated | Very uniform, plastic sheen | Weak; coating carries the load | Linings, backings, internal reinforcement |
| Bonded | Reconstituted fibre and binder | Flat, dead, no grain life | Poor; delaminates and cracks | Avoid in bag construction |
| Microfibre synthetic | None | Very regular, matte nap | Consistent; does not patina | Vegan lines, linings, trims |
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |

The Five Bench Tests, in Order
Run the tests in this sequence because each is cheaper and less invasive than the next, and because each narrows the possibilities for the one that follows. None requires laboratory equipment; together they resolve the great majority of identification questions on a sample. Where the conclusion matters commercially, they are a screening step before verification rather than a substitute for it.
- Surface under raking light. Hold the panel so light grazes it. Real leather shows irregular pore structure and markings that do not repeat. An embossed pattern that repeats at regular intervals indicates a corrected surface or a synthetic film.
- Cut or unfinished edge. Look at a raw edge, a strap end or inside a pocket. Leather presents a dense, slightly fuzzy fibrous core. A synthetic shows a distinct film over a woven or nonwoven base, and the layers can often be seen separating.
- Flex and release. Gently crease the surface and let it go. Leather's crease breaks up into fine, irregular multi-directional lines that largely recover. A plastic coating creases into a single pale line that lingers.
- Water absorption. Place a small drop of water on an inconspicuous area. Unfinished or lightly finished leather darkens and absorbs it over a minute or two. A heavily pigmented or synthetic surface beads it and leaves it sitting.
- Warm smell. Rub the surface briskly to warm it and smell immediately. Leather gives a characteristic warm, slightly sweet, organic note. Synthetics give either nothing or a chemical, plastic note. This test is useful but the least reliable on finished production goods.
| Test | Real leather result | Synthetic result | Reliability |
|---|---|---|---|
| Grain under raking light | Irregular, non-repeating pores | Regular repeating embossed pattern | High, unless grain is heavily embossed |
| Raw edge inspection | Fibrous core throughout | Film over woven or nonwoven base | High where an edge is exposed |
| Flex and release | Fine irregular creases that recover | Single pale line that lingers | Moderate; soft finishes confuse it |
| Water absorption | Darkens and absorbs slowly | Beads on the surface | Moderate; modern topcoats defeat it |
| Warm smell | Warm, organic, slightly sweet | Neutral or chemical | Low on finished goods; useful on raw material |
One caution about the burn test, which circulates widely in consumer advice. Burning a fibre does distinguish protein-based leather from petroleum-based synthetics, but the method is destructive, it is unsafe around finishes and adhesives, and it tells you nothing about grade. On a finished bag it is indefensible as a procurement method. Use it, if at all, on a loose cutting of raw material supplied by the tannery, and never as the basis of a claim against a supplier.
Reading the Surface Under Magnification
A ten-times loupe costs little and resolves most remaining ambiguity. The distinction is not simply that leather has pores and synthetics do not, since a synthetic can be engineered with an artificial pore pattern. The distinction is irregularity: the pore structure of a hide varies in size, spacing and depth across a single panel, because it reflects hair follicles distributed across a living animal. Manufactured regularity is the tell, and it becomes obvious at magnification even when the pattern is convincing to the eye.
| Observation | Indicates | Caveat |
|---|---|---|
| Pores vary in size, depth and spacing | Natural grain surface | Heavily pigmented finishes can fill pores |
| Pores identical and evenly spaced | Embossed corrected grain or synthetic | Some embossing is applied to genuine leather |
| Fine hairs visible at pore openings | Leather, minimally finished | Absent on sanded or corrected leather |
| Straight, uniform fibre bundles at an edge | Textile base under a coating | Laminated leather can show a backing too |
| Coat of a different colour beneath the surface | Pigmented or coated material | Normal on corrected leather; a red flag on full-grain claims |
- Carry a reference. Identification is comparative. A known sample of full-grain, corrected and synthetic material in a sample wallet beats any description in memory.
- Use consistent light. Grain character changes dramatically between warm retail lighting and daylight; assess under a neutral source wherever possible.
- Inspect more than one unit. A single bag proves one bag. Sample across the carton, because mixed lots and mid-run substitution are both real risks.
- Check hidden locations. Inside pocket bags, under strap ends and beneath hardware plates are where the material is least likely to have been upgraded for inspection.
- Photograph everything. Macro images with a scale reference make a later conversation with a supplier evidential rather than anecdotal.
What Labels and Certificates Actually Prove
Documentation is where many buyers place their trust and where most of it is misplaced. A label tells you what the seller is prepared to assert, and a certificate tells you what a laboratory tested on a particular sample on a particular date. Neither is a substitute for a specification that names the material, but both are useful when read for what they cover rather than for the reassurance they appear to offer.
| Document | What it covers | What it does not cover | How to use it |
|---|---|---|---|
| Tannery article specification | Grade, substance, finish, temper for a named article | Whether the bag used that article | Cite the reference in the bill of materials and require it on delivery documentation |
| Material composition label | Broad origin claims | Grade, durability, or the panels used | Treat as a claim to be verified, not evidence |
| REACH test report | Restricted substances in the tested sample | Whether the material is leather, or its grade | Commission per material and colourway; check the report covers the supplied lot |
| OEKO-TEX certification | Textile components against a human-ecological standard | Leather grade or structural performance | Apply to linings, webbing and thread |
| Leather Working Group audit | Environmental performance of the tannery | The quality of any individual hide | Use for sourcing policy and traceability requirements |
| Inspection report | Conformity of finished goods to the agreed specification | Material identity unless specifically included | Add material verification to the inspection scope in writing |
The pattern to notice is that nearly every document in circulation tests something other than the question a buyer is actually asking. A restricted-substance report demonstrates that a material is compliant; it says nothing about whether it is full-grain. A tannery audit demonstrates that a supplier operates to an environmental protocol; it says nothing about the article used in your run. Material identification requires either a specification enforceable against a sealed reference or a laboratory test commissioned specifically for identification.
Common Substitutions and How They Are Made
Substitution is rarely dramatic. It is usually a quiet change in a material schedule, applied to a panel the buyer is unlikely to examine closely or describe precisely in the specification. Understanding where the opportunity sits is the best defence, because each of these substitutions is invited by a specification that failed to name a component.
| Substitution | Where it appears | Why it is tempting | Prevention |
|---|---|---|---|
| Split in place of grain leather | Gussets, linings, inner pocket bags | Materially cheaper, invisible in photographs | Name the grade per panel in the panel schedule |
| Bonded leather on flat panels | Base stiffeners, internal reinforcement | Very cheap, cuts cleanly, looks flat and uniform | Exclude bonded material by name in the specification |
| PU-coated textile on straps | Webbing, crossbody straps, trim | Lower cost, consistent thickness, no grading waste | Specify leather straps with substance and construction |
| Microfibre lining labelled suede | Interiors, pocket bags, trim | Attractive hand, low cost, consistent supply | Require a fibre composition declaration for linings |
| Thinner substance than specified | Body panels, flaps | Yield improves and material cost falls measurably | State substance with tolerance and measure at inspection |
Two clauses in the purchase agreement do most of the preventive work. The first prohibits material substitution without written approval, naming the components covered. The second makes the sealed pre-production sample the contractual reference for material, temper, finish and substance, with the retained sample held by both parties. Together they convert a disagreement about what was supplied into a comparison against an agreed object, which is a very different conversation from an exchange of opinions.
Verifying at Sample, Pre-Production and Bulk
Verification is a schedule rather than a single event, and each stage has a different purpose. Sampling establishes what is intended, pre-production establishes what will be run, and bulk inspection establishes what was made. Skipping the middle stage is the most common cause of a bulk argument, because it removes the only reference that was produced from the material actually used in production.
- At sampling. Confirm the material against the specification using the bench tests, and record the tannery article reference in the technical pack. Assess the prototype in the intended material rather than a substitute.
- At pre-production. Build the golden sample from the bulk-intent lot. Examine it, photograph it, sign it and retain it, with a duplicate travelling with the shipping documents.
- At cutting. Where volume justifies it, verify the material lot identification on the cutting floor against the purchase order before panels are cut.
- During bulk. Include material verification in the inspection scope rather than assuming the inspection covers it. Inspectors check what the check-list asks them to check.
- Before shipment. Confirm carton markings, packing specification and documentation, and reconcile the retained sample against a unit pulled at random from the finished lot.
| Stage | Artefact | Window | What can still be fixed |
|---|---|---|---|
| Feasibility | Feasibility note covering route and cost band | A few working days | Everything; nothing is committed yet |
| Sampling | Prototype in the intended material | 6–10 working days, 12–15 for complex builds | Material, construction and geometry |
| Pre-production | Golden sample from the bulk-intent lot | Sign-off dependent | Material lot, finish level, colour standard |
| Bulk | Production units with in-line records | 35–50 days after approval | Process corrections only |
| Inspection | Report against the agreed sampling plan | A few working days | Rework or rejection, both expensive |
The inspection standard itself deserves a line in the purchase agreement. A single sampling plan built on ISO 2859-1 at an AQL of 2.5 under general level II is the common trade baseline, supported by a written defect classification that separates critical, major and minor faults. Material substitution belongs in the critical class, alongside a failed load test and a sharp hardware edge, because it affects every unit in the lot rather than a statistical sample of them.
Identification in the Context of a Sustainability Claim
Material identification has acquired a second purpose. A vegan line must demonstrably contain no animal-derived material, while a leather line making a traceability or environmental claim must be able to substantiate where the hide came from and how it was processed. In both directions, the evidence is documentation rather than inspection, and it should be gathered during sourcing rather than assembled under pressure later.
- Vegan claims. A composition declaration covering the body, lining, thread, adhesive and finishing agents, because a bag with a leather trim is not a vegan bag.
- Traceability claims. Documentation from the tannery identifying the article and, where the claim goes further, the sourcing chain behind it.
- Environmental claims. Evidence from an audited tannery, most commonly under the Leather Working Group protocol, which assesses environmental performance rather than the quality of an individual hide.
- Chrome-free claims. Test evidence for the specific chemistry used, since the term covers several processes with very different profiles.
- Recycled content claims. A defined methodology and a figure, because recycled content is meaningless without both.
Identification is ultimately a documentation discipline wearing the costume of a sensory test. The bench tests are valuable because they are immediate and they catch the obvious, but the durable protection comes from a panel schedule that names every material, a sealed reference built from the production lot, and an inspection scope that includes material verification. Buyers who arrange those three things rarely need the tests at all, and buyers who skip them find the tests are not enough. Material questions belong in the specification stage, and the quality control scope is where they are made enforceable.
Verify the material in your specification
Send your material schedule and target price. The programme team will confirm what each panel requires, name tannery references where available, and set out the sampling window and verification steps before bulk begins.
Frequently Asked Questions
What is the most reliable way to identify real leather on a finished bag?
Inspect a raw or unfinished edge. Real leather shows a dense, fibrous core throughout the material, while a synthetic shows a distinct film over a woven or nonwoven base, and the layers are often visible where they meet. Combine that with grain inspection under raking light: leather's pores vary in size and spacing, whereas an embossed pattern repeats. Together these two checks resolve most identification questions without damaging the bag.
Does the water drop test really identify leather?
It helps but it is no longer decisive. Unfinished or lightly finished leather will darken and slowly absorb a small drop of water, whereas a plastic surface beads it. However, modern protective topcoats applied at the tannery make genuine leather behave like a synthetic, so a negative result proves only that the surface is sealed. Treat the test as supporting evidence rather than as a conclusion.
Can you identify leather by smell?
Smell is a useful screening tool on raw material and a weak one on finished goods. Warm the surface by rubbing and smell immediately: leather gives a warm, slightly sweet, organic note, while synthetics give either nothing or a chemical one. On a production bag, adhesives, finishes and packaging can mask or mimic that note, so smell should confirm other findings rather than lead them.
Is the burn test a safe way to check for real leather?
It is not appropriate for a finished bag. Burning distinguishes protein-based leather from petroleum-based synthetics, but the method is destructive, unsafe around finishes and adhesives, and says nothing about the grade of the leather. If it is used at all, it should be on a loose cutting of raw material supplied by the tannery, and it should never be the basis of a claim against a supplier.
What is bonded leather, and should it be used in bags?
Bonded leather is shredded leather fibre mixed with a binder and pressed onto a backing. It contains leather but behaves nothing like it: it has no grain structure, it cracks and delaminates, and it cannot hold a stitch under load. It is sometimes found in base stiffeners and internal reinforcement. For any load-bearing panel in a bag it should be excluded from the specification by name.
How can I tell a coated split from a full-grain leather?
Look at the surface under raking light and at the reverse. A coated split has a perfectly uniform embossed grain with no pore variation and a visibly printed pattern, while full-grain shows irregular pores and natural markings. The reverse of a split is loose and distinctly fibrous. Under magnification, a coated split often reveals a film layer sitting on top of the fibre rather than a continuous structure.
Do certificates prove a bag is made of real leather?
Usually not. A REACH test report demonstrates that the tested sample complies with restricted-substance limits, not that the material is leather. An OEKO-TEX certificate covers textile components against a human-ecological standard. A Leather Working Group audit assesses a tannery's environmental performance. Only a laboratory identification test, commissioned on the supplied lot and written into the inspection scope, actually addresses the question of what the material is.
What should a specification say to prevent material substitution?
It should name the grade, tannery article reference, substance with tolerance, temper and finish for every panel, presented as a panel schedule rather than a single line for the bag. Add a clause prohibiting substitution without written approval, and make the sealed pre-production sample the contractual reference. Together these convert a dispute about what was supplied into a comparison against an agreed object.
How do microfibre synthetics differ from suede in use?
Microfibre is a nonwoven of very fine polymer fibres impregnated with resin, engineered to imitate a suede hand. It is consistent in colour and thickness, resists water better than untreated suede and does not shed pile, but it does not patina, it can feel warmer against the skin, and it holds a crease differently. It is a legitimate material for vegan lines and linings, provided it is described accurately rather than as leather.
Why does material identification matter for a bulk order?
Material is normally the largest single cost line in a leather bag, and the gap between a full-grain hide and a coated split of similar appearance can be a multiple rather than a margin. It also determines durability: a split used on a strap or handle will fail at the stitch line long before a grain leather. Substitution on hidden panels is invisible in photography and easy to miss without a panel schedule.
How many units should be checked for material verification?
Material identity is a lot-level question rather than a sample-level one, because substitution affects every unit made from the lot rather than a statistical proportion. It belongs in the critical defect class in the inspection plan, alongside a failed load test, and should trigger lot-level action rather than the numeric threshold applied to major and minor faults under a plan built on ISO 2859-1.
Which inspection standard should be agreed before bulk production begins?
The common trade baseline is a single sampling plan built on ISO 2859-1 at an AQL of 2.5 under general level II, agreed in writing before bulk is authorised and supported by a defect classification separating critical, major and minor faults. Add material verification explicitly to the inspection scope, because inspectors check what the checklist asks them to check, and material identity is not automatically included.
How does identification support a vegan or sustainability claim?
In both directions the evidence is documentation rather than inspection. A vegan claim needs a composition declaration covering the body, lining, thread, adhesive and finishing agents, since a leather trim invalidates it. A leather claim needs tannery documentation identifying the article and, where traceability is asserted, the sourcing chain behind it. Gather this evidence during sourcing rather than assembling it under commercial pressure later.
When should material verification happen during production?
At three points: sampling, where the prototype is built in the intended material; pre-production, where the golden sample is built from the bulk-intent lot, signed and retained; and bulk inspection, where the retained reference is compared against a unit pulled at random from the finished lot. Skipping the middle stage is the most common cause of a bulk dispute, because it removes the only reference made from the material actually run.