
You can judge the quality of a bespoke bag before placing a bulk order by assessing five things in the sample: stitch density and thread quality, edge and seam finishing, hardware weight and movement, structural reinforcement at load points, and interior cleanliness. Alongside the physical assessment, request documented evidence — material test reports, inspection standards and comparable references. A supplier who can satisfy both halves of that assessment is very unlikely to disappoint in bulk.
The reason this matters is that bulk rarely improves on the sample. If stitch density is inconsistent at unit one, it will be inconsistent at unit three hundred, only across more pieces. If an edge is poorly burnished on the prototype, the production version will inherit the same method. The sample tells you what the process produces, and processes do not spontaneously improve under volume.
What follows is a working assessment framework rather than a set of aesthetic preferences. It is deliberately organised from the fastest check to the most involved, so that a buyer with ten minutes and a sample bag can form a defensible view before committing to a longer evaluation.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The Five-Minute Physical Assessment
Start with the object in your hands and no instruments. The purpose of this pass is not to approve anything but to decide whether a deeper evaluation is worth the time. Most experienced buyers can eliminate a significant proportion of unsatisfactory samples in this first pass, because the failures that matter most are usually tactile rather than visual.
- Weigh it: does the mass feel appropriate to the stated material and construction, or unexpectedly light?
- Flex the panels: does the bag hold its intended shape, or collapse in a way the design did not intend?
- Run a finger along every edge: are they smooth, consistent and continuous, or uneven and sticky?
- Work every zip and closure: is the movement smooth under light load and under tension?
- Lift it empty by the handles and then loaded: do the handles and attachment points feel secure?
- Turn the lining out as far as it goes: are the raw edges concealed and the seams clean?
Each of these checks corresponds to a failure mode that shows up in the field. Unexpected lightness usually indicates a thinner lining or a lighter interlining than specified. Edge unevenness predicts edge coating failure within months. Handles that feel loose when empty will not improve under load. The assessment is crude but it is not arbitrary.
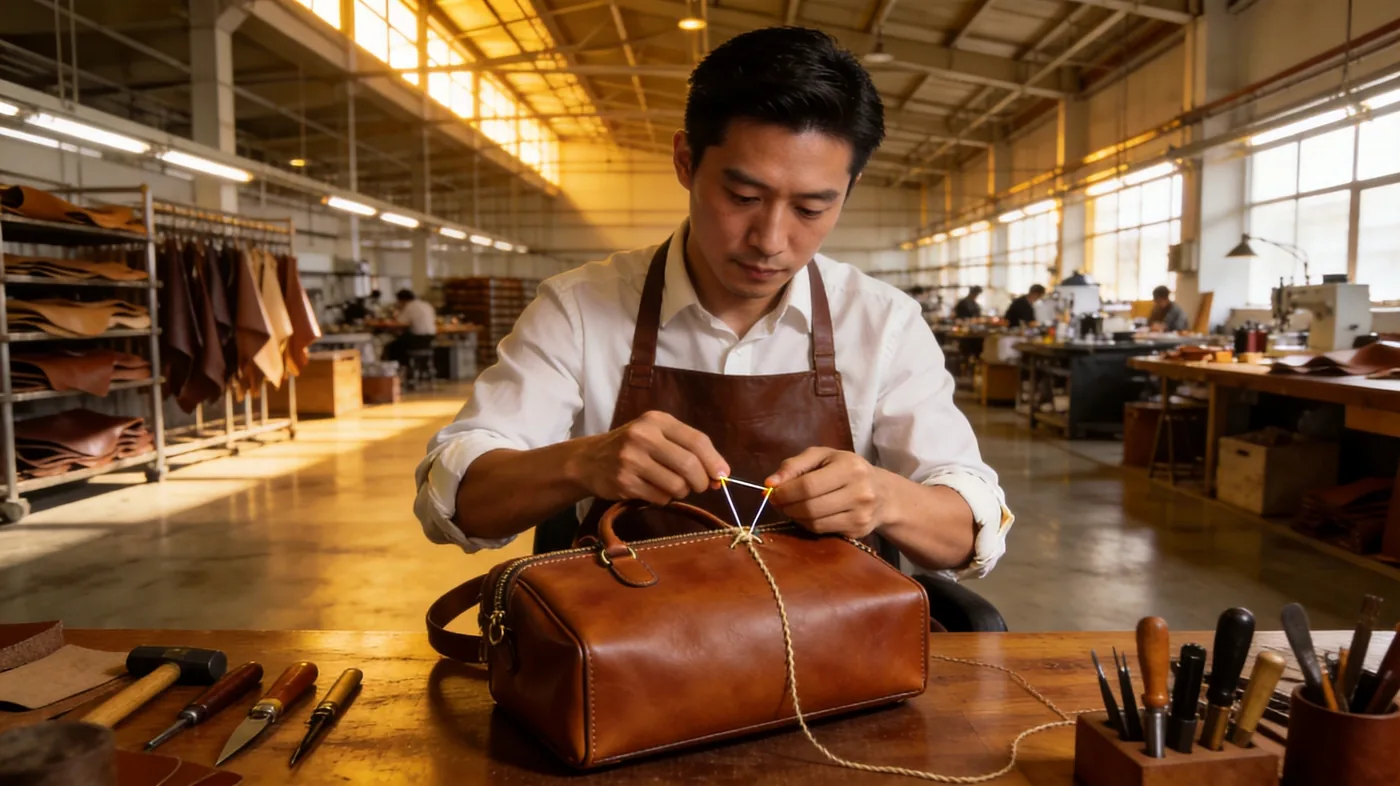
The second pass benefits from one inexpensive tool: a ruler. Measure the critical dimensions against your specification and record the deviations rather than noting that they look about right. Check handle drop, strap length at full extension, base dimensions and internal pocket sizes. A bag can feel excellent and still be three millimetres outside the tolerance that governs whether a laptop fits, and that discrepancy is invisible until it matters.
Stitching: Density, Thread and Termination
Stitch density is the most cited quality marker in this trade and the most frequently misunderstood. Higher density is not automatically better; it is better up to a point, beyond which perforating the leather weakens it. What matters more is consistency: even spacing, uniform tension, and correct termination. A row of stitches that varies in length is a visible defect regardless of the average count.
| Stitch attribute | What to look for | What it indicates |
|---|---|---|
| Density | Even, appropriate to material substance | Correct specification and machine set-up |
| Spacing | Uniform along the full run | Operator discipline and machine condition |
| Tension | Neither puckering nor loose loops | Correct thread, needle and tension settings |
| Termination | Backstitched or secured, no loose ends | Process discipline at start and stop points |
| Thread | Appropriate material and weight for the leather | Specification quality rather than convenience |
| Seam alignment | Stitch line parallel to the panel edge | Pattern accuracy and jig use |
Look specifically at the start and finish of each run, and at corners and junctions. These are where the operator has most discretion and therefore where variation concentrates. A sample that is clean along straight runs but untidy at corners tells you the standard depends on operator care rather than process control, which will show up across five hundred units.
Edges, Seams and the Places Bags Actually Fail
Bags fail at predictable locations: the point where a handle meets the body, the base corners, the zip ends, and anywhere two materials meet at different tensions. Inspecting these areas tells you more than inspecting the flat centre of a panel. The question to ask at each is whether load is distributed into the structure or concentrated at a stitch line.
| Location | Failure mode | What good construction looks like |
|---|---|---|
| Handle attachment | Tearing away from the body | Reinforcement plate or internal stay distributing load |
| Base corners | Abrasion through the finish, then the substrate | Reinforced corner construction and feet |
| Zip ends | Slider derailment or tape separation | Secured end stops and bar-tacked tape |
| Strap junctions | Elongation then failure at the stitch line | Skived and layered joint, stitched through reinforcement |
| Gusset folds | Cracking at a repeated flex point | Correct substance and a fold allowance matched to the material |
Edge finishing is worth its own attention because it is the most visible craft signal and the most common shortcut. A painted edge should be smooth, even in width, and neither tacky nor brittle. A burnished edge should be slick and dense rather than fuzzy. A turned edge should lie flat with no rippling. Any of these can be achieved well; all of them are expensive to achieve well, which is why they are the first place cost pressure appears.
Seam construction deserves separate attention from stitching, because a seam can be perfectly sewn and still be wrong for the application. A butt joint, a lapped seam and a bound seam behave differently under load and wear differently over time. The correct choice depends on where the seam sits, what it carries and what material it joins. A supplier who can explain why a particular seam was chosen at a particular location is demonstrating engineering judgement rather than habit.
Hardware: Weight, Plating and Movement
Hardware is the second most common place for silent cost reduction, because a lighter Zamak fitting looks identical to a heavier brass one in a photograph. Pick the piece up. Test the movement of each clasp, swivel and slider through its full range. Look at the plating at contact points and edges, where wear appears first. Ask what the base metal is and how the finish is applied.
- Weight and feel: solid fittings are heavier than hollow castings of the same size.
- Plating consistency: check edges, corners and contact points for thinning or flaking.
- Movement: clasps should close with a definite action and open without sticking.
- Attachment: rivets and screws should be seated flush with no burr or movement.
- Marking: custom logo plates should be crisp, with consistent depth and alignment.
- Protection: fittings should be separated from leather in packing to prevent marking.
Where hardware is custom-tooled, ask about the tooling itself: who owns it, what it costs, and what happens to it. Custom fittings are one of the strongest exclusivity mechanisms available to a brand, precisely because they cannot be ordered from a catalogue. They are also a committed cost, which is why the decision belongs after sample approval rather than before.
Hardware assessment should extend to how fittings meet the bag. A well-made attachment spreads load through a reinforcement layer rather than concentrating it at the point of contact, and the difference is visible in how the panel behaves when the handle is pulled. Lift the bag by one handle, then by the other, then by both, and watch whether the body distorts. Distortion at the attachment is a prediction, not a cosmetic issue.
Structure, Reinforcement and Load Paths
Structure is what separates a bag that looks good in a photograph from one that looks good after two years. The underlying question is always the same: where does the load go? A bag carrying several kilograms transfers that weight through the handles, into the attachment, into the body panels, and finally to the base. Any weak link in that chain will announce itself eventually.
Load testing is the other assessment worth specifying before bulk. A simple protocol — load to a stated weight, carry for a defined distance or cycle count, then inspect handles, attachments and seams — surfaces most structural weaknesses within hours. It is not a substitute for laboratory testing where a market requires it, but it catches the majority of construction problems while correction is still cheap.
Interior assessment should also include the parts a customer touches most: zip pulls, pocket openings and the lining surface itself. Cheap linings fail by abrasion and pilling long before the outer material shows wear, which is why lining specification deserves the same scrutiny as the outer shell. A heavy, tightly woven lining costs more and lasts materially longer than a lightweight alternative that looks identical on a specification sheet.
Interiors, Linings and Finishing Standards
Interiors are where makers and manufacturers diverge most visibly, because internal finishing consumes hours and is rarely photographed. A well-finished interior has no visible adhesive, no raw seam allowances, no loose threads and no puckering at the corners. Pockets sit flat. Device sleeves are dimensioned to an actual device rather than approximately. Where the design includes organisation, the layout reflects how the bag will actually be used.
- Seam allowances: concealed or cleanly bound, with no raw edges visible anywhere.
- Adhesive: no squeeze-out at seams, pockets or lining attachment points.
- Threads: no loose ends at any termination, inside or out.
- Corners: lining corners flat, with no bunching or excess material.
- Pocket construction: sized to the stated contents, attached to carry load.
- Branding inside: applied consistently, positioned per the specification.
One distinction separates a competent assessment from a superficial one. A superficial assessment asks whether the bag looks good. A competent assessment asks whether the process that made this bag will make five hundred more like it. That reframes everything: consistency matters more than excellence, documentation matters more than charm, and the questions that feel slightly awkward at the time are precisely the ones worth asking.
Evidence Beyond the Sample: Tests, Audits and References
A good sample is necessary but not sufficient, because a sample can be made carefully in a way that a production run cannot. Documented evidence is what bridges that gap. Ask for material test reports by lot, the inspection standard applied to bulk, and references from buyers running programmes of comparable size and complexity.
| Evidence | What it proves | Red flag |
|---|---|---|
| Material test report by lot | The specific material lot was tested against a method | Undated certificate covering a material family |
| Inspection standard in writing | Bulk will be checked to a defined AQL | Vague assurance that quality is checked |
| Capacity with line allocation | Your programme has scheduled production space | Headline monthly figure with no allocation |
| Comparable references | Similar work has been delivered successfully | References from unrelated product categories |
| Corrective action records | Problems are documented and resolved | Claim that problems never occur |
| Certification numbers and scope | Claims can be independently verified | Logos without certificate numbers |
References deserve a note on how to read them. Ask for buyers running comparable programmes rather than the largest name available, because capability at one scale does not predict it at another. Ask what went wrong and how it was handled, since every programme encounters problems and the response is more informative than the absence of one. A supplier who describes a failure plainly is usually safer than one who claims never to have had one.
Scoring a Supplier Before You Commit
The final step is to convert all of this into a decision. Scoring suppliers against a fixed set of criteria removes the halo effect of a beautiful sample and forces the comparison that matters: not which bag is nicest, but which programme is most likely to deliver five hundred of them on time and to standard.
| Criterion | Weight | Passing standard |
|---|---|---|
| Sample construction quality | High | Consistent stitching, clean edges, solid hardware |
| Specification responsiveness | High | Technical questions answered specifically, not generically |
| Documented compliance | High | Test reports by lot with dates, methods and scope |
| Capacity with allocation | High | Named lines and a date range in writing |
| Communication and escalation | Medium | Named contact with a committed response time |
| Commercial terms | Medium | Tooling, sampling and payment structure itemised |
Scoring also protects against a subtler risk: the confident supplier. Fluency in trade vocabulary is not evidence of capability, and a polished presentation can conceal an operation that has never built your construction. Weight the criteria that can be verified — test reports, comparable examples, line allocation, corrective action records — above those that depend on impression. Verification is slower than trust, and considerably cheaper.
None of this requires special expertise, only a checklist and the discipline to use it before the deposit rather than after the disappointment. Buyers who assess this way tend to find the same thing: the samples that impress most on a screen are not always the ones that survive a proper look.
Evaluate a sample properly
Request a prototype built to your specification and assess it against this framework. The programme team will supply the evidence pack that goes with it.
Frequently Asked Questions
What is the fastest way to judge bespoke bag quality in a sample?
Use a tactile pass: weigh the bag, flex the panels, run a finger along every edge, work each closure, then turn the lining out as far as it goes. Inconsistent stitching, sticky edges and loose handle attachments show up immediately.
Does higher stitch density always mean better quality?
No. Density is better up to a point, beyond which perforation weakens the leather. Consistency matters more: even spacing, uniform tension and properly secured terminations indicate process control, whereas a high average count with visible variation does not.
Where do bespoke bags most often fail in use?
Handle attachments, base corners, zip ends, strap junctions and gusset folds. Each is a point where load concentrates or material flexes repeatedly, and each has a known construction response that should be visible in a well-made sample.
How can I tell if hardware quality has been reduced?
Weigh the fitting and compare it with a known reference, inspect plating at edges and contact points, and test each moving part through its full range. Ask what the base metal is and how the finish is applied, then verify the answer.
Should I approve a sample before seeing material test reports?
It is better to review both together. A sample proves the construction; the test report proves the material in that sample meets the restrictions applicable to your market. Approving one without the other leaves a gap that surfaces later.
What inspection standard should apply to the bulk order?
Specify AQL 2.5 under ISO 2859-1, single sampling, general level II, in the purchase order. Add a defect classification matrix defining critical, major and minor defects for the specific product, ideally with photographs.
How many sample rounds should I expect before approval?
Two rounds is typical, three is prudent for complex constructions or where fit against a specific device or garment matters. Each standard round takes six to ten working days, longer for complex work.
What is the minimum order quantity for a bespoke bag programme?
The standard minimum is 500 pieces per style per colourway. A small-batch pilot route exists for brands validating demand, with a higher unit cost because tooling and set-up are spread across fewer pieces.
How long does bulk production take after sample approval?
Bulk runs 35 to 50 days after sample approval. Plan against the upper end, and build the schedule backwards from the date goods must land rather than forwards from the date of the order.
Why does the sample matter so much for a bulk order?
Bulk rarely improves on the sample. The prototype reveals the process that will be repeated hundreds of times, so inconsistency, shortcuts or weak construction observed at unit one will recur across the full run.
What should a supplier's evidence pack contain?
Photographs under neutral light, a dimension report measured against your brief, the material swatch board, test reports by lot, and a written list of any deviation from specification with the reason for it.
How do I verify a supplier's capacity claim?
Ask which lines are allocated to your programme type and in which weeks, request a live video walkthrough you direct yourself, and check certification numbers against issuing bodies. Specificity is the test of a genuine answer.
Are sustainability claims verifiable in bespoke bag production?
Yes, if you ask for evidence. Request Leather Working Group audit references for tanneries, OEKO-TEX documentation for textiles and linings, and recycled content declarations for packaging, each with numbers and dates.
What payment structure protects a buyer before bulk?
T/T with 30 per cent deposit and 70 per cent before shipment is standard. Releasing the balance against an inspection pass rather than a production photograph preserves leverage until quality has been evidenced.
How do I compare two suppliers fairly?
Score both against the same criteria: sample construction, specification responsiveness, documented compliance, capacity with allocation, communication and commercial terms. Fixed criteria remove the halo effect of an attractive prototype.
What is a pre-production sample and why retain it?
It is built from exact bulk materials and hardware and becomes the reference standard for the run. Retaining it with the buyer means any later dispute is resolved by comparison against an object rather than by memory.
Can I judge quality without visiting the production floor?
Yes, through a structured physical assessment, a complete evidence pack, live video verification and contractual inspection standards. Travel helps, but a disciplined documentary process covers most of the same ground.
How important is edge finishing as a quality signal?
It is among the most reliable. Achieving clean edges costs hours, so painted, burnished or turned edges are the first place cost pressure shows. Uneven, tacky or brittle edges predict early failure.
What should I do if a sample has a defect?
Document it photographically, describe it against the specification rather than in general terms, and return a written correction list. Treat the second round as verification that the correction was applied, not as a fresh evaluation.
Does material grade affect how long a bag lasts?
Substantially. Full-grain leather develops a patina and can last for decades, while corrected or bonded constructions rely on surface coatings that fail earlier. Grade selection should follow the intended life of the product.