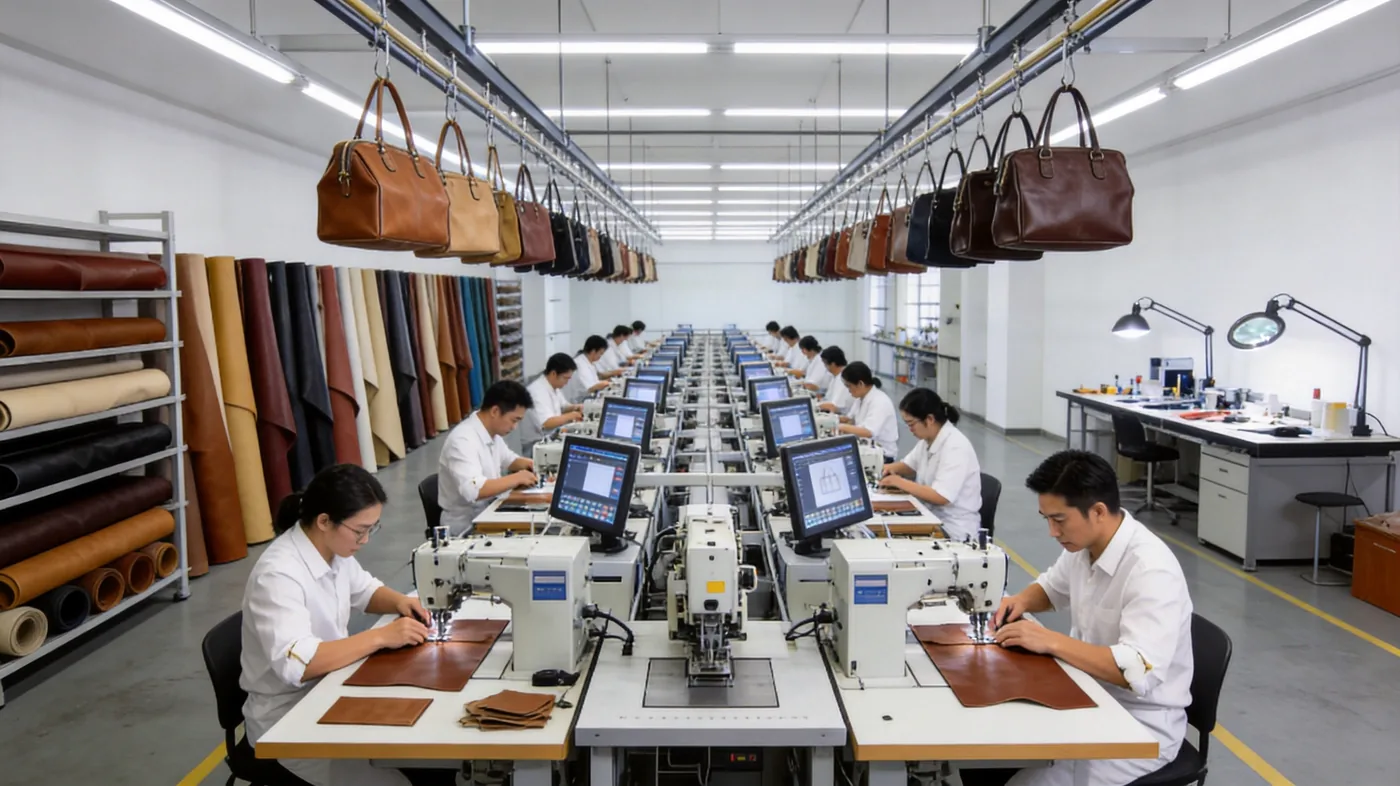
Most bespoke leather bags perform best between 1.2 mm and 2.0 mm, with the correct figure set by silhouette rather than by prestige: soft clutches and linings sit near 0.8–1.0 mm, everyday crossbodies around 1.2–1.4 mm, structured totes and briefcases at 1.6–2.2 mm, and load-bearing straps thicker again or reinforced internally. Specify substance in millimetres with an explicit tolerance and named measurement points, because a drift of 0.2 mm changes finished weight, drape, stitch length and how cleanly a panel turns. Thickness works alongside temper, finish and reinforcement; the four together decide whether a bag holds its architecture or slowly slumps.
How Leather Thickness Is Measured and Specified
Leather substance is quoted in two competing systems. Tanneries in North America and much of the saddlery trade use ounces, where one ounce equals one sixty-fourth of an inch, roughly 0.4 mm. European and most Asian tanneries quote millimetres directly, and millimetres are what belong on a technical pack because patterns, skiving blades and sewing machine clearances are all dimensioned metrically. Confusion between the two systems is a recurring source of sampling error, particularly when a brand brief written in ounces reaches a cutting room working in millimetres.
| Ounces (oz) | Millimetres (mm) | Where it typically appears |
|---|---|---|
| 1–2 oz | 0.4–0.8 mm | Garment leather, linings, soft folds |
| 2–3 oz | 0.8–1.2 mm | Clutches, wallets, lightweight travel pieces |
| 3–4 oz | 1.2–1.6 mm | Crossbody bodies, backpack shells, slouchy totes |
| 4–5 oz | 1.6–2.0 mm | Structured totes, briefcases, holdalls |
| 5–6 oz | 2.0–2.4 mm | Bases, handles, attachment cases, straps |
| 6–8 oz | 2.4–3.2 mm | Belting, heavy straps, harness work |
A thickness figure without a tolerance is not a specification. Hides are natural material; substance varies across the flank and back, and finishing operations such as milling, embossing or heavy pigment application change the final reading. The workable convention on our programmes is a target with plus or minus 0.1 mm, measured at three points per panel with a dial gauge, and stated as substance after finishing rather than in the crust.
- Always state the unit. A brief reading eight ounce is unambiguous only to readers already fluent in the imperial system.
- Measure substance after finishing. Pigment, wax and embossing add measurable substance that disappears from a pre-finish reading.
- Name the measurement points: centre of the panel, 20 mm from the cut edge, and at the tightest turn.
- Record the temper alongside the substance. Two hides of identical thickness behave completely differently when one is boarded soft and the other is milled firm.
- Retain a physical reference swatch from the approved bulk lot and attach it to the gold-seal file.
The Right Weight for Each Bag Silhouette
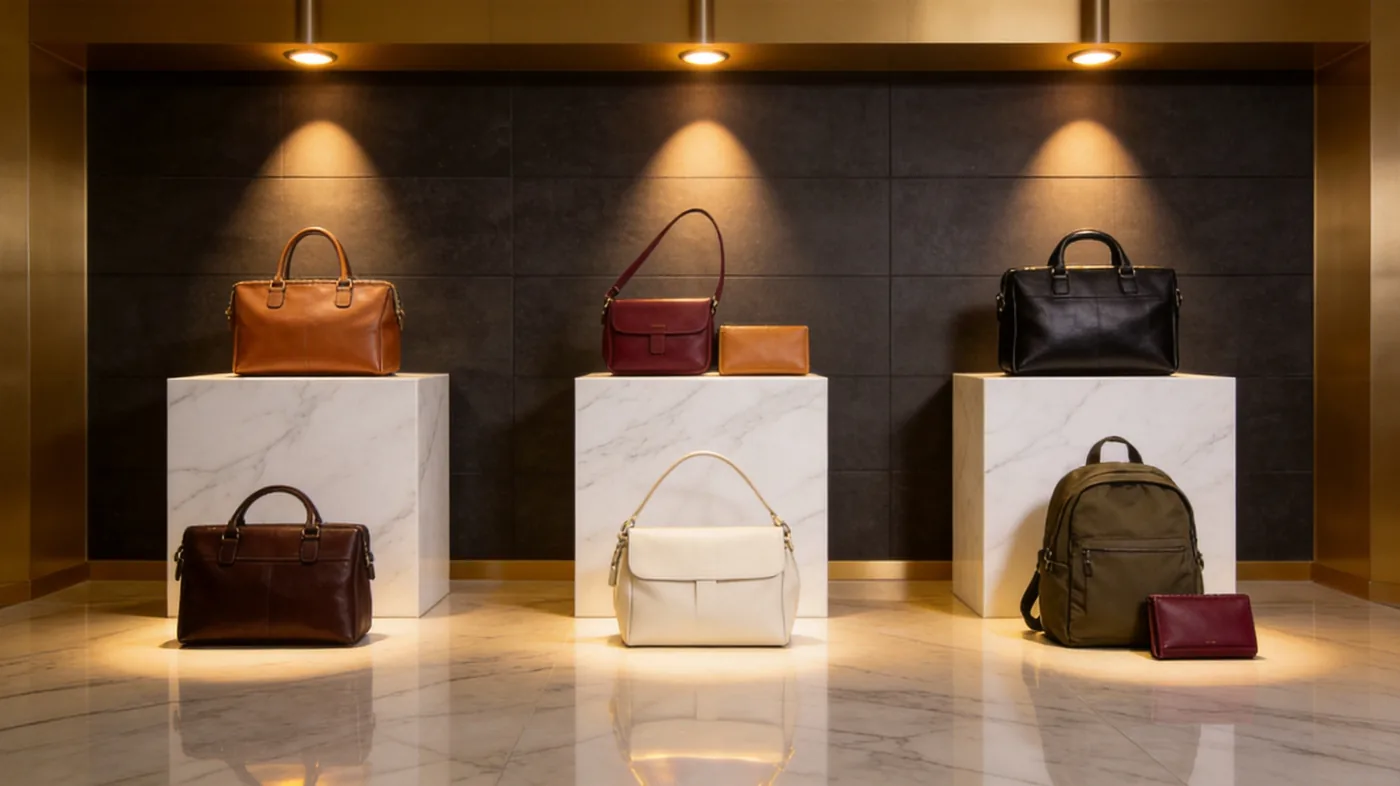
Silhouette is the strongest single predictor of correct substance. A shape that depends on a crisp edge and a self-supporting panel needs material heavy enough to resist gravity; a shape that depends on collapse and softness needs less, and will look clumsy if overweighted. The table below reflects the ranges the programme team specifies most often, and each assumes a full-grain or top-grain bovine hide of medium temper unless stated otherwise.
| Bag style | Shell substance | Temper | Why that range |
|---|---|---|---|
| Card holder, slim wallet | 0.6–1.0 mm | Soft to medium | Must fold flat and slide into a pocket without bulk |
| Wash bag, toiletry case | 1.0–1.2 mm | Medium, wipeable finish | Needs shape retention but packs flat; heavy substance resists folding |
| Flat clutch, envelope | 1.0–1.2 mm | Soft | Hand feel dominates; structure is not required |
| Crossbody bag | 1.2–1.4 mm | Medium | Balances drape against the pull of a loaded strap |
| Shoulder bag, hobo | 1.0–1.3 mm | Soft, milled | Slouch is the design intent; heavier substance fights it |
| Backpack shell | 1.4–1.8 mm | Medium to firm | Must hold form under compression and carry harness stress |
| Unstructured tote | 1.4–1.6 mm | Medium | Soft enough to fold, strong enough for daily load |
| Structured tote | 1.6–2.0 mm | Firm | Panels stand unaided; edges can be painted cleanly |
| Top-handle, satchel | 1.8–2.2 mm | Firm | Architecture is the product; lighter substance collapses at the gusset |
| Briefcase, attaché | 1.8–2.2 mm | Firm | Professional silhouette and long-span panels need stiffness |
| Holdall, duffel | 1.6–2.0 mm | Medium to firm | Resists abrasion at the base while remaining packable |
| Garment bag, suit carrier | 1.0–1.4 mm | Soft to medium | Weight matters more than rigidity when the piece is carried empty |
Two patterns emerge from the table. First, the range narrows as the silhouette becomes more defined: a hobo can tolerate half a millimetre of variation without anyone noticing, while a satchel cannot. Second, larger bags do not automatically need thicker material. A holdall is larger than a briefcase yet often specified lighter, because a travel piece is judged on empty weight and packability, whereas an executive case is judged on how squarely it stands on a desk.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
Handles, Straps, Bases and Gussets Carry the Load
The shell is rarely the component that fails. Handles, straps, base panels and gussets absorb the concentrated stress of a loaded bag, and they are the parts that should be specified above the shell substance. This is the single most useful adjustment a designer can make: keep the body light for comfort and weight, then add substance or reinforcement exactly where force is applied.
| Component | Specified substance | Failure mode if underspecified |
|---|---|---|
| Top handle core | 2.0–2.6 mm, often doubled | Stretch at the rivet holes, permanent curl, eventual tear-out |
| Shoulder strap body | 2.2–3.0 mm | Elongation under load, edge cracking at the fold |
| Base panel | 2.0–2.4 mm or reinforced | Sagging, abrasion through the finish, loss of footprint |
| Gusset | 1.4–1.8 mm, skived at folds | Bulky corners, splitting at the turn, poor edge paint adhesion |
| Zip facing and binding | 0.8–1.2 mm after skiving | Puckering, tape bite, difficulty feeding through the machine foot |
Reinforcement is frequently the better answer than raw substance. A 1.6 mm shell with a bonded interlining at the base will outperform a 2.4 mm shell of the same leather at lower weight and lower material cost, and it will turn more cleanly at the corners. The trade-off is that reinforcement must be specified on the pattern, not improvised on the line, and it must be recorded because it changes cutting yield and the skiving plan.
What Thickness Does to Finished Weight
Weight is the consequence of substance that customers feel first. Bovine leather weighs roughly 0.8 to 0.9 kilograms per square metre per millimetre of substance, so a bag with 0.45 square metres of shell material gains about 380 grams for every additional millimetre. On a tote that is already near the limit of comfortable carry, the difference between a 1.6 mm and a 2.0 mm specification can be the difference between a daily bag and one left at home.
| Shell substance | Material weight on 0.45 m² | Indicative finished bag weight | Comfort read |
|---|---|---|---|
| 1.0 mm | ≈ 0.38 kg | 0.55–0.70 kg | Light, packs easily, minimal structure |
| 1.4 mm | ≈ 0.54 kg | 0.75–0.95 kg | Comfortable daily carry |
| 1.8 mm | ≈ 0.69 kg | 0.95–1.25 kg | Substantial; structure holds unaided |
| 2.2 mm | ≈ 0.85 kg | 1.20–1.55 kg | Heavy; acceptable in a briefcase, tiring in a tote |
| 2.6 mm | ≈ 1.00 kg | 1.45–1.85 kg | Heritage or specialist brief only |
Hardware and lining add to these figures, typically 15 to 30 per cent on a bag with substantial fittings. That is why the weight target belongs in the brief from the outset: when a brand states a finished-weight ceiling of, say, 900 grams, the substance decision is already constrained, and arguing about millimetres afterwards wastes a sampling round.

Temper, Drape and the Thickness Illusion
Buyers routinely assume that thicker means firmer, but temper is an independent property set by the tannery through milling, boarding, staking and the type and quantity of fatliquor applied. A soft-milled 2.0 mm hide can drape more loosely than a firm 1.4 mm hide. When a sample feels wrong, the instinct is often to change the substance; the faster correction is usually to change the temper and leave the millimetres alone.
- Soft temper at low substance produces a fluid, garment-like drape suited to hobos and slouchy totes.
- Firm temper at moderate substance delivers architecture without the weight penalty of heavy material.
- Soft temper at high substance creates a heavy bag that still collapses, which is the worst of both outcomes.
- Milled grain hides small scratches and softens the visual weight of a thick panel.
- Wax and oil finishes increase perceived stiffness slightly and must be accounted for when drape is critical.
There is a second illusion around durability. Within a sensible band, service life correlates more closely with fibre structure, tannage and grade than with substance. A 2.6 mm corrected-grain hide with a heavy pigment coat will abrade and crack sooner than a 1.6 mm full-grain hide of the same tannage, because the failure point is the finish and the grain layer rather than the bulk of the material.
Skiving, Splitting and Reinforcement: Engineering Around the Number
Skilled makers rarely build a bag from a single substance. Panels are split to a uniform thickness at the tannery, then skived locally where they must fold, turn or pass under a needle. This is how a structured bag with 2.0 mm body panels can still have slim, elegant facings and edges: the substance is high where stiffness is needed and reduced by half where the material must wrap.
- Machine skiving removes material to a set depth across a band, typically 8 to 15 mm wide, and leaves a feathered edge.
- Hand skiving with a French edge skiver gives a longer, more gradual taper that reads better on visible folds.
- Turned edges need the outer substance reduced dramatically, often to 0.6–0.8 mm, or the fold will bulk and crack.
- Edge paint adhesion improves on a slightly roughened, consistently skived edge; uneven skiving shows as ridges under the finish.
- Bonded interlining, canvas backing and foam lamination add stiffness without adding much weight or substance.
Hardware, Stitching and Machine Limits
Every mechanical operation in bag assembly has a clearance envelope, and substance pushes against all of them. Rivet shanks, magnetic closure prongs, Chicago screws and zip tapes are all dimensioned for a combined material stack; exceed it and the fitting will not seat, or it will seat with the leather compressed and the finish fractured. Stitch length follows substance too: coarse material needs fewer, longer stitches per inch, while fine material supports a denser seam.
| Operation | Practical stack limit | Consequence of overshoot |
|---|---|---|
| Rivet and burr setting | 3.0–4.5 mm combined | Shank too short to roll; head sits proud or pulls through |
| Magnetic closure prongs | 2.0–3.0 mm combined | Prongs bend instead of folding; closure loses strength |
| Machine lockstitch | ≈ 4.0–6.0 mm under the foot | Feed failure, skipped stitches, broken needles |
| Saddle stitching by hand | Up to ≈ 8.0 mm combined | Requires awl discipline and heavier thread |
| Zip insertion | 1.0–1.6 mm per facing after skiving | Tape bite, puckered facing, wavy zip line |
Stitch density should be recorded on the same sheet as substance. Industry practice for medium-weight leather runs at six to eight stitches per inch on machine and seven to nine on a hand-sewn saddle stitch; move beyond that on thick material and the perforations begin to crowd the seam line, weakening it rather than strengthening it. Where a design needs a dense decorative seam on heavy leather, the answer is to reduce substance at that seam, not to force the needle.
Writing Thickness Into the Technical Pack
The technical pack is where substance becomes enforceable. A sample that feels right in the hand is an opinion; a tolerance recorded on the pack is a term of the order, and it is the document our production partners in Quanzhou work from when they set the splitting and skiving plan. Our programme team recommends the fields below, completed for every component rather than for the bag as a whole.
One further field pays for itself: a finished target weight with an acceptance band. It is the only specification that a customer, a buyer and a quality inspector can all check without instruments, and it catches cumulative drift in substance, lining and hardware in a single reading.
Substance, temper, reinforcement and finish form one decision rather than four, and they are settled in the sampling round. Our team develops the specification with the brand, records it on the pack, and holds the retained swatch that subsequent seasons are matched against; examples of how these ranges resolve in finished product appear across the custom collections catalogue.
Set the right substance before sampling starts
Send the silhouette, target finished weight and intended use. The programme team will recommend substance, temper, skiving and reinforcement per component, then confirm them on a physical sample within the standard 6–10 working day window.
Frequently Asked Questions
What thickness leather is best for a handbag?
For a structured handbag, 1.6–2.0 mm in a firm temper is the usual answer, because panels must stand unaided and edges must take a clean finish. For a slouchy hobo or soft shoulder bag, 1.0–1.3 mm in a milled temper drapes better and feels lighter. Decide the silhouette first, then choose substance to serve it rather than defaulting to the heaviest material available.
How do you measure leather thickness?
Leather substance is measured with a dial or digital thickness gauge, reading in millimetres to one decimal place. Take readings at several points because a hide varies across the back and flank, and measure after finishing, since pigment, wax and embossing add substance. Record the temper alongside the figure, as two hides of equal substance can behave very differently in construction.
What is 4 oz leather in millimetres?
Four ounces is approximately 1.6 millimetres, since one ounce of leather equals one sixty-fourth of an inch, or about 0.4 mm. The conversion is approximate because tanneries round, and finishing can shift the final reading by a tenth of a millimetre. For specification purposes, quote the target in millimetres and treat the ounce figure as the descriptive shorthand used in the brief.
Is thicker leather always better for a bag?
No. Beyond the band required by the silhouette, extra substance adds weight, resists turning at the corners and can read as clumsy rather than luxurious. Durability within a sensible band depends more on grade, fibre structure and tannage than on bulk. A heavy corrected-grain hide will typically abrade and crack before a lighter full-grain hide of equivalent tannage.
Why does the same stated thickness feel different between suppliers?
Temper is set independently of substance through milling, boarding, staking and fatliquoring, so a soft 2.0 mm hide can drape more loosely than a firm 1.4 mm hide. Finish type contributes as well: heavy pigment stiffens a panel while a wax or oil finish softens the hand. Always approve a physical swatch rather than comparing numbers on a specification sheet.
What substance should a bag strap be?
A shoulder strap is normally specified at 2.2–3.0 mm, or built as two plies around a core, because it carries concentrated load and must resist elongation. Detachable webbing straps may be thinner where the load is shared with a fabric core. Whatever the construction, the fold at the end and the hole positions for buckles or rivets should be reinforced to prevent tear-out.
How much does leather thickness affect bag weight?
Bovine leather weighs roughly 0.8 to 0.9 kilograms per square metre per millimetre of substance. On a bag using 0.45 square metres of material, each additional millimetre adds about 380 grams before hardware and lining. Since fittings and interiors typically add a further 15 to 30 per cent, a modest change in substance can move a bag out of comfortable daily carry.
Can thick leather still be stitched on a machine?
Standard lockstitch machines handle a combined stack of roughly 4 to 6 millimetres beneath the foot, beyond which feed, needle penetration and thread tension all suffer. Heavier assemblies are saddle stitched by hand with an awl, or the panel is skived locally so the machine only ever meets a reduced stack. Stitch length should also open up as substance increases.
What is skiving and why does it matter for thickness?
Skiving thins leather over a narrow band so it can fold, wrap or pass under a needle without bulking. It matters because a bag almost never uses one substance throughout: a 2.0 mm body panel may need its facing reduced to 0.6–0.8 mm where it turns. Recording skive width, depth and residual thickness keeps that consistent across a production run.
Should the base of a bag be thicker than the body?
Usually yes, or reinforced. The base carries abrasion, sits on rough surfaces and takes the full load of the contents, so it is typically specified at 2.0–2.4 mm or backed with interlining. Reinforcement is often preferable to raw substance because it adds stiffness at lower weight and keeps the corners turning cleanly, provided it is recorded on the pattern.
What thickness suits a leather backpack?
A leather backpack shell generally works at 1.4–1.8 mm in a medium to firm temper. That range holds form under compression while keeping the empty weight reasonable, which matters because a backpack is carried for long periods. Harness attachment points, the base panel and the top handle should all be specified heavier or reinforced where the load concentrates.
How tight should the thickness tolerance be?
Plus or minus 0.1 millimetres is the practical standard for body panels, tightening to about 0.05 mm on turned or skived components where fit is critical. Tolerances tighter than that are difficult to hold across a natural material and tend to raise cutting waste without improving the finished result. Always state whether the tolerance applies before or after finishing.
Does leather thickness change after finishing?
Yes. Pigment coats, waxes, oils, embossing and plating all add measurable substance, and milling can compress a hide slightly in the opposite direction. For that reason a specification should state substance after finishing and name the exact tannery article. Approving a crust-stage figure is a common cause of bulk material arriving different from the approved sample.
What substance works for a leather wallet or card holder?
Wallets and card holders are normally built at 0.6–1.0 mm so they fold flat and slide into a pocket without bulk. Pockets within the wallet are often skived further, to around 0.4–0.6 mm, so stacked layers do not create a wedge. Full-grain is preferred at this substance because it resists tearing where the material is thin and repeatedly flexed.
How is thickness verified during production?
Inspectors check substance with a gauge on a sample drawn under AQL 2.5 single sampling at general level II, using the retained approved swatch as the reference. Results are recorded against the tolerance on the technical pack, and out-of-tolerance panels are rejected before assembly. Including substance in the written defect checklist is what makes the specification enforceable rather than advisory.
Can we change thickness after the sample is approved?
A change of substance after approval is treated as a specification revision and usually triggers a further sample, because it alters drape, finished weight, skiving plan, stitch length and hardware seating. Small adjustments within the stated tolerance can sometimes be absorbed. Anything beyond it should be re-sampled and re-costed before bulk begins, to protect the launch date.