
Quality control in bag craft is the structured inspection of a bag against its approved sample at defined stages, using documented checkpoints and a statistical sampling plan rather than a personal opinion. An inspector checks the shell, stitching, edges, linings, hardware, symmetry, dimensions and branding against the gold-sealed reference, then classifies every deviation as critical, major or minor. When the defect count falls within the acceptance number for AQL 2.5 single sampling under ISO 2859-1, the lot passes; when it does not, the lot is rejected, reworked or re-inspected.
What Quality Control in Bag Craft Actually Covers
The phrase covers far more than a visual pass over a finished bag. A serious programme treats quality control as a system that begins with incoming material and ends with the sealed carton, and each stage has its own checklist, its own tools and its own acceptance criteria. Inspectors are checking whether the object in front of them matches a documented standard, and whether the process that produced it is likely to produce the same result tomorrow.
- Incoming material: leather thickness, grain consistency, colour against the retained swatch, lining yardage and hardware finish.
- In-process checks: panel dimensions after cutting, skiving accuracy, seam alignment and the setting of stress-point reinforcement.
- Final inspection: the assembled bag examined against the approved sample for construction, symmetry and branding.
- Functional testing: zip runs, clasp engagement, handle load, magnetic closures and strap hardware under tension.
- Documentation: inspection reports, defect logs and retained reference samples that make a dispute objective rather than personal.
The Inspection Sequence, From Material to Packing
Checks sit at four points in a production run, and each exists to catch a different class of problem before it becomes expensive. Material that is wrong is cheapest to remove before it is cut, and a seam that is misaligned is cheapest to correct before the lining is fitted. The sequence is deliberate rather than ceremonial.
| Stage | What is examined | Typical reject trigger |
|---|---|---|
| Incoming material | Hide thickness, grain, colour, lining, hardware finish | Colour outside the approved tolerance or thickness under the minimum |
| Post-cutting and skiving | Panel dimensions, edge bevels, reinforcement placement | Dimensional drift beyond drawing tolerance or torn skive edges |
| In-process assembly | Seam alignment, stitch density, glue lines, hardware setting | Uneven stitch run, visible adhesive or a rivet set off-centre |
| Final inspection | Whole bag against the gold-sealed sample | Symmetry faults, edge-finish gaps, branding misplacement |
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
What Inspectors Check on the Shell and Stitching
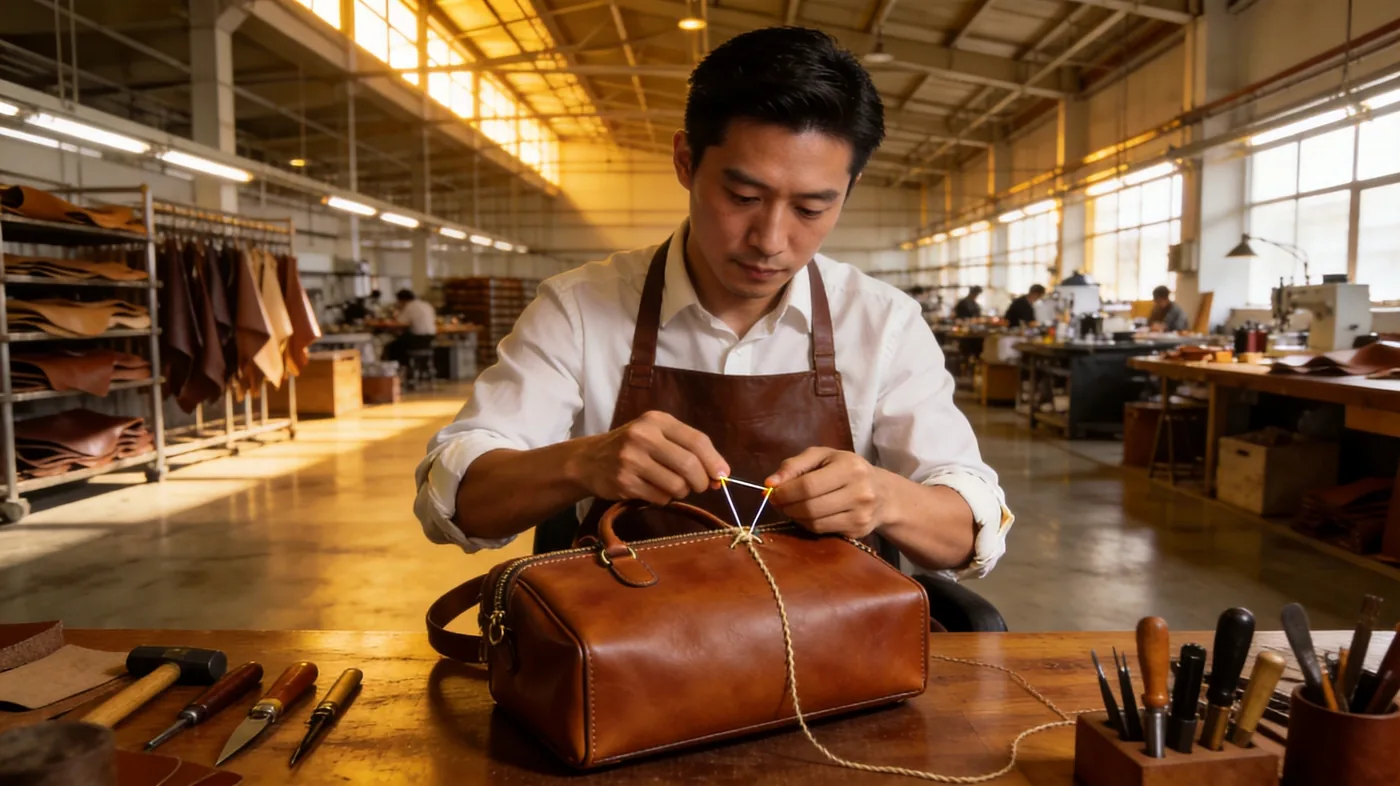
The shell and its seams carry most of the structural load, so they attract the most detailed checklist. Inspectors are not judging whether a bag looks nice; they are confirming that the construction matches the approved sample and that the workmanship falls within a defined tolerance band.
| Checkpoint | Method | Pass standard |
|---|---|---|
| Stitch density | Count stitches over a fixed length, usually per inch or per 3 cm | Within one stitch of the approved sample across all seams |
| Seam alignment | Sight along the seam line against the panel edge | No wandering, no drift beyond the seam allowance |
| Back-stitching | Inspect the start and end of each structural seam | Locked and secure, with no loose or cut thread ends |
| Panel symmetry | Measure matched panels against each other | Full panels within agreed tolerance; pattern-matched panels aligned |
| Grain direction | Compare the surface against lighting at an angle | Grain runs consistently across all panels of the same view |
| Dimension check | Measure height, width and depth at defined points | Within the tolerance stated on the tech pack |
| Reinforcement | Inspect handle roots, gusset corners and strap anchors | Reinforcement present, correctly placed and fully stitched |
Stitch density is worth dwelling on, because it is the single check most often misread by buyers new to inspection. More stitches per inch is not automatically better; a very short stitch perforates the leather and can weaken it at a fold, while a very long stitch leaves a gap a sharp object can catch. The correct density sits within one stitch of the approved sample, whatever that sample specifies, and the inspection confirms consistency rather than maximalism.
Edges, Hardware and Linings
These are the components a customer touches first and the ones where small lapses read as large quality signals. Each has its own inspection routine, and each tends to fail in a characteristic way that an experienced inspector learns to recognise on sight.
- Edge paint: continuous, even in thickness, no beading, no thin patches and no paint creeping onto the grain face.
- Burnished edges: uniform colour and sheen, no dry or furry patches where the fibre was not consolidated.
- Hardware: correct finish, correct orientation, no scratches, correct marking and firm, silent engagement.
- Zips: smooth full-length travel, no skipped teeth, tape cleanly stitched and the slider locking firmly at rest.
- Linings: no puckering, no slack, seams matched to the shell and the interior free of adhesive and stray thread.
- Branding: correct placement, depth and legibility for embossing, debossing and any hot-stamped foil.
Edge finishing deserves particular attention because it is where craft and process meet. A hand-painted edge and a machine-applied edge can both pass inspection, but only if each is judged against its own standard. An inspector looking at a painted edge is checking for a continuous, level film that follows the curve of the panel without thinning at corners, while a burnished edge is checked for a consolidated, sealed fibre rather than a soft, tufted one.
Defect Classification: Critical, Major and Minor
Inspection only becomes objective once every possible fault has been assigned a class. Classification is what allows an inspector to move through hundreds of units at a consistent standard rather than adjudicating each bag on instinct, and it is what allows a buyer and a supplier to agree in advance on what constitutes a failure.
| Class | Definition | Examples |
|---|---|---|
| Critical | A fault that makes the product unsafe, unusable or legally non-compliant | Sharp hardware edge, a strap anchor that fails under load, prohibited substance present |
| Major | A fault that a customer would reject or that materially shortens service life | Broken or skipped stitches, hardware that does not engage, a misaligned zip, torn lining |
| Minor | A cosmetic deviation that does not affect function or durability | Slight shade variation within tolerance, a faint handling mark, minor adhesive residue |
AQL 2.5 in Practice
Acceptable quality limit is a statistical method, not a promise that no defects exist. It defines how many defective units a random sample may contain before a lot is judged unacceptable, and it allows a buyer and a supplier to agree on a consistent, defensible threshold rather than inspecting every single piece or none at all.
| Element | Setting | Why it matters |
|---|---|---|
| Standard | ISO 2859-1 | An internationally recognised framework both sides can reference |
| Level | AQL 2.5 | A demanding but realistic bar for consumer leather goods |
| Sampling | Single sampling plan | One sample, one decision, no staged accept or reject |
| Inspection level | General level II | The default rigour for normal commercial inspection |
| Outcome | Accept, reject, rework or re-inspect | Defines what happens to the lot rather than leaving it to chance |
The practical consequence is that a batch is judged as a batch. A sample is drawn at random from the finished goods, each unit is examined against the checkpoints and the defect log, and the arithmetic then determines whether the lot is released. Because the plan is fixed in advance, neither side can move the goalposts after the fact, which is the entire point of committing to it in the quotation.
In-Process Checks Versus Final Inspection
Buyers often assume that inspection means a single visit at the end. It does not. End-of-line inspection catches what has already gone wrong; in-process checks prevent faults from being repeated across hundreds of units. The two are complementary, and a programme that relies on final inspection alone will always carry a higher rework cost.
| Dimension | In-process check | Final inspection |
|---|---|---|
| Timing | During cutting, assembly and finishing | After the lot is complete and packed or pre-packed |
| Purpose | Prevent repetition of a systematic fault | Confirm the finished lot meets the approved standard |
| Scope | Targeted at the operation in progress | Whole bag against the gold-sealed sample |
| Cost of a miss | Low, if caught early | High, because value has been added throughout |
| Reported as | Line correction and rework instruction | Lot acceptance, rejection or re-inspection |
For a programme aiming at consistent quality, the in-process discipline matters more than the final sheet. Catching a drifting stitch setting at unit fifty is a line adjustment; catching it at unit five thousand is a rework programme. The programme team schedules these checks as part of the run rather than treating them as an optional extra.
Building a QC Specification That Holds
A quality control specification is the document that makes inspection possible, because an inspector cannot confirm compliance with a standard that has never been written down. It should be short enough to be used and precise enough to be enforceable, and it should be agreed before the sample is approved rather than assembled during the run.
Where a buyer intends to use an independent third-party inspector, the specification should be shared in advance so that the auditor examines the same checkpoints and applies the same plan. Third-party inspection does not replace an internal system; it verifies one, and it works best when the internal standard is already documented. Our production floor in Quanzhou runs to the same AQL 2.5 single sampling plan whether the buyer attends in person or appoints an agency, which keeps the result consistent between visits.
Quality control in bag craft is ultimately a discipline of definition. A bag passes because both sides agreed in advance what passing means, and the inspector's role is to apply that definition consistently. Programmes that invest in classification and in-process checks spend far less time arguing about finished goods, and they ship with a confidence that rests on evidence rather than optimism. Related craft techniques sit alongside this work across the wider leather craftsmanship techniques pillar.
Make quality a specification, not a hope
Send the style, the tolerances and the defect concerns that matter most to your line. The programme team will return a written inspection plan with checkpoints and an AQL 2.5 single sampling scheme before a single unit reaches the line.
Frequently Asked Questions
What does an inspector check on a leather bag?
An inspector works through a documented checklist covering the shell, stitching, edges, linings, hardware, dimensions, symmetry and branding, comparing each against a gold-sealed approved sample. Seam density, back-stitching, edge-paint continuity and hardware engagement all have their own pass standards. Functional checks confirm zips run freely and handles hold under load, and every deviation is classified before the lot is accepted or rejected.
What does AQL 2.5 mean in bag inspection?
AQL 2.5 is the acceptable quality limit applied to a single sampling plan, most often under ISO 2859-1 at general level II. It sets the number of defective units a random sample may contain before a lot is judged unacceptable. It is a statistical threshold agreed in advance so that both buyer and supplier apply the same rule, not a promise that every bag is flawless.
How many bags are inspected in a bulk order?
The quantity is set by the sampling plan rather than chosen arbitrarily. Under ISO 2859-1 single sampling at general level II, the sample size scales with the lot size, so a larger production run draws a proportionally defined sample rather than a fixed number. The exact figure is stated on the inspection plan and is determined by the lot size, not by the buyer's preference.
What is the difference between a major and a minor defect?
A major defect is one a customer would reject or that materially shortens the bag's service life, such as a skipped stitch on a load-bearing seam or hardware that will not engage. A minor defect is a cosmetic deviation that does not affect function or durability, such as slight shade variation within tolerance. Critical defects, such as unsafe hardware, make the product unusable or non-compliant and trigger rejection outright.
Should quality control happen during production or only at the end?
Both, and in-process checks matter more for consistency. Catching a drifting stitch setting or a mis-cut panel early is a small line correction, while catching the same fault after the lot is finished is a full rework programme. Final inspection confirms the finished goods meet the standard; in-process checks stop a systematic fault from being repeated across hundreds of units.
What is a gold-sealed sample?
It is the approved reference bag, retained and marked by both buyer and supplier, against which every production unit is compared. It resolves ambiguity, because a physical object settles questions that a written description cannot. It should be signed off before bulk begins, and both parties should hold an identical retained piece so that any later dispute has an agreed benchmark.
Can a third-party inspector replace internal quality control?
No. A third-party inspector verifies an internal system rather than substituting for one. Their value comes from independence and from applying a documented standard consistently, which is why the specification and the AQL plan should be shared with them in advance. The internal system does the daily work; the third party confirms it at a defined point, most often before shipment.
What happens if a lot fails inspection?
The agreed remediation applies. Depending on the defect class and the count, the lot is reworked and re-inspected, sorted with the defective units removed, or rejected entirely. What matters is that this is decided before production rather than negotiated after a failure, so that responsibility and cost are clear and the timeline can be adjusted without ambiguity.
How is edge finishing checked during inspection?
It depends on the method. A painted edge is examined for a continuous, level film that does not thin at corners or creep onto the grain face, while a burnished edge is checked for a consolidated, sealed fibre with uniform colour and sheen. Both methods can pass, but each is judged against its own standard rather than against the other, and the standard is fixed at sampling.
What stitch density is acceptable in bag quality control?
Acceptable density is defined by the approved sample rather than by a universal figure. Inspectors count stitches over a fixed length and confirm the run sits within one stitch of the reference across all seams. Consistency matters more than a high count, because an over-dense stitch perforates the leather at folds while an over-long stitch leaves a gap that can catch.
Is colour variation a defect in a leather bag order?
It depends on the tolerance agreed at sampling. Natural leather varies between hides and across a single hide, so a defined colour band is normal and expected. Variation within that agreed band is a minor or non-defect, while a lot that sits visibly outside the retained swatch is a major issue and should be raised before the goods are packed.
How long does a final inspection take?
It depends on the lot size, the sample size and the number of checkpoints, but a final inspection is a scheduled stage rather than an interruption. In a standard programme it sits inside the 35 to 50 day bulk window after sample approval, positioned so that any rework can be completed without delaying the shipment date.
What tools do bag inspectors use?
The toolkit is deliberately simple. Inspectors work with a ruler or steel tape for dimensions, a stitch counter or a magnifier for seam density, a colour-approved light box or a neutral viewing light for shade, and the retained swatch for hand and finish comparison. A load test rig checks handle and strap strength, and a torque or pull gauge confirms hardware engagement. Digital calipers verify leather thickness at defined points, and a camera documents every recorded defect.
Can a brand set its own AQL level?
Yes, and many do. AQL 2.5 at general level II is a sensible default for consumer leather goods, but a luxury line with a very low tolerance for cosmetic variation may tighten the cosmetic class while keeping functional defects at the standard level. The essential point is that the level is agreed and written into the quotation before production, because changing it once a lot is finished turns a clear standard into a dispute.
How is handle and strap strength inspected?
Handle and strap inspection combines a visual check with a load test. The inspector confirms that reinforcement is present at the roots, that the stitching is locked and secure, and that no seam sits where the full load concentrates. A defined weight is then applied to the handle for a set period to confirm the assembly holds. Most handle failures trace back to reinforcement that was omitted or misplaced rather than to the leather itself.
Do you inspect every bag or only a sample?
Final inspection follows the agreed sampling plan, most commonly AQL 2.5 single sampling under ISO 2859-1 at general level II, which examines a defined random sample rather than every unit. Individual operations such as hardware setting and edge finishing are checked in-process across the run, so the combination gives both statistical assurance and continuous coverage of the riskiest steps.