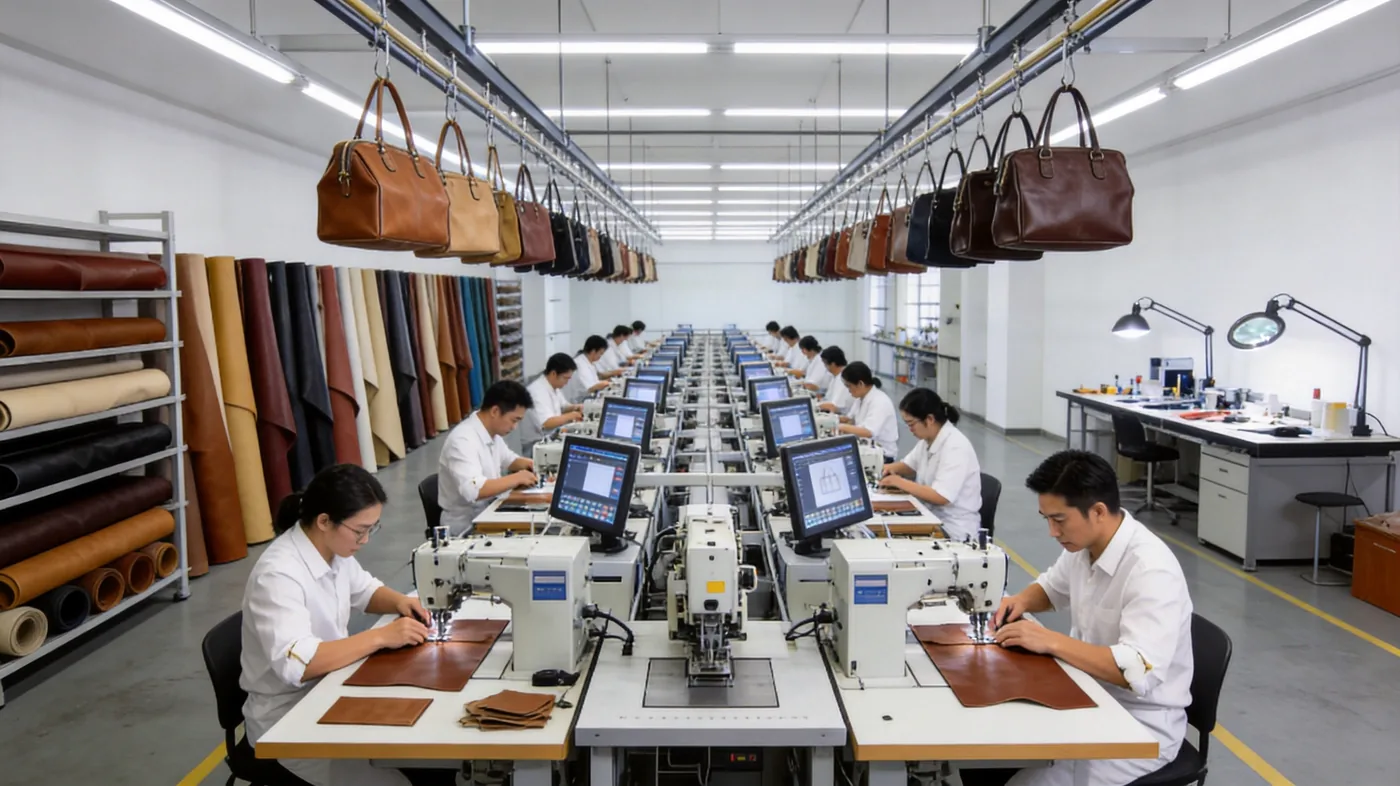
A bespoke leather bag is a bag engineered upwards from the hide for a single brief: the tannery and the substance are chosen for that silhouette, the panels are cut from a marker planned around that specific leather, and the construction sequence, hardware and inspection standard are written down before a deposit moves. The craft that determines whether the bag lasts three years or thirty is largely invisible in a photograph — it sits in selection at the tannery, in yield at the cutting table, in tension at the machine and in patience at the edge bench. This guide maps where that craft lives, what each decision costs, and which specification choices separate a bag still improving at ten years from one that looks tired after a season.
What "Bespoke Leather Bag" Means in the Trade
In retail copy the word describes a mood. In a production brief it describes a set of documents and a set of decisions that belong to you. A bespoke leather bag starts with a specification drafted for one buyer: the silhouette is drawn from the brief, the pattern is graded for it, and the leather is called out by tannery reference, finish and substance rather than by a generic category. Remove every logo, tag and dustbag and what remains could only have come from your brief. That test is worth running in thirty seconds before you sign anything, because the pricing, the lead time and the exclusivity clause all follow from it.
Most collections are mixed rather than pure, and that is a rational choice rather than a compromise. A launch range typically pairs one bespoke hero style, the piece that carries the press story and the visual identity, with three or four adapted core styles that carry the margin and reach the floor sooner. As sell-through data accumulates, the ratio tends to invert. What matters is that the brief names the tier each style occupies, because the development cost, the sampling window and the exclusivity language are all derived from that classification.
| Tier | Pattern and specification | Sampling window | Development cost | Best used for |
|---|---|---|---|---|
| Bespoke | Newly drafted; buyer's property by agreement | 6–10 working days per round; 12–15 on complex builds | Highest; amortised over the run | Signature styles and exclusive capsules |
| Made-to-measure | Producer base pattern, dimensions held for buyer | 6–10 working days | Low; pattern adjustment only | Category fillers sized around a device or garment |
| Customised | Producer pattern unchanged | 6–10 working days | Minimal | Colourway extensions and seasonal refreshes |
| Private label | Producer retains ownership | No development round | None | Speed-to-market and promotional lines |
| Small-batch pilot | Either, subject to feasibility | Same as the parent route | Higher unit cost, lower commitment | Market testing before full commitment |
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
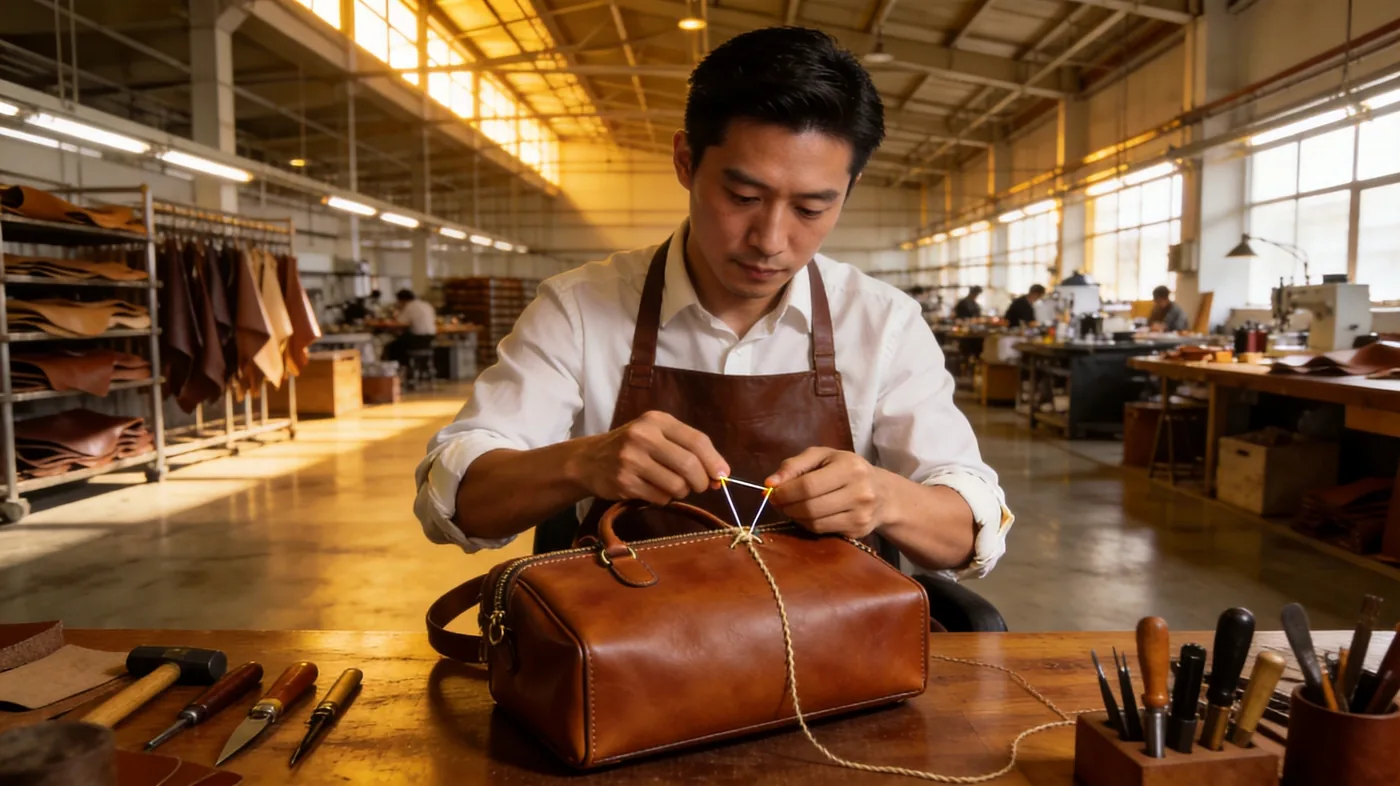
Choosing the Hide: Where Quality Is Decided
Leather is an agricultural material traded by the hide, and no two hides are identical. The decisions taken at selection determine the appearance, the handling and much of the durability of the finished bag, and they are irreversible: once a panel is cut, its position on the animal is fixed for the life of the product. Buyers often spend their effort on the visible specification — colour, hardware, stitch colour — while the decision that most affects how the bag looks in five years is made by somebody standing at a bench with a lamp and a tolerance card.
| Leather | Character | Typical substance | What it suits | Watch for |
|---|---|---|---|---|
| Full-grain bovine | Natural grain intact, develops patina | 1.2–2.2 mm | Structured totes, briefcases, holdalls | Scarring on lower grades; requires careful selection |
| Top-grain / corrected | Surface lightly corrected and finished | 1.0–1.6 mm | Uniform production runs, branded lines | Heavier finish can mask poor substrate |
| Calfskin | Fine, tight grain, supple hand | 0.9–1.4 mm | Top-handle bags, evening pieces | Cost and lower abrasion resistance at thin substances |
| Suede and nubuck | Napped surface, matte, tactile | 1.0–1.6 mm | Soft bodies, linings, accent panels | Water staining and pile burnishing in high-contact zones |
| Vegetable-tanned | Firm, pale, darkens with use | 1.8–3.0 mm | Bridle work, structured cases, belts | Slow break-in; stiff at heavy substances |
| Exotic (crocodile, ostrich, lizard) | Distinctive scale or quill pattern | Varies by species | Hero pieces and limited capsules | CITES documentation and restricted supply |
Two practical points follow from that table. The first is substance: the thickness chosen has to suit the construction, not the mood board. A soft hobo body wants a pliable 1.0–1.2 mm, while a framed briefcase wants 1.8–2.0 mm or a laminated build, and specifying the wrong one produces either a bag that collapses or one that fights the machine. The second is lot consistency. A colour standard held across a 500-piece run requires hides from a single dyed lot, and across repeat orders it requires a tannery able to reproduce that lot. Ask how the reference is retained, because a swatch card alone will not settle a dispute twelve months later.
Tanning, Finish and Colour: The Decisions Behind the Surface
Tanning converts a perishable skin into a stable material, and the route chosen shapes everything downstream — the hand, the colour depth, the way the surface ages, and the set of chemical tests the finished bag has to pass. Chrome tanning dominates commercial production because it is fast, consistent and produces a supple leather in a wide colour range. Vegetable tanning is slower and yields a firmer, paler leather that darkens markedly with handling. Neither is intrinsically superior; each suits a different product promise, and the honest answer for a given brief depends on how the bag is meant to age.
| Route | Process character | Hand and appearance | Ageing behaviour | Compliance notes |
|---|---|---|---|---|
| Chrome | Days; chromium salts; high consistency | Supple, wide colour range | Stable colour; modest patina | Restricted-substance testing under REACH is routine |
| Vegetable | Weeks; plant tannins; small batches | Firm initially, deepens in tone | Strong patina; darkens with light and handling | Often specified for chrome-free claims; verify rather than assume |
| Combination | Chrome base with vegetable retannage | Balanced temper and colour depth | Moderate patina development | Verify the claim with documentation from the tannery |
| Chrome-free (alternative) | Aldehyde or synthetic tanning agents | Pale, firm, low shrinkage | Varies widely by chemistry | Requires explicit test evidence for the destination market |
- Aniline versus pigment. Aniline leather carries dye with little surface coverage, so the grain shows through and the colour is deep but vulnerable to staining. Pigmented finishes cover the surface and resist marking at the cost of some natural character. Semi-aniline sits between the two and is often the sensible production default.
- Finish protection. A light protective topcoat reduces water spotting and crocking — the transfer of colour onto light clothing — which is the single most common complaint on saturated dyed leathers.
- Colour standard. Approval against a physical reference under controlled lighting, with an accepted tolerance range, prevents the most frequent bulk dispute: a bag that is technically within tolerance but visibly different from the sample the buyer approved.
- Crocking and rub fastness. Where a deep or dark shade is specified, rub fastness should be tested before bulk rather than discovered on a customer's coat.
- Documentation. Traceability back to an audited tannery, most commonly one assessed under the Leather Working Group protocol, is increasingly a procurement requirement rather than a marketing asset.
Construction: What the Craft Actually Consists Of
The romance of leather craft is in the finished object; the substance of it is in a sequence of operations, each with a failure mode and each cheapest to correct at the moment it happens. A bag that looks identical in a photograph can be assembled in a dozen different ways, and the difference shows up at the handle root after a year of real load, at the edge paint after a winter, or at the zip after a few hundred openings. Understanding the sequence lets you write a specification that inspectors can actually enforce.
- Selection and cutting. Hides are graded, flawed areas are marked, and panels are cut to a planned marker that maximises yield while keeping structural panels out of the weaker belly and neck areas.
- Skiving and preparation. Edges are thinned where panels will fold or overlap, so that seams lie flat rather than building bulk at the join.
- Splitting and laminating. Where a panel needs body, leather is laminated to a reinforcement; where it needs to be lighter, it is split to a precise substance.
- Assembly and sewing. Panels are closed in a defined order with a specified stitch density and thread; the sequence determines where stress concentrates.
- Edge finishing. Edges are sanded, painted or burnished; on a full-grain build this is where most visible quality judgment occurs.
- Hardware setting. Rivets, screws, feet and plates are set with the correct tool and backing; poorly set hardware is the leading cause of early returns.
- Lining and closing. Interiors are inserted and attached so they float cleanly rather than dragging, then the bag is turned, shaped and rested.
- Shaping and final checks. The bag is dressed, inspected against the sealed reference, cleaned and packed to the carton specification.
| Operation | What goes wrong | What to specify |
|---|---|---|
| Cutting | Structural panels taken from weak belly sections | Panel placement rules by hide area; yield target agreed in writing |
| Skiving | Bulk at folds; visible ridge along seams | Skive width and residual substance per panel |
| Sewing | Seam slippage; broken stitches at stress points | Stitch density per inch, thread type, seam allowance, back-tack at ends |
| Edge finishing | Peeling paint, tacky edges, uneven colour | Number of coats, sanding between coats, gloss level |
| Hardware setting | Spun rivets, scratched plates, loose feet | Backing washer specification and setting tool, protection during assembly |
| Lining | Dragging interior, puckering at the mouth | Attachment method and ease allowance |
| Final inspection | Subjective grading after goods are finished | Defect classification and acceptable quality limit agreed before bulk |

From Brief to Bulk: The Programme Sequence
A programme is a chain of gates, and each gate produces an artefact you can approve or reject. The gates exist because the cost of a correction rises roughly by an order of magnitude at each stage: a changed dimension is a pencil stroke during drafting, a second sample during development, and an entire run if it surfaces after cutting. Buyers who compress the early gates to save a fortnight regularly lose a season to the ones they skipped.
| Gate | Artefact you receive | Window | Decision you own |
|---|---|---|---|
| Feasibility | Written note with construction route and cost band | A few working days | Whether the brief is buildable at the target price |
| Specification | Technical pack and bill of materials | One to two weeks with the buyer | Approving materials by tannery or mill reference |
| Pattern and sourcing | Pattern, graded marker, yield calculation | Concurrent with specification | Confirming substance, temper and colour standard |
| Prototype | First physical build with a comment log | 6–10 working days | Fit, balance, closure alignment, strap geometry |
| Correction | Corrected sample | 6–10 working days; 12–15 for complex builds | Whether the comments were understood |
| Compliance | Test reports against the required framework | Laboratory dependent | Authorising bulk to proceed |
| Pre-production | Golden sample sealed and retained | Sign-off dependent | Accepting the bulk-intent material lot |
| Bulk | Production units with in-line records | 35–50 days after approval | Release for inspection |
| Inspection and release | Report against the agreed sampling plan | A few working days | Accept, rework or reject the shipment |
| Logistics | Shipment with commercial documents | Transit dependent | Incoterm and customs documentation |
The gate most often skipped is the pre-production seal, and it is the one that matters most. Without a physical sample retained from the bulk-intent lot, every later disagreement about colour, temper or finish becomes a contest of opinions rather than a comparison against an agreed object. Insist that the seal is signed, dated, photographed and stored, and that a duplicate travels with the shipping documents when the goods leave.
Specification, Compliance and Inspection
Quality in a bespoke programme is not a sentiment, it is a written standard agreed before production begins. The specification names the material by reference, the construction sequence, the tolerances and the defect classification; the inspection plan then measures production against it. Agreeing these after the goods exist converts a technical question into a commercial negotiation, and the party holding the goods usually wins it.
| Defect class | Examples in leather bags | Consequence at inspection |
|---|---|---|
| Critical | Broken handle root, failed load test, sharp hardware edge, non-compliant restricted substance | Automatic rejection of the lot; escalation beyond the sampling plan |
| Major | Visible grain damage on a front panel, misaligned closure, peeling edge paint, wrong hardware finish | Counted against the acceptable quality limit for majors |
| Minor | Slight stitch irregularity inside a pocket, dust marks removable in cleaning, carton scuffing | Counted against the limit for minors; usually tolerated within threshold |
- Name the standard. A single sampling plan built on ISO 2859-1 at an AQL of 2.5 under general level II is the common trade baseline; state it in the purchase agreement, not in an email.
- Test to the destination market. Restricted-substance screening under REACH is routine for the European Union, CPSIA applies to children's products in the United States, and textile components are frequently certified to OEKO-TEX standards.
- Classify defects in writing. A defect list distinguishing critical, major and minor faults removes the argument about whether a fault is acceptable before the argument starts.
- Fix the tolerance. Dimensional tolerance, colour tolerance and stitch tolerance should each carry a number, because a tolerance without a number is a preference.
- Inspect before release. Inspection performed while goods remain in the country of production keeps the remedy available; inspection performed after arrival leaves you negotiating from a warehouse.
What a Bespoke Leather Bag Costs, and Why
The unit price of a bespoke leather bag is the sum of material, labour, overheads, development and margin, and the parts buyers tend to overlook are the ones that move most. Material is usually the largest single line, but its cost is governed by yield — the proportion of the hide that becomes saleable panels — which is a function of the pattern and the grade of leather rather than of the tannery's price list alone. Labour varies less than buyers expect between competing partners and more than they expect between construction routes.
| Cost driver | Why it moves | How to control it |
|---|---|---|
| Hide grade and selection | Higher grades reject more area; price rises with the selection standard | Match grade to panel: prime grain on visible panels, utility grades inside |
| Cutting yield | Pattern geometry and defect placement decide the waste percentage | Refine the marker and allow panel placement rules in the specification |
| Substance and lamination | Thicker leather and reinforced builds consume more material | Specify substance per panel rather than a single figure for the bag |
| Construction complexity | Framed openings, gussets and moulded shells add operations | Simplify geometry where it is invisible; spend complexity where it shows |
| Hardware | Solid brass and custom tooling cost multiples of stock zamac | Use custom hardware on one visible element only |
| Development and tooling | Pattern drafting, knives, moulds and plates are fixed costs | Amortise over repeats; confirm ownership in the agreement |
| Compliance testing | Each material and colourway may need its own submission | Plan the test matrix before sampling rather than after approval |
Freight and settlement structure round out the picture. A quotation that lands goods on your dock and one that leaves them on a vessel differ by a sum that rate volatility can turn into a season's margin. The conventional structure is T/T with a 30% deposit against materials and development and the 70% balance before shipment, and the quotation should state the Incoterm explicitly so that two offers can be compared honestly.
Planning a First Run Without Wasting It
A first bespoke run teaches you things no amount of pre-production correspondence can, and the objective should be to buy that lesson at the lowest tolerable cost. That means choosing one style to carry genuine development, keeping the specification tight on the elements that define the brand, and resisting the urge to resolve every aesthetic question inside the first order. The most common failure is a first brief that tries to prove everything at once and therefore proves nothing cleanly.
| Decision | Conservative first run | Aggressive first run | Trade-off |
|---|---|---|---|
| Number of bespoke styles | One hero, three to four adapted | Full bespoke range | Development cost against differentiation |
| Material | Mid-weight full-grain or lightly corrected bovine | Exotic or very soft nappa | Tolerance window against impact |
| Colourways | One core plus one accent | Four or more | Lot minimums against choice |
| Hardware | Stock finishes with one custom plate | Fully custom tooling | Lead time against identity |
| Quantity | Standard minimum on the hero, pilot elsewhere | Standard minimum across the range | Commitment against unit cost |
- Write the brief around use, not appearance. What the bag carries, how it is carried and where it is put down determine substance, structure and reinforcement.
- Fix the three numbers that matter. Target retail price, target quantity and deadline; everything else is negotiable and should be presented as such.
- Ask for the artefacts. A versioned technical pack, a marked pattern with a yield calculation, a line-item bill of materials and a retained seal are what separate a programme from a decoration service.
- Plan the repeat before the first run. Reserved material lots, retained tooling and a documented tolerance make the second season materially cheaper than the first.
- Start the conversation early. Sampling, testing, bulk and freight compound; the calendar, not the price, is the usual constraint on a launch date.
What the premium on a bespoke leather bag purchases is control: over the material, over the construction, over the tolerance and over the standard to which the result is judged. That control is worth little if it is left implicit, and worth a great deal once it is written down, sealed against a physical reference and inspected against an agreed plan. Programmes begin with a conversation rather than a purchase order, and the contact channels route directly to the team that will carry it.
Commission your bespoke leather bag programme
Send drawings, target price, intended volume and deadline. The programme team will return a written feasibility note covering hide selection, construction route, sampling window and cost band before any deposit is discussed.
Frequently Asked Questions
What makes a leather bag genuinely bespoke rather than customised?
A bespoke bag has a specification drafted for one buyer: the pattern is new, the leather is called out by tannery reference and substance, and the construction sequence, tolerances and inspection standard are written into a technical pack you own. A customised bag is a shared base pattern altered in colour, hardware or branding. Strip the logos and the distinction becomes obvious — a bespoke bag still belongs only to your brief, while a customised one is recognisably somebody else's geometry.
Which leather is best for a first bespoke bag run?
A mid-weight full-grain or lightly corrected bovine leather offers the widest tolerance window: it forgives machine settings and operator variation, resists abrasion and improves with handling. Very soft nappa and heavy bridle leather are less forgiving, demanding tighter process control and a more experienced line. For a first run, choose the material that tolerates imperfection rather than the one that photographs most attractively.
How long does a bespoke leather bag programme take from brief to delivery?
Plan on 6–10 working days for each sampling round, rising to 12–15 days where the build demands it — framed openings and multi-compartment cases fall into that bracket — followed by 35–50 days of bulk once the sample is signed off. Laboratory testing for restricted substances, freight and customs clearance sit on top of those figures. A first programme is realistically measured in months from first conversation to goods on the dock, which is why early engagement protects a launch date better than expedited production.
What is the minimum order quantity for bespoke leather bags?
Most programmes start at 500 units per style and per colourway. That figure reflects line set-up economics — machine settings, operator briefing, material lot minimums and inspection sampling — rather than any constraint on the leather itself. Small-batch pilots below the threshold can be negotiated where the construction allows it and where the purpose is market testing before a full commitment; the unit cost is higher, but the alternative is an untested assumption.
Is full-grain leather the right choice for every bespoke bag?
Full-grain retains the natural grain surface, so it develops patina and generally resists fatigue better over years of use. Top-grain has the surface lightly corrected and finished, which gives greater uniformity across a production run and better resistance to marking. Full-grain is the better choice where character and longevity are the promise; corrected top-grain is often the better choice where 500 units must look identical to one another on a shelf.
How much does leather thickness affect how a bag performs?
Substantially. A soft, unstructured body wants a pliable 1.0–1.2 mm, while a framed briefcase or structured tote needs 1.8–2.0 mm, or a thinner leather laminated to a reinforcement. Specifying the wrong substance produces either a bag that collapses under its own weight or one too stiff to close cleanly. The specification should state substance panel by panel rather than a single figure for the whole bag, because different panels do different work.
Can a bespoke leather bag be made water-resistant?
Resistance can be improved considerably, but no leather bag is waterproof. A protective topcoat applied at the tannery, a wax or fluorocarbon-free finish applied after manufacture, sealed seams and covered zips all reduce water ingress. The limitation is structural: stitching perforates the leather, and no finish survives immersion. Where weather exposure is routine, waxed cotton or a coated textile panel is a more honest specification than a leather one.
Why do two bags from the same order sometimes differ in colour?
Leather is a natural material dyed in lots, and variation between lots is normal even within one tannery specification. Within a single run the risk is controlled by cutting from one dyed lot and by approving colour against a physical reference under controlled lighting with a stated tolerance. Across repeat orders, the risk returns: insist that the retained reference and the lot formulation are documented so the tannery can reproduce the shade rather than approximate it.
What inspection standard should be agreed before bulk production?
The common trade baseline is a single sampling plan built on ISO 2859-1 at an AQL of 2.5 under general level II, agreed in writing before bulk is authorised and supported by a written defect classification separating critical, major and minor faults. Critical defects such as a failed load test or a sharp hardware edge should fall outside the sampling logic entirely and trigger lot-level escalation rather than a numeric threshold.
Which compliance frameworks apply to leather bags sold in Europe and the United States?
Restricted-substance testing under REACH is routine for the European Union and covers substances including certain chromium compounds and azo dyes. In the United States, CPSIA applies principally to children's products, while California's Proposition 65 drives practical testing decisions for adult accessories. Textile components such as linings and webbing are frequently certified to OEKO-TEX standards. Each material and colourway may require its own submission, so plan the test matrix during sampling rather than after approval.
Do I need my own drawings before approaching a production partner?
Drawings help but are not required. A usable opening brief contains reference photographs, target dimensions, intended contents, target retail price, quantity and deadline. What matters more than draughtsmanship is knowing which elements define the brand and which are negotiable, because a feasibility note tests exactly that distinction against material availability, construction capability and realistic labour cost.
Who owns the pattern and tooling developed for my bag?
Patterns drafted to your brief can be contractually ring-fenced for your exclusive use, and tooling you have paid for is normally yours to redirect. Both depend entirely on being written into the agreement before development begins; absent an explicit clause, default positions vary and a pattern may remain available to other buyers. Confirm ownership, permitted use, territory, duration and what happens to tooling if the programme moves.
How should a bespoke leather bag be cared for after purchase?
Keep it away from direct heat, store it stuffed and in a breathable dustbag, and wipe it with a dry cloth after use. Condition sparingly — once or twice a year is usually sufficient — using a product compatible with the finish, and test any treatment on an inconspicuous area first. Suede and nubuck need a brush rather than a cream. Address stains quickly by blotting rather than rubbing, and accept that some marking is the material ageing rather than failing.
Are exotic leathers a practical choice for a production run?
They are practical only under narrow conditions. Crocodile, ostrich, lizard and snake require CITES documentation for cross-border movement, supply is limited and graded by tile or skin size, and cutting yield is far lower than for bovine hides because the usable area is irregular. Exotics suit hero pieces and limited capsules where the documentation burden is proportionate; they rarely suit a core style that must be replenished season after season.
What payment and shipping terms are usual for a bespoke leather bag order?
The conventional structure is T/T with a 30% deposit to release materials and development, and the 70% balance before shipment, with tooling typically invoiced separately at the outset. FOB Xiamen is the standard quotation basis, with EXW, CIF or DDP available on request. Insist that the Incoterm appears on the quotation, because the same bag produces materially different landed costs under each and the difference is rarely small at distance.
Is a bespoke leather bag a sound investment compared with a designer bag?
It depends on which value you are measuring. A designer bag carries resale liquidity and brand recognition that a bespoke piece cannot match. A bespoke bag carries specification control, exclusivity and a cost structure that improves on repeat, and it can be maintained and repaired for decades. If the objective is a durable object built exactly to requirement, bespoke wins; if the objective is a store of exchangeable value, established brands retain the advantage.