
Bespoke bags are bags that did not exist until you commissioned them: the silhouette is drawn from your brief, the pattern is drafted and graded for that silhouette, and the leather, lining, hardware and construction sequence are selected to suit it. They cost more than catalogue equivalents because that development is paid for inside the first order — new patterns, new tooling, longer sampling rounds and a line learning curve all sit in unit one. This guide sets the definition the trade actually uses, walks the bespoke process gate by gate, itemises the cost drivers, and gives you the questions that reveal whether a programme offered to you is genuinely bespoke.
What Bespoke Means in Practical Terms
The word is used loosely in retail copy and precisely in a production brief. In the narrow trade sense, bespoke bags are specified by the buyer and engineered from nothing: no shared base pattern, no existing cutting file, no tooling already paid for by somebody else. The practical test is straightforward and takes thirty seconds in a showroom. Remove every piece of branding from the bag — the logo plate, the lining print, the dustbag. If what remains is recognisably a style someone else also sells, you bought customisation. If what remains could only have come from your brief, you bought bespoke.
The distinction matters commercially because it determines three outcomes that show up on your P&L rather than in a specification sheet. Exclusivity is the first: only a newly drafted specification can be contractually ring-fenced from other buyers, and only a design you own can be enforced against a copycat. Cost structure is the second: development costs amortise over the run, so the same bag priced at 500 pieces and 5,000 pieces differs by far more than the material line. Control is the third: a bespoke specification lets you dictate tolerance, construction sequence and inspection standard, whereas a shared base pattern comes with the producer's tolerances embedded in it.
Most real programmes are mixed rather than pure. A launch collection frequently pairs one bespoke hero style — the piece that carries the press story and the visual identity — with three or four made-to-measure core styles that carry the margin and ship faster. As the label matures and sell-through data accumulates, that ratio tends to invert. There is nothing evasive about a mixed programme provided the brief states which tier each style occupies, because the pricing, the lead time and the exclusivity clause follow directly from that classification.
| Tier | Pattern ownership | Typical sampling window | Minimum volume | Best used for |
|---|---|---|---|---|
| Bespoke | Newly drafted, buyer's property by agreement | 6–10 working days per round, 12–15 for complex builds | 500 pieces per style/colourway | Signature styles, exclusive capsules, hero products |
| Made-to-measure | Producer's base pattern, dimension variant held for buyer | 6–10 working days | 500 pieces per style/colourway | Category fillers sized to a device or garment |
| Customised | Producer's pattern unchanged | 6–10 working days | 500 pieces per style/colourway | Colourway extensions and seasonal refreshes |
| Private label | Producer retains full ownership | Existing sample, no development round | 500 pieces per style/colourway | Speed-to-market ranges and promotional lines |
| Small-batch pilot | Either, subject to feasibility | Same as parent route | Negotiated pilot quantity below standard minimum | Market testing before a full commitment |
Read that table as a decision tool rather than a hierarchy. A pilot run below the standard minimum is often the smarter opening move for a new label: it buys you sell-through evidence at a tolerable premium before the full commitment. Buyers comparing bespoke bags UK suppliers with programmes elsewhere in Europe frequently find that the limiting factor is not geography but whether the partner can hold a written tolerance across a repeat order twelve months later.
Programme parameters at a glance
| Parameter | Commitment |
|---|---|
| Minimum order quantity | 500 pieces per style / colourway |
| Sampling lead time | 6–10 working days (12–15 days for complex constructions) |
| Bulk production lead time | 35–50 days after sample approval |
| Inspection standard | AQL 2.5 (ISO 2859-1), single sampling, general level II |
| Incoterms | FOB Xiamen — EXW, CIF and DDP available on request |
| Payment terms | T/T 30% deposit / 70% before shipment; L/C at sight for container loads |
| Verified production floor space | 4,950 m² (SGS-verified) |
| Team | 137 staff across 7 production lines |
| Equipment | 149 machines including computerised saddle-stitch and edge-painting units |
| Monthly capacity | 200,000 pieces |
| Entity | Founded 2014; principal has worked in bag development since 2004 |
The Bespoke Process, Gate by Gate
A bespoke programme is a sequence of gates, each producing an artefact you can approve, reject or send back. The gates exist because every correction costs roughly ten times more at the next stage: a change to a dimension costs a pencil stroke during pattern drafting, a second sample during development, and an entire production run if it surfaces after cutting. Understanding where those multipliers bite is most of what separates a clean first run from an expensive education.
- Brief and feasibility. You supply drawings or references, a target retail price, a target volume and a deadline. The programme team tests the brief against material availability, construction capability and realistic cost, then returns a written feasibility note with the risks flagged before any deposit moves.
- Specification and costing. The brief becomes a technical pack: dimension drawings, panel schedule, material call-outs by tannery or mill reference, hardware finishes, stitch specification, tolerances and packing method. Costing follows from a line-item bill of materials plus a labour-minute estimate per operation.
- Pattern, grading and sourcing. The pattern is drafted and the marker calculated for yield — the percentage of the hide or roll that becomes saleable panels, which is the single largest hidden variable in leather costing. Materials, linings, trims and hardware are ordered or reserved at this gate.
- Prototype build. The first bag is constructed in the intended materials rather than a substitute. A prototype exists to expose problems while they remain cheap; expect comments about balance, roll, closure alignment and strap geometry rather than a finished article.
- Correction and second sample. Comments are applied to the pattern and specification, and a corrected sample follows. Complex constructions — framed openings, multi-compartment cases, moulded shells — routinely need this second pass before they behave correctly.
- Compliance and testing. Where the destination market requires it, materials are submitted for restricted-substance testing against the relevant framework, commonly REACH in the European Union and CPSIA in the United States, with textile components often certified to OEKO-TEX standards.
- Pre-production sample and golden seal. A sample from the bulk-intent material lot is signed off and physically retained. This is the reference against which inspection is judged; without a sealed reference, any dispute about bulk quality degenerates into competing opinions.
- Bulk production. Cutting, skiving, skiving-dependent folding, assembly, edge finishing and hardware setting run to the sealed reference, with in-line checks at the operations where defects are cheapest to intercept.
- Inspection and release. Finished goods are sampled to the agreed inspection plan, packing is verified against carton specification, and the balance payment releases the shipment.
- Logistics and repeat. Goods ship on the agreed Incoterm with documentation for customs. The retained pattern, specification and tooling make every subsequent run faster and cheaper than the first.
| Gate | Artefact you receive | Typical duration | What can go wrong |
|---|---|---|---|
| Feasibility | Written feasibility note with target cost band | A few working days | Target price incompatible with the requested construction |
| Specification | Technical pack and bill of materials | One to two weeks with the buyer | Unresolved material call-outs carried into costing |
| Pattern and sourcing | Pattern, graded marker, yield calculation | Concurrent with specification | Tannery lot unavailable; colour standard cannot be held |
| Prototype | Physical first build with comment log | 6–10 working days | Prototype built in substitute material, hiding real behaviour |
| Correction | Corrected sample | 6–10 working days; 12–15 for complex builds | Unclear comments leading to repeat rounds |
| Compliance | Test reports against the required framework | Laboratory dependent | Late submission delaying bulk authorisation |
| Pre-production | Golden sample and signed specification | Sign-off dependent | No physical seal retained, weakening later inspection |
| Bulk | Production units with in-line records | 35–50 days after sample approval | Material arrival or line capacity slipping |
| Inspection | Inspection report against the agreed AQL | A few working days | Standard negotiated after production rather than before |
| Logistics | Shipment with commercial documents | Transit dependent | Documentation errors delaying customs clearance |
The two gates buyers most often try to compress are prototype correction and pre-production sealing. Both are false economies. A second sample costs a few hundred dollars and a week; discovering the same fault after fifteen hundred units are cut costs the run. The sampling and minimum-order guide sets out what each round legitimately costs and how many revision cycles are normal before a style is ready for bulk.
Why Bespoke Bags Cost More: Seven-Drivers
Bespoke pricing is not arbitrary, and it is rarely a margin grab. It reflects identifiable costs that a catalogue style has already amortised across thousands of units and dozens of previous customers. Seven drivers account for most of the gap, and each one is either visible in your brief or controllable by changing it.
- Development labour. Pattern drafting, grading, marker planning and the first construction sequence are borne entirely by your order. Later runs do not carry them again, which is why second-season pricing steps down.
- Tooling. A bespoke logo badge, an embossing plate, a custom zip pull or a moulded shell component each require tooling with its own lead time and cost. You are buying exclusivity as much as metal.
- Material minimums. Tanneries and mills sell in lot sizes. A bespoke colourway may require a hide purchase larger than your immediate consumption, with the balance held as reserved stock against your repeats.
- Yield. An original silhouette wastes more leather than a mature pattern that has been iteratively improved. Every extra square decimetre of offcut is cost without revenue attached.
- Learning curve. The first hundred units of a new construction are slower than the thousandth. Operators establish the correct feed rate, skive thickness and fold sequence empirically, and that time is real cost.
- Construction intensity. Hand-finished edges, turned-and-stitched construction, piped seams and hand-set hardware add labour minutes that compound across a run of five hundred.
- Sampling rounds. Each correction cycle is paid work. Two rounds is normal; five suggests the brief was ambiguous rather than that the producer is inefficient.
Roughly half of those drivers shrink with volume and the other half are fixed by design. Tooling is fixed: it costs the same whether it serves five hundred units or five thousand. Learning curve and yield improve with volume. Construction intensity is a design decision you make once and then live with. The practical implication is that the honest conversation about cost is not 'how cheap can this be' but 'which elements are we paying to own and which can we borrow from an existing library'. If your differentiation lives in the silhouette and the hardware, spend there. If it lives in the colourway and the lining story, borrow the base and spend your budget on materials.

There is also a cost of ownership worth naming. A bespoke specification you control lets you move production later if the relationship, the tariff picture or the freight economics change. A private label design does not: the specification belongs to the producer, and switching means starting again. Buyers who treat that option value as part of the price tend to make calmer decisions about a five-unit difference in FOB cost.
Materials and Construction: Where Quality Actually Lives
Two bags can share an outline and differ by years of service life. The difference sits in decisions that are invisible in a photograph: whether the hide is full-grain or corrected, whether the panel is lined or merely faced, whether edges are painted or bound, whether stress points are reinforced with a hidden stay. A serious specification addresses all of them explicitly, because anything left to default will be resolved by somebody else's cost model.
| Element | Economy execution | Premium execution | How to verify |
|---|---|---|---|
| Base material | Corrected grain with heavy pigment finish | Full-grain hide, aniline or semi-aniline dyed | Request tannery reference and finish specification |
| Panel structure | Single ply with fabric backing | Reinforced ply with hidden interlining at stress zones | Cut a sample; inspect the cross-section under light |
| Edge finish | One coat of edge paint | Multi-coat paint sanded between layers, or turned and burnished | Run a fingernail along the edge; feel for ridges |
| Stitching | Machine lockstitch at standard density | Higher stitch density with back-tacking at terminations | Count stitches over a measured inch |
| Hardware | Plated zinc alloy, unspecified plating thickness | Solid brass or stainless with stated plating specification | Request plating micron thickness and salt-spray test result |
| Lining | Loose poly lining | Suede, canvas or microfibre cut to pattern with pocket engineering | Check lining tension and pocket reinforcement |
| Base protection | None | Metal feet, reinforced base board, or both | Set the loaded bag down and watch the silhouette |
Translate these choices into a written tolerance before bulk starts. 'Edges cleanly finished' is not a specification; 'edge paint applied in three coats, sanded between coats, no visible ridges under raking light at 300 mm' is. The same discipline applies to colour, where a retained reference swatch and a sealed golden sample per colourway are the only reliable defence against drift across hides, lots and seasons.
Independent frameworks help here because they convert opinion into evidence. Sampling plans derived from ISO 2859-1, expressed as an AQL of 2.5 under single sampling at general level II, give both sides a shared arithmetic rather than a shared adjective. Restricted-substance compliance to REACH or CPSIA and textile certification to OEKO-TEX do the same for chemistry. Tannery audits under Leather Working Group protocols address the ethical questions that increasingly appear in brand procurement questionnaires. None of these are decoration; each is a sentence you will later need in writing.
What a Genuine Bespoke Partner Should Provide
Because the market uses the word loosely, due diligence matters more than vocabulary. A partner running genuine bespoke programmes will evidence capability in documents rather than adjectives: a versioned technical pack, a marked pattern with yield calculation, a line-item bill of materials, retained golden samples, and a written inspection standard. If those artefacts cannot be produced, the programme is customisation regardless of what the proposal says.
- A versioned technical pack naming every material by reference, not by description.
- A marked pattern and yield calculation, showing consumption per unit.
- A line-item bill of materials with an explicit substitution policy.
- A retained pre-production sample, physically held for the life of the programme.
- A written inspection standard agreed before bulk authorisation, stating the AQL and the defect classification.
- A documented position on exclusivity: which elements, which territories, for how long.
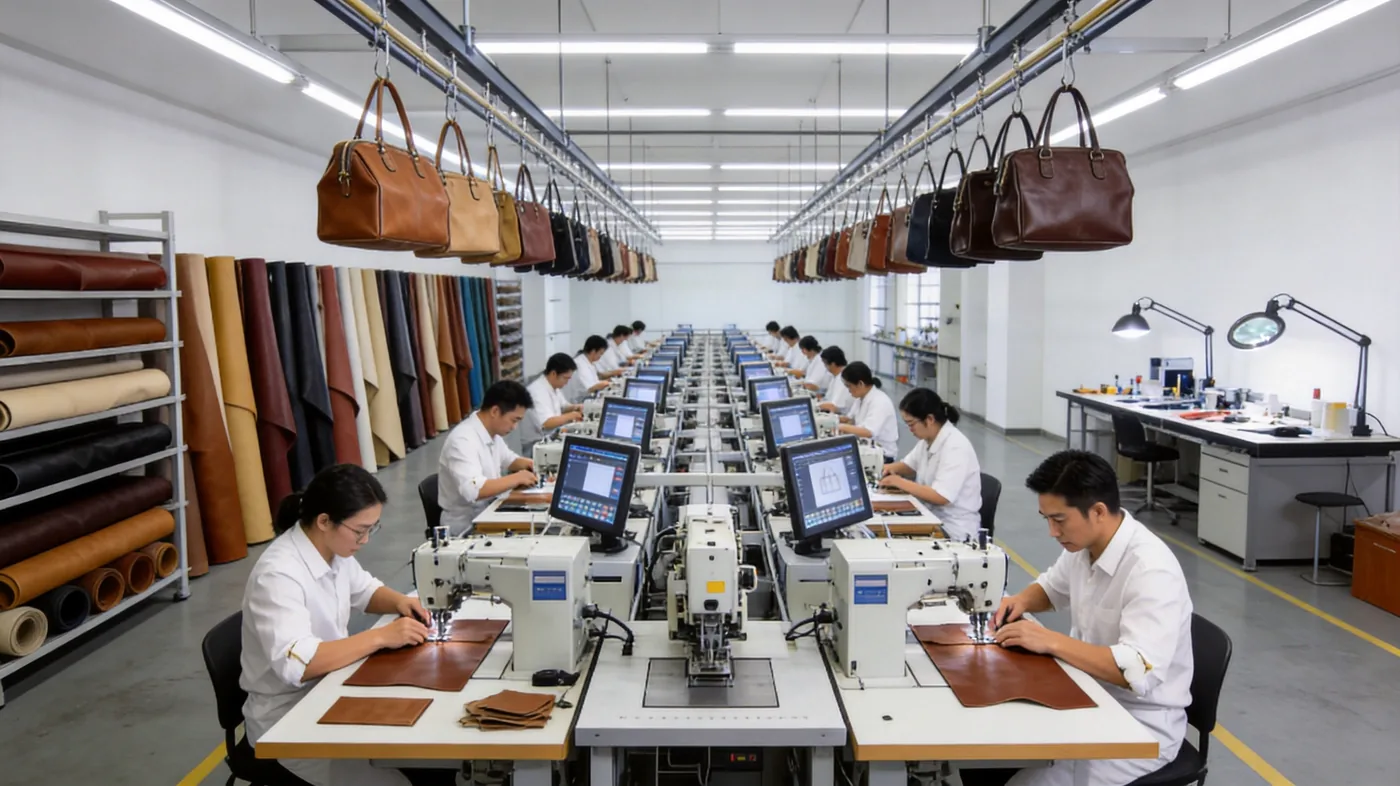
Ask also about the floor the work happens on, because capability is physical. Our SGS-verified production floor in Quanzhou covers 4,950 m² with 137 staff, seven lines, 149 machines and a capacity of 200,000 pieces per month; the entity dates from 2014, though the principal has worked in the trade since 2004. Those numbers are a context for scale decisions, not a boast — the relevant question is always whether the specific construction you want sits inside the line's demonstrated competence.
When Bespoke Is the Wrong Answer
Honest advice includes telling a buyer not to commission. Three situations make bespoke the wrong route, and in each the money is better spent elsewhere. If your differentiation is entirely in graphics, buy a well-made base style and invest in print, packaging and storytelling. If your deadline leaves less than the sampling window plus the 35–50 day bulk window after sample approval, no amount of goodwill compresses an ISF filing or a sewing line. And if your first order cannot absorb development costs at a unit price your retail strategy supports, a customised or small-batch pilot route will get you to market evidence faster and with less capital at risk.
| Situation | Recommended route | Reason |
|---|---|---|
| Differentiation is graphic or colour-led | Customised base style | Spend the budget where the customer perceives it |
| Deadline inside 70 days from today | Private label or existing tooling | Sampling plus bulk plus freight exceeds the window |
| First season below standard minimum | Small-batch pilot | Buys sell-through evidence before full commitment |
| Category filler to complete a range | Made-to-measure adaptation | Range completeness does not need a new silhouette |
| Signature piece defining the brand | Bespoke, full development | Exclusivity and control justify the development cost |
Reading a Bespoke Proposal Without Being Misled
Proposals are written to be accepted, so read them for what is absent as much as for what is present. The most informative paragraph in any quotation is the exclusions clause, because it tells you precisely what you will later be asked to pay for. Four omissions account for most cost escalations between first quote and final invoice.
- Tooling stated separately. If tooling is folded silently into unit cost, you do not know what you own and cannot take it elsewhere. Ask for it line-itemed.
- Material call-outs by reference. 'Top-grain leather' is a category, not a specification. A tannery reference, finish and thickness allow you to quote the same bag elsewhere and compare honestly.
- Inspection standard named. Without an agreed acceptable quality limit and defect classification, every disagreement becomes negotiable in the producer's favour.
- Incoterm and payment terms stated. A quotation on FOB Xiamen terms and one towards EXW, CIF or DDP on request are different prices for the same bag, and the difference is not small at distance.
- Sampling rounds capped. A fixed number of included revisions aligns incentives; unlimited revisions invite ambiguity and delay.
Freight is the last place budgets quietly fail. A quotation that lands goods on your dock and one that leaves them on a vessel in Fujian differ by a sum that, at today's rate volatility, can exceed a whole season's margin. Settlement is conventionally T/T with a 30% deposit and the 70% balance before shipment; ask what documentation accompanies each payment, because those documents are what your customs broker will eventually need.
The value of getting the definition right is that everything downstream follows from it. A genuine bespoke bag gives you a specification you own, a cost structure you can explain, a quality standard you can enforce, and a route to a second production partner if circumstances demand one. Those four things are what the premium actually purchases, and they are what separates a considered commission from an expensive shopping trip. Programmes begin with a conversation rather than a purchase order; the contact channels carry direct routes to the programme team.
Define your bespoke specification
Send drawings, target price and intended volume. The programme team will return a written feasibility note covering construction route, material options, sampling window and cost band before any deposit is discussed.
Frequently Asked Questions
What does bespoke mean when it is applied to bags?
Bespoke means the bag did not exist before you commissioned it. The silhouette is drawn from your brief, the pattern is drafted and graded specifically for it, and the leather, lining, hardware and tolerances are chosen to suit that construction. Removing all branding still leaves an object unlike anything else on the market. Anything less is customisation or private label, both of which are legitimate but cheaper and rarely exclusive.
Why do bespoke bags cost more than similar-looking designer bags?
Because development is amortised over one order instead of many. Pattern drafting, tooling, material lot minimums, lower cutting yield on an unrefined pattern and the operator learning curve all sit in the first run. Volume reduces several of these: the learning curve flattens, yield improves as the pattern is refined, and repeat orders drop the development cost entirely. Tooling, however, is a fixed cost independent of quantity.
How long does it take to produce bespoke bags from first sketch?
Allow 6–10 working days for a sampling round, or 12–15 days for complex constructions such as framed openings and multi-compartment cases, then 35–50 days for bulk after sample approval. Freight, customs and any laboratory testing sit on top of those figures. A realistic planning horizon from conversation to delivered goods is therefore measured in months rather than weeks for a first programme.
What minimum quantity applies to bespoke bags?
The standard minimum is 500 pieces per style and colourway, which reflects line set-up economics rather than material constraints. Small-batch pilots below that threshold can be negotiated where the construction allows it and where the purpose is market testing before a full commitment. A pilot quantity carries a higher unit cost but converts an unknown sell-through assumption into evidence.
Can I own the pattern and tooling for my bespoke bag?
Patterns developed to your brief can be contractually ring-fenced for your exclusive use, and tooling you have paid for is normally yours to redirect. Both depend entirely on being written into the agreement before development begins: without an explicit clause, default positions vary and the pattern may remain available to others. Confirm ownership, permitted use and what happens to the tooling if you move the programme.
Are bespoke bags higher quality than mass-produced bags?
Bespoke permits higher quality but does not guarantee it. The advantage is control: you specify the tannery reference, the edge finish, the stitch density, the hardware plating thickness and the inspection standard. If those are left to default, a bespoke bag can be built to exactly the same standard as any other. The quality comes from the specification, not from the label.
What is the difference between bespoke and made-to-measure bags?
Made-to-measure adapts an existing pattern to your dimensions: a laptop bay, a garment length, a wheel base. The silhouette itself is not redrawn. Bespoke drafts the silhouette from scratch. Made-to-measure reaches production faster and costs less in development, which is why it suits category fillers, whereas bespoke suits signature pieces where exclusivity carries commercial value.
Which materials are best for a first bespoke bag run?
Full-grain or lightly corrected bovine leather in a mid-weight offers the widest tolerance window, forgiving both machine settings and operator variation while ageing well. Very soft nappa and heavy bridle leather are less forgiving: they demand tighter process control and a more experienced line. For a first run, choose the material that tolerates imperfection rather than the one that photographs best.
How do I know whether a supplier is genuinely offering bespoke?
Ask for artefacts. A genuine programme produces a versioned technical pack, a marked pattern with a yield calculation, a line-item bill of materials with tannery references, a retained golden sample and a written inspection standard naming the acceptable quality limit. Producers offering decoration on shared base styles cannot produce these documents, because the specification is not yours to see.
What inspection standard should I use for bespoke bags?
A single sampling plan built on ISO 2859-1 at an AQL of 2.5 under general level II is the common trade baseline, agreed in writing before bulk authorisation and accompanied by a classified defect list distinguishing critical, major and minor faults. Agreeing it afterwards converts a quality question into a negotiation you will lose, because the goods already exist.
Can bespoke bags be produced sustainably?
Yes, though the levers are material and durability rather than marketing. Traceable hides from Leather Working Group audited tanneries, chrome-free or vegetable tanning, OEKO-TEX certified linings and a longer service life all reduce genuine impact. The most effective single measure is durability: a bag lasting ten years spreads its footprint across a decade of use.
Do I need my own drawings before approaching a bespoke partner?
Drawings help but are not mandatory. A clear brief containing reference photographs, target dimensions, intended use, target retail price, quantity and deadline is sufficient to open a feasibility conversation. What matters is knowing which elements define your brand and which are negotiable, because that distinction is what the feasibility note will test against real material and labour costs.
What payment terms are usual for a bespoke bag order?
The conventional structure is T/T with a 30% deposit to release materials and development, and the 70% balance before shipment. Tooling is usually invoiced separately at the start. Make sure the quotation states the Incoterm explicitly — FOB Xiamen is standard, with EXW, CIF or DDP available on request — because the same bag produces very different landed costs under each.
Can a bespoke bag design be used again for future seasons?
Yes, and this is where the economics improve. Retained patterns, sealed golden samples and existing tooling mean repeat runs skip most development stages: sampling is confirmation rather than exploration, tooling is already paid for, and yield improves with each refinement. Buyers frequently find the second season lands at a materially lower unit cost than the first for identical specification.
What should I ask before signing a bespoke bag agreement?
Five things: who owns the pattern and the tooling; what is exclusive, in which territories and for how long; what the inspection standard is and when it was agreed; what the substitution policy allows without your written approval; and what happens to retained samples and reserved material lots. Each answer should appear in the agreement itself rather than in an email thread.
Are bespoke bags worth commissioning for a small brand?
They are when one signature style carries the brand's identity and the rest of the range can ride on adapted base patterns. Commissioning bespoke across an entire first collection consumes capital and development time faster than a new label usually recovers it. Start with one hero piece built properly, learn from how customers respond to it, then extend the bespoke content of the range.